The Differences Between Investment Casting and Sand Casting
When a metal component has a complex shape, tight dimensional requirements, or a large amount of machining would be required after casting, the choice of casting process can have a major effect on production cost and part quality. Two established options are investment casting and sand casting. Although both processes produce metal components from molten metal, they use very different mold-making methods and are suited to different manufacturing requirements. The process of reproducing the needed component geometry with the help of a disposable wax pattern and ceramic shell is known as investment casting or lost-wax casting. Sand casting A reusable pattern is used to form a hollow in bonded or chemically treated sand. The types of mould construction influence the dimensional accuracy, surface polish, complexity of the design, tooling, economics of manufacturing, and quantity of machining needed after casting. Neither technique is inherently preferable for all applications. A relatively big, and simple part may be more affordable to make by sand casting, whereas a smaller part with intricate passageways and limited machining allowance may justify the additional tooling and processing required in investment casting. Being aware of these variances allows engineers, sourcing teams, and manufacturers to choose a casting technique depending on the real needs of the product instead of a broad preference for one process.
How Do the Two Casting Processes Work?
Investment Casting Process
Investment casting starts with the fabrication of a wax pattern that is a duplicate of the shape of the finished part. For mass production the wax pattern is usually made with a special-purpose die. A plurality of wax designs may then be joined on a runner system to form a cluster.
The wax assembly is dipped several times into ceramic slurry and refractory material to construct a shell around the designs. Remove the wax when the shell is of sufficient thickness and strength. The mold cavity is the resultant hollow ceramic shell. The hot shell is filled with molten metal and then dried and fired as required.
When the metal has cooled, the ceramic shell is torn away and the individual castings removed from the runner system. Additional procedures such as heat treating, shot peening, grinding, dimensional control, or CNC machining may be performed, depending on component needs.
This procedure involves more steps than standard sand casting, but the ceramic shell reproduces precise geometric detail and reasonably smooth surfaces.
Sand Casting Process
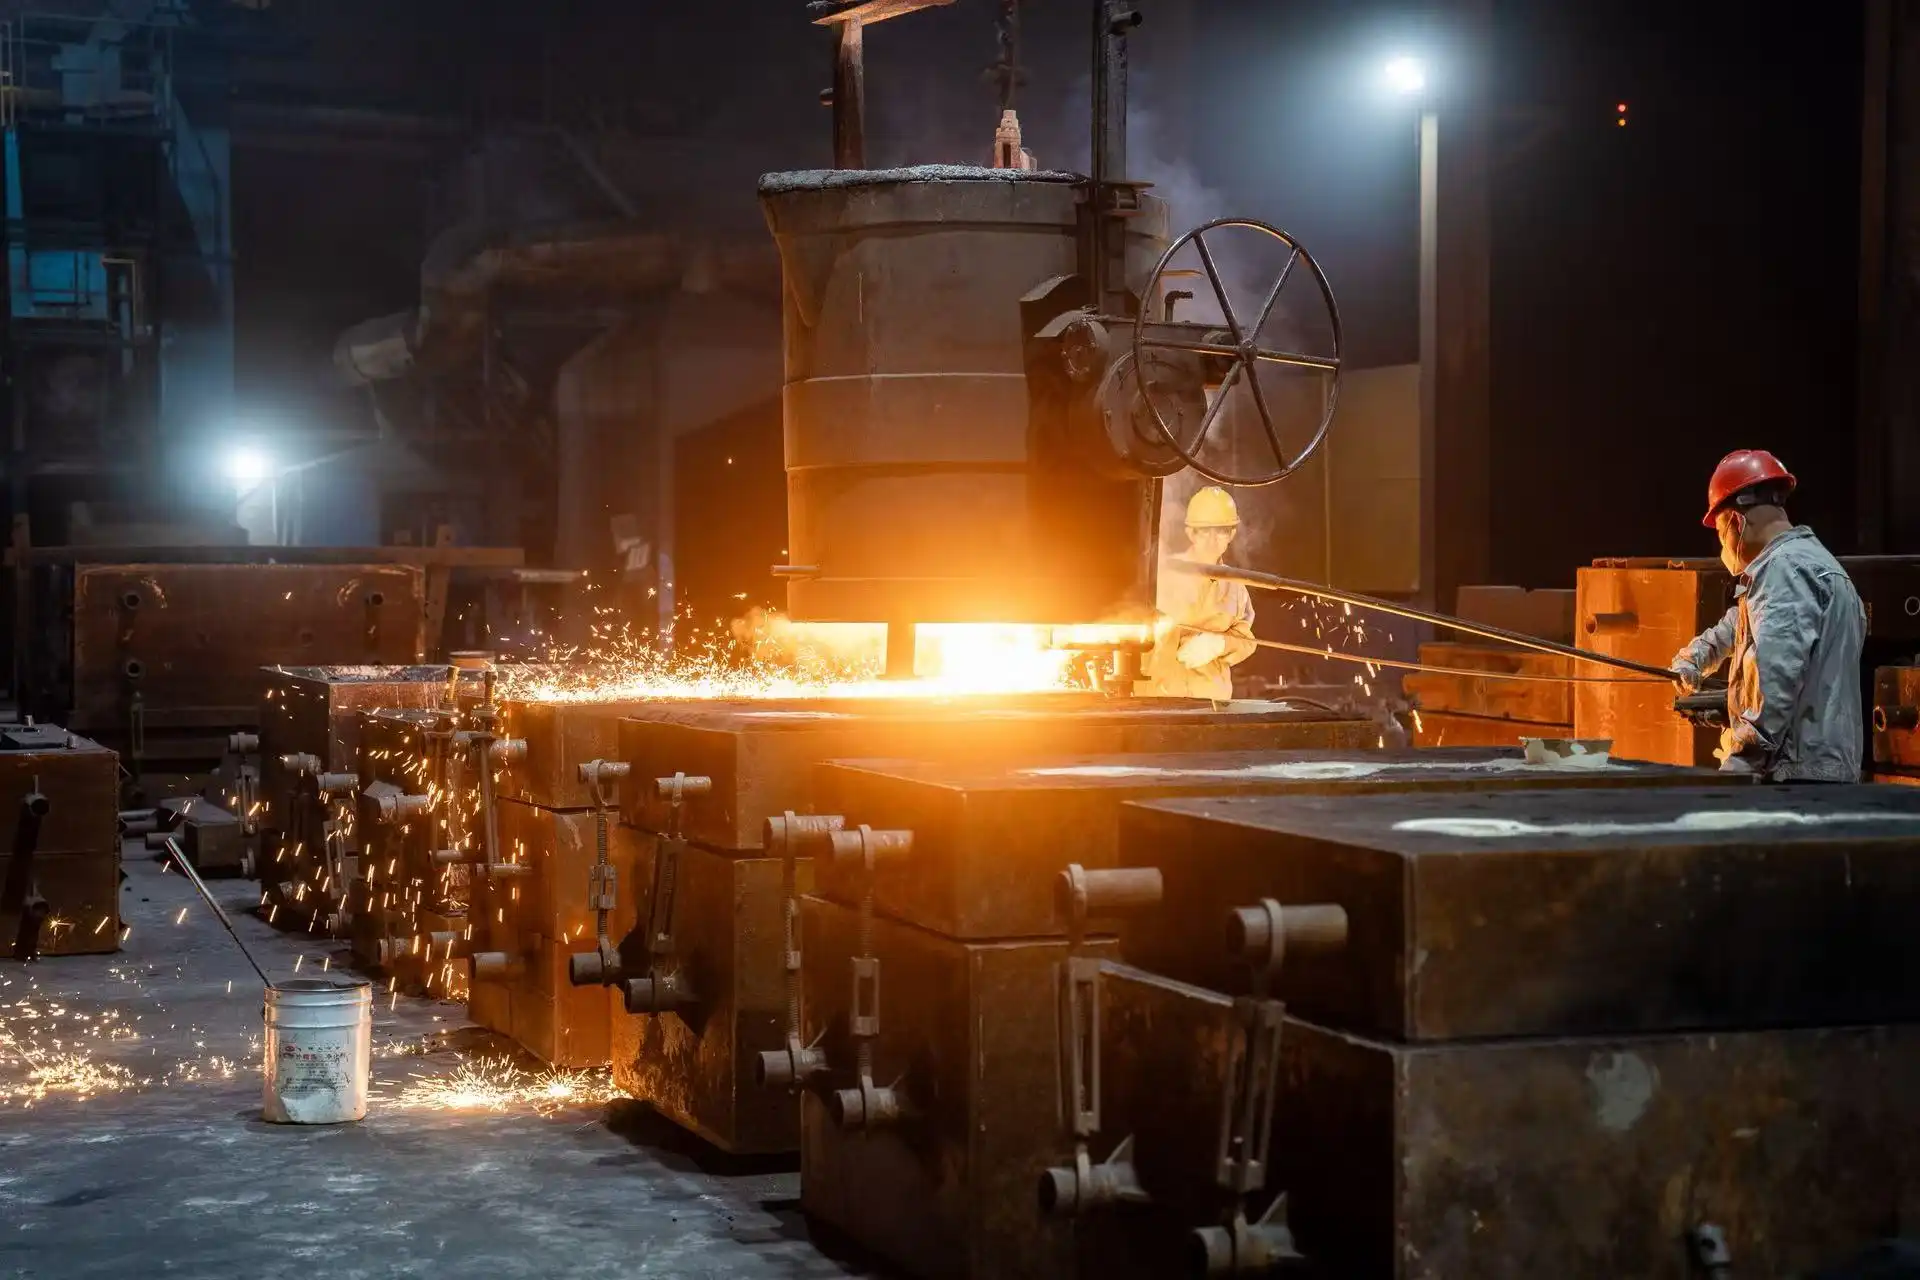
Sand casting begins with a pattern that defines the outside shape of the component to be cast. The pattern is set in moulding sand to create a hollow. When the design is taken out, it leaves a hole in the sand mold.
Core materials are used for castings that require internal channels or hollow parts. The mold is then closed, and molten metal is poured into the hollow. The sand mold is shattered after solidification so as to remove the casting.
One of the key benefits of sand casting is its flexibility. Patterns can be made from a variety of materials and customized for specific needs. The casting method can be adapted to anything from quite small parts to extremely massive castings. It is also extensively used for prototypes, replacement parts, machinery components, and production runs where the surface polish and dimensional precision do not warrant the added expense of an investment casting technique.
Where Investment Casting Has a Technical Advantage?
Surface Finish and Dimensional Reproduction
The most obvious difference between the two techniques is the surface that results from the mold. Investment casting employs a fine ceramic shell, which can reproduce fine detail and usually results in a smoother as-cast surface than typical sand molds.
This can minimize the amount of cleanup and machining that is required after casting to the surface. The alloy, shell system, pattern quality, casting geometry, and process control all influence the actual outcome, although the method is well suited to components where the as-cast surface is a critical factor.
Sand casting usually results in a relatively coarse surface since the mold cavity is made of sand particles. Machining can improve important surfaces, but the cost of material and processing time increase with increased machining.
For a component with multiple external contours, it can be profitable to reduce the machining allowance. That nevertheless, engineers should still specify machining on surfaces that require strict dimensional control, rather than presuming that every cast surface would automatically satisfy a finished-part tolerance.
Complex Geometries and Fine Features
Investment casting is particularly suitable when a component has complex curves, thin sections, small features, or geometries that would be difficult to make in a cost-effective way with conventional machining.
Wax is easy to shape into complex forms, and the disposable pattern can replicate features that would be hard to remove from a standard hard mold. Internal channels can also be incorporated in properly built cores.
Sand casting also allows for complicated designs, especially with the use of cores, although the practical limitations are highly dependent on the geometry of the part, the design of the mold, the configuration of the cores, and the dimensional accuracy needed.
The point is not that investment casting can achieve complexity that sand casting cannot. Investment casting can be a more practical solution for certain complex geometries when the alternative would be substantial machining, several components, costly equipment, or difficult assembly.
Reduced Machining Requirements
Another reason manufacturers turn to investment casting is near-net-shape production. If the casting is near the final necessary geometry, material removal by CNC machining may be minimized.
This can be particularly useful for parts with uneven exterior profiles and for alloys that are difficult to manufacture. Rather than beginning with a huge casting and subtracting vast quantities of material, the casting process can be structured to yield a geometry that needs to be machined just at key interfaces and functioning surfaces.
The savings should be considered on a total manufacturing basis. Reduced machining does not inherently make investment casting cheaper, as it has greater pattern and shell-making costs. The proper decision depends on the link between tooling, casting, machining, material utilization, manufacturing quantity, and inspection needs.
Cost Comparison: Which Process Is More Economical?
Tooling and Pattern Costs
Sand casting is usually the method of choice when tooling is to be kept to a minimum investment. Depending on the process used, sand molds can be made using relatively inexpensive templates, and some projects may be easier to modify.
Mass manufacturing of investment castings usually needs a dedicated die for the wax pattern. This increases the initial tooling cost and engineering time. The economic advantage is more pronounced when the same component is made frequently, because the tooling cost can be spread over a larger number of pieces.
However, the tooling strategy for prototypes or extremely low-volume production may be different. Manufacturers may employ other pattern-creating technologies such as additive manufacturing, where applicable. So the tooling cost needs to be discussed with the casting provider based on the required quantity and production route, and not just based on the name of the casting process.
Part Cost and Production Volume
Investment casting pattern making, shell preparation, wax assembly, ceramic processing, casting, and finishing determine the cost per part. For relatively simple components where you can get away with sand casting at a cheaper cost, these extra steps can be a less desirable technique.
At the same time, a simple price comparison for casting may be misleading. A sand-cast component may be cheaper to cast initially but much more to machine subsequently. An investment cast part may cost more per casting but requires less machining.
Procurement teams should look at the whole cost of manufacturing rather than just the price of the raw casting. A good comparison involves tooling, casting, heat treatment, machining, finishing, inspection, scrap, material consumption, and estimated production quantity.
Long-Term Manufacturing Economics
The most economical casting process depends on the complete production line. The economics of investment casting might be beneficial for a mass-produced part if its dimensional consistency and near-net form capability cut down on downstream machining.
Sand casting remains very competitive for big components, basic geometries, prototypes, replacement parts, and applications where a rougher as-cast surface is acceptable.
It matters how much is produced. A tooling expenditure that looks pricey for 50 pieces may be relatively negligible when amortized over several thousand parts. However, for a one-time job, a large initial investment in tooling may not be justifiable.
Material Selection and Casting Capability
Common Investment Casting Alloys
Investment casting can be used with many ferrous and non-ferrous alloys. Depending on the foundry's equipment and process capability, common choices can include stainless steels, carbon steels, alloy steels, aluminum alloys, nickel-based alloys, and cobalt-based alloys.
The suitability of a specific alloy depends on melting equipment, shell materials, pouring conditions, component geometry, heat treatment, and quality requirements. High-temperature alloys can require specialized process control, so alloy selection should be confirmed with the foundry before the design is finalized.
Common Sand Casting Materials
Sand casting also supports a broad range of metals. Cast iron, carbon steel, alloy steel, aluminum alloys, copper alloys, and other materials can be produced through different sand-casting systems.
This is why it would be inaccurate to select a process simply because one casting method is assumed to support more alloys than the other. The more useful question is whether the chosen foundry has proven experience with the required alloy and can meet the customer's mechanical, dimensional, and inspection specifications.
For procurement teams, material certificates, heat-treatment requirements, chemical composition, mechanical testing, and traceability should be considered during supplier evaluation.
Which Applications Suit Each Casting Method?
Aerospace and High-Performance Components
Investment casting is frequently considered for aerospace and other demanding engineering applications where complex geometry, material capability, and dimensional control are important. Components such as turbine-related parts, structural components, brackets, housings, and other intricate metal parts may benefit from the process.
However, aerospace applications normally involve strict material specifications, inspection requirements, traceability, and process qualification. The suitability of investment casting should therefore be evaluated against the applicable drawing, material specification, and quality standard rather than based only on the industry's general use of the technology.
Automotive and Industrial Equipment
Both casting methods have extensive applications in automotive and industrial equipment. Investment casting can be useful for compact components with detailed geometry, while sand casting is often suitable for larger housings, machinery bodies, brackets, pump components, and other parts where the geometry and production requirements fit the process.
For automotive production, factors such as annual volume, cycle time, machining requirements, dimensional consistency, material utilization, and the suitability of investment casting can determine which process provides the better overall solution.
Pumps, Valves, and Flow-Control Components
Cast components used in pumps and valves can contain internal cavities, passages, flanges, bosses, and other features that influence mold and core design.
Investment casting can be advantageous when the component is relatively intricate and dimensional reproduction is important. Sand casting can be preferable for larger valve bodies, pump housings, and other components where size, production economics, and structural requirements make the process practical.
The final selection should consider pressure requirements, wall thickness, machining surfaces, internal passage geometry, material specification, and required inspection methods.
General Machinery and Replacement Parts
Sand casting is particularly useful for machinery components and replacement parts where flexibility and cost are important. Large or irregular components can often be produced without the extensive pattern and ceramic-shell process required for investment casting.
Investment casting becomes more attractive when the replacement component has a complicated shape, limited production volume but high machining cost, or features that are difficult to reproduce economically using conventional sand molding.
Investment Casting vs. Sand Casting: A Practical Selection Guide
When choosing between the two methods, engineers should start with the component rather than the casting process. The first consideration is geometry. If the part contains numerous small features, thin sections, intricate contours, or difficult-to-machine areas, investment casting may deserve closer evaluation.
The second consideration is size. Very large components can often be more practical for sand casting because the process can accommodate substantial mold dimensions. Smaller and moderately sized precision components are frequently stronger candidates for investment casting.
The third consideration is dimensional and surface requirements. If extensive machining is already planned for most of the component, the surface-finish advantage of investment casting may provide less value. If many surfaces need to remain close to the as-cast condition, the investment process may offer a greater manufacturing advantage.
Production quantity is another important factor. Investment casting tooling becomes easier to justify as the number of parts increases, while sand casting can remain attractive for smaller runs and projects where pattern flexibility is important.
Finally, the decision should include downstream operations. Heat treatment, machining, grinding, surface treatment, inspection, assembly, and material utilization can have a significant impact on the final cost.
What Buyers Should Discuss With a Casting Supplier?
A casting supplier needs more than the part name to determine the appropriate process. Buyers should provide the latest component drawing, 3D model when available, material grade, annual or batch quantity, dimensional requirements, critical tolerances, machining requirements, surface-finish expectations, heat-treatment requirements, and applicable inspection standards.
It is also useful to identify critical features early. Holes, sealing surfaces, bearing seats, threads, mating surfaces, and pressure-containing areas may require different machining or inspection strategies from the general casting surface.
A qualified supplier should be able to review the geometry and recommend a suitable casting route based on manufacturability and total production requirements. For complex parts, early communication between the design engineer and foundry can also help identify unnecessary machining allowances, difficult core arrangements, excessive wall-thickness changes, or other features that could affect casting yield.
Conclusion
Finally, investment casting and sand casting serve different manufacturing priorities, and the better choice depends on the requirements of the individual component. Investment casting is well suited to relatively intricate parts that benefit from detailed geometry, good as-cast surface quality, and near-net-shape production. It can reduce machining requirements when the casting is properly designed and the production volume supports the required tooling and processing costs.
Sand casting remains a practical and economical solution for many large, simple, irregular, prototype, and lower-volume components. It offers considerable flexibility in pattern and mold production and can support a broad range of engineering alloys.
The most effective way to choose between the two is to compare the complete manufacturing route rather than looking only at the initial casting price. Geometry, component size, alloy, production quantity, dimensional requirements, machining, inspection, tooling, and delivery requirements should all be evaluated together.
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd., established in 2001, provides customized metal components for customers in multiple industries. The company holds ISO 9001:2015 and API-7-1 certifications and supports forging, sand casting, investment casting, centrifugal casting, and machining. Its material capabilities include iron, steel, stainless steel, aluminum, copper, zinc, and various alloys.
For projects that require a comparison between sand casting and investment casting, Welong's engineering team can evaluate the component geometry, material, production quantity, machining requirements, and quality specifications to help determine a suitable manufacturing route. Its production and quality-control capabilities are supported by an experienced technical team and international supply-chain experience, with customers across Europe, North America, Asia, and Oceania. For inquiries, please contact us at metal@welongpost.com.
FAQ
1: What is the main difference between investment casting and sand casting?
The main difference is that investment casting uses a wax pattern and ceramic mold for greater precision and surface finish, while sand casting uses sand molds for larger, simpler parts.
2: Which casting method is more cost-effective for large production runs?
Sand casting is generally more cost-effective for large production runs, especially for simpler part geometries.
3: Can investment casting produce more complex parts than sand casting?
Yes, investment casting can produce more complex and intricate parts with finer details compared to sand casting.
4: What industries benefit most from investment casting?
Aerospace, medical, dental, automotive, and racing industries benefit significantly from investment casting due to its precision and ability to work with specialized alloys.
References
1. Smith, J. D. (2018). "Advanced Casting Technologies: A Comprehensive Guide to Investment and Sand Casting." Materials Processing Handbook, 3rd Edition.
2. Johnson, R. E., & Amstead, B. H. (2019). "Comparative Analysis of Investment and Sand Casting Processes in Modern Manufacturing." Journal of Materials Engineering and Performance, 28(4), 2145-2160.
3. Chang, L., & Thompson, S. (2020). "Cost-Benefit Analysis of Investment Casting vs. Sand Casting in Aerospace Applications." International Journal of Metalcasting, 14(2), 412-425.
4. Williams, M. A., & Davis, K. L. (2017). "Surface Finish Characteristics of Investment Cast and Sand Cast Components: A Quantitative Study." Materials Science and Engineering: A, 695, 154-165.
5. Rodriguez, C., & Lee, S. H. (2021). "Advancements in Investment Casting Technology for Medical Device Manufacturing." Journal of Biomedical Materials Research Part B: Applied Biomaterials, 109(5), 720-735.
6. Brown, T. E., & Wilson, G. R. (2019). "Environmental Impact Assessment of Investment Casting and Sand Casting Processes." Journal of Cleaner Production, 225, 1235-1248.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

