What Equipment Is Needed for Open Die Forging
Open die forging uses localized compressive force to shape heated metal between dies that do not completely enclose the workpiece. Unlike closed-die forging, the material can be handled, turned, dragged out, upset or otherwise during the procedure. This makes the technique especially ideal for big shafts, rings, blocks, discs, flanges, pressure-vessel components and other pieces that may be too large or geometrically unsuitable for fully enclosed dies. The equipment required depends on the size and material of the workpiece, the amount of deformation required, the production volume and the final dimensional and inspection requirements. A tiny forging shop might be a quite simple mix of a furnace, a forging hammer or press, and some handling tools. Big industrial operations may need high-capacity hydraulic presses, motorised manipulators, overhead cranes, dedicated furnaces, tooling, temperature measuring, and inspection equipment. It is crucial to know this equipment when you are assessing a forging provider because the final quality is not determined by the machine. The combination of the forging machine, heating system, tooling, workpiece handling method, process control and inspection system determines if the finished forging will satisfy the specified specifications.
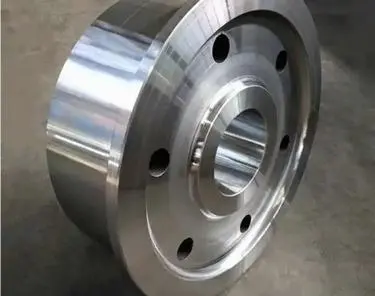
What Does an Open Die Forging Line Need?
A typical forging process can be broken down into a number of interrelated stages: heating, transfer, deformation, repositioning, cooling, inspection, and, in some cases, machining. For each stage there is a tool that suits the size and material of the workpiece.
The basic equipment generally includes a forging press or hammer, heating furnace, manipulator or other handling equipment, overhead cranes, forging dies and tools, temperature measuring instruments, and inspection equipment. Depending on the product, the production path may include cutting machines, descaling systems, heat-treatment equipment, and machining centers.
The equipment configuration must therefore be seen as a total production system and not as a list of individual units. For instance, a very large hydraulic press is not very useful if the shop cannot securely locate a multi-ton hot billet in the correct place under the dies. In the same way, a furnace of suitable size must be able to heat the entire workpiece evenly to the required degree for the intended deformation sequence.
How Do Hydraulic Presses and Forging Hammers Shape the Workpiece?
Hydraulic Presses for Controlled Deformation
They are also commonly employed in big and demanding open-die forgings, where they can apply huge forces at a controlled rate. The press delivers a compressive force with a controlled stroke rather than depending mostly on repetitive impact.
This feature is advantageous when a predictable deformation through a large cross section is desired in the forging process. The operators can regulate the ram movement and coordinate the press with the manipulator. The location of the workpiece can be continuously changed.
Hydraulic presses are particularly suited to massive shafts, discs, blocks, rings, and other heavy components. The capacity must be selected on the basis of greater than the stated weight of the forging. The amount of force required also relies on the strength of the material at the forging temperature, the size of the workpiece, the reduction ratio, the area of contact between the workpiece and die, and the sequence of deformation intended.
These factors are very crucial for a provider when evaluating a new forging project. A machine with sufficient lifting capacity might not be suitable if the available forging force or operating envelope is not adequate.
Forging Hammers for Repeated Impact
Forging hammers does not continuously push the metal but forms it by repeated strikes. The impact energy is transmitted via the tooling to the heated workpiece and allows the operator to progressively reduce or redistribute the cross-section.
Hammers are useful for roughing and drawing processes, especially if repeated deformation is useful. But the right hammer capacity relies on the workpiece size, material, tooling, and needed deformation. For large industrial forgings, equipment specialized for high-energy operations may be required rather than the smaller power hammers often associated with general blacksmithing.
The difference between a hammer and a hydraulic press is important for production planning. A hammer offers impact energy and repeated strikes, but a hydraulic press provides regulated force and stroke. The choice must therefore be based on the forging path and not on the presumption of superiority of one machine over the other.
When Are Screw Presses Used?
Screw presses are suitable for some forging applications where controlled energy and reasonably high forming force are required. Their functioning concept is different from that of a hydraulic press in that mechanical energy stored or created by the screw mechanism is turned into forming force.
But screw presses are not necessarily the first choice for all large open-die forging operations. Suitability relies on the part geometry, deformation required, production volume, tooling arrangement, and available machine capacity.
The main forming equipment for open die forging of big industrial free forgings is often represented by hydraulic presses and suitable forging hammers. Screw presses are to be considered an application-specific choice, not a general necessity.
Why Is the Heating System Critical to Forging Quality?
Gas-Fired Furnaces for Large Workpieces
The furnace should heat the workpiece to a suitable forging temperature and provide adequate temperature homogeneity throughout the material. This becomes more critical as the billet or ingot gets larger.
For big workpieces, open die forging often relies on gas-fired furnaces because they can accept huge loads and provide continuous heating over relatively large furnace chambers. The temperature required for forging can vary greatly depending on the alloy, so the furnace should be chosen based on the exact material specification rather than a general temperature range.
The heating cycle may also include a soak time to allow the interior of the workpiece to attain the desired temperature. Excessive heating is equally undesirable as insufficient heating, particularly for overheating-sensitive alloys. Thus, in process control, furnace temperature, workpiece temperature, heating duration, and appropriate forging range for the material should be considered.
Induction Heating for Localized and Controlled Heating
Using induction heating, heat is generated in the conductive metal using electromagnetic fields. It can heat quickly and with precision control; thus, it can be suitable for several forging applications and production arrangements.
Its application strongly depends on workpiece size, material, desired temperature profile, and manufacturing cycle. In applications where reproducible heating of certain areas is needed, induction systems can be especially helpful.
Very big forgings, however, may require a different heating method than that utilized for smaller billets. The choice of the system must consider the capacity of the furnace, the availability of the electricity, the geometry of the workpiece, and the time required to reach uniform temperature.
Electric Resistance Furnaces for Temperature Control
Electric resistance furnaces create heat by electrical resistance elements and may offer reliable temperature control. They may be used for materials and components requiring controlled heating conditions.
The many heating zones can also be used to allow operators to create varying temperature conditions along a lengthy workpiece if localized control is desired in a process. This may be advantageous in some specific forging processes.
Temperature monitoring should be part of the production operation, regardless of the type of furnace used. The furnace setpoint is not necessarily the actual temperature of the metal, and direct measurement of the workpiece may be necessary.
What Equipment Moves Heavy Forgings During Production?
Powered Manipulators for Positioning and Rotation
The manipulator is one of the most critical pieces of equipment in large-scale open-die forging. It grips the hot workpiece and transfers it relative to the forging machine.
The operator may have to turn the workpiece during a forging sequence, move it back and forth, modify the orientation of the workpiece, or put a particular area of the workpiece under the dies. These are performed with the assistance of a motorized manipulator, keeping the material at forging temperature.
The needed capacity of the manipulator relies on the maximum weight and size of the workpiece. Its gripping configuration must also match the forms being manufactured. A lengthy shaft, a huge disc, or an uneven billet may demand distinct handling procedures.
The synchronization of the manipulator and the open die forging machine is very critical. If there is misalignment, the workpiece and tools can be unevenly deformed, handled for longer than necessary, or even damaged.
Overhead Cranes and Hoists
Overhead cranes support almost every step in a major forging operation. They are used to unload incoming material, move billets to the furnace, transfer tooling, position workpieces, and move finished forgings to the following processing locations.
Crane capacity and working clearance must be evaluated together. The hook height, span, lifting accessories, or working area may not be suitable for the forging even if the crane is rated for a certain load.
Cranes are also necessary during die changes and maintenance. Properly structured lifting equipment enhances throughput and allows the production space to be organized around the actual movement of materials, as forging tools can be heavy and difficult to handle manually.
Tongs, Grips, and Specialized Handling Tools
Small forgings can be handled with tongs or special grips, while bigger pieces may need specific attachments used with manipulators or cranes.
The gripping surface must ensure sufficient contact, yet without hindering the area of deformation. Tool materials and dimensions must also survive repeated exposure to high temperatures and mechanical loading.
Special geometry workpieces can be fitted with handling tools to ease the positioning and to decrease the needless handling. The goal is not just to retain the workpiece but also to provide a steady and predictable location throughout the forging procedure.
Which Tooling and Support Equipment Are Also Required?
Open-Die Tooling and Forging Dies
The dies are the direct interface between the forging machine and the heated metal. Unlike closed dies, open-die tooling generally does not surround the entire workpiece. Common tools may include flat dies, V-dies, swages, mandrels, and other shapes designed for specific operations.
Different tooling configurations support different deformation methods. Flat dies can be used for compression and drawing, while V-shaped tools can help reduce and control a section. Mandrels may be used when producing or enlarging holes in suitable components.
Tool dimensions, material, surface condition, and alignment can influence the resulting forging. Tool selection should therefore be considered together with the required reduction, workpiece geometry, and machine capacity.
Cutting and Cropping Equipment
Some forging routes require the billet or ingot to be cut before forging, while others require cropping after deformation. Cutting equipment may include saws or other suitable systems depending on material size and production requirements.
Removing unwanted ends or excess material helps establish the correct starting geometry and can support subsequent machining. The cutting method should be compatible with the alloy and dimensions involved.
Descaling and Surface Cleaning Equipment
Heating can generate oxide scale on the surface of steel and other alloys. Removing loose scale during the forging process can help maintain a cleaner working surface and reduce the amount of unwanted material carried into later operations.
The appropriate descaling method depends on the material, temperature, equipment configuration, and production requirements. For some large industrial forgings, water-based descaling systems can be integrated into the forging line.
Temperature Measurement Systems
Temperature measurement is an important part of process control because forging should be performed within the appropriate working range for the material.
Depending on the application, manufacturers may use infrared pyrometers, thermocouples, or other temperature measurement methods when performing open die forging. The measurement method should account for the workpiece surface condition, emissivity, accessibility, and operating temperature.
Accurate temperature information allows operators to make better decisions about when to transfer a workpiece from the furnace, when to continue forging, and when reheating may be necessary.
What Inspection Equipment Is Needed After Forging?
Equipment selection should not stop when the final forging blow is completed. Inspection is an important part of confirming that the finished component meets dimensional, material, and quality requirements.
Dimensional inspection equipment can include calipers, micrometers, height gauges, templates, and coordinate measurement systems, depending on the required accuracy and component size.
For applications with demanding internal quality requirements, non-destructive testing may also be specified. Ultrasonic testing is commonly used for suitable forged components because it can help identify internal discontinuities that cannot be detected through visual inspection alone. Other inspection methods may be selected according to the material, specification, and customer requirements.
Surface inspection is also important. Operators may examine the forging for visible laps, cracks, seams, scale-related issues, or other surface conditions before the component proceeds to heat treatment or machining.
The inspection plan should be established before production begins. This helps ensure that the forging process, heat treatment, machining allowance, and inspection methods are compatible with the customer's final requirements.
How Should a Manufacturer Choose the Right Equipment?
Choosing equipment for open die forging starts with the component rather than the machine. Several factors should be reviewed before selecting a production route.
The first is material. Carbon steel, alloy steel, stainless steel, nickel-based alloys, titanium, and other materials can have different forging temperature ranges and deformation characteristics.
The second is component size and weight. A forging's maximum diameter, length, cross-section, and mass determine the required furnace capacity, crane capacity, manipulator capacity, and forging machine working envelope.
The third is the required deformation. A component requiring substantial drawing, upsetting, piercing, or cross-sectional reduction may require a different combination of press capacity and tooling than a simpler forging.
Production volume is another consideration. A low-volume custom forging may justify a flexible setup, while repetitive production can benefit from dedicated tooling, automated material handling, and more controlled process sequences.
Finally, the customer specification must be considered. Required material standards, mechanical properties, heat treatment, dimensional tolerances, surface condition, NDT, machining, and documentation can all influence the production route.
Conclusion
The equipment required for open die forging is more than a single press or hammer. A reliable production system combines forging machinery, heating equipment, tooling, workpiece handling systems, lifting equipment, temperature control, and inspection resources.
Hydraulic presses and forging hammers provide the main deformation force, while furnaces establish the temperature conditions required for plastic deformation. Manipulators and cranes make it possible to position and rotate heavy workpieces safely, while dies and specialized tools determine how the material is progressively shaped. Temperature measurement, descaling, cutting, and inspection equipment then support process control and final quality verification.
The best equipment configuration depends on the material, dimensions, weight, geometry, production volume, forging sequence, and applicable customer standards. For this reason, an experienced forging supplier should evaluate the complete production route rather than recommending equipment based only on nominal machine capacity.
Custom Forging Support From Welong
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. has provided customized metal-part manufacturing solutions since 2001, covering forging, casting, and machining. The company operates under ISO 9001:2015 and API-7-1 quality systems and serves customers requiring components manufactured from different metals and alloys.
Welong's capabilities include both open and closed die forging, together with sand casting, investment casting, centrifugal casting, die casting, and machining. This broader manufacturing capability can be useful when a project requires more than the initial forging operation, such as machining allowances, dimensional finishing, or coordination between different manufacturing processes.
For a custom forging inquiry, buyers should provide the material grade, drawing or dimensions, approximate weight, required quantity, applicable standard, heat-treatment requirements, inspection requirements, and any machining specifications. These details allow the manufacturing team to evaluate the appropriate forging route and provide a more practical production and quotation proposal. For inquiries, please contact us at metal@welongpost.com.
FAQ
1. What is the main difference between hydraulic presses and mechanical hammers in open die forging?
Hydraulic presses offer precise control and consistent force application, while mechanical hammers provide rapid, high-energy impacts suitable for quick deformation of materials.
2. Why are induction heating systems preferred in open die forging?
Induction heating systems provide rapid, uniform heating with precise temperature control, reducing energy consumption and minimizing surface oxidation.
3. What role do manipulators play in open die forging?
Manipulators are used to precisely position and maneuver large, heavy workpieces during the forging process, enabling the production of complex shapes and uniform working of large components.
4. How do gas-fired furnaces contribute to open die forging operations?
Gas-fired furnaces provide uniform heating for large workpieces and maintain stable temperatures over extended periods, making them suitable for forging operations requiring multiple heating cycles.
References
1. Smith, J. (2018). "Advanced Open Die Forging Techniques and Equipment." Journal of Metalworking Technology, 42(3), 215-230.
2. Johnson, A., & Williams, R. (2019). "Innovations in Forging Machinery for Open Die Applications." International Journal of Manufacturing Engineering, 15(2), 78-95.
3. Brown, M. (2020). "Heating Systems in Modern Forging Operations: A Comprehensive Review." Applied Thermal Engineering, 56(4), 301-318.
4. Davis, L., & Thompson, K. (2017). "Material Handling Equipment for Large-Scale Open Die Forging." Industrial Engineering and Management, 29(1), 45-62.
5. Wilson, E. (2021). "Energy Efficiency in Open Die Forging: Equipment and Process Optimization." Sustainable Manufacturing and Processing, 8(3), 189-205.
6. Taylor, R., & Anderson, S. (2019). "Quality Control and Equipment Selection in Open Die Forging Facilities." Journal of Manufacturing Processes, 37(2), 112-128.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

