Forging Tolerance Guidelines for Shafts and Flanges
In forged shafts and flanges, dimensional tolerance is not simply a number placed on a drawing. It affects how much machining allowance is available, whether mating components can be assembled correctly, and how consistently a forging can be produced from one batch to the next. For buyers and engineers, understanding these factors is important when defining a forging specification and evaluating a supplier. shaft forging is particularly sensitive to dimensional changes because long shafts can be affected by material flow, die condition, forging temperature, cooling, and subsequent heat treatment. Flanges present a different set of challenges, especially around outside diameter, thickness, bore dimensions, bolt-hole locations, and face alignment. A practical tolerance guideline therefore needs to consider the entire manufacturing route rather than the forging operation alone. The material grade, forging method, die configuration, heating cycle, cooling method, heat treatment, machining allowance, and inspection procedure all contribute to the final dimensional result. Understanding these variables helps manufacturers establish realistic tolerances while avoiding unnecessary machining costs or repeated production adjustments.
What Determines the Dimensional Accuracy of a Forging?
Material behavior during deformation
One of the first elements to be considered in developing a forging tolerance is material selection. Different engineering materials such as carbon steel, alloy steel, and stainless steel behave differently under heat and deformation. Their flow properties, resistance to deformation, and thermal expansion and contraction during cooling might affect the size of the forged product.
On a shaft these variations can influence diameter, total length, shoulder dimensions, and other key areas. Also, a lengthy component may behave differently than a compact forging because the material flow and cooling may not be consistent along its length.
Same for flanges. The flange thickness, outer diameter, hub dimensions, and the amount of material available for subsequent machining can be affected by changes in material flow.
Hence, a tolerance shall be put in place, taking into account the material grade and the forging procedure. A practical tolerance for one grade or shape of steel may not be equally practical for another.
Forging temperature and dimensional change
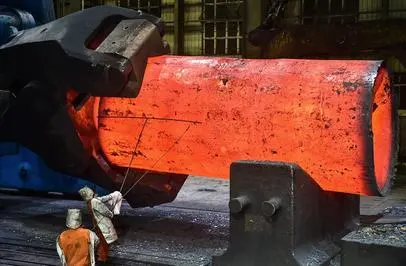
The forging temperature directly influences the material flow. The workpiece shall be heated to a high enough temperature for the forging method selected. However, the exact temperature range shall be managed to meet the material and production requirements.
Temperature changes throughout a billet or preform can lead to deformation variances. If one portion is much hotter or cooler than another, the material flow may be less uniform. This may cause differences in diameter, thickness, or shape.
Cooling after the forging is also necessary. The part does not necessarily keep the same dimensions that it had immediately after deformation. Thermal contraction and different cooling conditions can alter the ultimate size and shape.
Thus, the design of tolerances should take into account the actual conditions of inspection of the part. If the drawing provides dimensions following heat treatment or machining, such activities have to be considered in the determination of the original forging dimensions.
Die design and die wear
Repeatability in closed-die forging is greatly affected by die geometry. Draft angles, separating lines, distribution of material, flash design, and dimensions of the cavity all affect the filling of the die.
Production planning must take die wear into account. A die that delivers acceptable dimensions at the start of a production run may slowly yield different dimensions as the working surfaces wear. The effect could be minimal on one component but becomes important when thousands of parts are manufactured.
Therefore, for shaft forgings made with tooling, the die condition should be tracked against real inspection data. Special attention could be necessary for flange manufacture around hub geometry, thickness, and other surfaces that directly affect the subsequent machining process.
A well-defined die maintenance and inspection program helps reduce dimensional drift between early and late manufacturing batches.
How Should Shaft and Flange Tolerances Be Defined?
Start with the final machined component.
One of the most fundamental aspects of forging tolerance control is to identify the forging dimension and the final machined dimension.
A forged shaft may be purposefully oversized in the diameter, as the surface will be turned, ground, or machined subsequently. In the same way, a forged flange might have a machining allowance on the face, bore, or outer diameter.
This indicates that the as-forged stage does not have to have the forging at the final component tolerance. Rather, the forging needs to provide enough and sufficiently consistent material for the next operation.
For essential applications, engineers should determine which dimensions are regulated as forged and which are controlled after machining. This avoids the problem of increased manufacturing costs due to too tight forging tolerances, which do not provide a functional benefit.
Consider machining allowance.
Machining allowance is directly related to forging tolerance. If the dimension is close to the ultimate machining limit, local dimensional variation can cause the material to be too little to machine. But the larger allowance increases the consumption of material, machining time, and the cost of production.
An allowance on a shaft may be on the outside diameter, shoulders, ends, or other machined surfaces, particularly in shaft forging. For a flange it may be required on the face, bore, hub or outside diameter.
The correct allowance depends on the forging method, material, component shape, and the ultimate finish desired. It has to be done before manufacturing, not added when dimensional problems arise.
Separate general dimensions from critical features.
Not all dimensions on a forged component need the same tolerance level. The functional specification separates generic forging dimensions from those features that have a direct bearing on assembly or performance.
For example, the overall length of a rough shaft can be allowed to vary considerably if there is enough milling allowance. Dimensions might need to be more restricted for a locating diameter or shoulder that engages with another component.
The outside diameter and rough thickness on a flange may be specified with a different tolerance requirement than the machining bore, bolt-hole pattern, or sealing face. The more a characteristic influences assembly, alignment, or sealing directly, the more crucial it is to regulate the feature through the relevant stage of manufacture.
This method does not hold the entire forging to the tightest tolerance unnecessarily.
Which Forging Process Is Appropriate for Tolerance Requirements?
Open-die forging for large components
Open-die forging is sometimes used for big shafts, rings, blocks, and other parts for which the dimensions or weight of the part make traditional closed dies unfeasible. The procedure generally gives less dimensional control than closed-die forging since the workpiece is not completely contained in a precision die chamber.
However, this does not mean that open-die forging is not suited for precision applications. The forging may be manufactured with deliberate machining allowances, heat treated, and then machined to final specifications.
For large shaft forgings, the manufacturing strategy should address the deformation sequence, material flow, upset or draw, and dimensional change that may occur during cooling and heat treatment.
Closed-die forging for repeatable geometries
Closed-die forging is capable of providing more robust control over the shape of parts, with reproducible geometries. The die cavity helps guide the material into the desired configuration, and the procedure is suited for various medium-sized shafts, flanges, and other forged items.
Tolerances that can be achieved are still dependent on material, part geometry, die accuracy, forging equipment, temperature management, and die wear. Therefore, closed-die forging should not be considered to guarantee any particular tolerance without regard to the overall manufacturing arrangement.
Repeatability of a well-controlled closed-die process can be a key advantage for higher-volume manufacturing since repeatable forgings reduce variation in subsequent machining.
Precision and near-net-shape forging
If material utilization and machining time are significant, precision or near-net-shape forging could be explored. The purpose of these methods is to improve the forged geometry to the desired final shape.
The benefit is not just a smaller dimension. A correctly planned near-net-shape procedure can reduce the amount of machining stock and the downstream processing. Tooling requirements and process controls, however, are usually more demanding.
It is crucial that a supplier and buyer compare the expense of tighter forging tolerances to the savings they provide in machining and material utilization. In some situations, traditional forging and machining is more affordable than trying to obtain extremely close as-forged dimensions.
How Do Heat Treatment and Machining Affect Final Tolerance?
Heat treatment can change dimensions.
The required mechanical qualities of a forged shaft or flange are usually achieved via heat treatment. Normalizing, annealing, quenching, tempering, etc. can affect material structure and may also cause dimensional change.
The magnitude of this change relies on material grade, shape, heating circumstances, cooling method, and component orientation. Long shafts are particularly susceptible to distortion because the ratio of length to diameter might make it more difficult to control straightness.
Dimensional inspection should therefore be planned at the right point. If final dimensions are required after heat treating and machining, measuring the forging before these procedures may not give the whole picture of final dimensional performance.
Machining establishes many final dimensions
Many of the closest tolerances on shafts and flanges are produced by machining rather than forging. The final dimensional and geometric requirements can be achieved by turning, milling, boring, drilling, grinding, and other procedures.
This means that a forged component needs to be assessed in the whole manufacturing chain. The forging provider needs enough information about the final component to know where machining allowance is needed and which forged parameters are important.
For example, a shaft may need controlled stock on a bearing diameter but more variance on a non-critical rough surface. A flange may require enough material on the sealing face to allow machining to obtain the ultimate flatness and thickness, particularly when shaft forging is involved.
What Inspection Methods Help Control Forging Tolerances?
Dimensional inspection during production
Dimensional examination should be expanded until the final shipment step. Dimensional drift can be detected by in-process tests while production is still going on.
Inspection may include diameter, length, thickness, bore size, shoulder position, straightness, concentricity, and other qualities as specified, depending on the part being inspected. We can select gauges, callipers, micrometers, height gauges, CMM equipment, and other measuring devices depending on the needed accuracy.
Measurement protocols for bigger forged components should additionally include handling and temperature conditions. It’s crucial to have a consistent method of inspection since you could misinterpret measurement variation for true manufacturing variation.
Final inspection and documentation
The final inspection plan shall directly relate to the drawing and purchasing specification. Acceptance criteria should be specified for critical dimensions, and the measurement equipment should be suitable to the tolerance being measured.
In industrial purchasing, the paperwork can be just as significant as the physical measurement. Depending on applicability, buyers may seek dimensional inspection reports, material certificates, heat-treatment records, and appropriate non-destructive testing reports.
A record of a clear inspection also helps to determine if a dimensional problem resulted from forging, heat treatment, machining, or measuring.
Non-destructive testing for forged components
Dimensional tolerance and material integrity are two distinct requirements, although both can influence the use of a forged part. Depending on the application, ultrasonic testing, magnetic particle testing, or other nondestructive testing procedures may be specified.
These inspections do not substitute for dimensional measurement. They address multiple quality attributes and may be used to develop a more complete quality-control system for important shafts and flanges.
How Can Manufacturers Improve Tolerance Consistency?
Control the complete process rather than one operation.
Consistent forging tolerance is easier to achieve when the complete process is controlled as a system. Material preparation, billet heating, forging, trimming, cooling, heat treatment, machining, and inspection should not be treated as completely independent operations.
Production data can be used to identify recurring dimensional changes. If a particular dimension gradually shifts during a production run, the cause may be related to die wear, temperature variation, equipment settings, or another process variable.
Corrective action is more effective when the underlying cause is identified instead of simply sorting finished parts.
Use realistic tolerance requirements.
The tightest possible tolerance is not automatically the best tolerance. An unnecessarily restrictive requirement can increase tooling costs, machining requirements, inspection time, and scrap without improving the function of the final component.
A more practical approach is to determine which dimensions are functionally critical and then assign tolerances according to their actual role.
This is especially important when requesting quotations. A supplier can provide a more accurate cost and production plan when the drawing clearly separates as-forged dimensions, machining allowances, and final machined requirements.
Communicate requirements clearly with the forging supplier.
Before production begins, the buyer and supplier should confirm material grade, forging method, approximate forging dimensions, machining allowance, heat-treatment condition, inspection requirements, and applicable standards.
Drawings should identify critical dimensions and geometric requirements rather than relying only on a general statement such as “tight tolerance.” If a particular shaft diameter, flange face, or bolt-hole relationship is important for assembly, that requirement should be clearly identified.
This communication is particularly valuable for custom forgings because the supplier may need to evaluate the tooling design and process route before confirming achievable dimensions.
Conclusion
Forging tolerance guidelines for shafts and flanges should be developed around the complete manufacturing process rather than the forging operation alone. Material behavior, forging temperature, die design, die wear, cooling, heat treatment, machining allowance, and inspection all influence dimensional results.
For shaft forging, particular attention may be required for diameter, length, straightness, shoulders, and other features that are later machined or used for assembly. Flanges require similar planning around thickness, outside diameter, bore, hub geometry, bolt-hole locations, and machined faces.
The most effective tolerance strategy is to identify functionally critical dimensions, establish appropriate as-forged tolerances, provide sufficient machining allowance, and verify the final component using a suitable inspection plan. Clear communication between engineers, purchasers, and forging suppliers can prevent unrealistic requirements while maintaining the dimensional quality needed for the finished component.
Your Trusted Partner for Custom Metal Manufacturing Solutions
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. provides customized metal manufacturing services for customers requiring forged, cast, and machined components. With more than 20 years of industry experience and certifications including ISO 9001:2015 and API-7-1, the company supports projects involving different materials, component geometries, and production requirements.
For custom shafts and flanges, the manufacturing process can be developed around the customer's drawings, material specifications, forging requirements, machining allowances, heat-treatment needs, and inspection criteria. This allows dimensional requirements to be considered from the initial forging stage through final machining and quality inspection rather than being addressed only at the end of production.
For projects involving custom shaft forging, forged flanges, or other metal components, customers can discuss drawings, material requirements, production quantities, tolerance expectations, and delivery requirements with the Welong team. A manufacturing plan based on the actual component and application can help balance dimensional requirements, machining costs, production efficiency, and final quality. Contact us at info@welongpost.com to discover how we can contribute to your project's success.
FAQ
1. What are the typical tolerance ranges for forged shafts and flanges?
Typical tolerance ranges vary depending on the size and complexity of the part, but generally fall within ±0.5mm to ±2mm for most applications.
2. How does material selection affect forging tolerances?
Different materials have varying flow characteristics and shrinkage rates, which can impact the achievable tolerances during forging.
3. Can post-forging heat treatment improve dimensional accuracy?
Yes, properly controlled heat treatment can relieve internal stresses and improve dimensional stability, potentially tightening tolerances.
4. What are the advantages of precision forging techniques for flange production?
Precision forging techniques can achieve tighter tolerances and reduce the need for post-forging machining, saving time and material costs.
References
1. Smith, J. D. (2018). Advanced Forging Techniques for Precision Shaft Manufacturing. Journal of Materials Processing Technology, 256, 112-124.
2. Johnson, R. A., & Miller, S. L. (2019). Tolerance Control in Flange Forging: A Comprehensive Review. International Journal of Advanced Manufacturing Technology, 102(5), 1845-1860.
3. Brown, T. E., & Davis, C. M. (2020). The Impact of Material Properties on Forging Tolerances for High-Performance Shafts. Materials Science and Engineering: A, 785, 139329.
4. Lee, K. H., & Park, S. Y. (2017). Optimization of Die Design for Improved Flange Forging Tolerances. Journal of Manufacturing Processes, 28, 11-23.
5. Thompson, A. W., & Wilson, R. D. (2021). Process Monitoring and Control Strategies for Maintaining Tight Tolerances in Shaft Forging. Journal of Intelligent Manufacturing, 32(3), 721-735.
6. García, M. L., & Rodríguez, F. J. (2019). Heat Treatment Effects on Dimensional Stability of Forged Shafts and Flanges. Heat Treatment and Surface Engineering, 1(2), 45-57.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

