Open Die vs Close Die Forging: Which Process Improves Production Efficiency
Choosing between forging processes is not simply a matter of selecting the method with the lowest initial cost. Part size, geometry, production quantity, dimensional requirements, material grade, tooling investment, machining allowance, and delivery requirements can all affect the final result. Two commonly considered approaches are open die forging and close die forging, and each is suited to a different manufacturing situation. For large shafts, discs, rings, blocks, and other heavy components, open die forging provides considerable flexibility because the workpiece is compressed between dies without being completely enclosed. Close die forging, in contrast, uses shaped dies that surround the heated metal and guide it toward a defined geometry. This can make the process highly productive for repeat production of smaller and more complex components. The important question for manufacturers is therefore not which process is universally better. It is which forging process provides the right balance of production efficiency, tooling cost, material utilization, dimensional control, and downstream machining for a specific part.
How Do Open Die and Close Die Forging Differ?
How the Workpiece Is Shaped
Open die forging is when the heated billet or workpiece is squeezed between relatively simple dies. Since the dies do not fully encircle the material, the workpiece may be repositioned by the user or by automated machinery between subsequent reductions. Operations may be upsetting, drawing out, flattening, punching, or other controlled deformation procedures depending on the component.
This versatility makes open die forging especially helpful for large parts and products that require incremental shaping rather than one-step forming. A forging can be diminished progressively to get the desired dimensions with control of the direction and quantity of deformation.
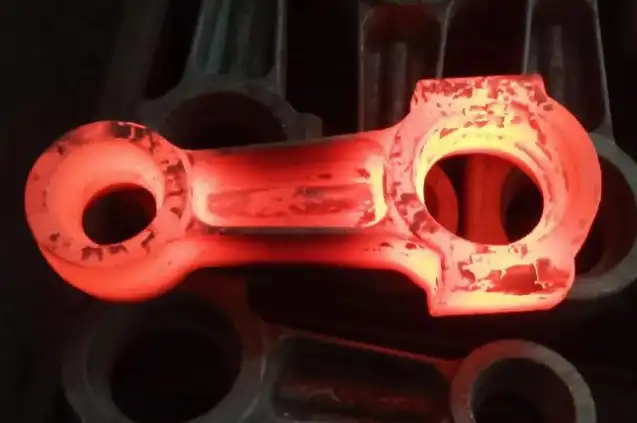
Close die forging employs dies with impressions closer to the final shape of the component. The heated material is deposited in the die cavity and pressed to flow under high pressure. The enclosed chamber allows far better control of the final shape than the relatively open tooling utilized for open die production.
This has resulted in a fundamental divergence in manufacturing philosophy: open die forging requires flexibility and controlled progressive deformation, while close die forging requires repeatable shape fabrication and greater production rates.
How Material Flow Affects the Part
The material flow is significant, as the manner in which the metal deforms during forging can affect the microstructure and mechanical properties of the final product.
In open die forging the workpiece can be modified between successive operations. This allows the forging team more control over the direction and sequence of deformation and can be useful for making huge sections that require significant reduction.
In close die forging, the dies push the metal into a specific cavity, which results in a more controlled flow of the material. With proper design of equipment and process settings, this regulated flow allows complex geometries to be produced with generally consistent outcomes from part to part.
Neither method inherently yields a better component in all applications. The correct procedure depends on the material, forging ratio, geometry, deformation schedule, heat treatment, and necessary mechanical qualities.
Which Forging Method Is Better for Different Production Requirements?
Open Die Forging for Large or Low-Volume Components
Open die forging is generally preferred when the part is large, production volume is low, or the shape may require customization.
Heavy forgings such as large shafts, discs, blocks, rings, etc. may need considerable forming forces and sophisticated equipment. Fully formed close-die tooling to make these parts may require a large tooling investment that is hard to justify for modest production runs.
The tooling itself is rather basic and can typically be changed to accommodate varied sizes and shapes of parts. This flexibility is especially valuable for prototype programs, replacement parts, heavy industrial equipment, energy sector components, and other applications where manufacturing volumes are relatively modest.
Another advantage is that it allows you to shrink a huge workpiece gradually. Instead of pressing the whole component into a complex die cavity in one operation, the producer can regulate the deformation through a series of forging operations.
Close Die Forging for Repeat Production
Close die forging is becoming increasingly desirable when producers need large volumes of repeatable parts with a somewhat uniform shape.
Once the correct dies are designed and produced, the same tooling can be utilized over and over. This makes the technique suited for production programs where the initial tooling cost can be amortized across a large number of parts.
Close die forging can also reduce the amount of subsequent machining necessary when the die cavity is a good approximation of the target component shape. But the precise machining required remains dependent on the component design, tolerances, surface requirements, and the forging supplier’s process capacity.
Therefore, for automotive, industrial machinery, hardware, and other industries where the same shaped parts are produced repeatedly, close die forging may have more advantage in production efficiency.
How Do Size and Geometry Influence the Decision?
Part Size Can Favor Open Die Processing
Part size is one of the most critical variables in the selection of a forging process.
The tooling requirements are more demanding with the larger component dimensions and weight. Big bespoke dies can demand a lot of material, machining time, handling capability, and maintenance. For a large part manufactured in relatively small numbers, these added expenses may make close die forging uneconomical.
The work is not fully contained in a complicated die cavity in the case of open die forging. This is one reason it remains relevant for large forgings and heavy industrial components.
But it is not the only thing in the process. The available forging presses or hammers, the component geometry, the material grade, the needed reduction, and the equipment capacity must also be considered.
Complex Geometry Can Favor Close Die Forging
Close die forging usually offers an advantage when the component has several characteristics that need to be forged repeatedly, compared with open die forging.
The die cavity can be made to the geometry required for the metal to flow into particular parts of the component. This can lower the amount of material removed during machining compared to a forging with a much simpler initial form.
For parts of simple cylindrical, rectangular, or disc-like shape, the added problem of close-die tooling might not bring sufficient value to compensate for its cost.
The practical aim then is to establish whether the geometry is repeatable enough and complex enough to justify dedicated tooling.
What Are the Main Cost Differences?
Tooling Investment
The tooling is frequently the clearest economic differential between the two processes.
The initial tooling need is smaller since dies for open die forging are often simpler. This can be useful for custom components, development programs, and low-volume orders.
Close die forging typically requires dies that are specifically constructed to have the necessary cavity geometry. So the initial outlay can be much more, particularly for sophisticated components.
That doesn't mean close die forging is necessarily more expensive per final product. The tooling cost can be amortized over a large number of components when the volume of production is large enough. Faster forming with less downstream machining can enhance the overall economics.
Hence, the comparison should be of overall cost per final component rather than the cost of tooling alone.
Production Rate and Labor
Production rate is another important consideration.
Open die forging can require multiple forming operations and repositioning of the workpiece. Depending on the equipment and degree of automation, this can increase cycle time and require experienced personnel to maintain dimensional control throughout the sequence.
Close die forging can provide more repeatable production once the tooling and process have been established. For high-volume manufacturing, this repeatability can contribute significantly to production efficiency.
However, actual cycle time varies with material, part size, equipment capacity, heating requirements, forging sequence, inspection procedures, and automation. Manufacturers should therefore request process-specific cycle estimates rather than assuming one universal production rate.
Does Material Utilization Change Between the Two Processes?
Starting Material and Forging Allowance
Material utilization depends heavily on part geometry and process design.
Open die forgings may begin with relatively large billets or bars and require additional machining to reach the final dimensions. The amount of material removed depends on the specified forging allowance and the dimensional requirements of the finished component.
Close die forging can often bring the workpiece closer to the required geometry, while open die forging may still consume material through flash, trimming, machining allowance, and other process requirements.
For this reason, it is not accurate to judge material efficiency only by whether a process is an open or closed die. A better approach is to compare the complete manufacturing route, including:
-
starting billet weight;
-
forging allowance;
-
flash or trimming requirements;
-
machining allowance;
-
rejected or reworked parts;
-
final component weight.
For expensive alloy materials, even a small improvement in material utilization can have a meaningful effect on total manufacturing cost.
How Does Forging Affect Mechanical Properties?
Grain Flow and Microstructure
Forging involves controlled plastic deformation at elevated temperature for many common forging alloys. The deformation and subsequent thermal processing can alter the microstructure of the material.
In open die forging, the sequence of reductions can be designed to achieve substantial deformation through the section of a large workpiece. Proper process control can help produce a more uniform forged structure than might be obtained from an inadequately processed starting material.
Close die forging also produces controlled deformation, with the die cavity influencing how material flows through the component.
However, mechanical properties cannot be guaranteed simply by choosing one forging method. They depend on the alloy, starting material, forging temperature, reduction, deformation sequence, cooling conditions, heat treatment, and applicable inspection requirements.
Directional Performance
The direction of deformation can be important for components subjected to known service loads.
For example, large shafts may be designed so that the forging process produces favorable material flow along important load-bearing directions. Similar considerations may apply to discs, rings, and other components where service stresses are not uniformly distributed.
For critical applications, manufacturers should evaluate the complete forging procedure and applicable material specifications rather than relying on the process name alone.
Which Process Offers Better Dimensional Accuracy?
Dimensional Control in Open Die Forging
Open die forging generally provides less geometric constraint than close die forging. Because the workpiece is shaped progressively, the final dimensions can depend on forging sequence, die configuration, operator control, temperature, material behavior, and the amount of subsequent machining.
This does not make open die forging unsuitable for precision components. Instead, it means that the process is commonly combined with machining when tight final dimensions are required.
For large shafts, discs, rings, and blocks, this approach can be practical because the forging establishes the basic structure and dimensions while machining produces the final tolerances.
Repeatability in Close Die Forging
Close die forging generally offers stronger control over repeatable external geometry because the die cavity provides a defined forming boundary.
This can be particularly valuable when many components must meet the same dimensional requirements. Nevertheless, close die forging should not be confused with a finished-machining operation. Critical dimensions may still require machining after forging.
The appropriate manufacturing route should therefore be evaluated according to the finished-part tolerance, not simply the forging method.
How Should Manufacturers Choose Between the Two Processes?
Match the Process to Annual Production Volume
Production volume is one of the first questions a supplier should ask.
For a small number of large, customized components, open die forging can often provide a practical balance between tooling flexibility and manufacturing cost.
For thousands or more of the same relatively compact components, close die forging may become more attractive because the initial die investment can be distributed across a much larger production quantity.
There is no universal volume threshold because tooling complexity and component value vary significantly from project to project.
Evaluate the Complete Manufacturing Route
A sound process decision should consider more than forging itself.
Manufacturers should compare:
-
Raw material cost.
-
Billet or ingot weight.
-
Tooling investment.
-
Forging cycle time.
-
Heat treatment requirements.
-
Machining allowance.
-
Machining time.
-
Inspection requirements.
-
Expected production quantity.
-
Transportation and handling requirements.
This broader comparison can reveal that a process with higher initial tooling costs may have a lower total cost over the life of a production program.
Give the Supplier Enough Technical Information
For a custom forging project, suppliers can make a more meaningful process recommendation when they receive complete technical information.
Useful inputs include the material grade, finished drawing, approximate part weight, required quantity, dimensional tolerances, mechanical-property requirements, heat treatment specification, surface requirements, inspection standards, and expected delivery schedule.
For large or critical components, information about loading conditions and service environment can also help the forging supplier evaluate the appropriate manufacturing route.
Conclusion
In conclusion, the choice between open die and close die forging should be based on the complete production requirement rather than on tooling cost or production speed alone. Open die forging is often well suited to large, heavy, customized, or lower-volume components because it provides flexibility and avoids the need for complex dedicated cavity tooling. Close die forging can be more efficient for repeat production of smaller and more geometrically complex components where higher tooling investment can be justified by production volume and repeatability.
The most effective choice depends on part size, geometry, material, production quantity, dimensional requirements, mechanical-property targets, machining needs, and total manufacturing cost. For OEM and industrial projects, comparing the entire manufacturing route with an experienced forging supplier is usually more reliable than selecting a process from a general rule of thumb.
Shaanxi Welong, established in 2001, provides customized metal parts and manufacturing support for industrial customers. With ISO 9001:2015 and API-7-1 certifications, the company offers forging, casting, and machining capabilities for different material and component requirements. Its experience with both open die and close die forging allows project requirements to be evaluated in relation to part geometry, production volume, machining, inspection, and delivery needs. For manufacturers developing a new component or reviewing an existing sourcing plan, providing the drawing, material specification, quantity, and key quality requirements gives the engineering team a stronger basis for recommending a suitable production route. For inquiries, please contact us at info@welongpost.com.
FAQ
1. What is the main difference between open die and closed die forging?
Open die forging uses simpler dies that don't fully enclose the workpiece, allowing for greater flexibility, while close die forging uses more complex dies that completely enclose the material, offering higher precision.
2. When is open die forging preferred over close die forging?
Open die forging is preferred for large parts, custom shapes, low to medium production volumes, and when specific directional material properties are required.
3. How does open die forging affect material properties?
Open die forging refines grain structure, enhances directional properties, and reduces internal defects, resulting in improved strength, toughness, and overall material integrity.
4. What are the economic advantages of open die forging?
Open die forging generally has lower tooling costs and offers greater flexibility for producing a variety of shapes, making it more economical for low to medium production volumes.
References
1. Smith, J. (2019). Advanced Forging Techniques: Open Die vs. Close Die. Journal of Materials Processing Technology, 45(3), 178-195.
2. Johnson, A. & Brown, M. (2020). Economic Analysis of Forging Processes in Modern Manufacturing. International Journal of Production Economics, 87(2), 301-318.
3. Lee, S. et al. (2018). Material Property Enhancement through Open Die Forging: A Comprehensive Review. Materials Science and Engineering: A, 712, 12-27.
4. Thompson, R. (2021). Optimization of Production Efficiency in Metal Forming Processes. Journal of Manufacturing Systems, 59, 45-62.
5. Garcia, C. & Wilson, D. (2017). Comparative Study of Open and Closed Die Forging for Aerospace Applications. Aerospace Science and Technology, 68, 213-229.
6. Patel, N. (2022). Advancements in Forging Technology: Improving Efficiency and Quality. International Journal of Mechanical Engineering, 14(4), 567-582.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

