How to Reduce Costs in Closed Die Forging Production?
Cost reduction in closed die forging It is not only about getting cheaper steel or running machines faster. The greatest savings are usually achieved before production begins, in decisions on part geometry, billet size, preform design, die configuration, machining allowance and production volume. During production, die life, heating efficiency, cycle time, lubrication, scrap and setup time can all further influence the cost of each final part. The most helpful way for forging manufacturers to evaluate cost is to look at cost on a cost-per-part basis rather than individual expenses in isolation. The minor reduction in material waste may be of less importance than increasing die life and a faster forging cycle may bring extra quality difficulties if process control is not good. The goal is therefore to optimise the use of the material, of the tooling, of the productivity, of the energy consumption and of the subsequent machining. This article provides practical methods to lower the total cost of manufacturing a closed die forging while preserving dimensional accuracy and product quality.
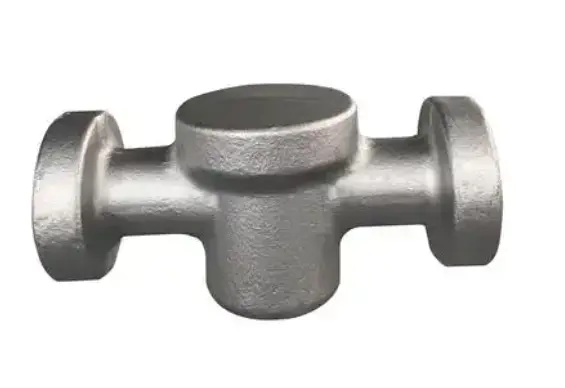
Optimize Part Geometry Before Cutting the First Billet
Improve Billet and Preform Design to Control Material Consumption
Material is one of the most noticeable expenditures in forging manufacturing, yet lowering the weight of the billet is not always the best approach. The billet must have enough material to fill the die cavity and produce all important portions of the component. If it is undersized, it can result in partial filling or dimensional problems. If excessive, additional material might be pushed into the flash, resulting in increased trimming and material loss.
A better way is to optimize the billet volume and the preform geometry simultaneously. For parts with substantial variations in cross-sectional area, a well-constructed preform can disperse the material more efficiently before the final forging operation. This may help to decrease excessive deformation in local locations and improve cavity filling.
Final billet dimensions should be determined from finished forging volume, anticipated flash, draft angles, fillet radii, and material flow. In high-volume production where you are talking thousands or millions of parts, even a tiny saving in billet weight can be financially significant.
The idea is not to get rid of all flash at any price. Rather, manufacturers should strive for reliable cavity filling with the minimum possible material input.
Use CAD and simulation before manufacturing production dies.
“Once production tooling has been built, design errors are extremely expensive. CAD modeling and forging simulation can be used to identify any difficulties before the first practical trial.
Three-dimensional CAD models help engineers to assess the parting line, draft angles, fillet transitions, machining allowances, and die geometry. Then forging simulation can provide insight into material flow, cavity filling, possible faults, and regions where there might be excessive flash.
This is especially helpful when dealing with intricate forgings or for new product development. Simulation may show that a seemingly simple geometry needs a preforming step or an alternative die setup. It is usually more disruptive to find this defect after you have made multiple trial forgings than to find it during the technical development phase.
Simulation should complement engineering decisions, not replace them. The actual forging behavior further depends on billet temperature, friction, lubrication, die temperature, equipment parameters, and properties of the material. The best results are obtained by integrating simulation with production experience and physical confirmation.
Reduce Machining Allowance Without Creating Forging Risk
Machining after forging can account for a rather high percentage of the entire cost of manufacture. Excessive machining allowance requires more metal to be removed after forging; this increases the time and cutting-tool consumption, labor, and waste of the material.
Near-net-shape forging has the potential to lower these expenses by manufacturing a component closer to its ultimate dimensions. But you should not just look for more precise forging sizes. If the predicted savings are lost because a narrower machining allowance needs much more expensive equipment or unstable manufacturing, then…
Hence, the overall forging and machining costs should be compared by engineers. If it significantly lowers CNC machining time, a little higher forging cost may be justified. Conversely, for smaller volume items, traditional tolerances can sometimes be cheaper due to the lower tooling investment.
The optimum solution will rely on the production volume, geometry, material, tolerance requirements, and downstream machining procedures.
Extend Die Life to Reduce Tooling Cost Per Part
Select Hot-Work Die Materials for the Actual Service Conditions.
The die material has a direct impact on tool life and the cost per part. The correct choice relies on forging temperature, contact pressure, wear circumstances, thermal cycling, component shape, and estimated production volume.
Hot-work tool steels, such as H13, are often the preferred choice for a wide range of hot forging applications because they offer a good balance of hot strength, toughness, wear resistance, and resistance to thermal fatigue. H13 is notably recognized as a hot-work tool steel employed in applications like forging dies.
But selecting the most expensive tool steel available on the market is not necessarily minimizing the production expenses. If a standard material gives a satisfactory service life, then a higher, expensive grade may not give a suitable return on investment.
The more meaningful calculation is tooling cost per good part for closed die forging. An expensive die to purchase, but one that gives a lot more good parts, could have a lower effective tooling cost than a cheaper die that has frequent failures.
Control Heat Treatment to Prevent Premature Die Damage.
The performance of the forging die depends not only on the steel grade but also on the heat treatment.
Hot-forging dies are subjected to cyclic thermal stress. In the course of manufacture the die surface is subjected to high temperatures and high mechanical loads and then cooled. Repeated cycling can contribute to thermal fatigue, heat checking, wear, and deformation.
Proper hardening and tempering techniques help to establish the needed mechanical characteristics for the application. The actual heat-treatment needs should be dependent on the tool steel selected and the planned forging conditions, not a generic hardness target for all dies.
Manufacturers shall maintain records of heat treatment and check hardness and dimensional stability prior to use in production. The cost of a die that fails prematurely due to improper heat treatment is more than the cost of the replacement die. It can also involve machine downtime, production delays, emergency tooling, and scrap parts.
Thus, management of the preparation of the die is a crucial part of cost management.
Optimize Lubrication and Die Cooling
Lubrication affects friction, material flow, die wear, and part surface quality. Insufficient lubrication increases friction and accelerates localized die damage, while excessive or irregular lubricant use can generate instability in the process.
The correct lubricant and manner of application depend on the forging temperature, material, tooling, equipment, and manufacturing conditions. Rather than randomly increasing lubricant use, manufacturers should concentrate on continuous application at the points where it gives the greatest process advantage.
Similar care is given to cooling. Forging dies are subjected to repetitive thermal shock. Excessive or non-uniform cooling can lead to temperature gradients that can lead to thermal fatigue.
Better regulation of water circulation, cooling channels, and die temperature monitoring will help to maintain more stable working conditions. The optimum cooling strategy is dependent on die design and forging process and so should be determined through process trials and production data rather than assumptions.
Apply Surface Treatments When the Economics Justify Them
If wear is limiting die life, surface treatment may be beneficial. Depending on the die material and application, surface-engineering methods, such as nitriding, can be used to increase surface hardness and improve resistance to particular wear mechanisms.
Also, unique conditions for forging can be addressed for the use of coatings. However, advanced surface treatments should be considered on a cost per part basis.
The increased treatment cost may not be repaid for a short run of manufacturing. For a large volume component, when die replacement or maintenance is a regular occurrence, prolonging tool life can provide a considerably stronger financial return.
Before adding a coating or surface treatment, producers should examine the forging temperature, the substrate material, the lubrication system, cooling circumstances, the expected wear mechanism, and the manufacturing amount.
Increase Production Efficiency Without Increasing Scrap
Reduce Setup and Die-Change Time
A forging machine may have great theoretical output capacity, but it may have poor economic performance if too much time is lost in setup.
The adjustments, alignment, equipment adjustment, billet preparation, and trial pieces might lead to the reduction of the productive machine hours. This can translate to a direct impact on cost per part from reduced setup time in high-volume manufacturing.
Manufacturers can improve this area by pre-building replacement tooling, standardizing setup methods, organizing tools and fixtures, and documenting common adjustment points.
Performance should also be measured in setup; keeping records of the actual time required for each die change helps identify reoccurring delays and assess if process improvements are bringing measurable results.
Stabilize the Forging Cycle
Increasing speed of production in closed-die forging is not necessarily a successful cost reduction strategy. The apparent gain in productivity might increase the real cost per good part if higher output results in increased die wear, non-uniform dimensions, or more trash.
Generally, a stable forging cycle is more important than an active cycle that necessitates intervention often.
Important factors are billet temperature, die temperature, transfer time, press settings, lubrication, cooling, and trimming conditions. Consistent control of these elements can reduce process variance and increase repeatability.
The same principle applies to closed die forging tooling. A more expensive die may be economically preferable if it substantially increases die life and reduces production interruptions. The right aim is the shortest stable cycle that always gives acceptable portions.
Reduce Unplanned Downtime Through Preventive Maintenance
Unscheduled equipment or tooling problems might set back the entire manufacturing schedule. A damaged die may need to be replaced immediately, but press faults can harm several items on the same machine.
These dangers can be reduced by preventive maintenance. Inspect dies for wear, cracking, heat checks, dimensional changes, and other evidence of deterioration. Maintain presses, heating systems, lubricating equipment, and material-handling systems according to set timetables.
Production records might help to spot patterns. If a die begins to show dimensional faults after a specified number of forging operations, that can be a good trigger for maintenance or inspection.
This means maintenance moves from reactive repairs to planned intervention.
Control Energy and Material Waste
Improve Billet Heating Efficiency
Heating is an important energy-demanding step in hot forging. Inefficient furnaces, poor insulation, long holding times, unneeded reheat, and delays between heating and forging may all result in energy losses.
Hence, it is necessary to have a consistent temperature control. Billets shall be heated to proper forging temperature without excessive overheating or holding.
Energy usage is influenced by furnace maintenance, insulation, temperature sensors, burner performance, and production scheduling.
Manufacturers can also track energy use on a per-batch or per-finished part basis. This is a more pertinent efficiency metric than just looking at the overall monthly energy usage, because the production volume might fluctuate greatly from month to month.
Reduce Flash and Trimming Loss
Flash is a natural aspect of many closed-die forging processes, although excessive flash might be an indication of an opportunity for optimization.
Flash formation is affected by billet volume, preform geometry, die design, material flow, friction, and temperature. Better die design and more accurate billet sizing can help keep unwanted material out of the flash area.
Take caution reducing flash. Overdoing the flash reduction might make cavity filling less reliable and increase the chances of problems.
The goal is to set up a steady process with a correct flash allowance, not just to minimize flash size.
Prevent Scrap Instead of Relying on Recycling
While scrap recycling can reclaim some value from discarded material, avoiding scrap typically yields greater economic benefits.
The rejected forging has already wasted material, energy, machine time, labor, tooling life, and inspection. Recycling the metal doesn’t recover all those costs.
Therefore, the manufacturer should establish the major causes of scrap. However, common causes are incorrect billet dimensions, improper heating conditions, die wear, inadequate lubrication, faulty setup, material faults, and dimensional fluctuation.
Once the reasons have been identified, corrective activities can be prioritized by financial impact.
Recycling should be part of the entire material-management strategy, but it should be preceded by scrap prevention.
Use Production Data to Identify the Largest Savings
Calculate the real cost per finished part.
Cost reduction becomes much easier when manufacturers calculate the actual cost of producing an acceptable component.
The calculation should consider more than billet price. Material waste, die consumption, labor, energy, forging time, setup, inspection, machining, rework, scrap, and downtime can all contribute to the final cost.
For example, reducing billet weight by a small amount may produce noticeable material savings. However, if the change increases incomplete filling and raises the scrap rate, the overall cost could actually increase.
The same principle applies to tooling in closed die forging. A more expensive die may be economically preferable if it substantially increases die life and reduces production interruptions.
The objective is to optimize the total manufacturing cost rather than one isolated expense.
Track Material Utilization, Die Life, and Scrap Rate
A small number of well-selected production indicators can provide useful insight into cost performance.
Material utilization can be calculated by comparing finished forging weight with starting billet weight. Tracking this value over time can reveal whether changes in billet sizing or preform design are producing genuine improvements.
Die life should also be measured based on acceptable parts produced, not simply the number of days the die remains in service. This provides a clearer relationship between tooling expenditure and production output.
Scrap and rework rates should be monitored separately because reworked parts consume additional labor and machine time even when they ultimately become acceptable products.
When these indicators are reviewed together, manufacturers can identify whether their largest opportunity lies in material savings, tooling, process stability, or downstream operations.
Coordinate Forging With Machining and Quality Control
Evaluate the Entire Manufacturing Route
Forging cost should not be evaluated separately from machining and inspection.
A component with a low forging price may still have a high total cost if it requires excessive CNC machining, additional inspection, frequent rework, or complicated handling.
For this reason, manufacturers and procurement teams should examine the complete route from raw material to finished component.
This may include billet preparation, heating, preforming, final forging, trimming, heat treatment, machining, inspection, surface treatment, packaging, and delivery.
A change that slightly increases the forging cost can still be beneficial if it eliminates a more expensive downstream operation.
This is particularly important when purchasing customized forgings. The lowest initial quotation is not necessarily the lowest total cost.
Work With a Supplier That Can Support Multiple Manufacturing Stages
Supplier capabilities can have a significant influence on project efficiency.
When forging, machining, inspection, and engineering support are coordinated through one experienced supplier, process changes can be evaluated across the complete manufacturing route. This can simplify communication and reduce the risk of optimizing one operation while creating additional costs somewhere else.
Shaanxi Welong Int'l Supply Chain Mgt. Co., Ltd. provides customized metal-component solutions covering forging, casting, and machining. Established in 2001, the company states that it operates under ISO 9001:2015 and API-7-1 quality systems and supports customized components for different industrial applications.
For buyers evaluating a closed die forging supplier, it is useful to examine not only the quoted unit price but also engineering support, tooling capability, inspection processes, production capacity, material traceability, and delivery performance.
A supplier that understands the complete manufacturing process can often identify cost-saving opportunities before production begins.
Conclusion
In conclusion, reducing costs in closed die forging production requires a multifaceted approach that encompasses design optimization, material efficiency, tooling longevity, and process improvement. By implementing advanced CAD/CAM software, utilizing near-net-shape techniques, and optimizing die materials and treatments, manufacturers can significantly reduce material waste and tooling expenses. Furthermore, adopting lean manufacturing principles, optimizing energy consumption, and implementing effective scrap reduction and recycling programs can lead to substantial overall cost savings. These strategies not only improve profitability but also enhance product quality and environmental sustainability in closed-die forging operations.
For expert assistance in implementing these cost-reduction strategies in your closed-die forging operations, consider partnering with Shaanxi Welong Int'l Supply Chain Mgt. Co., Ltd. Established in 2001 and certified by ISO 9001:2015 and API-7-1 quality systems, Welong specializes in customized metal parts for various industries. With expertise in forging, casting, and machining, Welong offers comprehensive solutions to optimize your production processes, control quality, and ensure timely delivery. Their experienced staff and engineers can help you modernize your operations and achieve significant cost savings. For more information, contact them at metal@welongpost.com.
FAQ
1: What is closed die forging?
Closed die forging is a metal forming process where a workpiece is compressed between two dies that contain a pre-cut profile of the desired part shape.
2: How does near-net-shape forging reduce costs?
Near-net-shape forging reduces costs by minimizing the amount of material that needs to be removed in post-forging operations, saving on machining time and material waste.
3: What are some common die materials used in closed die forging?
Common die materials include high-grade tool steels such as H13 and D2, chosen for their hot hardness and wear resistance properties.
4: How can energy consumption be optimized in forging operations?
Energy consumption can be optimized by upgrading to energy-efficient heating systems, implementing advanced insulation techniques, and utilizing heat recovery systems.
References
1. Smith, J. (2019). Advanced Techniques in Closed Die Forging. Journal of Manufacturing Processes, 45(2), 112-128.
2. Johnson, R., & Brown, T. (2020). Cost Reduction Strategies in Metal Forming Industries. International Journal of Production Economics, 215, 45-62.
3. Lee, K., & Park, S. (2018). Energy Efficiency Improvements in Forging Operations. Energy, 156, 433-445.
4. Williams, A. (2021). Lean Manufacturing Implementation in Forging Processes. Journal of Cleaner Production, 298, 126872.
5. Chen, H., & Liu, Y. (2017). Advances in Die Materials for Closed Die Forging. Materials Science and Engineering: A, 707, 56-69.
6. Thompson, M. (2022). Waste Reduction and Recycling in Metal Forming Industries. Resources, Conservation and Recycling, 178, 106073.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

