How to Optimize Production Time in Closed Die Forging?
Closed die forging is widely used for components that require high strength, repeatable dimensions, and efficient material utilization. However, production time is not determined by the forging press alone. Billet preparation, heating, die setup, material transfer, forging sequence, trimming, inspection, and unplanned downtime can all affect the final delivery schedule.
For a forging manufacturer, improving productivity therefore means looking at the complete production route rather than trying to shorten one operation in isolation. A die that produces a part quickly but requires frequent maintenance may not deliver the best overall result. Likewise, a highly automated press cannot compensate for inconsistent billet temperatures or excessive die changeover time.
This is why production optimization should begin with process planning. Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. works with customized metal parts through forging, casting, and machining processes, giving buyers an integrated perspective when evaluating production requirements. The following guide explains the practical factors that can help manufacturers shorten production time while maintaining dimensional consistency and process control.
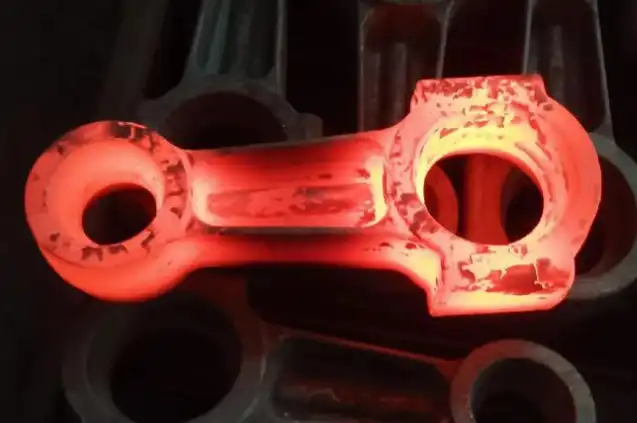
Which Production Stages Have the Biggest Impact on Forging Time?
Start With the Complete Process Route
Increasing the press speed does not considerably effect the overall delivery timetable if the forging technique itself is not the rate-limiting phase. But there is a much higher gain to be obtained by reducing die changeover or by stabilising billet heating.
First thing you do is measure the Cycle Time
Measured data, not assumptions, should drive production decisions. Manufacturers can schedule the loading, heating, transferring, forging, trimming and inspecting of the billets over a number of production runs.
This info will help find repeated delays. Where the press is continually calling for material, the heat or handling system may need adjustment. “Setup processes are the biggest opportunity when equipment sits idle too long between batches of product.
Tracking of scrap, rework, die maintenance and unplanned equipment stoppages is equally important. A nominal reduction in cycle time is not a significant productivity gain if it increases faults or maintenance interruptions.
Measure Cycle Time Before Making Changes
Production decisions should be based on measured data rather than assumptions. Manufacturers can record the time required for billet loading, heating, transfer, forging, trimming, and inspection over several production runs.
This information helps identify recurring delays. If the press is frequently waiting for material, the heating or handling system may need attention. If the equipment spends too much time between product batches, setup procedures may be the main opportunity for improvement.
Tracking scrap, rework, die maintenance, and unplanned equipment stoppages is equally important. A nominal cycle-time reduction is not a genuine productivity improvement if it creates more defects or maintenance interruptions.
How Can Die Design Shorten the Forging Cycle?
Design the Cavity Around Material Flow
Die design directly influences how quickly and consistently metal fills the cavity. Engineers need to consider part geometry, forging direction, draft, fillet radii, flash, and the expected flow of material.
Poor material flow in closed die forging can lead to incomplete filling, excessive flash, localized die wear, or additional forging operations. These problems increase production time because operators may need to repeat operations or adjust the process.
A well-developed die design aims to distribute material efficiently while keeping forging loads within the capability of the selected equipment. For complex components, the design should be reviewed together with the billet size and preform geometry rather than treated as a separate tooling decision.
Use Simulation Before Cutting Production Dies
Forging simulation can reduce unnecessary physical trials during tooling development. Finite element analysis can help engineers examine material flow, cavity filling, forging load, potential folding, and other process risks before production dies are manufactured.
This is especially useful for parts with complex transitions, deep cavities, or uneven material distribution. Engineers can compare different preforms, parting-line locations, flash designs, and forging sequences in a virtual environment.
Simulation does not replace production validation, but it can reduce the number of avoidable design iterations. That matters because every additional die modification can affect tooling cost and project lead time.
For repeat-production components, simulation can also provide a useful reference when a process is transferred to another press or when a design change is introduced.
Reduce Unnecessary Die Changeover
Die changeover can become a significant source of lost production time, particularly when a factory produces multiple part numbers on the same equipment.
Manufacturers can improve this area by preparing tools, fasteners, lifting equipment, and process documentation before the previous batch ends. Standardized setup procedures can also reduce variation between operators.
Where practical, die components can be prepared offline before the press becomes available. Quick-change fixtures and clearly defined setup checks may further reduce idle equipment time.
The important point is that production efficiency should be measured across the entire batch, not only by the time required to forge one component.
How Does Billet Preparation Affect Production Efficiency?
Control Billet Weight and Dimensions
Billet preparation has a direct relationship with forging stability. The billet must provide enough material for the finished geometry while limiting unnecessary excess that becomes flash or additional trimming material.
Inconsistent billet weight can create variation in cavity filling and final dimensions. It may also require process adjustments that slow the production line.
Accurate cutting equipment and routine checks of billet dimensions can help maintain consistent starting conditions. For high-volume production, automated cutting and material handling may provide additional advantages by reducing manual measurement and transfer work.
Maintain Consistent Heating Conditions
Heating is another important source of variation. Forging temperature affects material deformation behavior, forming loads, surface condition, and the ability to fill the die correctly.
Uneven heating can create temperature differences between billets or within a single billet. This may result in inconsistent forging behavior and additional inspection or process adjustments.
Induction heating, controlled furnaces, and temperature monitoring can help establish more repeatable conditions. The most appropriate system depends on the material, billet dimensions, production volume, and required temperature range.
The goal of closed die forging is not simply to heat billets faster. A faster heating cycle is only beneficial when the resulting temperature distribution remains suitable for the forging process.
Coordinate Heating With Press Availability
Heating and forging should be synchronized as closely as practical. If billets are heated significantly ahead of the forging operation, they may spend unnecessary time waiting. If the press is ready but heated material is unavailable, the equipment remains idle.
Production planning should, therefore, consider the capacity of the heating system and forging press together. Matching these capacities can eliminate avoidable waiting time and create a more balanced production flow.
What Role Does Automation Play in Reducing Production Time?
Automate Repetitive Material Transfer
Robotic or automated handling can reduce the time required to move hot billets and forged parts between stations. In a properly designed line, automated handling can coordinate the heating system, forging press, trimming station, and cooling area.
The primary benefit is consistency. Automated handling can maintain repeatable transfer paths and reduce waiting between operations. It can also reduce operator exposure to hot workpieces and heavy components.
However, automation should be introduced where it addresses a measurable bottleneck. A highly automated handling system may not provide a meaningful return if production volume is low or if another process remains significantly slower.
Improve Die Lubrication Consistency
Lubrication affects friction, material flow, part release, and die wear. In repeated production, inconsistent manual application can create variation between forging cycles.
Automated lubrication systems can control spray timing, coverage, and application quantity more consistently. This can help stabilize the process and reduce interruptions associated with manual application.
The system should be selected according to the die configuration, lubricant type, production rate, and environmental requirements. Excessive lubricant application should also be avoided because more lubricant does not automatically mean better forging performance.
Consistent lubrication can be particularly valuable in high-volume production, where even a small difference per cycle becomes significant over thousands of parts.
Automate Inspection Where It Makes Sense
Inspection is essential, but not every inspection task needs to interrupt production. Depending on the component and tolerance requirements, manufacturers may use gauges, dimensional checking systems, sensors, or automated visual inspection to identify process deviations earlier.
For critical components, automated inspection should complement rather than replace appropriate quality procedures.
Early detection can prevent a large quantity of nonconforming parts from moving to later operations. This reduces the time associated with sorting, rework, and repeated processing.
How Can Manufacturers Reduce Non-Production Time?
Shorten Setup and Changeover Activities
A major productivity opportunity is often found outside the actual forging stroke. Setup, cleaning, die installation, parameter adjustment, trial pieces, and inspection can consume substantial time between production batches.
A standardized changeover checklist can help operators prepare the required tools and documentation before the equipment becomes available. Manufacturers can also analyze which setup activities can be completed in parallel.
For example, while one team prepares the next die set, another operator may complete material verification or production documentation. Proper planning turns sequential activities into parallel activities where practical.
Schedule Preventive Maintenance Around Production
Unexpected equipment failure can disrupt an entire forging schedule. Presses, heating systems, lubrication equipment, handling systems, and dies all require maintenance.
Preventive maintenance for closed die forging should be planned around production demand whenever possible. Monitoring wear on critical components can also help manufacturers replace parts before a failure causes an extended stoppage.
Die maintenance deserves particular attention because excessive wear can affect both productivity and product quality. A die that requires repeated adjustments may create more downtime than a properly maintained tool.
Manage Production Batches Carefully
Production scheduling can have a substantial influence on changeover time. Grouping compatible parts and materials may reduce the number of die changes, heating adjustments, and process resets required during a shift.
However, large batches are not automatically better. Excessive batch sizes can increase inventory and extend the time before later orders enter production.
The optimal schedule should balance setup time, customer demand, material availability, equipment capacity, and delivery requirements.
How Can Data Help Improve Closed Die Forging Productivity?
Track the Right Production Indicators
Manufacturers should avoid relying on a single cycle-time figure. A more useful production dashboard can include the following:
-
Actual cycle time
-
Equipment availability
-
Die changeover time
-
Billet heating time
-
Scrap rate
-
Rework rate
-
Die life
-
Unplanned downtime
-
First-pass yield
-
Overall equipment effectiveness (OEE)
These indicators provide a clearer picture of where production time is being lost.
For example, a line may show excellent theoretical cycle time but poor equipment availability because of frequent stoppages. Another line may have slightly longer forging cycles but achieve better overall output because it requires fewer adjustments.
Use Process Data for Continuous Improvement
Sensors and production records can help identify patterns that are difficult to see from individual production runs. Temperature, press force, stroke position, lubrication timing, and other process variables may be monitored where appropriate.
The purpose of collecting this information should be practical: identify abnormal conditions, establish repeatable process windows, and support maintenance and quality decisions.
Advanced analytics and machine-learning tools may provide additional value when sufficient historical data is available. However, manufacturers should first establish reliable data collection and basic process control before introducing more complex systems.
What Should Buyers Discuss With a Forging Supplier?
Provide Complete Part Information
Production-time optimization begins before the purchase order. Buyers should provide the supplier with the latest part drawing, material specification, required quantity, dimensional tolerances, quality requirements, and expected delivery schedule.
If the component requires heat treatment, NDT, mechanical testing, machining, coating, or special documentation, those requirements should also be stated during quotation.
Complete information allows the forging supplier to evaluate the process route more accurately and avoid later changes that can extend tooling or production lead time.
Ask About Tooling and Production Capacity
When comparing suppliers, buyers should ask how the supplier plans to manufacture the part rather than focusing only on the quoted unit price.
Useful questions include:
-
What forging process is proposed?
-
How many forging stages are required?
-
What type of press will be used?
-
How will billets be heated and transferred?
-
What is the expected tooling lead time?
-
How are dies maintained?
-
What inspection stages are included?
-
What is the expected production capacity?
-
How will quality records and traceability be managed?
The answers can reveal whether the quoted delivery schedule is supported by a practical production plan.
Evaluate Quality and Delivery Together
Short production time has little value if it results in inconsistent parts. For industrial components, delivery performance needs to be considered alongside dimensional control, material verification, inspection, and traceability.
A capable supplier should be able to explain how the production route supports both output and quality. This is especially important for components used in demanding mechanical applications where material properties and dimensional consistency are critical.
Conclusion
You can’t just turn up the speed on the press to optimise production time in closed die forging. The best improvements are generally made by looking at the entire production flow, identifying the true bottlenecks and improving the areas that consistently cause waiting, rework, setup delays or unexpected downtime.
A better die design can increase the flow of material and avoid wasteful process repeats. Simulation can assist discover tooling problems before the production dies are finalised. Consistent billet cutting and heating results in more stable starting conditions. Automated handling and lubrication can increase repeatability in high volume production. At the same time, preventive maintenance, standardised changeovers and production data are tools for producers to control wasted time sources that are less visible.
For buyers, the choice of forging provider should also take into account production efficiency. Complete drawings, material requirements, quantities, tolerances, testing requirements and delivery targets enable the supplier to build a realistic process route and tooling plan.
Founded in 2001, Shaanxi Welong Int’l Supply Chain Mgt Co., Ltd. produces customised metal parts via forging, casting and machining. The company is ISO 9001:2015 and API-7-1 certified and assists projects requiring coordinated manufacturing, quality control and supply-chain management. For forging project, customer may give component drawing, material grade, expected quantity, needed specifications and delivery target for evaluation of process. This information provides a practical basis for the engineering and production team to discuss tooling, manufacturing stages, inspection requirements and production schedule.For more information or inquiries, please contact us at metal@welongpost.com.
FAQ
1: What are the main advantages of closed die forging?
Closed die forging offers high strength, precision, and material efficiency, making it ideal for producing complex, high-performance parts.
2: How does simulation-driven design benefit closed die forging?
Simulation-driven design allows for virtual optimization of die designs, reducing physical prototyping time and costs while improving part quality.
3: What role does material selection play in closed die forging efficiency?
Proper material selection for both dies and workpieces is crucial for optimizing die life, part quality, and overall production efficiency.
4: How can automation improve closed die forging operations?
Automation in material handling, die lubrication, and process control enhances consistency, reduces cycle times, and minimizes human error.
References
1. Smith, J. (2020). Advanced Techniques in Closed Die Forging. Journal of Manufacturing Processes, 45(2), 78-92.
2. Johnson, R., & Brown, T. (2019). Optimization Strategies for Die Design in Metal Forging. International Journal of Material Forming, 12(3), 401-415.
3. Lee, S., et al. (2021). The Role of Automation in Modern Forging Operations. Robotics and Computer-Integrated Manufacturing, 68, 102086.
4. Wilson, M. (2018). Material Selection for High-Performance Forging Dies. Materials & Design, 156, 327-340.
5. Chen, X., & Zhang, Y. (2022). Simulation-Driven Approaches in Closed Die Forging Process Design. Journal of Materials Processing Technology, 300, 117345.
6. Taylor, E. (2019). Process Monitoring and Control in Advanced Forging Operations. CIRP Annals, 68(2), 605-628.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

