How does heat treatment affect forged part performance?
Heat treatment can have a major influence on how forged parts perform after forging, machining, and assembly. Although forging already enhances the internal structure of many metal components by means of controlled plastic deformation, the forging process alone does not always give the end combination of hardness, strength, toughness, ductility and dimensional stability needed for service. Controlled alteration of the microstructure of forged material is achieved by carefully selecting heat treatment processes. These treatments may consist of annealing, normalising, quenching and tempering or other specialised treatments depending upon the grade of the material and the qualities required. The ultimate result is affected by heating temperature, holding duration, cooling rate, part geometry and chemical composition. “For manufacturers and OEM buyers, heat treatment should be viewed as part of the total forging process, and not a separate finishing operation. The right cycle can increase mechanical performance and uniformity, whereas an improper cycle may lead to excessive hardness, insufficient toughness, distortion, residual stress, etc.
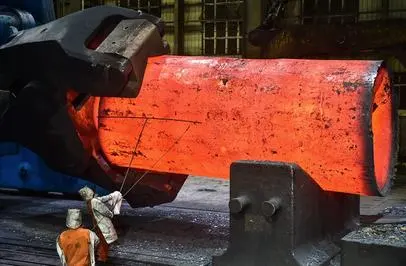
Why is heat treatment important after forging?
Heat treatment adjusts the microstructure created during forging.
Metal to large strains at high temperature. Depending on the forging method, material grade, amount of deformation and cooling conditions, the microstructure obtained may not yet have the homogeneity and/or mechanical qualities necessary in the completed part.
The structure can be easily tuned upon heat treatment. For example, normalising can be used to refine and homogenise the microstructure of acceptable carbon and low-alloy steels. Quenching and tempering can generate a stronger and harder structure with increased toughness compared with an untempered quenched condition.
The goal isn't only to make a forging harder. The correct heat treatment should be aimed at obtaining a microstructure that can satisfy the real service demands of the component.
Mechanical properties depend on more than hardness.
Hardness is generally one of the easiest attributes to quantify, but it should not be thought of as the sole measure of forging quality. A component may require a certain combination of tensile strength, yield strength, elongation, impact toughness, fatigue resistance and wear resistance.
A severely loaded shaft, for example, needs to be of great strength but must also possess enough toughness to withstand rapid loading. One wear-resistant part might need a higher surface or overall hardness, while another structural forging might need more ductility.
Manufacturers can use heat treatment to achieve a balance of these attributes instead of optimising a single value in isolation.
Dimensional stability also matters
Heat treatment may cause thermal stresses and dimensional changes, especially in components with large cross-sections, complex geometries or huge variances in section thickness.
This is critical for precision-machined forgings. If heat treatment produces distortion, extra machining may be needed, and in severe cases the component may not be within the dimensional tolerances set by the customer.
Heat treatment parameters should therefore be assessed combined with the geometry of forging, machining allowances and final dimensional requirements.
Which heat treatment processes are commonly used for forged parts?
Annealing for machinability and stress relief
Annealing is usually heating the steel to a temperature suitable for the steel and holding for a time at a comparatively moderate and controlled rate of cooling, as is commonly applied to forged parts. The exact cycle will depend on the grade of material and the desired effect of the treatment.
Annealing can lower hardness and increase machinability in suitable forged steels. This can be advantageous where a forging requires significant machining prior to final assembly.
Residual strains from prior manufacturing operations can also be reduced by annealing. This means less dimensional displacement during further machining due to reduced internal tension.
But you should not consider annealing as a general way of "making every forging softer". Different microstructures and characteristics are obtained by different annealing cycles, and the suitable treatment has to be chosen according to material specification.
Normalising for a more uniform structure
Normalising is usually accomplished by heating a suitable steel over its critical transformation temperature, maintaining it at temperature for the time necessary for the needed transformation and then cooling it in still air.
Normalisation is often cooled at a faster pace than full annealing. In many carbon and low-alloy steels this can create a finer ferrite-pearlite structure and can provide a more uniform distribution of mechanical characteristics.
Forged parts may be normalised if a more uniform microstructure is desired prior to machining or additional heat treatment. It can also be used as a preliminary treatment prior to quenching and tempering.
Quenching and tempering for strength and toughness
Quenching and tempering is the most common heat treatment for forged steel components that require a controlled mix of strength, hardness and toughness.
The process of quenching involves heating the material to the desired austenitising temperature range, then cooling at a rate fast enough to generate a hardened microstructure, usually with martensite. Depending on the steel grade and the geometry of the component, the quenching media can be water, oil, a polymer solution or another suitable medium.
Quenching may result in an extremely hard condition but one which may also have considerable residual tensions and excessive brittleness. Tempering is consequently often done subsequently. The component is warmed to a lower temperature, kept for a defined duration and chilled under controlled conditions.
Tempering decreases the brittleness of the as-quenched condition while keeping an acceptable degree of strength and hardness. The ultimate balance of characteristics is strongly dependent on the selected tempering temperature.
Quenching and tempering can be a key aspect in obtaining the needed mechanical properties for shafts, gears, heavy-duty pins, structural components and other highly stressed forgings.
How does cooling rate change the properties of forged parts?
Faster cooling can increase hardness.
The cooling rate of the material is one of the most essential variables in heat treatment, since it affects the formation of phases when the material passes through critical temperature ranges.
In certain steels, diffusion-controlled transformations can be prevented by fast cooling from the austenitising temperature, and martensite can develop. This usually results in a tougher and stronger state than if the cooling is slower.
But faster cooling is not necessarily good. Severe quenching might result in increased thermal and transformation stresses. Depending on the geometry and the substance, this may cause deformation or cracking.
The choice of quenching medium for forged parts therefore must take into account the hardenability of the steel, the size and geometry of the part, the desired hardness, and the amount of distortion that is acceptable.
Slower cooling can improve machinability and reduce stress.
Slower cooling usually gives more time for diffusion-controlled changes. This can result in a softer and more machinable microstructure in processes such as annealing.
This is advantageous when the forged part is later heavily machined after heat treatment. Lower hardness can minimise the cutting tool loads and make material removal easier.
Slower cooling rates compared to severe quenching may also result in reduced thermal gradients, although the actual dimensional and residual stress response is a function of the entire heat treatment cycle and component design.
The goal is therefore not only to choose the fastest or slowest cooling rate. The cooling rate should be consistent with the material and the qualities required in service.
Controlled cooling helps manage the trade-off.
In manufacturing controlled cooling can be employed when a more predictable development of the microstructure and dimensional behaviour is needed.
This is especially significant for big forgings or parts with large variations in cross-sectional thickness. Thin portions will cool faster than thick parts. This leads to differences in transformation behaviour and hardness.
Manufacturers may utilise proper furnace controls, quenching systems, agitation or other process controls to make cooling more uniform.
For complex forgings, the heat treatment may be supplemented by hardness surveys or mechanical testing at representative sites. This is an assurance that the indicated qualities are present across the component and not just at the surface.
How does material composition affect heat treatment results?
Carbon content influences hardness and transformation behaviour.
Carbon has a great influence on the heat treatment reaction of steel. However, the final result is determined by the full alloy composition and heat treatment cycle. Generally, increasing carbon content may enhance the hardness that can be reached in the hardened stage.
Carbon influences also transformation temperatures and properties of phases formed during cooling.
However, carbon content should not be utilised as a straight replacement for hardenability. Even if the carbon content of a steel is not very high, it can be effectively hardened through a bigger cross-section by proper alloying additions.
This difference is essential in the choice of material for big forged parts.
Alloying elements affect hardenability.
Chromium, manganese, molybdenum and nickel are some of the elements which may considerably impact the transformation behaviour and hardenability of steel.
Hardenability is the ability of a steel to reach a specified hardness at some depth after quenching. This is particularly critical to big forged components where the cooling rate is non-uniform in the section.
A massive forging may cool rapidly on the surface, while the middle cools more slowly. A steel with a proper hardenability can give the desired microstructure deeper in the component.
Therefore, the material selection and heat treatment design should be evaluated at the same time. The choice of steel grade based solely on its nominal carbon content may not be suitable for demanding large-section forgings.
Grain size affects strength and toughness.
Another major determinant in the performance of forged steel parts is grain size. A fine and more regular grain structure in many steels can give a desirable combination of strength and toughness.
Grain growth is affected by heat treatment settings. Too high an austenitising temperature or too lengthy holding durations may induce grain coarsening, which may have an adverse effect on certain mechanical qualities.
This is why the makers need to regulate not just the hardness after treatment but also temperature and holding duration.
The forging process itself also refines the grain and develops the structure. Heat treatment should therefore be designed with the prior forging history in mind.
What factors should manufacturers control during heat treatment?
Component size and geometry
A heat treatment schedule that works for a small forging may not produce the same result in a large component.
Thicker sections take longer to heat through and cool more slowly. Sharp transitions, holes, keyways, and other geometric features can also create differences in thermal behaviour and stress concentration.
Manufacturers should therefore consider the complete geometry of forged parts when establishing the heat treatment cycle.
Heating temperature and holding time
Temperature must be high enough to produce the intended transformation without causing unnecessary grain growth or other undesirable effects.
Holding time is equally important. The component needs sufficient time to reach the required temperature throughout its relevant section, but excessive holding can negatively affect the microstructure or production efficiency.
Heat treatment specifications should therefore define appropriate temperature ranges and holding requirements based on the material and component dimensions.
Quenching and tempering parameters
For quenched and tempered forgings, the quenching process and tempering cycle must be treated as a connected system.
Quenching determines the hardened condition, while tempering modifies that condition to obtain the required balance of strength, hardness, and toughness.
A supplier should be able to explain how the selected process relates to the material grade and specified mechanical properties rather than simply reporting that the component has been “heat treated".
Inspection and verification
Heat treatment quality should be verified using appropriate inspection methods. Depending on the application and specification, these may include hardness testing, tensile testing, impact testing, metallographic examination, dimensional inspection, and other non-destructive or destructive tests.
For critical applications, test results and heat treatment records can provide valuable traceability. Customers should also confirm whether the supplier can provide the inspection documentation required by the project specification.
How should buyers evaluate heat treatment when sourcing forged parts?
Start with the material and required properties.
Before selecting a supplier, buyers should define the material grade, component dimensions, service conditions, and required mechanical properties.
If the drawing specifies tensile strength, yield strength, elongation, impact toughness, hardness, or another property, these requirements should be communicated clearly to the forging manufacturer.
The supplier can then determine whether the proposed forging and heat treatment route is suitable.
Ask about process control and inspection.
A reliable forging supplier should be able to explain its basic manufacturing and heat treatment capabilities without relying only on general statements such as “high quality” or “advanced technology".
Useful questions include:
-
Which heat treatment processes are available?
-
Which steel grades can be treated?
-
How are furnace temperatures monitored and recorded?
-
How are large or complex forgings handled during quenching?
-
What mechanical tests can be provided?
-
Can heat treatment records and inspection reports be supplied?
-
Can forging, heat treatment, machining, and inspection be coordinated as one production process?
These questions help buyers evaluate the actual manufacturing capability behind a supplier's claims.
Consider the complete manufacturing route.
Heat treatment is only one stage of a forged component's production route. Forging method, material quality, heat treatment, machining allowance, dimensional control, and final inspection all influence the finished product.
For OEM projects, it is often more efficient to work with a supplier capable of coordinating multiple stages of production. This can reduce communication gaps between separate vendors and make it easier to maintain traceability from raw material through final inspection.
Conclusion
Heat treatment has a direct influence on the mechanical performance, microstructure, hardness, toughness, machinability, and dimensional stability of forged parts. Annealing can improve machinability and help relieve residual stress, while normalising can produce a more uniform and refined structure in suitable steels. Quenching and tempering can provide a controlled balance of hardness, strength, and toughness for components exposed to demanding loads.
The final result depends on more than the selected heat treatment name. Material composition, hardenability, grain size, component geometry, section thickness, heating temperature, holding time, cooling rate, and tempering conditions all need to be considered together. Excessively aggressive cooling, for example, may increase hardness but also raise the risk of distortion or cracking.
For this reason, heat treatment should be developed as part of the overall forging and manufacturing process. Buyers evaluating forged components should look beyond a basic “heat treated” statement and ask about material selection, process control, mechanical testing, inspection, and traceability.
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd., established in 2001, provides customised forging, casting, and machining solutions for customers across different industrial applications. The company works with a range of metal materials and supports processes from engineering and manufacturing through quality control and delivery. With ISO 9001:2015 and API-7-1 certifications, Welong can support customers that require controlled production processes and documented quality requirements.
For OEM and industrial projects, coordinating forging, heat treatment, machining, and inspection through an experienced manufacturing partner can help simplify procurement and improve consistency. Discussing the material grade, drawing requirements, heat treatment specification, mechanical properties, and inspection requirements with the supplier at the beginning of a project can also help ensure that the finished forging is manufactured for its intended operating conditions. For more information, contact us at metal@welongpost.com.
FAQ
1: What is the primary purpose of heat treating forged parts?
The primary purpose is to enhance mechanical properties such as strength, hardness, and durability while relieving internal stresses.
2: How does annealing benefit forged parts?
Annealing softens the metal, improves machinability, and relieves internal stresses in forged parts.
3: What effect does rapid cooling have on forged parts during heat treatment?
Rapid cooling typically increases hardness and strength but can also introduce brittleness and internal stresses.
4: How does carbon content affect the heat treatment of forged parts?
Higher carbon content generally increases the hardenability of forged parts, allowing for greater hardness after quenching.
References
1. Smith, J. (2018). "Principles of Heat Treatment for Forged Components." Journal of Materials Processing Technology, 256, 112-124.
2. Johnson, A. & Brown, M. (2019). "Effect of Cooling Rates on Microstructure and Mechanical Properties of Forged Steels." Metallurgical and Materials Transactions A, 50(3), 1425-1437.
3. Zhang, L. et al. (2020). "Influence of Alloying Elements on Phase Transformations in Heat-Treated Forgings." Materials Science and Engineering: A, 772, 138709.
4. Thompson, R. (2017). "Optimization of Heat Treatment Processes for High-Performance Forged Parts." International Journal of Advanced Manufacturing Technology, 88(5-8), 1845-1858.
5. Garcia, C. & Martinez, V. (2021). "Grain Size Control in Heat-Treated Forged Components: A Comprehensive Review." Materials Today: Proceedings, 45, 3256-3265.
6. Wilson, E. (2016). "Advanced Heat Treatment Techniques for Improving Forged Part Performance." Heat Treatment and Surface Engineering, 2(1), 15-29.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

