How does closed die forging work?
Closed die forging is a metal-forming process that utilises curved dies to press a hot workpiece into a component with controlled geometry. In closed die forging, the material is forced into the required shape by impressions in the dies, but in open die forging it is freer to spread out. It is a process used for components that require high strength, uniform dimensions and predictable mechanical performance. The idea is simple. A measured billet or preform is heated to a suitable forming temperature and placed in the lower die and pressed by the upper die. The metal is driven into the die cavity under pressure. Depending on the part design, numerous forging procedures are required for the final geometry. Excess material may flash around the line of separation and this is removed in a subsequent trimming process. Understanding how Closed die forging works is essential to manufacturers and industrial buyers since the process affects material usage, dimensional accuracy, mechanical strengths, tooling costs and downstream machining needs. The result, however, is not solely a function of the forging press, but of the material chosen, the shape of the die, the management of heat, lubrication, the sequence of forging, heat treatment and inspection.
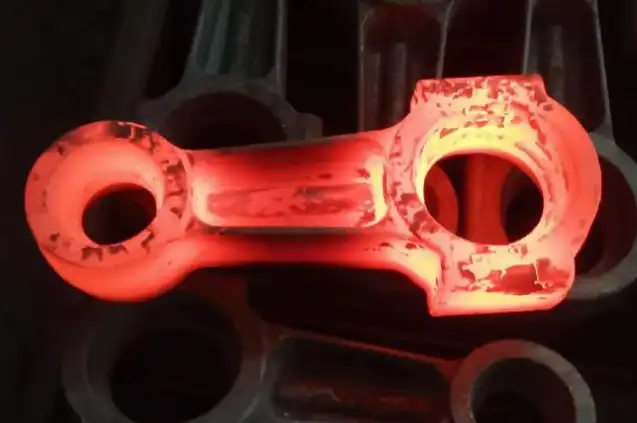
What happens during the closed die forging process?
Selecting and preparing the forging material
The first step is to choose a metal or alloy that is appropriate for the mechanical and service requirements of the component. Materials: carbon steels, alloy steels, stainless steels, aluminium alloys, and titanium alloys. The decision relies on the strength, toughness, corrosion resistance, operating temperature, weight and the environment in which it is to be used.
The chosen material is then cut to preset sizes in the form of bars, billets or other stock shapes. Controlling the initial weight is critical because the billet must contain enough material to fill the die chamber and allow for trimming and other process losses.
The material traceability is especially significant for industrial applications. The material used for a forging should be traceable to its heat or lot documentation by a skilled manufacturing process. Depending on the customer's requirements, these may contain material certificates, records of the chemical composition, mechanical test results and other quality documentation.
Heating the workpiece to the correct temperature
The billet is heated before forging so that the material is malleable enough to flow under pressure without excessive forming force.
The correct temperature depends on the alloy. There are temperature ranges at which steel grades, aluminium alloys, titanium alloys and nickel-based alloys can be forged. Therefore, a set temperature should not be considered a universal criterion for all closed die forging applications.
Heating also has to be carefully monitored. If the workpiece is too cold, the material may not fill the die properly, and the forging forces can increase. Too much heat, however, can cause oxidation, grain formation, surface damage or other metallurgical difficulties depending on the alloy.
Hence, the temperature of the furnace and the period of heating are controlled in the industrial forging operation as per the material and process specification. In some applications, dies are additionally warmed to avoid excessive heat loss while the hot billet is in contact with the tooling.
Designing and preparing the forging dies
One of the most critical steps of closed die forging is the design since the die controls the flow of metal and the closeness of the forged component to its planned shape.
Engineers will often generate a 3-D model of the component and construct the die cavity around the desired shape. Important design parameters are parting line, draft angles, fillet radii, wall thickness, flash land, machining allowance and projected material flow.
Modern CAD and forging simulation software can allow engineers to discover possible difficulties before real tooling is made. Simulation can be used to study the filling behaviour, the forming load, the temperature distribution and potential areas where defects or incomplete filling might occur.
The dies are usually made from heat-resistant tool steels chosen for their ability to tolerate repetitive mechanical and thermal stress. Depending on the material being forged and the amount of production, the surface treatments or coatings can also be considered to improve the wear resistance and lengthen the tool life.
Positioning the billet and forming the component
The billet is then transported to the forging area, where it is inserted into the lower die. The higher die then slides toward the lower die under the force created by a mechanical press, hydraulic press or other suitable forging machine.
As the dies close, the billet is crushed and is forced to flow into the formed cavity. The material does not just flow in one direction. It is controlled by the cavity geometry, friction conditions, billet volume, forging temperature and the sequence of deformation.
For reasonably basic components one main forging stroke may be sufficient. More complex parts may need numerous processes like preforming, blocking and finishing. These intermediate steps assist in managing the flow of material and limit the chance of faults.
Managing flash and trimming
In many typical closed-die forging designs, the surplus metal is expelled into a small area surrounding the die splitting line. This surplus material is called flash.
Flash is a key factor in the forging process, as it generates pressure in the die cavity and allows the material to fill the precise portions of the imprint. However, flash is not generally part of the finished component.
The component is then sent to a trimming procedure where the excess flash is trimmed away. The way the part is trimmed is determined by its geometry, its material, the volume of manufacturing and the dimensional requirements.
Modern near-net-shape forging methods are designed to minimise flash and reduce the amount of machining required thereafter. But after forging, the quantity of material removed still relies on the tolerances necessary and the final geometry.
What factors affect closed die forging quality?
Material flow and grain structure
One of the big reasons manufacturers utilise closed die forging is the favourable grain flow which can be developed during deformation. A properly planned forging process can allow the grain flow to follow the basic geometry of the part instead of being interrupted by excessive material removal.
This can lead to good strength and fatigue performance, especially when the forging is laid out for a rigorous load path. But the flow of grains doesn’t guarantee performance. Final properties are also a function of alloy chemistry, deformation circumstances, heat treatment, cooling rate and inspection results.
Instead, safety-important components require producers to oversee the whole process, not only be able to say a component is forged.
Die alignment and dimensional control
Proper alignment of the dies is critical in making consistent parts. Misalignment can lead to uneven parting lines, dimensional variance, excessive flash, or issues in later machining.
Thus, dimensional inspection is a key aspect of production quality control. Depending on the component, producers may utilise gauges, callipers, coordinate measuring machines (CMMs), optical inspection systems or other measurement equipment.
Check key dimensions against the approved drawing or technical specification. Inspection records can be important documentation for OEM projects verifying production items are still within the specified dimensional tolerances.
Temperature, lubrication, and process consistency
Temperature affects the material flow and forging force directly. A controlled forming window will ensure that the material performs the same from batch to batch.
Another crucial factor is lubrication. Proper die lubrication reduces workpiece-to-tooling friction, promotes material flow, reduces die wear and aids part release.
The specific lubricant and application procedure will depend on the alloy, forging temperature, die material and equipment. Automated lubrication systems can provide consistency in high-volume production by managing the amount and timing of lubricant application.
What are the main advantages of closed die forging?
High strength and reliable mechanical performance
The closed die forging process has the benefit of producing parts with good mechanical performance if the material and process are regulated.
The deformation process can increase the consolidation of the material and provide the desired grain flow. This makes forged components suited for applications where strength, toughness, fatigue resistance and durability are required.
Typical applications are automotive drivetrain components, industrial machinery parts, construction equipment components, aerospace hardware and other load-carrying goods.
Complex shapes with reduced machining requirements
Closed die forging can make shapes that would require a great deal of machining if they were made from a solid block of material.
Because much of the needed shape is created by the die cavity during forging, the completed forging can be closer to the final geometry than a plain billet. This can cut down on machining time and material removal.
But “near-net shape” does not mean there is no need for machining. Even with forging, CNC machining may be needed for critical surfaces, holes, threads, bearing seats and other precise features.
Better material utilisation for suitable production volumes
Closed die forging can make shapes that would require a great deal of machining if they were made from a solid block of material.
Because much of the needed shape is created by the die cavity during forging, the completed forging can be closer to the final geometry than a plain billet. This can cut down on machining time and material removal.
But “near-net shape” does not mean there is no need for machining. Even with forging, CNC machining may be needed for critical surfaces, holes, threads, bearing seats and other precise features.
When is closed die forging a good manufacturing choice?
High-volume production
Closed die forging is particularly attractive when a project requires repeated production of the same or similar components. Once the dies have been developed and validated, they can be used repeatedly to produce consistent shapes.
For OEMs and industrial buyers with stable annual demand, the initial tooling investment can therefore be justified by lower production costs over the product lifecycle.
Components exposed to demanding loads
Forging is often selected for components where mechanical reliability is more important than simply achieving a particular external shape.
Parts exposed to repeated loads, impact, vibration, or high mechanical stress may benefit from an appropriately designed forged structure. Examples include shafts, connecting components, gears, levers, brackets, and heavy machinery parts.
The actual suitability must still be confirmed through engineering analysis and applicable material and testing requirements.
Projects requiring repeatable production
For international OEM projects, consistency between batches is often just as important as the performance of an individual part. A properly controlled forging process can support repeatable dimensions and mechanical properties.
Buyers should therefore look beyond the forging equipment itself and evaluate the manufacturer's complete quality system, including incoming material inspection, process control, heat treatment, dimensional inspection, mechanical testing, and traceability.
How has technology improved closed die forging?
CAD and forging simulation
Modern CAD software allows engineers to develop detailed die models before tooling production begins. Forging simulation can then help predict how the material will flow through the cavity.
This digital approach can identify potential filling problems, excessive forming loads, and areas requiring design changes before expensive production tooling is completed.
For customised components, simulation can therefore reduce development iterations and support a more controlled transition from engineering design to production.
Automated forging and material handling
Automation has become increasingly important in modern forging facilities. Robots and automated handling systems can transfer heated billets between heating equipment, presses, trimming stations, and other process stages.
Automation can reduce unnecessary manual handling of hot materials and improve process repeatability. It can also help maintain consistent cycle times, billet positioning, lubrication, and production records.
For high-volume closed die forging manufacturing, these improvements can contribute to better productivity and more stable quality.
Advanced die materials and surface treatments
Forging dies are repeatedly exposed to high temperatures, pressure, friction, and thermal cycling. The wear can therefore become an important factor in production economics and dimensional stability.
Advances in tool steels, heat treatment, surface engineering, and coatings can improve resistance to wear and thermal damage. The appropriate solution depends on the material being forged, forging temperature, production volume, and die geometry.
Rather than assuming that one coating or die material is suitable for every application, manufacturers should select tooling materials according to the actual process conditions.
What should buyers check when sourcing closed-die forged parts?
Confirm the complete manufacturing route.
Instead of simply asking whether a supplier can provide a forged component, buyers should ask for the proposed manufacturing route. This may include billet preparation, heating, preforming, closed die forging, trimming, heat treatment, surface cleaning, machining, and final inspection.
Understanding the complete route makes it easier to identify where dimensional variation or quality risks may occur.
Review inspection and traceability capabilities.
For industrial components, buyers should confirm what inspection documentation can be supplied with each batch. Depending on the application, this may include material certificates, heat treatment records, dimensional inspection reports, mechanical test results, and certificates of conformity.
Traceability is particularly important when components are used in demanding equipment or when the customer has strict quality documentation requirements.
Evaluate tooling and production capability.
A capable supplier should be able to explain how the proposed die design supports the required component geometry and production quantity.
Buyers should also consider whether the supplier can support the full project lifecycle, from prototype development and tooling through mass production, machining, inspection, and delivery.
This can reduce communication gaps between separate suppliers and make production changes easier to manage.
Conclusion
Modern production uses closed die forging because it can produce strong, accurately shaped components with repeatable properties and efficient material utilisation when the process is properly designed. The method is particularly valuable for high-volume applications and components that must withstand demanding mechanical loads.
The quality of a forged part, however, depends on much more than pressing hot metal between two dies. Material selection, billet preparation, heating, die design, material flow, lubrication, trimming, heat treatment, machining, and inspection all influence the final result.
Technology is continuing to improve the process through CAD modelling, forging simulation, automated handling, advanced tooling materials, and more consistent process monitoring. These developments allow manufacturers to produce increasingly complex components while improving repeatability and controlling production costs.
For companies sourcing custom forged components, the most important consideration is not simply whether a supplier offers closed die forging, but whether the supplier can control the complete manufacturing chain and provide consistent quality from raw material to finished part.
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd., established in 2001, provides customised metal components for customers in different industrial sectors. With ISO 9001:2015 and API-7-1 certifications, the company supports forging, casting, and machining projects from manufacturing planning through final delivery. Its experience with customised metal parts allows customers to coordinate different production stages with one supplier, while quality control and inspection procedures help maintain consistency across production batches. For OEMs and industrial buyers, this integrated approach can simplify sourcing, improve communication, and support the development of forged components according to specific drawings, materials, dimensions, and application requirements. For inquiries, please contact us at info@welongpost.com.
FAQ
1: What is the main difference between closed die forging and open die forging?
Closed die forging uses dies that completely enclose the workpiece, producing near-net shape parts with high precision. Open die forging uses simpler dies and is better suited for larger, less complex shapes.
2: What types of materials can be used in closed die forging?
Closed die forging can be used with a wide range of metals, including carbon steel, alloy steel, stainless steel, aluminum alloys, titanium, and various other metals and alloys.
3: How does closed die forging improve the mechanical properties of a part?
The intense pressure applied during forging refines the grain structure of the metal, increasing strength, toughness, and fatigue resistance while eliminating internal voids.
4: Is closed die forging suitable for small production runs?
While closed die forging is most cost-effective for large production runs due to high initial tooling costs, advancements in technology are making it increasingly viable for smaller batches.
References
1. Smith, J. (2019). Advanced Techniques in Closed Die Forging. Journal of Manufacturing Processes, 45, 112-125.
2. Johnson, R., & Williams, T. (2020). Comparative Analysis of Forging Methods in Aerospace Applications. International Journal of Materials and Manufacturing Processes, 33(2), 78-92.
3. Brown, A. (2018). The Evolution of Die Design in Metal Forming Processes. Materials Science and Engineering: A, 712, 281-295.
4. Lee, S., & Park, K. (2021). Simulation-Driven Optimization in Closed Die Forging. Journal of Materials Processing Technology, 289, 116935.
5. Thompson, M. (2017). Advances in Automated Forging Systems: A Review. Robotics and Computer-Integrated Manufacturing, 47, 1-12.
6. Garcia, E., & Martinez, L. (2022). Novel Coatings for Extended Die Life in High-Temperature Forging. Surface and Coatings Technology, 428, 127774.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

