Hot Forging Process Challenges and How to Solve Them?
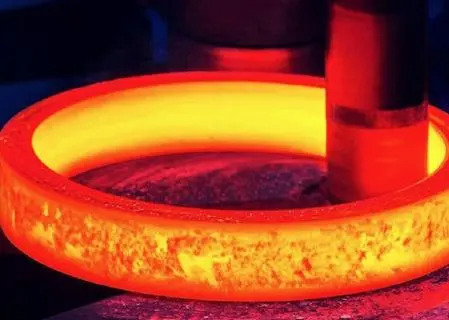
Hot Forging is commonly utilised to make high-strength metal parts for applications where mechanical performance, structural integrity and repeatable manufacturing are required. Unlike cold forming, this procedure requires heating of the workpiece to an appropriate forging temperature before applying compressive force through dies. The heat reduces the material's resistance to distortion and allows producers to make shapes which would be difficult or expensive to make at normal temperatures.
But hot forging is not only about heating metal and pressing it in a die. Temperature variation, uncontrolled material flow, die wear, dimensional changes, oxidation and process inefficiencies can all affect the finished component. If uncontrolled, these issues can cause underfilling, large flash, surface flaws, inconsistent dimensions, early die failure and wasteful energy use by the producers.
Knowledge of these problems is crucial both to the manufacturer of forgings and to the consumer of forged components. A stable process is based on the correct material selection, the preform design, the die engineering, the temperature management, and the condition and inspection of the equipment. This article looks at the most prevalent hot forging problems and what producers may do to increase process stability and part quality.
What Causes Material Flow Problems in Hot Forging?
The material flow controls the filling capacity of the heated billet in the die cavity. Although the forging procedure as a whole may be stable, the flow may be poorly managed and cause local problems.
Improve Preform Design and Material Distribution
One of the typical problems is the uneven distribution of the material throughout the forging process. If the beginning billet or preform does not contain the required quantity of material in the right places, some regions of the die may be underfilled while other regions of the die create excessive flash.
Preform geometry is thus a key feature of process development. Rather than pressing the original billet straight into the final cavity, fabricators may utilize one or more intermediate forming steps to help guide material into areas requiring extra volume.
Computer-aided design and finite element analysis (FEA) can be of use in this stage. Simulation lets engineers examine filling behavior, material flow, deformation, and forging load before investing in production tooling. It is also helpful to identify problematic folding or underfilling areas at an earlier stage.
The geometry and lubrication should be examined simultaneously. Good lubrication can reduce the friction between the workpiece and die surfaces, and well-planned radii, transitions, and flash lands can help promote more predictable material movement.
The challenge with complex components is not only to fill the cavity. The method should lead the material through the hollow, not create unfavorable flow patterns that could influence the final portion.
Control Flash, Folding, and Underfilling
Three observable effects of bad material flow include flash, underfilling, and folding.
Underfilling occurs when (1) the billet capacity is insufficient, (2) the workpiece loses excessive heat before forming, or (3) the die design does not offer an appropriate flow path.
Overflashing can be caused by too much billet, wrong process parameters, or a mismatch between the die design and the forming sequence.
Folds or laps occur when the surface of the material folds back on itself, rather than flowing smoothly to the desired geometry. Such faults demand special care, as they may be present in the forged component after future procedures.
These difficulties can be corrected by the manufacturer through assessment of the billet dimensions, preform geometry, die transitions, lubrication, forging sequence, and workpiece temperature. Then production trials should be compared with simulation results and inspection data instead of visual judgment.
How Can Forging Dies Be Protected From Wear and Deformation?
Forging dies are subjected to repetitive mechanical stresses and high temperatures. This combination can result in wear, cracking, deformation, and loss of dimensional accuracy over time.
Select Die Materials for the Actual Service Conditions.
The material selection must consider the forging temperature, workpiece material, forming load, manufacturing volume, and estimated service life.
A die material that is acceptable in a low-volume application may not have the same service life under continuous high-volume production. Thermal fatigue is especially critical when dies are exposed to repeated heating and cooling cycles.
Manufacturers should consequently consider not only hardness but also hot strength, toughness, thermal fatigue resistance, and wear resistance. The right combination will depend on the forging application.
The surface treatment or coating can also be considered when compatible with the material and the operating conditions of the die. The general aim is to reduce surface deterioration and to enhance useable die life rather than to increase hardness alone.
Establish a Preventive Die Inspection Routine.
Waiting until a die produces visibly defective parts is usually not an efficient maintenance strategy. Periodic inspection can identify progressive wear before it causes a major production problem.
Critical dye areas should be monitored for the following:
-
cavity wear
-
cracks
-
deformation
-
damaged radii
-
surface deterioration
-
changes in flash formation
-
dimensional changes in forged parts
Inspection frequency should be related to production volume and the severity of the forging application. For repeat production, historical inspection data can help manufacturers establish practical maintenance intervals.
Replacing or repairing a die at the appropriate time can prevent larger production losses caused by rejected batches, unexpected downtime, and damage to downstream equipment.
Why Is Temperature Control Critical in Hot Forging?
Temperature is one of the most important variables in hot forging because it influences material flow stress, deformation behavior, surface condition, die loading, and final properties.
Maintain a Consistent Forging Temperature
If the workpiece is too cold, deformation resistance increases and the required forming load may rise. The material may also become more difficult to fill in complex sections.
If the workpiece is overheated, excessive oxidation, grain growth, or surface degradation may occur depending on the alloy and process conditions.
For this reason, the target temperature should be established according to the material grade and forging process rather than applying one temperature range to every alloy.
Temperature monitoring can be performed at appropriate points throughout heating and forging. Where necessary, automated controls can adjust heating parameters to maintain greater consistency between production batches.
The time between furnace removal and die contact should also be controlled. A workpiece may lose substantial heat during transfer, particularly when the transfer distance is long or the production cycle is slow.
Reduce Heat Loss During Transfer
Heating equipment is only one part of temperature management. Handling systems, transfer time, furnace loading patterns, and production layout can also influence heat loss.
Manufacturers can reduce unnecessary temperature variation by minimizing transfer distances, coordinating heating and forging cycles, and avoiding unnecessary waiting time between operations.
For suitable applications, induction heating can provide rapid and localized heating with good process control. Furnace heating may remain appropriate for other production requirements, especially when large quantities or specific heating profiles are involved.
The best heating method depends on workpiece dimensions, alloy characteristics, production volume, required temperature uniformity, and overall equipment configuration.
What Can Manufacturers Do to Improve Dimensional Accuracy?
Dimensional accuracy in a forged component depends on more than the final die cavity. Material volume, temperature, die wear, elastic deformation, trimming, heat treatment, and subsequent machining can all influence the final dimensions.
Optimize the Preform and Forging Sequence
The closer the material distribution is to the desired final geometry before the finishing operation, the easier it becomes to control the final dimensions.
A well-designed preform reduces unnecessary material movement and can improve cavity filling. Multiple forming stages may be appropriate for components with complex geometries or significant differences in cross-sectional area.
FEA simulation can help engineers evaluate how changes in billet size, preform geometry, friction assumptions, and forming sequence affect the result.
However, simulation should support production engineering rather than replace physical validation. Trial forgings, dimensional inspection, and process adjustments remain important when introducing a new component.
Improve Die Manufacturing and Alignment
Even a well-designed forging process can produce inconsistent results if the dies are manufactured inaccurately or incorrectly aligned.
Modern CNC machining and EDM processes can produce complex die geometries with controlled dimensions. During die assembly, proper alignment is equally important because misalignment can influence flash distribution, part geometry, and die wear.
Manufacturers should also identify critical-to-function dimensions on the forged component. Not every surface requires the same tolerance. Establishing which dimensions are functionally important helps determine where forging accuracy is essential and where subsequent machining is more appropriate.
This approach can prevent unnecessary tooling costs while maintaining the performance requirements of the finished component.
Use Trimming, Heat Treatment, and Machining Strategically
Forging is often one stage within a larger manufacturing process. After forming, components may require trimming, heat treatment, shot blasting, machining, or inspection.
Trimming removes unwanted flash and establishes the basic outline of the part. Heat treatment may then be used when required by the material specification or component application to obtain the required metallurgical condition.
Machining is commonly used for surfaces that require tighter dimensional control than the forging process can economically provide.
Manufacturers should therefore define the relationship between forging tolerances and machining allowances during the initial process design. Leaving insufficient machining allowance can make final correction difficult, while excessive allowance can increase material removal, machining time, and cost.
How Can Hot Forging Operations Reduce Energy Consumption?
Hot forging requires significant energy because the workpiece must be heated before deformation. Energy efficiency therefore has both economic and operational importance.
Improve Heating Efficiency
A well-maintained heating system can reduce unnecessary energy loss. Manufacturers should monitor furnace condition, insulation performance, heating cycles, and loading efficiency.
Poor insulation allows heat to escape into the surrounding environment, while inefficient furnace loading can result in uneven heating or unnecessary operating time.
For appropriate applications, induction heating can provide rapid heating with precise control. However, the energy performance of any heating method should be evaluated based on the complete production cycle rather than comparing equipment types in isolation.
Optimize Cycle Time Without Sacrificing Quality
Shorter cycle time does not automatically mean better production. If the process is accelerated beyond suitable limits, operators may experience inadequate die filling, excessive equipment loading, or temperature instability.
The objective should be to eliminate unnecessary waiting, handling, reheating, and idle time while maintaining the required forging conditions.
Process monitoring can help identify bottlenecks. For example, if workpieces repeatedly wait between heating and forging, production scheduling or material handling may need adjustment rather than simply increasing furnace capacity.
Near-net-shape forging can also reduce downstream machining requirements for suitable components. When less material needs to be removed after forging, the overall manufacturing route may require less machining time and material consumption.
Maintain Equipment and Tooling
Equipment condition directly affects production efficiency. Worn dies, poor alignment, hydraulic problems, inefficient heating systems, and unplanned equipment stops can increase energy consumption per acceptable part.
Preventive maintenance helps reduce these losses. Presses, heating equipment, transfer systems, lubrication equipment, and dies should be inspected according to their operating conditions and maintenance requirements.
The most meaningful efficiency indicator is not simply energy used by the furnace. Manufacturers should consider energy consumption in relation to the number of conforming components produced.
How Should Manufacturers Control Surface Quality?
Surface condition is another important consideration in hot forging. Heating can produce scale and oxidation, while unsuitable die surfaces or lubrication conditions may influence surface appearance.
Manage Oxidation and Scale Formation
Oxidation increases as heated metal is exposed to the atmosphere. Excessive scale can affect surface quality and may also influence subsequent machining or finishing operations.
The appropriate heating environment depends on the alloy, component requirements, equipment, and production economics. Manufacturers should control heating conditions and avoid unnecessary exposure time at elevated temperatures.
Where surface quality is critical, the process may require additional cleaning or surface treatment after forging.
Monitor Lubrication and Die Surface Condition
Lubrication can influence friction, material flow, die temperature, and surface quality. Too little lubrication may increase friction and die wear, while an unsuitable application method can produce inconsistent results.
The lubrication system should therefore be monitored as part of normal process control rather than treated as an isolated operation.
Consistent application is particularly important in automated or high-volume production because variations between cycles can eventually become variations in part quality.
What Should Buyers Check When Selecting a Hot Forging Supplier?
For buyers, evaluating a supplier involves more than comparing the quoted price. A technically suitable supplier should be able to explain how the forging process will meet the drawing, material, inspection, and production requirements.
Review Manufacturing and Inspection Capabilities
Before placing an order, buyers should consider whether the supplier can support the complete manufacturing route required for the component.
Important questions include:
-
What forging equipment is available?
-
Which material grades can be processed?
-
Can the supplier manufacture or modify forging dies?
-
Is CNC machining available after forging?
-
What dimensional inspection equipment is used?
-
Can material and inspection documentation be provided?
-
What heat-treatment capabilities are available when required?
-
Can the supplier support prototype and repeat production?
These questions are especially relevant for custom forgings because tooling, process development, and inspection requirements can vary considerably between components.
Provide Complete Technical Information for Quotation
A supplier can normally prepare a more accurate quotation when the buyer provides sufficient technical information.
Useful information may include the material grade, component drawing, target dimensions, annual or batch quantity, required surface condition, heat-treatment requirements, machining requirements, inspection standards, and packaging expectations.
If certain dimensions are critical to assembly or performance, they should be clearly identified on the drawing.
Clear technical communication at the quotation stage reduces the risk of misunderstandings later in tooling, production, and inspection.
Conclusion
Hot forging offers an effective manufacturing route for producing strong and durable metal components, but consistent results depend on controlling several variables at the same time. Material flow, die condition, forging temperature, dimensional accuracy, surface quality, energy use, and equipment maintenance all influence the stability of the production process.
Manufacturers can address these challenges by improving preform and die design, using appropriate simulation and inspection methods, maintaining controlled heating conditions, monitoring tooling, and optimizing the complete production cycle. Buyers can also contribute to a successful project by providing clear drawings, material requirements, quantities, tolerances, and inspection expectations at the beginning of the sourcing process.
For custom components, the most reliable approach is to evaluate the entire manufacturing route rather than focusing on one parameter in isolation. A supplier with appropriate forging, machining, inspection, and quality-control capabilities can help identify potential production issues before they become costly problems.
Welong Delivers Quality Metal Parts for Global Industries
Shaanxi Welong Int'l Supply Chain Mgt. Co., Ltd. provides metal manufacturing and supply-chain services for customers requiring forged, cast, and machined components. The company works with materials including steel, stainless steel, aluminum, and other metal grades according to project requirements.
Its capabilities cover different stages of metal component production, allowing customers to discuss forging, casting, machining, inspection, and delivery requirements within one supply-chain process. For projects involving hot forging, technical factors such as material grade, component geometry, forging sequence, dimensional requirements, heat treatment, and subsequent machining can be reviewed before production.
Welong states that its quality management system includes ISO 9001:2015 and API-7-1-related capabilities. Its experience in international supply-chain management also supports customers who require coordinated production and delivery for industrial metal components.
When requesting a quotation, customers can provide drawings, material specifications, target quantities, tolerances, inspection requirements, and any downstream machining requirements. With this information, the manufacturing team can better evaluate hot forging, tooling, process requirements, production feasibility, and the appropriate manufacturing route for the component.
We have over 100 clients around the world who work in car and other businesses. Please mail us at info@welongpost.com if you require more data or have questions.
FAQ
1: What is hot forging?
Hot forging is a manufacturing process where metal is heated above its recrystallization temperature and shaped using dies and presses, resulting in improved material properties and complex shapes.
2: How does temperature control affect hot forging quality?
Precise temperature control is crucial in hot forging as it influences material flow, die filling, and final product properties. Fluctuations can lead to defects and inconsistent quality.
3: What are some common challenges in hot forging?
Common challenges include uneven material distribution, die wear and deformation, temperature control issues, and achieving dimensional accuracy in final products.
4: How can manufacturers improve dimensional accuracy in hot forged parts?
Dimensional accuracy can be improved through optimized preform design, precise die manufacturing, and careful post-forging processes and heat treatment.
References
1. Smith, J. R., & Johnson, A. B. (2019). Advanced Techniques in Hot Forging Process Optimization. Journal of Materials Processing Technology, 287, 116-128.
2. Lee, Y. S., & Kim, H. J. (2020). Energy Efficiency Improvements in Hot Forging Operations. International Journal of Precision Engineering and Manufacturing-Green Technology, 7(2), 421-436.
3. Wang, L., & Zhang, G. (2018). Dimensional Accuracy Control in Hot Forging: A Comprehensive Review. Journal of Manufacturing Processes, 35, 239-255.
4. Brown, T. C., & Davis, E. F. (2021). Die Wear Mitigation Strategies for Hot Forging Processes. Wear, 476, 203675.
5. Anderson, M. K., & Wilson, R. T. (2017). Material Flow Control in Complex Hot Forging Operations. Journal of Materials Engineering and Performance, 26(8), 3712-3724.
6. Thompson, S. L., & Roberts, C. J. (2022). Advancements in Simulation Technologies for Hot Forging Process Design. Computers & Industrial Engineering, 165, 107917.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

