Drop Forging Explained: How It Works and When to Use It?
Drop Forging is a metal forming method that produces strong, durable parts by using controlled impact pressures on heated metal within a forging die. Forging alters the workpiece without material removal and maintains the continuous metal structure. Machining, by contrast, removes material to produce a shape. This makes drop forging excellent for numerous components that are subject to repetitive loading, impact, pressure and mechanical stress. This method is used extensively for automotive, oil and gas, heavy equipment, industrial machinery and other applications where component reliability is important. However, not every part is best served by drop forging by default. Considerations include tooling investment, volume of production, material selection, component geometry, dimensional requirements and secondary machining. Knowing how the process works and where it adds the most value can assist engineers and procurement teams decide if forged manufacturing is right for a certain application.
How Does Drop Forging Work?
Preparing the Metal Before Forging
Usually the process begins with a billet, bar, or other suitable piece of metal. The raw material is cut to a set size and weight, depending on the final component and the estimated material loss during forging.
It is crucial to prepare stocks properly. If the original material is too tiny, the die cavity may not be filled well. If it’s too big, too much flash can mean more material is consumed and more trimming is needed.
It must also be compliant with the chosen forging temperature and deformation conditions. Some of the popular materials are carbon steel and alloy steel. Non-ferrous metals like aluminum can also be forged if the right equipment and process parameters are used.
Heating the Workpiece
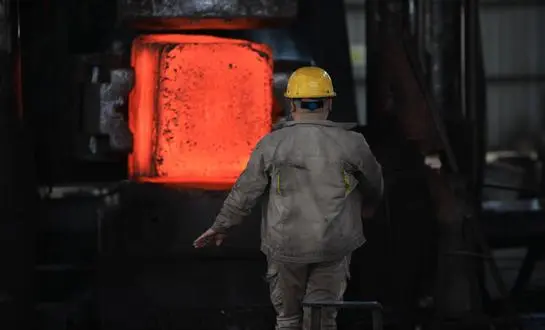
After cutting, the workpiece is heated to a forging temperature sufficient for the work. Exact temperature relies on the grade of material and its deformability.
But the purpose is not only to make the metal softer. The temperature has to be regulated in a proper range so that the material may flow into the die without generating unnecessary flaws or oxidation too much.
Production needs to keep the temperature consistent. If the workpiece is allowed to cool too much before forging is finished, material flow is hindered and the forming loads are higher. Excessive heat might influence the surface quality or the material qualities.
Forming the Part Inside the Die
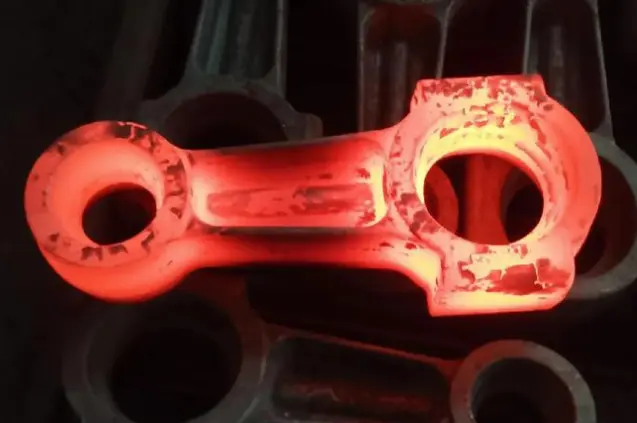
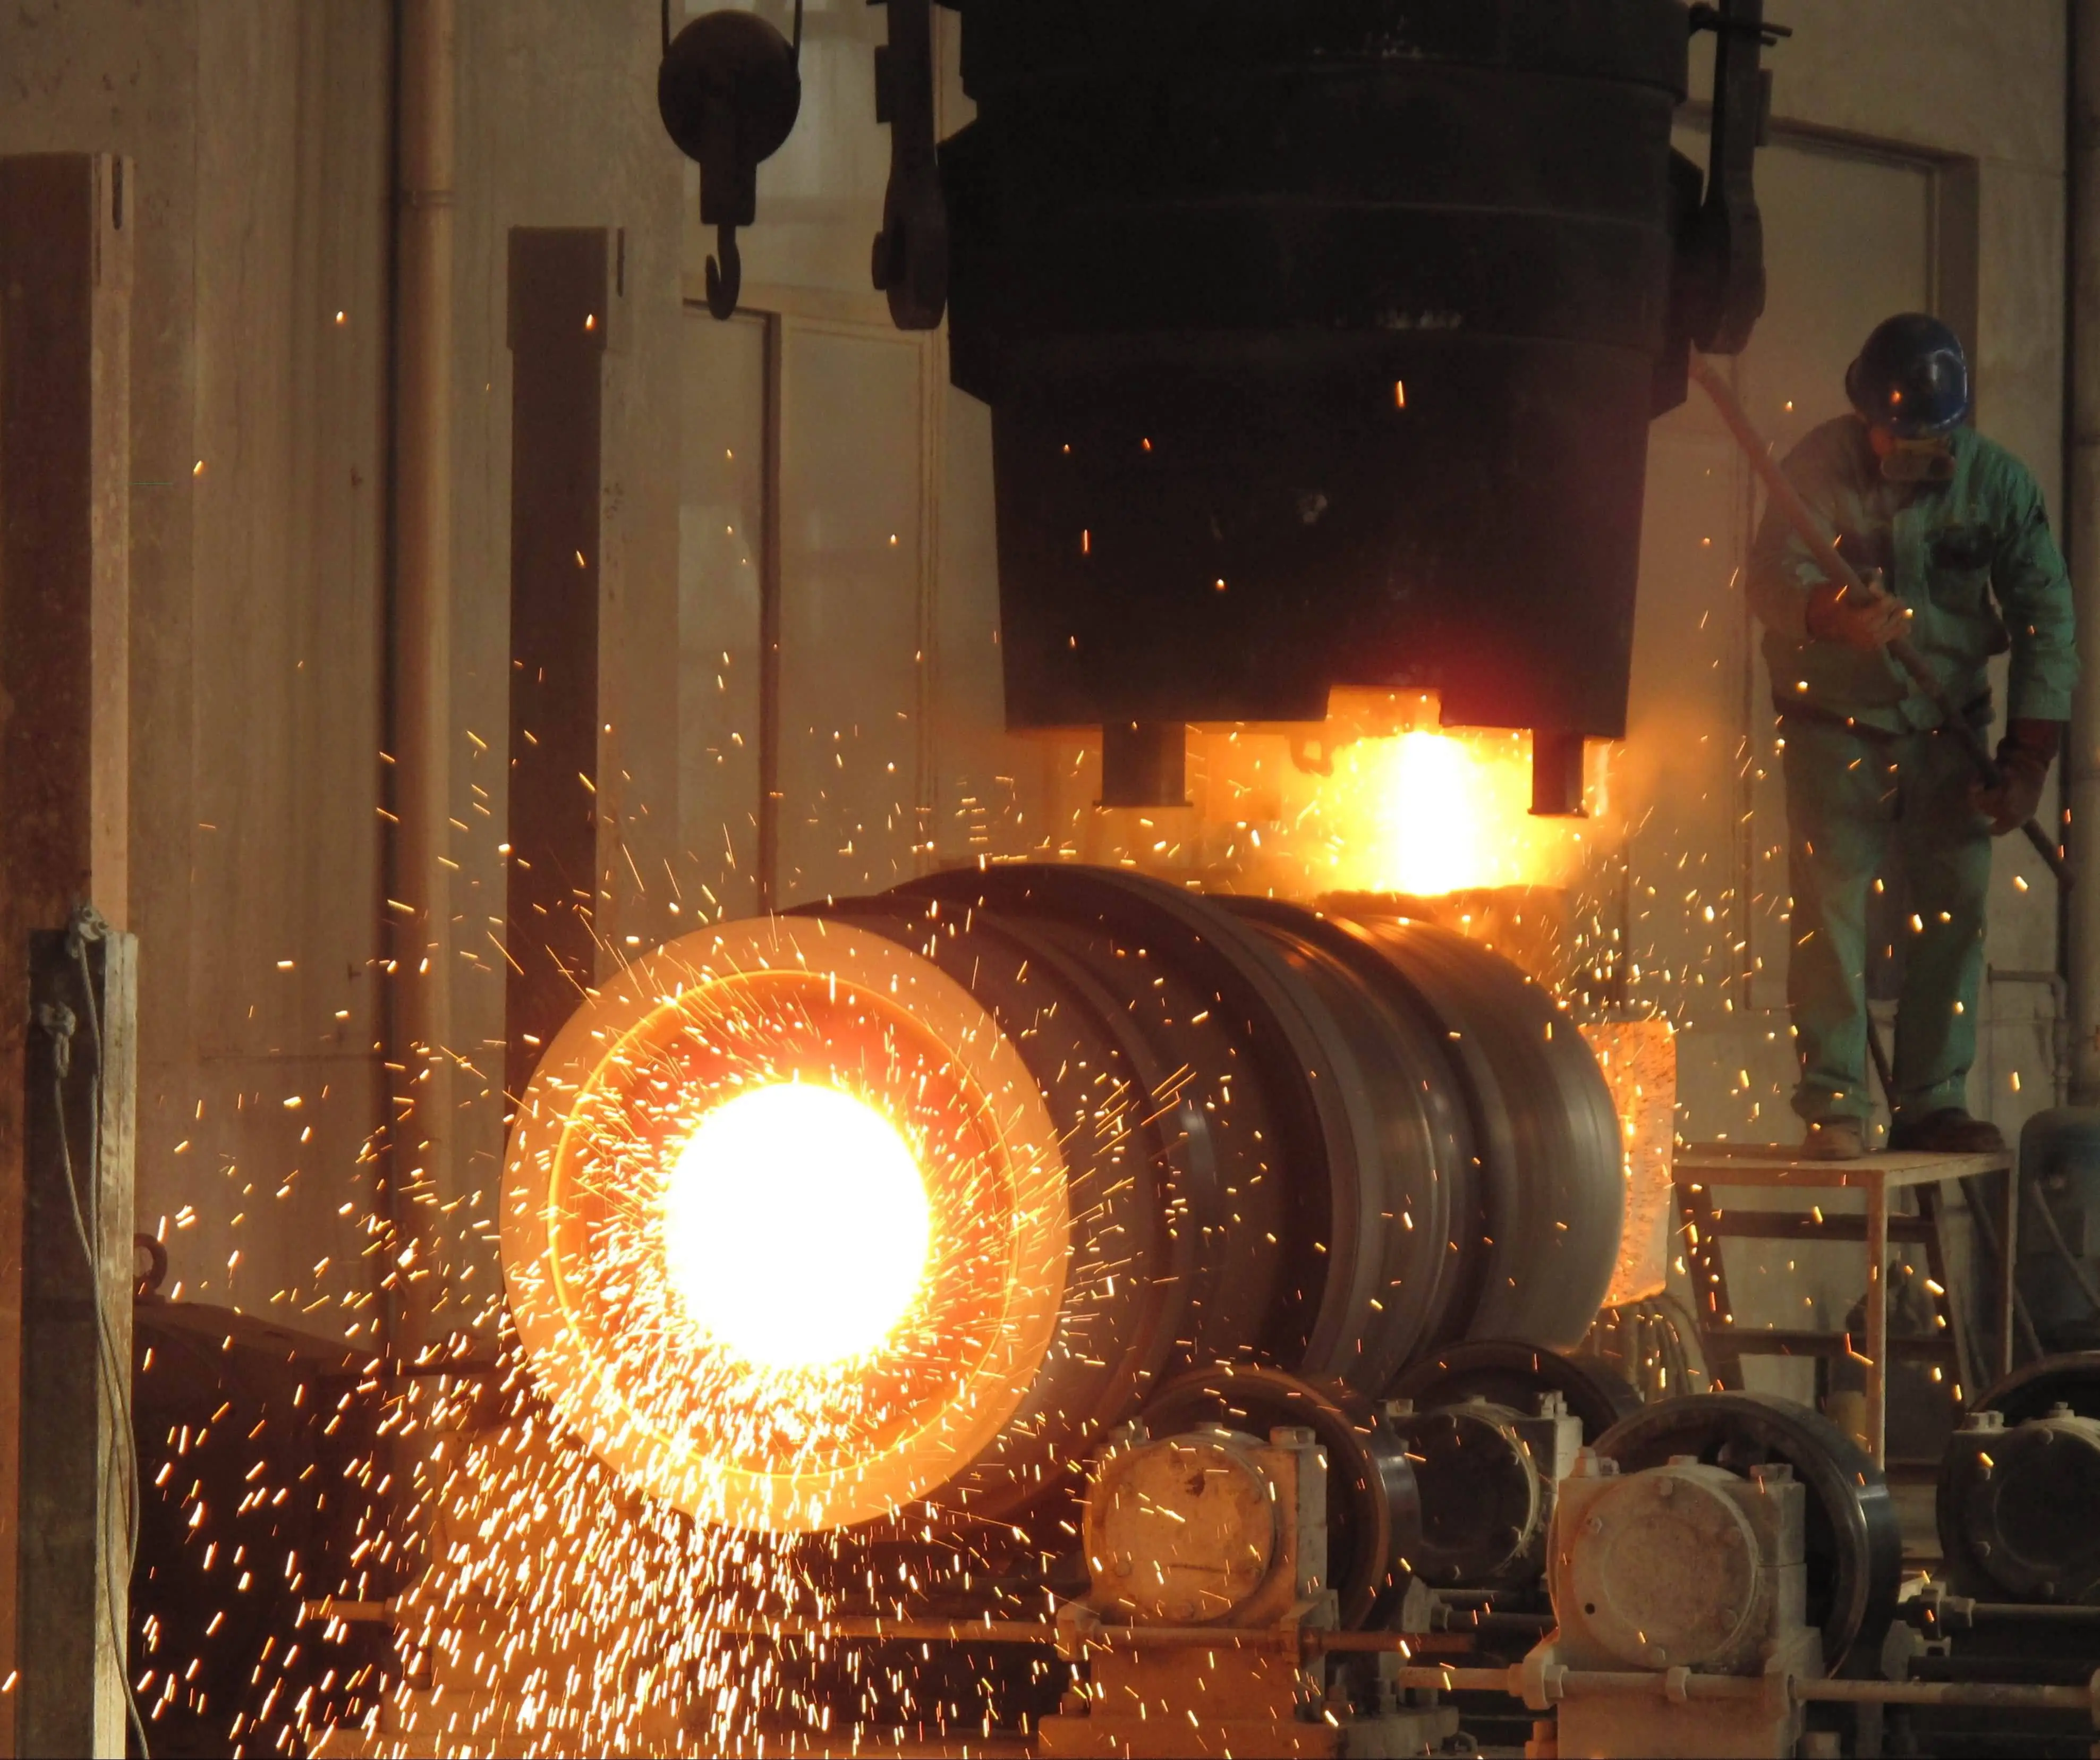
The workpiece to be heated is placed between the forging dies. The upper die is attached to a hammer or ram; the lower die holds the workpiece.
At the moment of the upper die impact on the workpiece, the metal under high compressive force flows and gradually fills the die cavity. Depending on the component design, the shape could be formed in numerous stages instead of a single blow.
Typical sequences may involve preforming, blocking, and finishing. Each stage controls the flow of material, helping the metal to achieve the ultimate shape.
In closed-die forging, surplus material may flow out of the die cavity and form a thin layer known as flash. The flash is usually removed in the next trimming procedure.
Trimming, Heat Treatment, and Finishing
After forging, the item is trimmed to remove the undesired flash. Further processes can be straightening, heat treatment, shot blasting, machining, and surface treatment.
Heat treatment is particularly crucial for the final element if it has special mechanical qualities. The methods indicated may include normalizing, quenching, tempering, or other regulated heat treatments, depending on the material and the application.
Machining can then be employed to obtain tighter dimensional tolerances, to make holes or threads, or to generate useful surfaces that cannot be cost-effectively created during forging.
The quality inspection must be integrated into the entire production process, not only at the conclusion. The final part can be verified to conform to the relevant standards by dimensional inspection, hardness testing, chemical composition verification, and, where applicable, non-destructive testing.
Why Choose Drop Forging for Industrial Components?
Improved Strength and Grain Flow
Drop forging is one of the preferred choices of the engineers due to the ability to manufacture the parts with desirable mechanical qualities.
During deformation, the material flows according to the die geometry. Properly planned forging processes create a grain flow that can follow critical load-bearing areas of the component.
This can give good strength, hardness, and fatigue performance compared with certain other ways of manufacture. Material grade, amount of forging reduction, heat treatment, shape, and process control are still factors in the actual performance.
This can be especially useful for components that will be subjected to repetitive mechanical loads where the proper integrity of the material is important.
Efficient Production for Repeated Components
The higher the manufacturing volume, the more desirable the drop forging. Once the dies have been created and built, the same tooling can be utilized to make a large number of components with the same geometry.
This is one reason the technique is so often considered for OEM production and other applications where recurring orders are expected.
The initial tooling expense is a significant factor, although it can be amortized over the entire production quantity. The economics for thousands or tens of thousands of components can be very different from those of a small production run.
Reduced Material Removal
Machining starts with a larger piece of material, and then material is removed until the desired form is produced. Drop forging, in contrast, brings the material closer to the desired geometry before machining.
This reduces the number of parts required to be machined in the next CNC operation.
However, not every forging should be labeled as a zero-waste process. You still have to take into account billet preparation, flash, trimming, machining allowance, and other process losses for material utilization calculations.
Drop Forging vs. Casting and Machining
When Forging Has an Advantage Over Casting
Casting is a great procedure for making huge parts and complex geometries; however, cast products might contain characteristics such as porosity or shrinkage faults if the process is not managed appropriately.
Forging is the plastic deformation of a solid piece of metal. This can be an advantage for applications in which strength and resistance to mechanical loading are of importance.
This doesn't mean you should use forging instead of casting for all applications. Complex shapes or large shapes that are difficult to forge may be better candidates for casting.
The proper decision depends on the geometry, material, production volume, mechanical requirements, and tolerable manufacturing cost for the component.
When Does Forging Have an Advantage Over CNC Machining?
CNC machining may provide great flexibility and dimensional control—especially with prototypes, small batches, and complex finishing features.
Its disadvantage for high-volume production is that a large quantity of material may have to be machined away from a billet or bar.
Hence, a combination of both processes is a practical way for many industrial components. Forging gives the fundamental structural shape, but CNC machining creates crucial dimensions, holes, threads, sealing surfaces, and other exact details.
This combination can provide a desirable balance between material efficiency, mechanical performance, and dimensional precision.
What Are the Limitations of Drop Forging?
Tooling Investment
The cost of forging dies is one of the first issues engineers should evaluate.
Forging dies must withstand repeated mechanical impact and elevated temperatures. Their design therefore requires appropriate materials, dimensional accuracy, surface quality, and heat treatment.
For very small orders, tooling costs can represent a significant portion of the total manufacturing cost. This is why drop forging is generally more attractive for medium- and high-volume production.
Geometry Restrictions
Not every component can be efficiently produced through closed-die drop forging.
Deep undercuts, extremely thin sections, difficult internal features, and certain complex geometries may require additional operations or a different manufacturing process.
Engineers should consider die opening direction, draft angles, parting lines, material flow, and machining allowances during the design stage.
Early design review can prevent situations where a part appears suitable for forging on paper but becomes unnecessarily expensive to manufacture.
Equipment Capacity
The size and weight of the component must also match the forging equipment.
Available hammer or press capacity places practical limits on the amount of force that can be applied. Very large components may therefore require open-die forging, hydraulic pressing, or another manufacturing method.
This is an important point for procurement teams because a supplier's general forging capability does not necessarily mean that every supplier can manufacture a particular part size.
When Is Drop Forging the Right Choice?
High-Volume Production
Drop forging is often a strong candidate when the same component needs to be manufactured repeatedly.
Higher production volumes allow tooling expenses to be spread across more parts, while dedicated dies can provide repeatable geometry and efficient cycle times.
For automotive, machinery, and industrial OEM applications, this can make forging economically attractive over the complete production lifecycle.
Components Exposed to Mechanical Loads
Components that experience repeated loads, impact, vibration, or mechanical stress can benefit from the material characteristics associated with properly controlled forging.
Typical examples may include:
-
Connecting components
-
Shafts and levers
-
Gears and gear-related components
-
Automotive parts
-
Industrial machinery components
-
Oil and gas equipment components
-
Heavy equipment parts
The suitability of forging should always be evaluated against the actual loading conditions and required material properties rather than assumed from the application alone.
Parts That Can Accept Secondary Machining
Drop forging does not have to produce the final finished dimensions directly.
A forged blank can be intentionally designed with machining allowance. CNC machining can then complete critical surfaces and dimensional features.
This approach is particularly useful when the component requires both strong structural geometry and precise interfaces.
How Should Buyers Evaluate a Drop-Forging Supplier?
Confirm Material and Manufacturing Capabilities
Before placing an order, buyers should confirm that the supplier can work with the required material grade and component dimensions.
Important information may include:
-
Material specification
-
Raw material form
-
Maximum forging size
-
Available hammer or press capacity
-
Heat treatment capability
-
Machining capability
-
Surface finishing options
-
Inspection equipment
A supplier should be able to explain how the selected manufacturing route matches the component requirements.
Review Quality and Inspection Requirements
Quality documentation is another important part of supplier evaluation.
Depending on the application, buyers may request material certificates, chemical composition reports, hardness results, dimensional inspection records, and other quality documentation.
For critical components, additional inspection methods may be required. The appropriate inspection plan should be established before production begins rather than added after manufacturing.
Compare Total Manufacturing Cost
The lowest unit quotation does not necessarily represent the lowest overall cost.
A useful comparison should include tooling, raw material consumption, forging, trimming, heat treatment, machining, inspection, packaging, and transportation.
For high-volume orders, tooling costs may have relatively little impact on the final unit price. For small batches, the opposite can be true.
Buyers should therefore compare suppliers based on total project cost and manufacturing capability rather than looking only at the quoted price per piece.
How Can Engineers Reduce Drop-Forging Costs?
Optimize the Part Design Early
Design decisions made before the production can have a major influence on manufacturing cost.
Engineers should consider whether the geometry allows efficient material flow and straightforward die separation. Unnecessary sharp transitions, difficult undercuts, and excessive machining allowances can increase manufacturing complexity.
A supplier's forging engineer can often identify design changes that simplify production without compromising the intended function of the component.
Balance Forging and Machining
Trying to achieve every final dimension directly through forging is not always economical.
A better strategy can be to forge the major load-bearing geometry while leaving appropriate machining allowance for critical surfaces.
This reduces unnecessary die complexity while still taking advantage of the structural benefits of forging.
Plan for the Full Production Cycle
Tooling life, maintenance, inspection, heat treatment, machining, and replacement requirements should all be considered when estimating long-term production costs.
For a recurring OEM program, these factors can have a greater financial impact than the initial forging quotation.
Conclusion
Drop forging is a practical metal-forming method for producing strong and repeatable components, particularly when production volume, mechanical performance, and material efficiency are important considerations. By applying controlled impact forces to heated metal within engineered dies, the process can create useful grain flow and produce shapes that require less material removal than machining from solid stock.
At the same time, drop forging has limitations. Tooling investment, component geometry, equipment capacity, material selection, and secondary machining must all be considered before choosing the process. For low-volume or highly complex parts, another manufacturing method may be more economical.
For OEMs and industrial buyers, the most effective approach is to evaluate the complete manufacturing route rather than focusing on one process in isolation. A detailed review of the drawing, material grade, annual quantity, tolerances, heat treatment, inspection requirements, and finishing needs can help determine whether drop forging is the right solution.
For customized drop forging components, Shaanxi Welong Int'l Supply Chain Mgt. Co., Ltd. provides integrated forging, casting, and machining services for industrial customers. Founded in 2001, the company operates under ISO 9001:2015 and API-7-1 quality systems and supports customized metal component production for different applications. Its engineering and production capabilities can help customers evaluate manufacturing routes, optimize production processes, manage quality requirements, and coordinate delivery for international projects. Write to info@welongpost.com if you would like more information about the ways in which Welong may assist you with your project.
FAQ
1: What are the main advantages of drop forging?
Drop forging offers enhanced mechanical properties, improved grain structure, and superior strength and durability compared to other manufacturing methods.
2: Is drop forging suitable for small production runs?
Drop forging is generally more cost-effective for large production runs due to high initial tooling costs, but it can be justified for smaller runs if the parts require exceptional strength and durability.
3: What materials can be used in drop forging?
Common materials include carbon steels, alloy steels, and non-ferrous alloys like aluminum and titanium. The choice depends on the specific application and desired properties.
4: How does drop forging compare to casting in terms of part quality?
Drop forged parts typically have superior mechanical properties and a more uniform, solid structure compared to cast parts, which may have internal voids or porosity.
References
1. Smith, J. (2019). "Advanced Drop Forging Techniques in Modern Manufacturing." Journal of Metalworking Technology, 42(3), 215-230.
2. Johnson, R. & Brown, T. (2020). "Comparative Analysis of Drop Forging and Alternative Metal Forming Processes." International Journal of Materials Engineering, 15(2), 78-95.
3. Lee, S. et al. (2018). "Microstructural Evolution in Drop Forged Components: A Comprehensive Study." Materials Science and Engineering: A, 725, 102-114.
4. Garcia, M. (2021). "Cost-Benefit Analysis of Drop Forging in High-Performance Applications." Journal of Manufacturing Economics, 33(4), 412-428.
5. Thompson, K. (2017). "Innovations in Die Design for Complex Drop Forged Parts." Forging Magazine, 28(6), 45-52.
6. Wu, X. & Zhang, Y. (2022). "Sustainability in Drop Forging: Energy Efficiency and Material Optimization." Green Manufacturing and Sustainability, 9(1), 18-33.

Share your inquiry, get the quotation accordingly!
China WELONG- Your Reliable Partner in Metal Solutions