Closed Die Forging vs Open Die Forging: Which Is Right for Your Parts?
Forging remains a proven manufacturing method for producing strong and durable metal components. Among the most widely used approaches, Closed Die Forging and open die forging are applicable for a broad range of part sizes, geometries, manufacturing quantities and cost structures. The choice between them isn’t just a comparison of two methods. Engineers and buyers should additionally consider tooling expenditure, material utilisation, dimensional requirements, machining allowances, production quantity and part design stability. Closed die forging is often ideally suited to the repeated manufacture of components with fixed geometry, while open die forging gives greater flexibility for big and relatively simple components. But the optimal solution is dependent on the whole production demand, not just one feature. Understanding how the two processes differ can help manufacturers choose a forging technique that balances part performance, production efficiency and total cost.
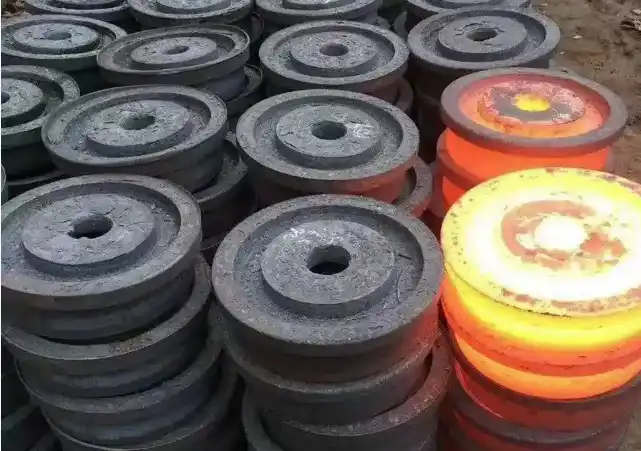
What Are the Main Differences Between Closed-Die and Open-Die Forging?
How does closed-die forging form the part?
The distortion of a heated metal billet is controlled by using shaped dies in closed-die forging. The workpiece is put between dies with the required component profile, and pressure or impact drives the material to flow into the die cavity.
The dies limit the material from various directions, which can yield repeatable exterior shapes with relatively close dimensional control. Depending on the design of the component, some parts can be created very close to their final dimensions, therefore lowering the quantity of material to be removed during machining.
The big trade-off is tooling. Each new component design may require dedicated dies. These dies entail engineering, machining, inspection, maintenance, and replacement costs. Closed die forging is thus becoming more and more attractive when the same or very similar component has to be produced in large quantities.
How Open Die Forging Works?
In open die forging the dies do not contain the workpiece completely. Instead, the material is squeezed between relatively simple tools while the workpiece is adjusted to create the desired dimensions and shape.
The method offers a lot of freedom because the tooling does not have to replicate the full final geometry. Therefore, it is often considered for large parts, limited-volume production, custom forgings, and applications where the design may evolve during development.
The trade-off is that open-die forging often produces less geometric detail and dimensional precision than a tightly controlled closed-die process. If the finished component needs to have tight tolerances or complicated features, it typically needs to be machined further.
How Should Production Volume Influence the Forging Decision?
When Does High Production Volume Favor Closed-Die Forging?
Production volume is one of the best signs that closed-die forging can be appropriate.
Dedicated dies might have high upfront costs. However, if the tooling is produced and authorized, the same die set can be used over and over again to produce vast numbers of similar parts. The tooling cost is consequently divided over a number of parts, lowering the impact on the cost per part.
For example, a manufacturer that is producing thousands of identical automotive or industrial components may find the initial tooling expenditure to be affordable because the process offers reliable production and efficient cycle times.
Closed die forging is especially attractive when part design is stable, large quantities are required, consistency of dimensions is critical, and decreased machining is desirable. It may also be helpful when production scheduling requires dependable output over a long manufacturing program.
Why Open-Die Forging Can Work Better for Smaller Production Runs?
Open die forging can be more appropriate when only a limited number of parts are required.
Tooling costs may be significantly less as the procedure generally does not require a specific die cavity representing the full component. This can be helpful if you are developing a prototype, working on a maintenance project, replacement parts, or another specific industrial job.
Another advantage of open die forging is the ability to change the design simply. If the size of a huge shaft or a heavy component changes during engineering development, it may be more economical to change the procedure than to redesign a complex closed die.
For low-volume applications, the benefits of speedier production with closed die forging may not warrant the hefty tooling cost.
How Do Part Size and Geometry Affect Process Selection?
Where Does Closed-Die Forging Have an Advantage?
Closed die forging works well when a part has a uniform outer shape that must be duplicated throughout a production run.
Possible applications include connecting rods, gear blanks, automotive steering components, industrial levers, chosen flanges, and a range of aerospace or power-generation components.
The die cavity acts as a guide for material flow. The die cavity also assists in determining the outside geometry of the part. This makes the method advantageous for components where repeatability and shape consistency are essential factors.
However, a complicated part does not mean that all the features can be immediately generated by closed-die forging. Special tooling, several forging operations, machining, or a mix of production processes may be required to forge deep recesses, severe undercuts, enclosed cavities, and other complex features.
Therefore, engineers should evaluate the actual part drawing, rather than assume that a difficult shape would always be suitable for closed-die production.
Why Open-Die Forging Suits Large Components?
Open die forging becomes particularly useful as component size increases.
Heavy parts such as large shafts, blocks, rings, discs, and the like are difficult or uneconomical to produce using traditional closed dies. Open die techniques enable producers to successively reduce and shape massive billets or ingots without the aid of a die cavity that duplicates the complete finished component.
Typical applications include huge shafts, pressure vessel components, turbine and power-generating parts, heavy industrial machinery components, giant discs, and special engineering forgings.
In certain applications, the ability to work with vast portions of material may be more significant than attaining a very detailed near-net shape right from the forging procedure.
How Do Accuracy and Machining Requirements Compare?
Dimensional Control in Closed Die Forging
The closed-die forging generally has finer control of the external shape as the dies define the profile of the component. Good die design, temperature control, preparation of the material, and the monitoring of forging force and process are used to achieve uniform dimensions.
This does not imply that the forged part will always be within the final machining tolerance without further processing. Forging allowances are normally incorporated, and crucial surfaces can be machined following forging.
Engineers should consequently distinguish between the dimensional precision of the forging and the final machined tolerance. The tolerance you can achieve relies on the material, the size of the part, the die design, the equipment, the process control, and the inspection requirements.
Where accuracy in final dimensions is required, the forging supplier should set up appropriate machining allowances in the early stages of process design.
Machining Requirements for Open Die Forgings
Open die forgings often need more machining because the technique is based on controlled material flow rather than replicating each final contour.
If it is a large shaft, the forging may be initially made with sufficient machining allowance. The final dimensions can then be fixed by CNC turning, milling, drilling, or other processes.
This adds extra processing but can be inexpensive when the alternative is expensive closed tooling for a small manufacturing run.
So the relevant question is not only what process yields the most accurate raw forging. Manufacturers should review the entire chain from raw material to final component, including machining, inspection, heat treatment, and any other essential activities.
What Difference Do the Processes Make to Mechanical Properties?
Grain Flow and Structural Integrity
One of the main advantages of forging is that it may refine the internal structure of a metal part by controlled plastic deformation.
In forging, some internal voids may close, and the grain structure and grain flow may be affected. The final qualities are dependent on the alloy, starting material, reduction ratio, forging temperature, deformation sequence, heat treatment, and other process parameters.
Closed die forging can provide regulated material flow around the component geometry for various applications that require consistent mechanical performance.
Open die forging also has significant metallurgical advantages. Progressive working can be carried out across large portions to increase material consistency and attain the needed reduction. This is especially useful in large industrial components where internal soundness and structural integrity are of considerable concern.
Neither process should be characterized as stronger across the board. The final mechanical qualities depend on the whole manufacturing method and on the material specification.
Why Material Selection Still Matters?
The inappropriate material cannot be compensated for by the forging procedure.
Before selecting a technique, engineers should consider the alloy composition, the forging temperature range, the tensile qualities required, the yield strength, the toughness requirements, the heat-treatment requirements, the ultimate working circumstances, the corrosion or wear environment, and the inspection needs.
Some alloys are more limited in forging range or need particular processing controls. Material behavior in such instances can be critical in determining the feasibility of closed-die or open-die forging.
Hence, the material quality has to be certified before the forging process is finalized. This allows the supplier to select the proper size of billet, heating settings, sequence of deformation, heat treatment, and inspection plan.
Which Forging Process Is More Cost-Effective?
Understanding the Impact of Tooling Costs
One of the most obvious differences between the two methods is tooling;
Closed-die forging usually demands a higher upfront cost as the dies need to be developed and produced for a particular component. The frequent mechanical and thermal pressure on the dies should also be taken into consideration due to the tool life.
Open die forging usually requires less dedicated tooling. It is thus attractive for large parts and limited production volumes.
But merely comparing the initial tooling price can lead to the inaccurate conclusion.
Calculate the total cost of the finished component.
A more appropriate cost comparison would include raw material, die and tooling expenses, forging cycle time, labor and handling, heat treatment, machining, inspection and testing, scrap, material loss, tool maintenance, packing, and transportation.
Let’s say you have a part that you need to make in thousands of identical copies. Faster manufacturing and less machining per part could recover more of the initial die cost.
Conversely, if a few large components are needed, the cost of pricey specialist tooling might drive up the whole project cost with minimal savings in manufacturing.
Manufacturers should look at cost on a comprehensive project and lifespan basis, not just in terms of comparing tool pricing.
What Should Engineers Check Before Choosing a Forging Method?
Start With the Part Requirements
Before requesting quotations, the engineering team should establish the critical requirements of the component.
At minimum, the specification should identify the material grade, finished dimensions, approximate forging weight, required tolerances, production quantity, annual demand, required mechanical properties, heat-treatment condition, machining allowance, surface requirements, and inspection or testing requirements.
A detailed drawing and material specification allow the forging supplier to assess whether the proposed manufacturing route is technically and economically appropriate.
Clear requirements also reduce the risk of receiving quotations based on different assumptions. For example, two suppliers may propose different processes because they interpret the machining allowance, production volume, or inspection requirements differently.
Consider the Stability of the Design
Design stability is often overlooked when selecting forging tooling.
If the component is still undergoing frequent revisions, investing immediately in a complex closed die may create unnecessary costs. An open die process or another flexible manufacturing route may be more suitable during the development stage.
Once the geometry has been finalized and production volume is established, the economics of closed die forging may become more favorable.
This is especially relevant to new product development. The manufacturing route selected for a prototype does not necessarily need to be the same route used for full-scale production.
Review Supplier and Quality Capabilities
The supplier's capabilities can also influence the practical choice between the two processes.
A capable forging supplier should be able to discuss available forging equipment, maximum forging capacity, die design and manufacturing, material traceability, heat-treatment capabilities, dimensional inspection, mechanical testing, non-destructive testing, machining capabilities, and quality documentation.
For safety-critical or high-value components, these capabilities become particularly important. Buyers should confirm how the supplier controls material identification, process parameters, heat treatment, dimensional inspection, and final documentation.
Which Parts Are Better Suited to Closed Die Forging?
Closed die forging is generally worth considering when the component has a stable design and requires repeatable production.
It can be a practical option when:
-
Production quantities are medium to high.
-
The component has a defined external geometry.
-
Consistent part dimensions are required.
-
The same design will be manufactured for an extended period.
-
Reducing machining requirements is important.
-
The tooling investment can be distributed across a sufficiently large production run.
-
The component requires controlled material flow around its external profile.
Automotive components are a common example because many programs require large numbers of repeatable parts. Similar considerations may apply to industrial machinery, aerospace components, agricultural equipment, and other products manufactured in established production runs.
When Is Open Die Forging the Better Choice?
Open die forging may be preferable when flexibility and component size are more important than producing a detailed shape directly from the forging operation.
It can be a strong candidate when:
-
The component is large or heavy.
-
Production volume is relatively low.
-
The design may change during development.
-
Dedicated closed tooling would be difficult to justify economically.
-
The component has a relatively simple overall geometry.
-
Significant material reduction is required.
-
Large shafts, discs, blocks, or similar heavy sections are involved.
For these applications, the ability to manipulate the workpiece during forging can provide valuable manufacturing flexibility.
How Can You Make the Final Decision?
The most reliable approach is to evaluate the complete manufacturing requirement rather than choosing a process based on a single advantage.
Start with the component drawing and material grade. Then determine the expected annual quantity, required delivery schedule, dimensional tolerances, mechanical properties, machining requirements, and inspection standards.
Next, compare the estimated tooling investment and recurring production costs. For closed die forging, pay particular attention to die development and expected tool life. For open die forging, consider the additional machining and handling that may be required.
Finally, discuss the design with an experienced forging supplier. A supplier can evaluate whether the component geometry is suitable for the available equipment and whether design modifications could improve material flow, reduce machining, simplify tooling, or lower production costs.
In many cases, the most economical solution is not obvious from the forging process alone. A slightly higher forging cost may still produce a lower finished-part cost if it reduces machining time or material consumption. Likewise, a low-tooling-cost process may become less attractive if extensive machining is required afterward.
Conclusion
Ultimately, the relative merits of open-die forging versus closed die forging depend on production volume, component size, geometry, material, tolerance requirements, tooling investment, and the amount of secondary machining required. Closed-die forging is often a strong option for repeatable production of components with defined geometries, particularly when production volume is high enough to justify dedicated tooling. Open die forging, meanwhile, provides greater flexibility for large, heavy, customized, or lower-volume components where specialized closed tooling may not be economical.
The best decision should therefore be based on the complete manufacturing route rather than a single cost or performance factor. By comparing tooling, material utilization, machining, mechanical requirements, production volume, and quality controls at the quotation stage, manufacturers can select a forging process that fits both the technical requirements of the part and the commercial goals of the project.
For manufacturers that need support evaluating different forging routes, Shaanxi Welong Int'l Supply Chain Mgt. Co., Ltd. can provide engineering and sourcing support across both closed-die and open-die forging applications. With more than 20 years of industry experience, Welong can help customers assess material requirements, component geometry, production quantities, machining needs, and quality expectations before selecting a suitable manufacturing approach. This project-based evaluation can help buyers avoid unnecessary tooling investment while establishing a practical route for producing reliable forged components.To learn more around how Welong can back your manufacturing prerequisites, contact them at info@welongpost.com.
FAQ
1: What is the main difference between closed die forging and open die forging?
The main difference is that closed die forging uses two or more dies with pre-cut impressions to shape the metal, while open die forging uses flat or simple contoured dies to shape the metal through repeated blows.
2: Which forging method is better for high-volume production?
Closed die forging is generally better for high-volume production due to its ability to produce near-net shape parts quickly and consistently.
3: Is closed die forging more expensive than open die forging?
Initially, closed die forging can be more expensive due to higher tooling costs, but it often becomes more cost-effective for high-volume production due to reduced material waste and secondary operations.
4: Can open die forging produce parts with tight tolerances?
While open die forging can produce parts with good tolerances, closed die forging typically achieves tighter tolerances and better dimensional accuracy.
References
1. Smith, J. D. (2018). Advanced Forging Techniques: A Comparative Study of Closed and Open Die Processes. Journal of Manufacturing Engineering, 42(3), 156-170.
2. Johnson, R. A., & Thompson, L. K. (2019). Optimizing Forging Processes for High-Volume Production. International Journal of Materials and Manufacturing Processes, 34(2), 89-104.
3. Chen, X., & Zhang, Y. (2020). Material Flow Behavior in Closed Die Forging: A Comprehensive Review. Materials Today: Proceedings, 25, 1234-1245.
4. Brown, E. M., & Davis, S. T. (2017). Cost-Effectiveness Analysis of Forging Methods in Automotive Component Manufacturing. SAE Technical Paper Series, 2017-01-1305.
5. Lee, H. S., & Kim, W. J. (2021). Advances in Net-Shape Forging Technologies for Aerospace Applications. Aerospace Manufacturing and Design, 15(4), 78-92.
6. Wilson, P. R., & Taylor, G. H. (2019). Comparative Study of Grain Flow and Mechanical Properties in Open and Closed Die Forged Components. Materials Science and Engineering: A, 758, 42-55.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

