Understanding Investment Casting Tolerances for Precision Engineering
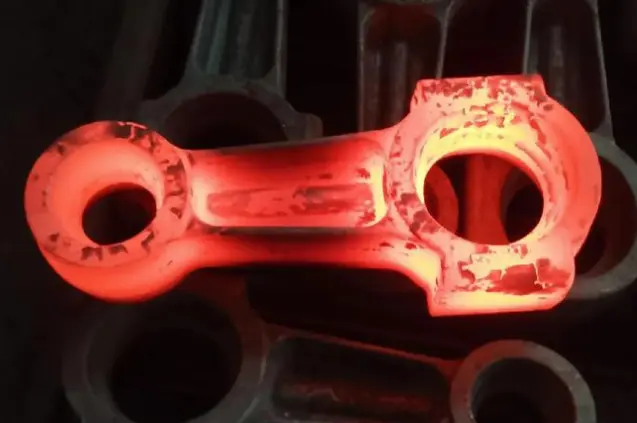
Investment casting,Also known as the lost-wax casting technique, it is widely utilised in creating complicated metal components with great dimensional accuracy, fine surface finishes and reliable repeatability. In precision engineering applications, understanding investment casting tolerances is important, as even slight dimensional changes can affect assembly performance, product reliability and total manufacturing costs.
Selecting the appropriate casting process for industries such as aerospace, energy equipment, automotive systems, medical devices and industrial machines is about more than creating complex forms. Engineers also have to consider if a manufacturing method can regularly meet its dimensional standards. Investment casting has major benefits in this area, as it allows producers to make near-net-shape components while decreasing machining requirements.
However, achievable tolerances are dependent on numerous factors such as wax pattern quality, tooling accuracy, ceramic shell thickness, alloy properties, pouring conditions and inspection procedures. The knowledge about these parameters enables the engineers and buyers to make wise judgements when choosing casting suppliers and creating precision parts.
Why Is Investment Casting Suitable for Precision Engineering Applications?
Exceptional Surface Quality and Complex Geometry Capability
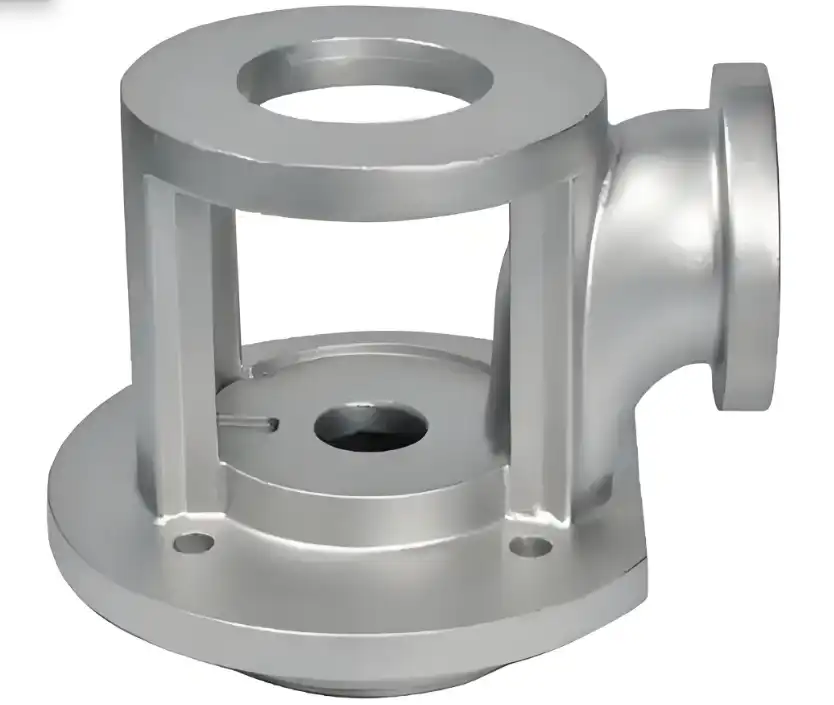
One of the primary reasons manufacturers select investment casting is that the process is capable of creating extremely detailed parts with smooth surface finishes. Investment casting differs from typical sand casting procedures in that it uses a wax pattern to exactly duplicate the shape of the finished part before the ceramic shell is formed.
This procedure allows producers to make the following:
-
Light walls
-
Complex interior passages
-
Small surface details
-
curving complex structures
-
Components with less machining allowance
The ceramic shell offers a robust mold surface that captures precise design elements, leading to better casting uniformity. Surface roughness values of Ra 1.6–6.3 μm can usually be achieved in investment casting, depending on the alloy, shell quality, and production conditions.
An improved surface polish has a number of practical advantages to be gained. It minimizes secondary polishing procedures, enhances fatigue performance in some applications, and helps manufacturers lower their total production cost. For components used in challenging conditions, e.g., turbine parts or industrial valves, the surface quality directly influences the service life and the operational reliability.
Reliable Dimensional Accuracy for Critical Components
Dimensional correctness is one of the most essential considerations in the evaluation of investment casting performance. Manufacturers in precision engineering are not only concerned with the manufacture of a single accurate component but also with the consistency of the component from one production batch to the next.
Typical investment casting tolerances are based on the following:
-
Size of parts
-
Geometry of components
-
Type of alloy
-
Tooling accuracy
-
Amount of output
-
Inspection requirements.
In a controlled manufacturing environment, investment casting may attain dimensional tolerances in the order of ±0.13 mm to ±0.25 mm for many small and medium-sized components. Larger parts or parts with complicated geometries may require further machining or finishing treatments to achieve tighter tolerances.
Generally, professional foundries employ modern tooling technology and inspection systems like coordinate measuring machines (CMM) to check important measurements. This guarantees that components fulfill engineering drawings and customer specifications prior to delivery.
Wide Material Compatibility for Different Engineering Needs
Another benefit of investment casting is that it can treat a wide variety of metals and alloys. They allow engineers to choose materials depending on mechanical strength, resistance to corrosion, temperature performance, and working environment.
Typical materials are
-
Stainless-steel
-
Carbon steel
-
Alloy steel
-
Aluminum Alloys
-
Superalloys based on nickel
-
Cobalt-base alloys
For instance, stainless steel investment castings are commonly chosen for applications that demand corrosion resistance, whereas nickel-based alloys are favored in high-temperature environments like aerospace and energy systems.
This versatility of materials enables engineers to retain the freedom of design and performance requirements. With investment casting, producers can usually produce the original complex geometry with a minimum of alteration, rather than adjusting designs to conform to the restrictions of a production process.
Key Tolerance Standards in Investment Casting
Understanding Linear Dimensional Tolerances
Linear dimensional tolerance is the permissible variance in dimensions such as length, width, height, diameter, or distance between features. To maintain these tolerances in the manufacturing of investment casting, good control of all the manufacturing stages is needed.
The primary sources of dimensional variance are the following:
-
Expansion and contraction of wax
-
Shrinkage of ceramic shell
-
Shrinkage in solidifying metal
-
Cooling rate variation
-
Wear of tools during multiple production cycles
In the design of tooling, skilled manufacturers normally provide for the rate of shrinkage of the material in advance. The dimensions of the wax pattern are modified depending on the expected contraction behavior of the alloy and casting process.
High-volume production is extremely sensitive to consistent tooling performance. Small variations in the wax injection pressure, temperature, or condition of the mold can alter the final dimensions.
CAD simulation and manufacturing analysis tools are routinely used in modern foundries to detect potential dimensional problems before production begins. This strategy cuts down on the trial and error period in development and improves the chances of first-pass manufacturing success.
Geometric Tolerances and Feature Control
Linear measures are about the precision of size, whereas geometric tolerances manage the shape, position, and alignment of certain aspects. These requirements are of interest where cast components have to mate with other mechanical assemblies.
Important geometric tolerances to be considered are:
-
Planarity
-
Roundness
-
Parallelism
-
Perpendicularity
-
Position accuracy
-
Cylindrical form
To maintain geometric precision, you need sturdy tooling, consistent shell buildup, and controlled solidification conditions.
Localized stresses caused by uneven ceramic shell thickness after cooling may result in deformation or warping. Manufacturers are very careful with shell layers, drying conditions, and firing temperatures so as to prevent these problems.
For parts that require tight tolerances, post-casting procedures such as precision machining, heat treating, and surface finishing can be incorporated into the investment casting process to reach final specifications.
Surface Finish Tolerances and Their Impact on Component Performance
Surface polish is another essential consideration in the evaluation of investment casting quality. A part may meet dimensions criteria and fail in service due to surface condition not meeting application requirements.
-
Effect of surface roughness
-
Moving parts' friction
-
Resistance to fatigue
-
Corrosion resistance
-
Sealing efficiency
-
More machining requirements
The ultimate surface quality of an investment casting is a function of several production variables such as the precision of the wax pattern, composition of the ceramic slurry, thickness of the shell, fire conditions, and cleanliness of the molten metal.
A highly regulated ceramic shell results in a smoother mold cavity. That allows the final metal component to reproduce small details more accurately. But the practical purpose of the component should always be taken into account when considering the surface finish requirements.
For instance:
-
Valve parts may need smooth surfaces for sealing.
-
Aerospace parts may need controlled surface conditions for improved fatigue performance.
-
Decorative or customer-facing parts could be more about looks and less about finishing work.
In some circumstances, manufacturers combine investment casting with secondary procedures, such as polishing, grinding, machining, or surface treatment, to meet more stringent criteria.
However, engineers need to clarify dimensional needs and expectations for surface finish early in the project when addressing casting tolerances with a supplier.
Major Factors That Affect Investment Casting Accuracy
Wax Pattern Quality and Tooling Control
The wax pattern provides the basis for the complete investment casting process. Because the ceramic mold is built around the wax pattern, the dimensional mistake of the pattern can be carried directly to the final casting.
Several factors affect the accuracy of the wax pattern:
-
Temperature of Injection
-
Injection pressure
-
Characteristics of wax substance
-
Time to cool
-
Mold design
-
The accuracy of the manufacture of tools
High-quality tooling is required to achieve repeatability in manufacturing. Casting dies with close dimensional specifications are typically made using precision CNC machining and electrical discharge machining (EDM).
Long production runs might slowly degrade mold accuracy. Experienced manufacturers also conduct frequent tooling inspections. Proper maintenance can avoid uneven dimensions of early and later production batches.
For complicated technical components, simulation and trial casting are commonly utilized to evaluate the operation of the tooling before full-scale manufacturing begins.
Ceramic Shell Manufacturing and Firing Process
The ceramic shell directly determines the stability of the mold during metal pouring. A weak or inconsistent shell can lead to defects such as deformation, cracks, dimensional variation, or surface imperfections.
The shell-building process typically includes:
-
Wax pattern assembly
-
Ceramic slurry coating
-
Sand stucco application
-
Drying between layers
-
Repeated coating cycles
-
High-temperature firing
Each layer must be carefully controlled because uneven thickness can affect thermal behavior during casting.
Important control factors include:
-
Slurry viscosity
-
Drying environment
-
Shell thickness
-
Firing temperature
-
Heating and cooling rates
Advanced foundries may use automated dipping equipment and controlled drying rooms to improve consistency. These technologies reduce human variation and help maintain stable casting dimensions across production runs.
Metal Pouring and Solidification Management
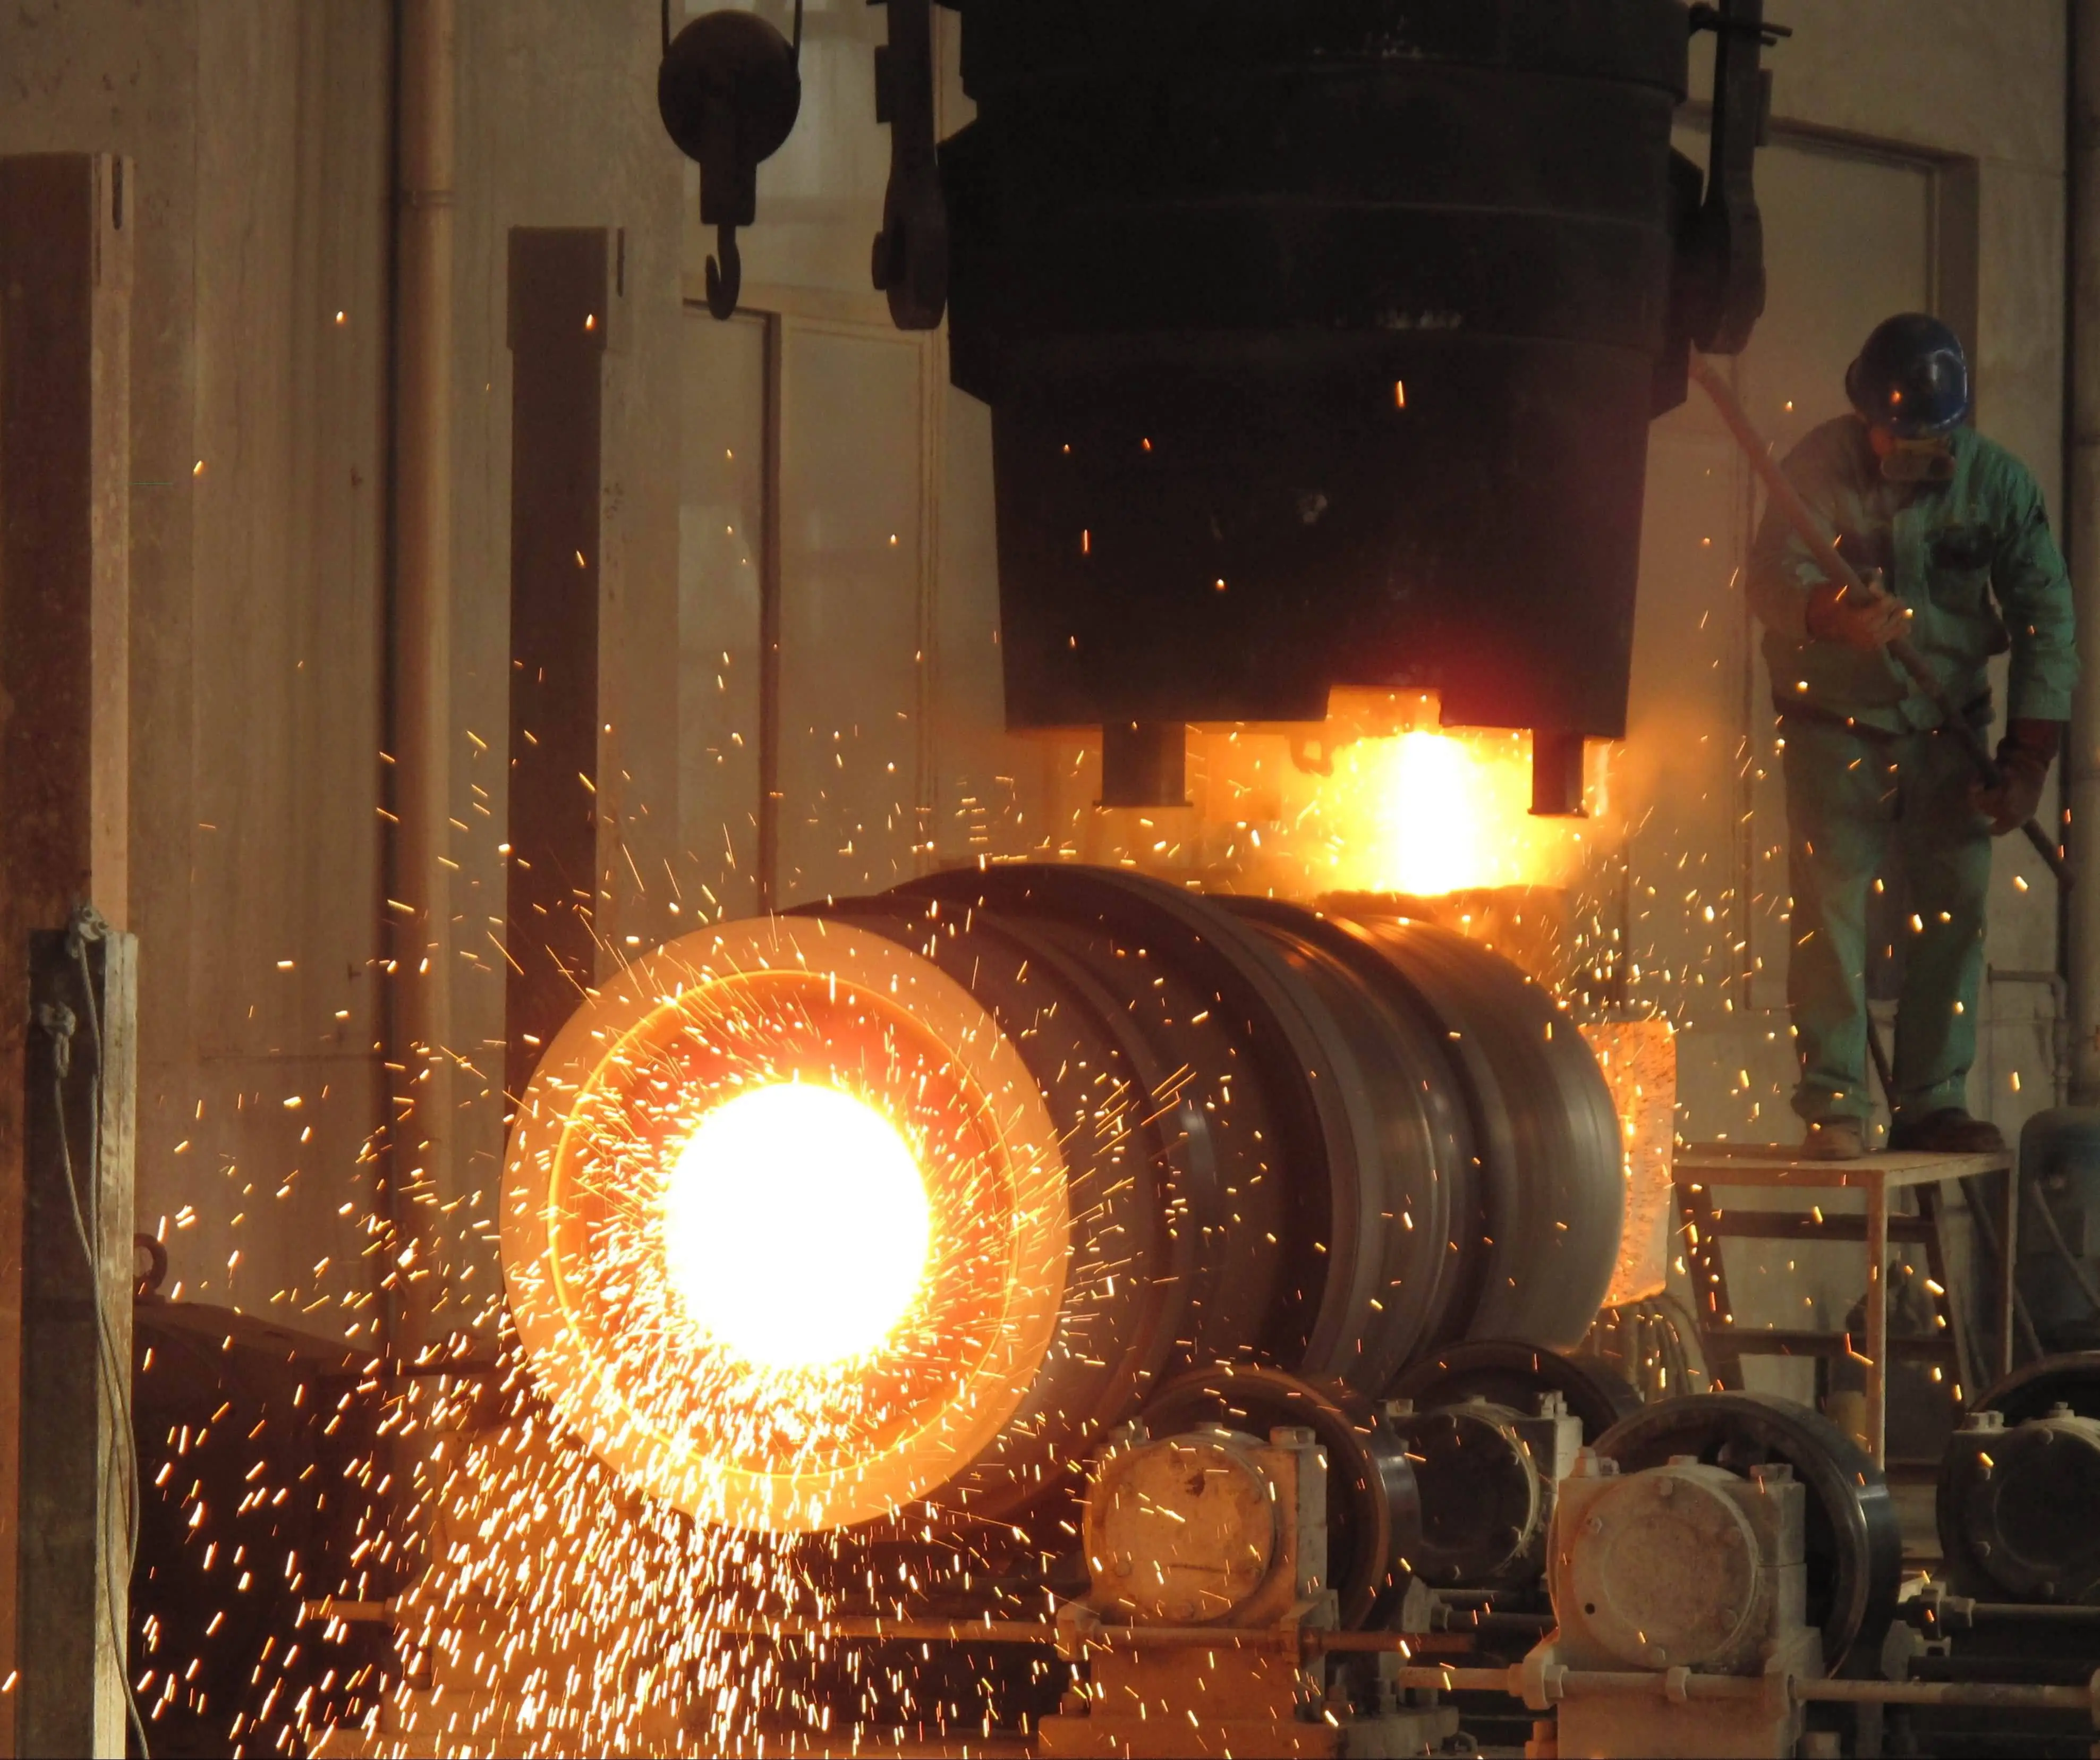
The final stage of investment casting involves pouring molten metal into the ceramic shell and allowing it to solidify. This stage has a direct influence on dimensional stability and internal quality.
Important variables include:
-
Pouring temperature
-
Metal flow speed
-
Mold preheating temperature
-
Alloy composition
-
Cooling conditions
If molten metal does not fill the mold evenly, defects such as incomplete filling, shrinkage cavities, or uneven structures may occur.
To improve casting consistency, manufacturers often use the following:
-
Computer simulation software
-
Optimized gating systems
-
Controlled solidification methods
-
Temperature monitoring systems
Metal simulation technology allows engineers to predict how molten metal flows and cools before actual production. This helps identify possible issues and optimize the design of gates and runners.
For precision components, controlling solidification behavior is especially important because uneven cooling can create internal stress and dimensional distortion.
How do manufacturers verify investment casting tolerances?
Precision Inspection and Quality Control Methods
Achieving accurate dimensions is only part of the manufacturing process. Reliable suppliers must also verify that finished components meet customer specifications through systematic inspection.
Common inspection methods include:
Coordinate Measuring Machine (CMM) Inspection
CMM equipment measures complex component geometries with high accuracy. It is commonly used to verify the following:
-
Critical dimensions
-
Hole positions
-
Surface profiles
-
Alignment requirements
Dimensional Inspection Reports
Professional manufacturers provide inspection documentation to confirm that production parts match engineering drawings and agreed specifications.
Non-Destructive Testing
Depending on application requirements, additional inspection methods may include the following:
-
X-ray inspection
-
Dye penetrant testing
-
Magnetic particle testing
-
Ultrasonic testing
These methods help identify internal or surface defects that may not be visible during normal dimensional measurement.
For industries such as aerospace, energy, and heavy equipment manufacturing, quality verification is often as important as the casting process itself.
How to Choose a Reliable Investment Casting Supplier?
Selecting the right supplier is essential because casting accuracy depends heavily on manufacturing experience and process control capabilities.
When evaluating a supplier, engineers and procurement teams should consider:
Manufacturing Experience
A supplier with extensive experience in investment casting is more likely to understand complex design requirements, material behavior, and tolerance challenges.
Important questions include:
-
How long has the supplier produced investment castings?
-
What industries do they serve?
-
Can they support prototype and mass production?
Engineering Support Capability
A qualified supplier should not only manufacture parts but also provide technical support during the design stage.
Professional suppliers can help customers optimize:
-
Casting design
-
Wall thickness
-
Machining allowance
-
Material selection
-
Production feasibility
Early engineering communication can prevent costly redesigns and improve manufacturing efficiency.
Quality Management System
A reliable investment casting manufacturer should have a structured quality management process covering:
-
Raw material inspection
-
Process monitoring
-
Dimensional verification
-
Final product inspection
-
Documentation control
For global industrial projects, internationally recognized quality systems provide additional confidence when selecting a manufacturing partner.
Conclusion
Understanding investment casting tolerances is essential for engineers and manufacturers who require accurate, reliable, and cost-effective metal components. This manufacturing method provides excellent dimensional consistency, complex geometry capability, and high-quality surface finishes, making it suitable for demanding applications across aerospace, energy, automotive, medical, and industrial sectors.
However, achieving precise results depends on much more than the casting method itself. Factors such as wax pattern accuracy, tooling quality, ceramic shell control, metal pouring conditions, and inspection procedures all influence the final component performance.
Manufacturers that carefully manage these variables can achieve stable production quality while reducing machining requirements and improving overall project efficiency. As simulation technology, automation, and inspection systems continue to develop, investment casting remains a valuable solution for producing precision-engineered components with increasingly demanding specifications.
For companies looking for professional investment casting solutions, Shaanxi Welong Int'l Supply Chain Mgt. Co., Ltd. provides customized manufacturing support for complex metal components. Established in 2001, Welong operates under ISO 9001:2015 and API-7-1 quality management systems and supports customers with a range of manufacturing capabilities, including forging, investment casting, centrifugal casting, and grinding.
With experience serving industrial applications worldwide, Welong focuses on process optimization, strict quality control, and customized production solutions. From material selection and prototype development to final inspection and delivery, the company works closely with customers to ensure that components meet engineering requirements and application expectations.
By combining manufacturing expertise with professional quality management, Welong helps customers develop reliable precision components while improving production efficiency and reducing long-term manufacturing risks.For more information or to discuss your investment casting requirements, contact Welong at info@welongpost.com.
FAQ
1: What are the typical dimensional tolerances achievable with investment casting?
Investment casting can typically achieve tolerances of ±0.13 mm (0.005 inches) for small parts and ±0.25 mm (0.010 inches) for larger components.
2: How does investment casting compare to other manufacturing processes in terms of surface finish?
Investment casting can achieve surface roughness values as low as 1.6 to 3.2 micrometers (Ra), which is superior to many other casting processes and reduces the need for extensive post-casting machining.
3: What materials can be used in investment casting for precision engineering applications?
Investment casting can accommodate a wide range of materials, including stainless steel, aluminum, titanium, and superalloys, making it versatile for various precision engineering applications.
4: How do wax pattern quality and tooling precision affect the final cast part?
The quality of the wax pattern and tooling precision directly impact the dimensional accuracy of the final cast part. Any imperfections in the pattern or tooling will be reflected in the finished product.
References
1. Smith, J. R. (2018). Precision Engineering: Principles and Applications in Investment Casting. Journal of Manufacturing Technology, 45(3), 215-230.
2. Johnson, M. K., & Thompson, L. A. (2019). Advancements in Investment Casting Tolerances for Aerospace Applications. Aerospace Engineering Review, 62(2), 78-95.
3. Chen, X., et al. (2020). Optimizing Investment Casting Processes for Improved Dimensional Accuracy. International Journal of Metalcasting, 14(4), 892-907.
4. Brown, A. D. (2017). Material Selection and Tolerance Control in Investment Casting. Materials Science and Engineering: A, 701, 12-25.
5. Williams, R. S., & Davis, K. L. (2021). Digital Technologies in Investment Casting: Enhancing Precision and Repeatability. Additive Manufacturing, 38, 101807.
6. Lee, H. J., et al. (2019). Surface Finish Optimization in Investment Casting for High-Precision Components. Surface and Coatings Technology, 372, 34-46.

Share your inquiry, get the quotation accordingly!
China WELONG- Your Reliable Partner in Metal Solutions