Open Die vs Close Die Forging: Which Process Fits Your Application
Choosing the right forging process affects more than how a metal component is formed. It can influence tooling investment, production volume, material utilization, dimensional accuracy, machining requirements, lead time, and the final mechanical properties of the part. For manufacturers and OEM engineers, the decision between open die forging and closed die forging should therefore be based on the complete production requirement rather than part shape alone. Open die forging forms heated metal between dies that do not completely enclose the workpiece. The operator or forging equipment controls the deformation through repeated operations such as upsetting, drawing out, and pressing. This makes the process particularly useful for large shafts, blocks, discs, rings, bars, and other customized forgings where flexibility and material integrity are important. Closed die forging, also known as impression die forging, uses shaped dies to control material flow within a die cavity. The process can produce more complicated geometries with greater repeatability and can reduce the amount of machining required after forging. However, the dedicated tooling normally requires a higher initial investment, making the process more attractive when production volumes justify the tooling cost. The right choice depends on several factors, including component size, geometry, annual quantity, material, tolerance requirements, machining allowance, tooling budget, and performance requirements.
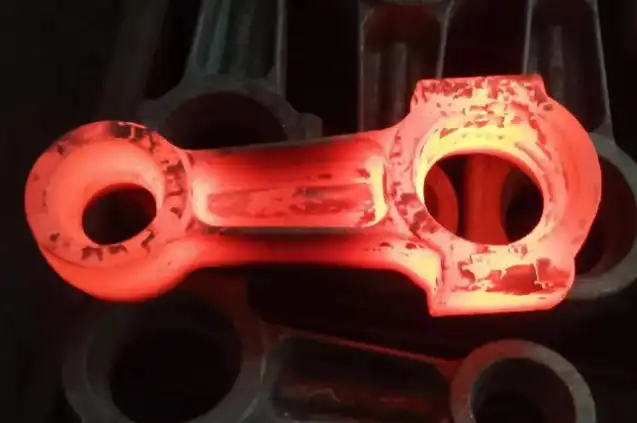
Where Does Open Die Forging Deliver the Most Value?
Large and heavy components
The obvious advantage of open die forging is that it can handle huge and heavy workpieces. The dies do not have to fully encircle the component; therefore, the process is not constrained by a set cavity as in conventional closed die forging.
This makes the method ideal for applications involving large-diameter shafts, turbine components, pressure vessel parts, generator shafts, high-duty discs and other components used in heavy industrial equipment.
For a massive forging, the engineering purpose is generally not to make the final geometry directly from the dies. Instead, forging is utilised to obtain the necessary reduction, grain flow, internal soundness and basic geometry before machining reduces the part to its final dimensions.
Flexible tooling for custom production
Dedicated impression dies are usually more complex than dies used for open die forging. This allows a lot of freedom for making unique parts or components that don't justify pricey tooling.
This can be especially useful for OEM projects when the design may alter during the development phase. The maker can vary the forging sequence and machining allowance, so he does not have to create a highly detailed die cavity for every revision.
This flexibility is also beneficial for replacement parts, prototypes, maintenance components, and specialised industrial equipment with limited manufacturing volumes.
Suitable for low and medium production volumes
One of the most critical variables in forging-process selection is production volume.
The cost of dedicated closed dies might be a large part of the entire manufacturing cost for a modest production run. Open die forging can eliminate some of this tooling outlay and allow the maker to make a bespoke component with more universal tooling.
But it's not necessarily the cheapest option to use open die forging. Its lower tooling cost may be countered by longer forging cycles, increased machining requirements, increased handling or increased inspection for some items. Hence, a valid cost comparison should take into account the whole manufacturing method and not the tooling cost only.
Supports controlled material deformation
The mechanical advantage of forging is not only in the shape of the dies but also in controlled plastic deformation. In open die forging, the workpiece can be modified via a series of reductions and changes in orientation.
Properly engineered deformation can refine the microstructure, close some of the internal discontinuities and generate desirable grain flow. The qualities obtained are a function of the material, beginning stock, the forging temperature, the reduction ratio, deformation sequence, cooling practice and subsequent heat treatment.
For key components, these process variables should be identified and validated as opposed to a blanket statement that all forged products inherently have better qualities.
Open Die vs. Closed Die: The Engineering Differences
Dimensional accuracy and machining allowance
Closed die forging often gives superior as-forged dimensional control since the die cavity directly controls much of the component shape. This is especially advantageous for components with repetitive characteristics and somewhat strict dimensional constraints.
Open die forging provides less direct control of the geometry. The final dimensions are produced by combining forged procedures and subsequent machining. Hence, the engineers designing a component for open-die forging usually have to define the proper machining allowances.
This is not to say that a component forged in an open die will be inaccurate after machining. In many situations the forging gives a good initial shape, and the CNC machining gives the final dimensional correctness.
So the important question is not which procedure is “more precise”, but if the additional tooling for closed die forging is justified by the as-forged tolerance required.
Geometry and design complexity
Closed die forging lends itself well to parts with various integrated elements, like bosses, ribs, recesses and other intricate curves. The die cavity can direct the material flow to these regions and form a reproducible shape.
Open die forging is more appropriate for shapes that can be generated through a sequence of relatively simple deformation stages. Some such examples are:
-
Shafts
-
Bars
-
Discs
-
Blocks
-
Rings
-
Hollow cylinders
-
Large hubs
-
Tapered sections
Complexity should still be looked at in the light of component size. Open die forging is an ideal choice for a big part with relatively simple geometry, but a smaller part with complex repetitive elements is more suited to closed die forging.
Production repeatability
Closed die forging is generally beneficial when you have to make thousands or millions of identical parts. When the tooling and process are validated, the die cavity is a repeatable reference for the material flow and the shape of the parts.
Open die forging can also produce consistent production, but the final geometry is more dependent on the forging sequence, equipment, operator control, tooling arrangement and machining process.
For low-volume industrial components, this difference may not have any commercial impact. However, repeatability can be a large element in the entire manufacturing cost of big-volume automotive or industrial production.
How Material Selection Changes the Forging Decision?
Carbon and alloy steels
Forged parts are most often made from carbon and alloy steels because of their broad spectrum of strength, hardness, wear resistance, and availability.
Open die forging is a frequent process for big steel parts when the final product has severe mechanical-property or internal-quality criteria. Depending on the grade, the forging procedure may be followed by normalising, quenching and tempering, annealing or other heat treatment processes.
The material grade can influence the production route through its hot working range, deformation behaviour, heat treatment reaction and needed mechanical qualities, and so the material grade should be decided before the forging process is selected.
Stainless steels and corrosion-resistant alloys
Stainless steels can also be forged by open or closed die forging. The correct path is determined by the alloy, the dimensions of the part, the geometry, the volume of production and the required dimensional and surface criteria.
Open die forging can give the flexibility to manage the general shape of big stainless steel components but then allow later machining to the finished specifications.
Costs for raw materials can be significant, which means that nickel-based alloys and other high-value elements require very strict process control. In these situations, engineers should be thinking about not only tooling costs but also material yield, machining allowance, heating cycles and scrap risk.
Material properties are process-dependent.
It is important to keep in mind that the same material will not necessarily give the same qualities regardless of the forging method used.
Mechanical performance could be affected by:
-
Degree of deformation
-
Forging temperature
-
Reduction ratio
-
Deformation direction
-
Cooling rate
-
Heat treatment
-
Starting material condition
-
Grain flow
-
Final machining and inspection
For essential applications the forging specification should specify the requisite mechanical qualities and related inspection criteria and should not rely merely on the name of the forging method.
A Practical Framework for Choosing the Right Forging Process
Choose open die forging when flexibility is the priority.
Open die forging is generally worth considering when several of the following conditions apply:
-
The component is large or heavy.
-
The production quantity is relatively low.
-
The geometry is simple to moderately complex.
-
Dedicated tooling would be difficult to justify economically.
-
The design may change during development.
-
Substantial machining will be performed after forging.
-
The application requires controlled material deformation and reliable internal quality.
-
The component is customised rather than mass-produced.
Typical applications include large shafts, power-generation components, pressure equipment parts, heavy industrial machinery, and custom replacement components.
Choose closed die forging when repeatability is critical.
Closed die forging becomes more attractive when:
-
Production volumes are medium to high.
-
The component geometry is relatively complex.
-
Consistent as-forged dimensions are important.
-
Reduced machining is commercially valuable.
-
The same component will be produced repeatedly.
-
The tooling investment can be distributed across a sufficiently large production quantity.
For these applications, the higher initial die cost can be offset by improved production efficiency, repeatability, and reduced machining requirements.
Do not select the process based on size alone.
Part size is an important consideration, but it should not be the only selection criterion.
A large component may still require a different forging route depending on its geometry, material, production quantity, equipment availability, and specification. Similarly, a smaller component does not automatically require closed die forging rather than open die forging.
A better approach is to evaluate the complete manufacturing chain:
Material → billet size → forging method → deformation sequence → heat treatment → machining → inspection → final delivery
This approach gives engineers a more realistic view of cost and technical risk.
What OEM Buyers Should Confirm With a Forging Supplier?
Ask for process and material information
Before placing an order, buyers should provide the supplier with as much technical information as possible. A typical RFQ package may include:
-
Material grade
-
Forging drawing
-
Finished dimensions
-
Estimated annual quantity
-
Required mechanical properties
-
Heat-treatment requirements
-
Applicable forging standard
-
Machining allowance
-
Surface requirements
-
Non-destructive testing requirements
-
Inspection documentation
-
Delivery requirements
The supplier can then determine whether open die forging, closed die forging, or another manufacturing route is appropriate.
Verify inspection and quality-control capability.
For critical forgings, purchasing decisions should not be based on price and production capacity alone. The supplier should be able to explain how it controls the forging process and verifies the finished product.
Depending on the application, inspection may include dimensional inspection, chemical composition verification, mechanical testing, hardness testing, ultrasonic testing, magnetic particle testing, or other non-destructive examination methods.
The exact inspection plan should follow the applicable material specification, customer drawing, industry standard, and application requirements.
Consider the complete manufacturing route.
A supplier offering forging alone may not always provide the most efficient solution. For many OEM projects, it can be advantageous to work with a manufacturer capable of coordinating forging, heat treatment, machining, inspection, and documentation.
This reduces the number of interfaces between suppliers and can simplify quality management and delivery coordination.
How Welong Can Support Custom Forging Projects?
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. provides customised metal manufacturing services covering forging, casting, and machining. Established in 2001, the company serves industrial customers requiring customised components and coordinated manufacturing support.
Welong works with materials including carbon steel, alloy steel, stainless steel, aluminium, and other engineering alloys. Its capabilities can support projects where the customer needs more than a basic forged blank, including process coordination, machining, inspection, and delivery management.
For an OEM or industrial project, the most useful starting point is the actual component requirement rather than choosing a forging process from a catalogue. Providing the material grade, drawing, dimensions, expected quantity, mechanical requirements, and inspection specifications allows the manufacturing team to evaluate the most suitable production route.
With ISO 9001:2015 and API-7-1 certifications, Welong can also support customers that require documented quality management and industry-specific manufacturing processes.
Conclusion
The choice between open die and closed die forging ultimately depends on the relationship between component geometry, size, production volume, material, dimensional requirements, tooling investment, and downstream machining.
Open die forging is often the stronger choice for large, heavy, customised, or lower-volume components where flexible tooling and controlled material deformation are more important than achieving complex near-net geometry directly from the die. It is commonly considered for shafts, discs, rings, blocks, and other large industrial forgings.
Closed die forging is generally more suitable for repeat production of smaller or moderately sized components with complex geometries, tighter as-forged dimensions, and production volumes high enough to justify dedicated tooling.
For OEM projects, the best decision should come from evaluating the complete manufacturing route rather than comparing the two processes on a single factor. When you provide the material grade, drawing, dimensions, production quantity, tolerance requirements, and inspection specifications, a qualified forging supplier can assess the appropriate process and determine the most practical balance between performance, tooling cost, machining, and delivery. For inquiries, please contact us atmetal@welongpost.com.
FAQ
1. When is open die forging preferred over closed die forging?
Open die forging is preferred for large, custom parts, low-volume production runs, and when working with materials that require significant grain refinement and improved mechanical properties.
2. What are the key advantages of open die forging?
The main advantages of open die forging include flexibility in part size and shape, cost-effectiveness for low volume production, and improved material properties through comprehensive deformation.
3. How does open die forging affect material properties?
Open die forging enhances material properties by refining grain structure, improving directional strength, increasing ductility and toughness, and eliminating internal defects and porosity.
4. What materials are suitable for open die forging?
Open die forging is compatible with a wide range of materials, including carbon and alloy steels, stainless steels, nickel-based alloys, aluminum alloys, and copper alloys.
References
1. Smith, J. (2019). Advances in Open Die Forging Techniques. Journal of Materials Processing Technology, 45(2), 112-125.
2. Johnson, A., & Brown, B. (2020). Comparative Analysis of Open and Closed Die Forging Processes. International Journal of Metalworking, 33(4), 78-92.
3. Thompson, R. (2018). Material Property Enhancement through Open Die Forging. Materials Science and Engineering: A, 712, 215-228.
4. Lee, S., & Park, K. (2021). Cost-Effectiveness of Open Die Forging in Low Volume Production. Journal of Manufacturing Processes, 62, 45-57.
5. Wilson, D. (2017). Open Die Forging: Applications in Aerospace and Energy Sectors. Advanced Materials and Processes, 175(3), 28-35.
6. Garcia, M., & Taylor, L. (2022). Precision and Tolerance Control in Open Die Forging Operations. Journal of Materials Engineering and Performance, 31(8), 6172-6185.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

