Continuous casting is a common metal manufacturing technology which has revolutionised the way molten metal is transformed into semi-finished products. Molten metal solidifies constantly, and the partially solidified result is pulled from the casting machine, eliminating the need to pour individual ingots and then do significant warming, cropping and forming processes. Depending on the application, the product can be a slab, billet, bloom, or other continuous portion for further processing. Continuous casting is more than just the speed of manufacturing. A well-designed casting process allows for better control of solidification, more consistent dimensions, lower material losses and a more direct route from liquid metal to a form ready for rolling, forging, machining or other subsequent processes. At the same time, the process calls for careful control of temperature, metal flow, mould cooling, withdrawal speed and secondary cooling. These technical considerations are crucial for manufacturers considering a new casting line or sourcing a provider for continuous casting equipment and components. The suitable setup depends on the production capacity and also on the alloy chemistry, the product geometry, the quality criteria and the intended downstream process.
How Does the Continuous Casting Process Work?
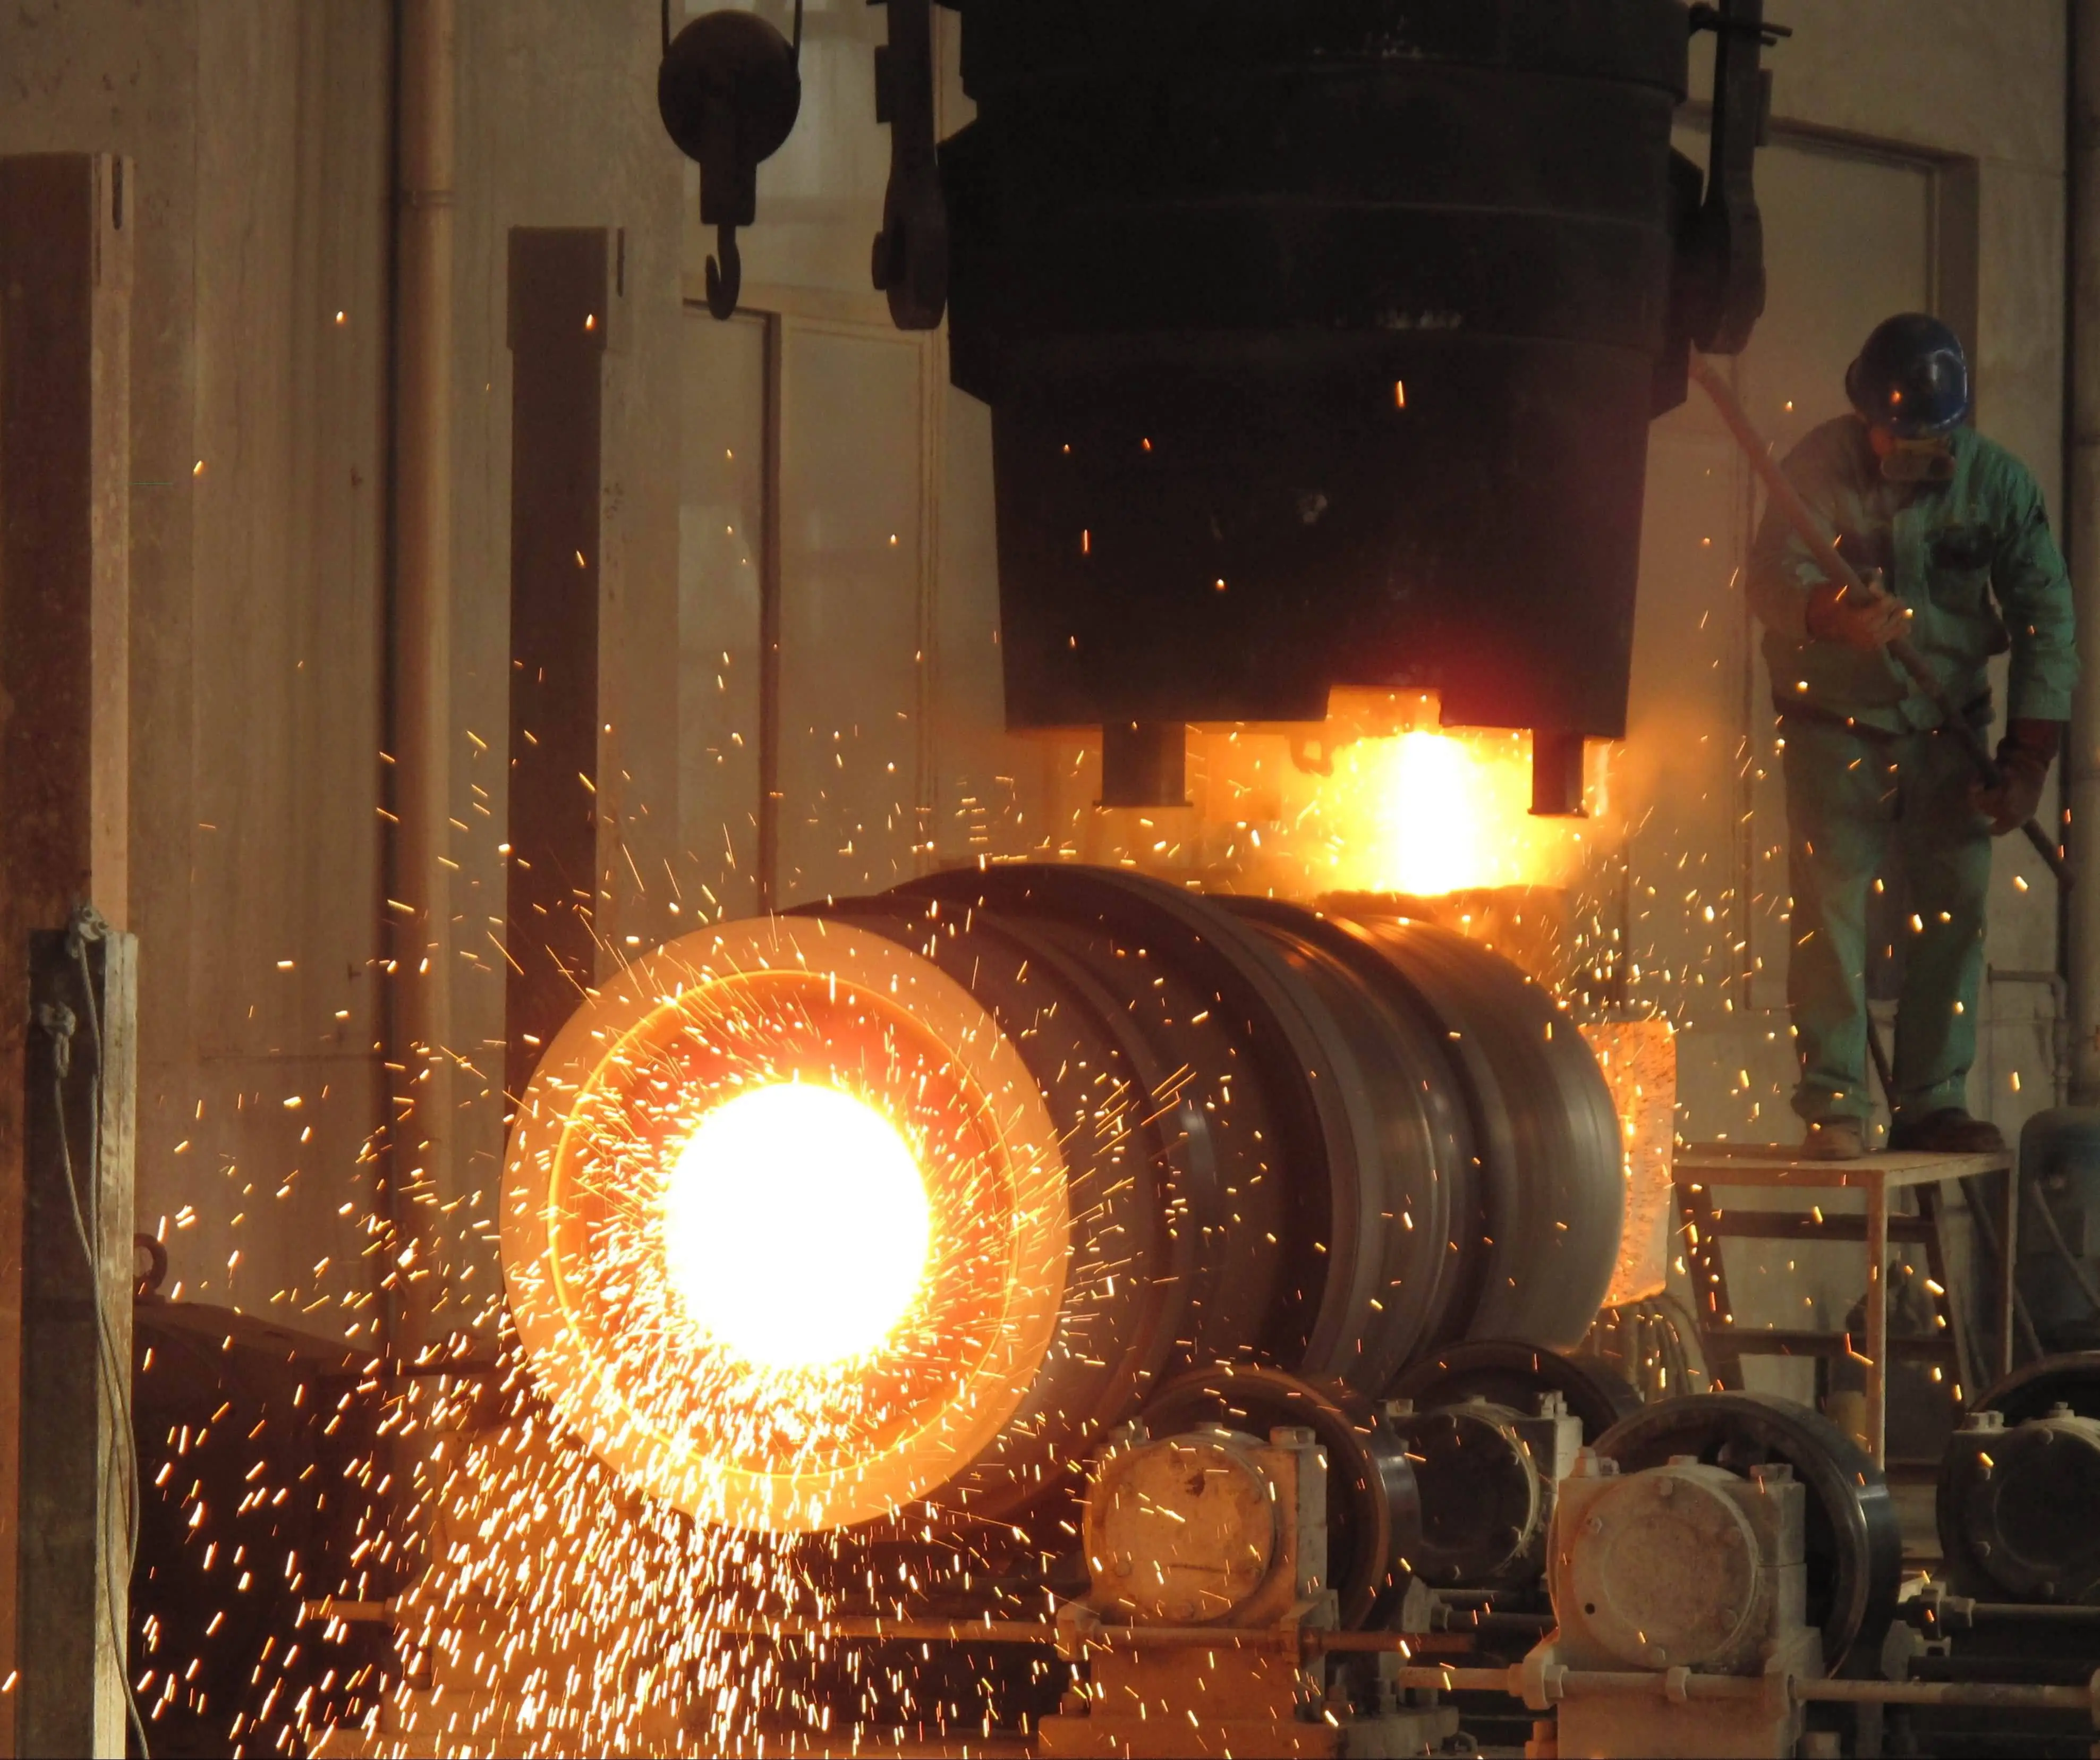
The premise is straightforward, yet success depends on careful management at every step. Molten metal is supplied from a furnace or holding system to a tundish, an intermediate vessel between the molten-metal supply and the mould. The tundish serves to control the flow of metal and gives a more even feed to the casting mould.
From Molten Metal to a Solidified Shell
As the molten metal flows into the water-cooled mould, heat is quickly drawn out of it through the mould walls. The strand forms a solid shell around its still-liquid core. The strand is then pulled out of the mould at a constant speed, and supplementary cooling devices take away further heat.
The procedure has to be a compromise between casting speed and correct solidification. If the alloy and section size selected are too rapid for withdrawal, the solid shell may not form sufficiently. Uncontrolled cooling conditions can cause the thermal stresses, which lead to surface or interior flaws.
Therefore, mould design and cooling-system performance are the key elements of the choice of the continuous casting equipment.
The Role of the Tundish and Mould
The tundish does not just pass on molten metal. Depending on the system design, it can aid in stabilising the flow, controlling the delivery of metal to the mould and enabling the removal or management of inclusions.
The initial geometry of the cast strand is determined by the mould. Because copper has a high thermal conductivity, water-cooled copper moulds are widely used for casting steel. The surface quality and shell formation are affected by mould dimensions, taper, cooling conditions, oscillation characteristics and lubrication.
The importance of the correlation between these factors is that a problem observed downstream may have originated in an upstream process parameter. Effective quality control must thus take into account the complete casting system, not a single machine component in isolation.
Major Continuous Casting Machine Configurations
Suitable machine configuration is the product geometry, metal type, necessary production volume and downstream manufacturing route. A system for flat slabs will have different needs than one for producing billets or blooms.
Slab Casting for Flat Products
Slab casters are often employed when the cast result is to be further processed into flat goods. The size of the slab is determined by the specifications of the rolling mill and the range of the finished product.
A slab casting line has to provide stable mould conditions, controlled secondary cooling and reliable strand extraction. The effect of the combination of casting speed, slab thickness and heat extraction is very relevant, as the interior quality may be influenced by the differences in solidification.
Buyers of projects supplying feedstock for demanding rolling operations should assess not only the nominal output capacity but also the ability of the machine to maintain consistent casting conditions during long production runs.
Billet and Bloom Casting
Billet casters are often utilised for smaller cross sections that can be rolled into items such as bars, wire rod and other lengthy products. Bloom casters are bigger and can produce material for structural items, rails, hefty sections and other uses.
Section size affects cooling requirements, solidification behaviour, withdrawal rate and where internal faults may be found. Hence, a casting machine has to be chosen according to the real product range and not only the overall production capacity.
Speciality Casting Configurations
More specialised casting arrangements are needed for some applications. These may include curved or vertical machines, systems utilising electromagnetic stirring and combinations based on individual alloy or product needs.
After examining the alloy, cross-section, estimated production rate, and needed downstream process and metallurgical quality, the correct configuration should be established. The machine with the highest nominal output is not always the technically correct one.
Process Parameters That Control Casting Quality
The quality of a continuously cast product is controlled by various interacting process variables. Casting systems are usually optimised as an integrated process, since the change of one parameter might effect others.
Casting Temperature and Superheat
The temperature of molten metal should be adjusted to an acceptable range for the specified alloy and casting system. Too high temperature might alter solidification behaviour and raise the thermal load of the equipment, while too low temperature can affect flow and increase the chance of premature solidification.
The target temperature should be chosen according to the alloy composition, machine design, section size and operating conditions, not a single universal value.
Withdrawal Speed
The withdrawal rate influences the period for shell development and solidification. Alloys and machine designs have quite different correct speeds.
The higher casting speeds increase the output of a given production unit but may also alter the temperature conditions inside the strand. A sound manufacturing plan is thus a compromise between throughput and the requisite internal and surface quality.
Secondary Cooling
After the strand leaves the mould, further cooling mechanisms are used to remove heat. The effects of water flow, spray pattern, cooling-zone design and temperature distribution on solidification are investigated.
Uneven cooling can induce temperature gradients and strains that can cause surface cracking and other quality concerns. Therefore, maintenance and process management are critical factors for consistent nozzle performance and accurate water-flow control.
Electromagnetic Stirring and Soft Reduction
Electromagnetic stirring can be applied to control the flow of the molten metal and to improve the solidification behaviour of advanced casting lines. In the appropriate processes, dynamic soft reduction can be applied to regulate the last phases of solidification and to diminish some internal quality problems.
These technologies are not a cure-all for every casting line. The value varies on the metal grade, product geometry, machine design and necessary quality.
Continuous Casting Compared With Ingot-Based Production
The fundamental advantage of continuous casting is that it provides a more direct route from molten metal to a semi-finished product. This means that traditional manufacture of ingots involves separate moulds, stripping of ingots, reheating and other procedures before the material can be moved on to the next stage of production.
Material Yield and Production Flow
Continuous casting produces a strand directly and so can reduce some of the material losses involved with the standard ingot process. The actual yield enhancement depends on the metal grade, product dimensions, cropping needs, process design and downstream processes.
Small gains in yield can have a large impact on material costs in high-volume production. This is one of the reasons why continuous casting has become an important method of production in the steel and other metal sectors.
Process Consistency
The steady state process under control allows for reliable operating conditions in protracted manufacturing runs. Automated temperature monitoring, mould level control, cooling management and strand monitoring let operators detect abnormalities before they become significant quality problems.
However, defect-free is not guaranteed in continuous casting. Poor process control can still create surface cracks, internal porosity, inclusions, segregation and dimensional variation. Hence, the design of the equipment and the operational process must go hand in hand.
Energy and Downstream Processing
Continuous casting can eliminate some of the warming and handling phases compared to traditional ingot techniques. The total energy advantage is a function of the whole manufacturing chain comprising furnace operation, casting, reheating, rolling and finishing.
So, the energy performance should be assessed on a full-process basis, not as one single % as a universal baseline.
How to Select a Continuous Casting Equipment Supplier?
Selecting a provider is not simply a matter of comparing equipment costs. A casting system is a long-term production asset, and the supplier’s technical capability, manufacturing quality, commissioning assistance and after-sales service can directly impact the operating performance.
Review Technical Capability
A qualified supplier should be able to discuss the project in terms of real metallurgical and production needs. The important technical information could cover alloy grades, product dimensions, projected throughput, casting speed, cooling requirements, automation level and downstream processing.
If suppliers propose a typical design without investigating these elements immediately, they are not responding to the true needs of the project.
Evaluate Manufacturing and Quality Control
Manufacturing should be capable, with proper inspection and quality-control procedures. Depending on the equipment or component being delivered, purchasers may require dimensional inspection, material paperwork, welding records, non-destructive testing, machining records or other quality documents.
Documentation should be an afterthought for important applications, and procurement teams should develop inspection needs prior to the start of production.
Consider Engineering and Communication Support
In continuous casting projects we commonly find technical drawings, samples, equipment interfaces, and customised components. By using technical drawings and communicating effectively with the buyer, the supplier can limit the chances of misinterpretation throughout production.
This is especially the case for multinational projects when the technical specifications, quality standards and paperwork requirements may differ between the buyer and the supplier.
Common Continuous Casting Defects and Their Causes
Defect control is one of the most important parts of continuous casting. A reliable process requires operators and engineers to connect observed defects with the conditions that created them.
Surface Cracking
Surface cracks can be associated with factors such as thermal stresses, mould conditions, cooling patterns, steel or alloy composition, and withdrawal conditions. Mould oscillation and lubrication must also be properly controlled because the strand is still relatively weak when it leaves the mould.
A useful troubleshooting process should examine temperature records, mould behaviour, cooling performance, and casting speed instead of assuming that every crack has the same cause.
Internal Porosity and Shrinkage
Internal defects can develop when gases, shrinkage, or inadequate feeding conditions are not properly controlled during solidification. The exact mechanism varies by metal and casting process.
Process monitoring, appropriate molten-metal treatment, and suitable solidification control can help reduce these problems. For demanding applications, internal quality may also need to be verified through ultrasonic or other appropriate inspection methods.
Segregation and Inclusion-Related Problems
Chemical segregation occurs because alloying elements do not always distribute uniformly during solidification. Inclusions can also affect the cleanliness and downstream performance of the cast product.
Process conditions, molten-metal cleanliness, electromagnetic stirring, cooling strategy, and final solidification behaviour can all influence these issues. Quality management should therefore cover both molten-metal preparation and casting operations.
Building an Effective Quality Control Program
A continuous casting operation benefits from combining real-time process monitoring with finished-product inspection.
Important operating data may include molten-metal temperature, mould level, casting speed, cooling-water conditions, and other machine-specific parameters. Tracking these values over time helps identify abnormal trends and supports more consistent operation.
Finished-product inspection should be selected according to the application. Depending on product type and customer requirements, dimensional inspection, chemical analysis, mechanical testing, surface inspection, ultrasonic testing, or metallographic evaluation may be appropriate.
The objective is not simply to collect more data. The quality system should connect process data with measurable product requirements so that engineers can identify the source of variation and make informed adjustments.
Procurement Considerations for a New Casting Project
Before requesting quotations, buyers should prepare a clear technical specification. At minimum, the supplier should understand the material or alloy, target product geometry, production capacity, operating environment, quality requirements, applicable standards, and expected delivery schedule.
For customised projects, drawings and samples can be particularly useful. They allow the supplier to evaluate dimensions, interfaces, machining requirements, material specifications, and inspection points before manufacturing begins.
Cost should also be evaluated over the complete operating life of the system. Purchase price is only one part of the total cost. Energy consumption, maintenance, replacement components, consumables, operator training, downtime, and technical support can all influence the actual economics of the project.
A supplier offering a lower initial price may not provide the best long-term value if the equipment requires frequent maintenance or lacks adequate technical support.
Why Engineering Support Matters in Continuous Casting?
The technical complexity of continuous casting makes engineering support an important part of supplier selection. Equipment must operate within the physical and metallurgical limitations of the material being processed.
Welong states that its engineering team works with AutoCAD, Pro-Engineering, and SolidWorks and can accept customer drawings and samples for customised manufacturing. This capability can be useful when a project involves non-standard dimensions or components that must interface with an existing production system.
For international buyers, engineering communication also provides an opportunity to clarify material specifications, tolerances, inspection requirements, packaging, and delivery expectations before production starts.
Conclusion
Continuous casting technology provides a highly efficient route for converting molten metal into semi-finished products while reducing the number of processing stages required in many traditional production routes. Its advantages can include improved material utilisation, consistent product geometry, controlled solidification, and reduced downstream processing requirements.
At the same time, the performance of a continuous casting system depends heavily on process control. Casting temperature, withdrawal speed, mould conditions, secondary cooling, molten-metal cleanliness, and solidification behaviour must work together to achieve the required product quality. Equipment selection should therefore be based on the complete production requirement rather than on capacity or purchase price alone.
For procurement teams, supplier capability is equally important. Engineering support, manufacturing quality, inspection procedures, documentation, communication, and after-sales service all contribute to the long-term value of a casting project. With appropriate technical planning and supplier evaluation, continuous casting can provide a reliable foundation for modern metal manufacturing and support demanding production requirements across multiple industrial sectors.
FAQ
1. What metals can be processed through continuous casting technology?
Continuous casting is widely used for steel, stainless steel, aluminium, copper, and other metal alloys. However, each material requires its own casting parameters because melting temperature, thermal conductivity, solidification behaviour, alloy chemistry, and product geometry can differ considerably. Equipment should therefore be selected according to the specific material rather than assuming one configuration is suitable for every metal.
2. What is the main advantage of continuous casting?
The main advantage is the ability to convert molten metal directly into a continuously produced semi-finished section. This can reduce intermediate processing, improve material utilisation, provide more consistent product dimensions, and support higher production efficiency compared with some conventional ingot-based routes.
3. What factors determine continuous casting quality?
Important factors include molten-metal temperature, alloy composition, mould design, mould cooling, casting speed, secondary cooling, lubrication, mould oscillation, electromagnetic stirring where applicable, and the control of molten-metal cleanliness. Quality also depends on how consistently these parameters are monitored and controlled during production.
Can continuous casting equipment be customised?
Yes. The appropriate level of customisation depends on the product, alloy, production target, existing equipment, and required automation. Customised engineering may involve mould dimensions, cooling systems, withdrawal arrangements, monitoring systems, equipment interfaces, or other production-specific components. Providing technical drawings, product samples, and detailed specifications for continuous casting can help a supplier evaluate the requirements more accurately. Contact us at info@welongpost.com to discuss your specific requirements and discover how our innovative manufacturing capabilities can enhance your operational efficiency.
References
1. Brimacombe, J.K. "The Challenge of Quality in Continuous Casting Processes." Metallurgical Transactions B, Volume 30, Issue 4, 1999.
2. Thomas, B.G. "Continuous Casting of Steel: Principles and Practice." Steelmaking Conference Proceedings, Iron and Steel Society, 2001.
3. Wolf, M.M. "Continuous Casting Technology: Current Status and Future Developments." Journal of Materials Processing Technology, Volume 155, 2004.
4. Cramb, A.W. "The Making, Shaping and Treating of Steel: Continuous Casting." Association of Iron and Steel Technology, 11th Edition, 2003.
5. Irving, W.R. "Continuous Casting of Non-Ferrous Metals and Alloys." Chapman and Hall Materials Engineering Series, 1993.
6. Zhang, L. "Advanced Continuous Casting Technologies for High-Quality Steel Production." International Conference on Clean Steel, 2007.