How to optimize forging parameters for strength?
Forged metal components are widely used when a part must withstand repeated loading, impact, pressure, or demanding operating conditions. However, simply selecting a strong alloy does not guarantee a strong finished component. The result also depends on how the material is heated, deformed, cooled, and heat treated. For this reason, parameter control is one of the most important parts of a reliable forging process The primary parameters include material selection, forging temperature, amount of deformation, strain rate, die design, lubrication, cooling conditions and post forging heat treatment. These variables are highly correlated. However, changing one parameter without addressing the other parameters may lead to new difficulties such as grain coarsening, incomplete die filling, excessive forging load, surface cracking, or unwanted residual stress. Thus a practical approach would be to optimise the whole manufacturing route rather than a single figure. The aim is to obtain the required mix of strength, toughness, fatigue resistance, dimensional precision and service life with defect risk and production cost under control.
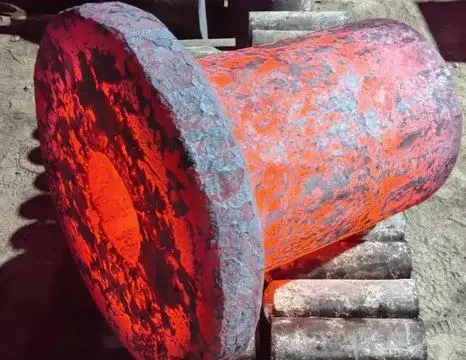
Which forging parameters have the greatest effect on strength?
Start with the right material and forging grade.
The first step is to pick the material. Different alloys react differently to deformation and heat treatment. Each type of steel, such as carbon steels, alloy steels, stainless steels, aluminium alloys, titanium alloys and nickel-based alloys, has its own forging temperature ranges and deformation characteristics.
For a part that is subject to large static loads, tensile and yield strength may be important design criteria. For items subjected to impact or cyclic loads, toughness and fatigue performance may be equally significant. Even an extremely hard material will not necessarily be the first choice for an application requiring resistance to shock or repeated stress.
The original state of the material is important as well. The chemical composition, initial microstructure, grain size and previous heat treatment can influence the behaviour of the material during forging.
Consequently, the supplier and client should agree on the required material grade, mechanical qualities, applicable specification and heat-treatment condition before manufacturing. This is a technical foundation for the rest of the forging process.
Establish a suitable forging temperature window.
Temperature is one of the most important parameters in hot and warm forging. The temperature range relies on the alloy and the manner of desired deformation.
The material is generally plastic enough to deform at a reasonable forging force at an adequate temperature. The material may also experience microstructural changes such as dynamic recovery or dynamic recrystallisation depending on its composition and processing circumstances.
But a higher temperature does not indicate better forging outcomes. Overheating or holding may produce grain growth, oxidation, decarburisation or other surface and microstructural defects. Forging below the correct processing range, in contrast, can increase flow stress and forging load and may increase the tendency to crack.
Therefore, temperature should be monitored during the production cycle and not only when the billet enters the furnace. For essential components, monitoring billet temperature, die temperature, transfer time and temperature decrease between forging processes can achieve significantly better process control.”
Control deformation and reduction ratio
Another important metric is the amount of deformation. Proper forging deformation is helpful to close internal voids, to refine microstructure and to establish favourable grain flow.
But the purpose is not only to maximise the deformation. Poorly designed sequences might result in excessive deformation, higher forging loads and local flaws. Also, insufficient deformation may not give the necessary interior structure.
The reduction ratio and deformation distribution should thus be examined in relation to the original billet size and the shape of the final component. In order for the deformation to reach the interior, rather than remain on the surface, it may be necessary to forge large parts several times.
When designing crucial forgings, the location of the maximum strains, as well as the amount of deformation dispersed along the cross-section, should be taken into account.
Optimise strain rate instead of maximising it.
Strain rate is a measure of how fast the material is deforming. The effect relies heavily on material, temperature, degree of deformation and forging equipment.
Many metals have increased flow stress with increased strain rate. This means that the equipment may have to supply increased forging force. Some alloys also exhibit varied behaviour to changes of strain rate and temperature.
Therefore, the optimal design goal is rarely the quickest achievable forging speed. The best target is to find a strain-rate window that gives stable material flow, acceptable forging loads, adequate die filling and the ideal microstructure.
Press forging, hammer forging and other equipment may give different deformation histories, even at equal nominal reductions. Therefore, the forging process design should contain the specified equipment and its operating parameters.
How can die design improve the strength of forged parts?
Design the die for controlled metal flow.
Die geometry controls material flow during deformation. A well-built die will provide controlled material flow and minimise undue stress concentrations.
Important design features are:
-
angled tapered
-
fillet radii,
-
parting line position,
-
flash design,
-
cavity shape,
-
transition areas,
-
machining allowances
Sharp edges cause local stress concentrations and hinder the flow of the material. Properly constructed fillets enhance flow and reduce the likelihood of localised problems.
The separating line also requires attention. Its position governs dispersion of the material, filling of the die, flash production and the final grain-flow pattern.
For complex parts it is better to use a multi-stage forging process instead of trying to force the whole shape in one operation. The intermediate preform can better distribute the material and limit the amount of uncontrolled deformation in the final die.
Consider grain flow when designing the component.
One of the key advantages of forging is the ability to create directional grain flow along the basic contour of the component.
This is especially helpful for components subject to cyclic mechanical loading. The correct design of the forging route allows to match the grain flow with the main load routes of the part.
Therefore, the design of the die should not be judged only on the basis of whether the cavity can be filled. In addition, the engineers should examine the effect of the deformation sequence on the interior structure.
A part may meet dimensional criteria but nevertheless have an inefficient forging route. Information about the suitability of the manufacturing process for the desired service conditions can be provided by the final grain flow and deformation history.
Select die materials and surface conditions carefully.
Process consistency influences performance. Repeated high temperatures and mechanical loads require that dies have appropriate strength, dimensional stability and wear resistance.
A used die gradually modifies cavity dimensions and flow of material. This can cause dimensional variance between batches of manufacturing and can also increase the amount of machining necessary following forging.
Another aspect is surface polish. Excessive die-workpiece friction may impede material flow and may increase forging load. Proper surface preparation and lubrication can help maintain a consistent material flow.
Monitoring die wear is equally critical as monitoring forging temperature, especially in high-volume manufacturing, as both can affect repeatability.
How should lubrication and cooling be controlled?
Use lubrication to manage friction and die temperature.
Lubrication has two primary functions in many forging operations: controlling friction and helping manage heat transfer between the workpiece and die.
The appropriate lubricant depends on the forging temperature, material, die design, equipment, and production method. Applying too little lubricant may increase friction and make die filling more difficult. Excessive or inconsistent application can also create process problems.
The objective is not to use the maximum amount of lubricant but to establish a repeatable application method.
For production components, operators should control factors in the forging process such as application coverage, timing, concentration where applicable, and die surface condition. Consistency is particularly important because changes in lubrication can alter metal flow and forging load.
Manage cooling after deformation.
Cooling begins as soon as the hot forged component leaves the deformation stage. The cooling rate can influence the final microstructure and the stresses within the component.
Cooling conditions should therefore be selected according to the alloy and subsequent heat-treatment requirements. Uncontrolled cooling can produce undesirable hardness differences between thick and thin sections or contribute to residual stresses and distortion.
Large forgings require particular attention because their surfaces may cool considerably faster than their cores. This difference can affect microstructural uniformity and dimensional stability.
Instead of treating cooling as a separate step after forging, manufacturers should include it in the overall process design.
What post-forging treatments increase mechanical performance?
Use heat treatment to achieve the required property balance.
Heat treatment is often essential for achieving the final mechanical properties of a forged component. The appropriate route depends on the alloy and required specification.
For suitable steels, quenching and tempering can be used to obtain a controlled combination of strength and toughness. Normalising may be used to refine or homogenise the microstructure in certain applications. Annealing can reduce hardness and improve machinability when required.
For precipitation-hardening alloys, the appropriate solution treatment, quenching, ageing, or related treatment sequence may be more relevant.
The important point is that heat treatment should be designed together with the forging route. The forging operation establishes the material's deformation history, while heat treatment modifies the resulting microstructure and mechanical properties.
Temperature, holding time, furnace uniformity, transfer time, and cooling rate should all be controlled according to the applicable material specification and process requirements.
Apply surface treatments when the service condition requires them.
Some forged components require more than high bulk strength. Parts exposed to contact fatigue, wear, or cyclic surface loading may benefit from an appropriate surface treatment.
Processes such as shot peening can introduce beneficial compressive residual stresses at the surface. Nitriding or carburising can be used for suitable alloys and applications where a hard, wear-resistant surface combined with a tougher core is required.
These treatments should not be treated as universal solutions. Their suitability depends on material composition, geometry, service conditions, and the required mechanical properties.
The objective is to match the surface condition to the actual failure modes expected during service.
How can manufacturers verify that forging parameters are optimised?
Combine process monitoring with mechanical testing
Parameter optimisation should be supported by measurable results. A production route should not be considered optimised simply because the parts look acceptable or meet dimensional requirements.
Depending on the component and specification, quality control may include:
-
chemical composition verification
-
dimensional inspection
-
hardness testing
-
tensile testing
-
impact testing where required
-
metallographic examination
-
ultrasonic testing
-
magnetic particle or other surface inspection methods
-
heat-treatment records
-
traceability documentation
Mechanical testing helps determine whether the finished material meets the specified property requirements. Metallographic examination can provide information about grain structure and other microstructural characteristics.
For critical forgings, non-destructive testing can also help identify internal or surface discontinuities that cannot be detected through visual inspection alone.
Use simulation and process data where appropriate.
Computer-aided process simulation can be useful when designing complex forgings. Depending on the software and project requirements, simulation may help engineers evaluate material flow, die filling, forging load, temperature distribution, and potential defect areas before physical production.
Simulation does not replace practical testing, but it can reduce trial-and-error during die and process development.
Production data can also be used to identify trends. If forging temperature gradually changes, die wear increases, or forging load moves outside the established process window, the manufacturer can investigate the cause before the issue becomes a major quality problem.
A stable process is generally easier to control than one that depends heavily on operator judgement.
A practical workflow for optimising the forging process
A systematic workflow can make parameter optimisation more effective.
First, define the application requirements. Identify the required strength, toughness, fatigue performance, hardness, dimensions, and applicable material standard.
Second, select a suitable material and confirm its forging characteristics. The material should not be chosen only according to its nominal strength.
Third, determine the appropriate heating and forging temperature range. Consider both the starting temperature and the temperature loss during transfer and deformation.
Fourth, establish the deformation sequence. Determine how the billet will be performed, upset, drawn, or shaped before the final die operation.
Fifth, select an appropriate strain-rate range and forging equipment. The objective is stable deformation rather than simply maximum speed.
Sixth, optimise die geometry, lubrication, and cooling conditions. These factors directly influence material flow, forging load, die life, and dimensional consistency.
Seventh, select the required post-forging heat treatment and define the applicable forging process controls.
Finally, verify the finished components through dimensional inspection, mechanical testing, NDT, and metallographic evaluation where required.
This approach makes it easier to identify the relationship between process parameters and final properties. If a component fails a strength requirement, for example, engineers can investigate material condition, deformation history, heat treatment, and inspection data rather than changing one parameter blindly.
What should buyers ask a forging supplier?
When sourcing forged components, buyers should look beyond the supplier's ability to provide a forged shape. A capable supplier should be able to explain how the manufacturing route supports the component's mechanical requirements.
Useful questions include:
What forging method is recommended for the component?
The supplier should be able to explain whether open-die, closed-die, ring forging, press forging, hammer forging, or another route is appropriate.
How is the forging temperature controlled?
Ask whether the supplier has defined temperature windows and how billet, die, and process temperatures are monitored.
How is material flow evaluated?
For critical components, buyers can ask how the supplier controls deformation and grain flow and whether process simulation is used during development.
What heat treatment is included?
The supplier should identify the proposed heat-treatment route and explain how the final mechanical properties will be verified.
What inspection documents are available?
Depending on the project, customers may require material certificates, dimensional reports, hardness results, mechanical test reports, NDT records, and other quality documentation.
How are production batches controlled?
Traceability is especially important for components used in demanding applications. The supplier should have a clear system for connecting raw material, forging operations, heat treatment, inspection, and final shipment.
Why process control matters for forged components?
Strength is not created by one forging parameter. It is the result of the interaction between material composition, heating, deformation, die design, cooling, heat treatment, and inspection.
For example, a high-strength alloy may not deliver the expected performance if it is forged outside its appropriate temperature range. Similarly, an excellent die design cannot compensate for unsuitable material or inadequate heat treatment.
This is why experienced manufacturers treat forging as a controlled manufacturing system rather than a single forming operation. The process should be developed around the actual service requirements of the finished component.
For OEMs and industrial buyers, this approach also reduces uncertainty. A documented and repeatable manufacturing route makes it easier to maintain consistent properties from one production batch to the next.
Conclusion
Optimising forging parameters for strength requires more than increasing forging temperature, deformation, or production speed. The best results come from balancing material selection, forging temperature, deformation amount, strain rate, die geometry, lubrication, cooling, and post-forging heat treatment.
A well-designed forging process should promote appropriate material flow, support a favourable microstructure, minimise defect risk, and achieve the mechanical properties required by the final application. Process monitoring, mechanical testing, non-destructive testing, and metallographic evaluation can then be used to verify that the selected parameters are producing consistent results.
For buyers, the most important consideration is not simply whether a supplier can produce a forged component. The supplier should be able to explain the manufacturing route, control critical parameters, provide appropriate inspection records, and adjust the process according to the component's material, geometry, and service requirements.
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd., established in 2001, provides customised metal component solutions covering forging, casting, and machining. With ISO 9001:2015 and API-7-1 certifications as stated by the company, its manufacturing and supply-chain services can support projects that require coordinated material sourcing, process development, quality control, and delivery management. For customised forgings, working with a supplier that can connect design requirements with manufacturing and inspection is an important step toward achieving consistent component performance. Contact us at metal@welongpost.com to discover how we can contribute to your project's success.
FAQ
1: What is the most important factor in optimizing forging parameters for strength?
While all factors are important, material selection is often considered the most crucial, as it sets the foundation for the forging process and final component properties.
2: How does forging temperature affect the strength of the final product?
Forging temperature influences material flow, microstructure development, and grain refinement, which directly impact the final strength of the forged component.
3: Can die design really make a significant difference in forged part strength?
Yes, proper die design ensures uniform material flow, minimizes defects, and promotes optimal grain structure, all of which contribute to improved strength.
4: What are the benefits of post-forging heat treatments?
Heat treatments can significantly enhance strength, hardness, and other mechanical properties by altering the material's microstructure.
References
1. Smith, J. R., & Johnson, K. L. (2018). Advanced Forging Techniques for High-Strength Components. Journal of Materials Processing Technology, 256, 112-125.
2. Zhang, Y., & Chen, X. (2019). Optimization of Forging Parameters for Improved Mechanical Properties. International Journal of Advanced Manufacturing Technology, 100(5-8), 1523-1537.
3. Brown, A. B., & Davis, C. D. (2020). Effect of Die Design on Forged Part Strength and Microstructure. Materials Science and Engineering: A, 772, 138705.
4. Wilson, E. F., & Taylor, G. H. (2017). Post-Forging Heat Treatments for Enhanced Strength in Aerospace Components. Heat Treatment and Surface Engineering, 2(3), 178-190.
5. Lee, S. M., & Park, J. K. (2021). Influence of Strain Rate on Microstructure and Mechanical Properties of Forged Alloys. Materials Characterization, 173, 110948.
6. Anderson, R. T., & Thompson, L. S. (2016). Surface Treatments for Improved Fatigue Strength in Forged Parts. Surface and Coatings Technology, 307, 462-475.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

