How to Inspect Quality in Closed Die Forged Parts?
When forged components are used in demanding industries such as oil and gas, aerospace, automotive, heavy machinery, and power generation, quality inspection becomes a critical step before the parts enter service. Even a small internal crack, dimensional deviation, or material inconsistency can affect the performance, safety, and service life of a forged component. Closed die forging is called a precision manufacturing technique as it can manufacture components which have a high strength, a fine grain structure and great dimensional accuracy. But these benefits are not only due to the forging process, but also to thorough inspection and quality control measures during production. Through a trusted inspection procedure, forged parts are checked for a number of attributes including internal integrity, surface condition, dimensional accuracy, chemical composition and mechanical qualities. To guarantee that each component meets engineering requirements, manufacturers often employ non-destructive testing (NDT), dimensional measurement, material verification and defect analysis. Knowing how to inspect the quality of closed die forged parts helps manufacturers and consumers to make better choices of suppliers, to eliminate quality risks and to assure the performance of the finished components in real operating conditions.
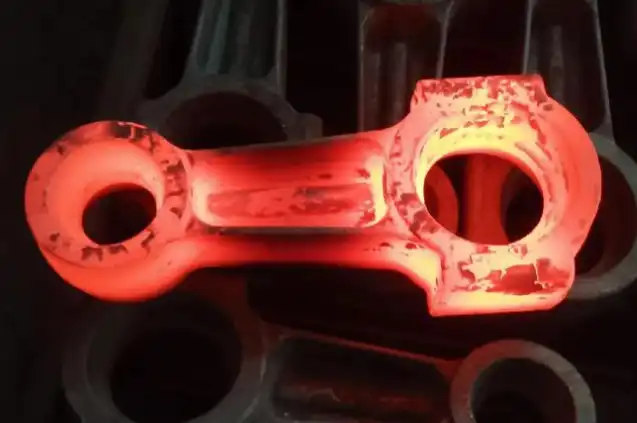
Comprehensive Non-Destructive Testing Methods for Forged Component Quality Control
Manufacturers may use non-destructive testing methods for evaluating forged parts without destroying them or impacting their usability. These inspection approaches are particularly vital for key components where internal faults could cause unexpected failures in service.
The selection of NDT methods depends on the part size, material, application needs, and the probable defect risk. For a full quality assessment in many industrial applications, a combination of several inspection methods is employed.
Ultrasonic Testing for Detecting Internal Forging Defects
Ultrasonic Testing (UT) is among the most commonly utilized inspection techniques to detect internal faults in closed-die forged components. This method sends high-frequency sound waves into the material and measures the discontinuities from the reflected signals.
In a UT examination, ultrasonic waves are sent through the forging. When the waves hit flaws like cracks, inclusions, voids, or internal discontinuities, the reflected signals are changed. These signals are analyzed by inspectors to determine the nature of the problem and assess the location and severity of the defect.
The fundamental benefit of ultrasonic testing is that it can detect issues within the material that cannot be seen visually. This makes UT especially useful for large-sized or thick-walled forged components used in applications where structural integrity is critical.
Heavy machinery parts, industrial shafts, and high-load components are frequently subjected to ultrasonic examination because internal faults can affect the fatigue resistance and the service life.
Radiographic Testing for Internal Structure Evaluation
Radiographic Testing (RT) utilizes X-rays or gamma rays to provide images of the internal structure of forged items. Inspectors can use these images to look for internal flaws like porosity, inclusions, shrinkage cavities, and other anomalies.
The advantage of radiographic examination over ultrasonic testing is that it provides a visual depiction of the internal conditions and is therefore effective in assessing complex geometries where the interpretation of defects might be difficult.
RT is often used for closed die forging parts with high requirements of reliability when manufacturers want further validation of internal quality. The procedure is typically used in conjunction with other examination techniques. Each technology has its merits.
For closed-die forged objects with complex shapes, radiographic testing assists inspectors to verify that the forging process has produced a consistent internal structure without undesirable discontinuities.
Dye Penetrant Testing for Surface Crack Detection
Dye Penetrant Testing (DPT), also known as liquid penetrant inspection, is an effective method for detecting surface-opening defects in forged components.
The process begins by cleaning the surface of the forged part. A liquid penetrant is then applied, allowing it to enter small surface defects such as cracks, seams, and pores. After removing excess penetrant and applying a developer, inspectors can clearly identify defect locations.
Dye penetrant testing is especially useful for non-porous materials and components where small surface cracks may not be visible during normal visual examination.
In closed-die forging production, DPT helps identify surface problems caused by improper material flow, forging stress, machining operations, or handling damage. Detecting these issues before delivery prevents defective components from entering final assembly.
Verifying Forging Accuracy Through Dimensional and Material Inspection
While non-destructive testing focuses on defect detection, dimensional and material inspections confirm whether forged parts meet design specifications and performance requirements.
A complete quality control system for closed die forging evaluates not only whether a component is free from defects but also whether it has the correct dimensions, material properties, and mechanical performance.
Dimensional Inspection Using Advanced Measurement Equipment
Dimensional accuracy is a key factor affecting the installation and performance of forged components. Even small dimensional deviations may cause assembly difficulties, poor fitting performance, or additional machining requirements.
Coordinate Measuring Machines (CMMs) are commonly used to measure complex forged components with high precision. These machines use advanced probing systems to collect accurate three-dimensional measurements and compare actual dimensions with engineering drawings.
CMM inspection can evaluate:
-
Overall dimensions
-
Hole locations
-
Surface profiles
-
Geometric tolerances
-
Alignment requirements
For industries such as automotive and aerospace manufacturing, where component precision is extremely important, CMM inspection provides reliable verification of manufacturing accuracy.
Manufacturers can use dimensional inspection reports to demonstrate that forged parts comply with customer drawings, specifications, and tolerance requirements.
Chemical Composition Testing for Material Verification
Material quality directly influences the strength, durability, and operating performance of forged parts. Therefore, chemical composition analysis is an essential step in the inspection process.
Spectrometry methods such as optical emission spectrometry (OES) and X-ray fluorescence (XRF) are commonly used to verify alloy composition.
These tests help confirm whether the material contains the required levels of elements such as
-
Carbon
-
Chromium
-
Nickel
-
Molybdenum
-
Manganese
Incorrect material composition may result in reduced mechanical performance, corrosion resistance problems, or premature failure.
For this reason, professional forging manufacturers maintain material traceability systems and provide documents such as material test reports (MTRs) or chemical analysis reports.
For customers purchasing customized forged components, material verification provides confidence that the supplied parts match the approved specifications.
Hardness Testing for Mechanical Property Confirmation
Hardness testing is another important inspection method used to evaluate closed die forging part quality. It measures the material’s resistance to indentation and provides information about strength characteristics and heat treatment effectiveness.
Common hardness testing methods include:
-
Rockwell hardness testing
-
Brinell hardness testing
-
Vickers hardness testing
The selected method depends on material type, component size, and customer requirements.
Hardness testing is particularly important after heat treatment because improper heat treatment conditions may cause inconsistent mechanical properties throughout the component.
By testing hardness at different locations, inspectors can confirm whether the forged part has achieved uniform material characteristics and meets required performance expectations.
Identifying Common Forging Defects Through Surface and Process Analysis
Although advanced testing technologies can detect many problems, understanding common forging defects helps manufacturers improve production processes and prevent quality issues.
Defects may occur because of improper die design, incorrect forging temperature, insufficient material flow, excessive stress, or unsuitable process parameters.
Visual Inspection for Detecting Surface Irregularities
Visual inspection is one of the first quality checks performed during forging production. Although simple, it remains an important method for identifying visible problems before additional testing.
Inspectors examine forged surfaces for defects such as
-
Surface cracks
-
Laps
-
Seams
-
Improper filling
-
Excessive oxidation marks
Magnification tools and surface measurement equipment may also be used when detailed examination is required.
For closed-die forged components, visual inspection helps identify issues related to metal flow inside the die cavity. For example, incomplete filling may indicate that the forging process parameters need adjustment.
Magnetic Particle Inspection for Ferromagnetic Forgings
Magnetic Particle Inspection (MPI) is designed for detecting surface and near-surface defects in ferromagnetic materials such as carbon steel and certain alloy steels.
During MPI testing, the forged component is magnetized, and magnetic particles are applied to the surface. When discontinuities exist, the magnetic field changes and causes particles to gather around defect locations.
This method is highly effective for finding:
-
Surface cracks
-
Grinding cracks
-
Seams
-
Near-surface discontinuities
MPI is commonly used for safety-critical components because it can identify small defects that may not be visible during normal inspection.
Eddy Current Testing for Conductive Materials
Eddy current testing (ECT) uses electromagnetic induction to identify surface and near-surface defects in conductive materials.
When an alternating magnetic field is applied to a conductive forged part produced by closed die forging, electrical currents are generated inside the material. Changes in these currents can indicate defects or variations in material conditions.
ECT offers several advantages:
-
Fast inspection speed
-
Ability to evaluate surface conditions
-
Suitability for automated inspection systems
-
No damage to the tested component
For high-volume manufacturing operations, eddy current testing can improve inspection efficiency while maintaining consistent quality control.
Building a Reliable Quality Inspection System for Closed-Die Forged Parts
A professional forging supplier does not rely on a single inspection method. Instead, quality assurance requires a complete system covering raw materials, forging processes, machining operations, heat treatment, and final inspection.
A comprehensive quality control process may include:
-
Incoming material inspection
-
Process monitoring during forging
-
Heat treatment verification
-
Dimensional inspection
-
Mechanical property testing
-
Non-destructive testing
-
Final quality documentation
In addition, manufacturers should maintain inspection records and provide supporting documents such as the following:
-
Material certificates
-
Inspection reports
-
Heat treatment records
-
Dimensional reports
-
Test results
These documents help customers verify product quality and support long-term traceability.
For companies sourcing customized forged components, choosing a supplier with strong inspection capabilities can reduce project risks and improve overall product reliability.
Conclusion
Inspecting the quality of closed-die forged parts requires a combination of advanced testing technologies, accurate measurement methods, and strict quality management procedures. Non-destructive testing methods such as ultrasonic testing, radiographic testing, dye penetrant testing, magnetic particle inspection, and eddy current testing help identify potential defects without damaging the components.
At the same time, dimensional inspection, chemical composition analysis, and hardness testing ensure that forged parts meet design requirements and mechanical performance expectations.
A reliable inspection system allows manufacturers to detect problems early, maintain consistent production quality, and deliver forged components that meet demanding industrial requirements.
For professional support in closed die forging and customized metal component manufacturing, Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. provides integrated solutions covering forging, casting, machining, and quality inspection. Founded in 2001 and certified under ISO 9001:2015 and API-7-1 quality systems, Welong supports customers with customized components, material verification, inspection documentation, and global delivery services. With experienced engineering teams and comprehensive manufacturing capabilities, Welong helps customers achieve reliable quality control from initial design to final production. For more information, contact them at metal@welongpost.com.
FAQ
1: What is the most effective non-destructive testing method for closed die forged parts?
While effectiveness depends on the specific part and material, Ultrasonic Testing (UT) is often considered highly effective for detecting internal flaws in closed die forged parts.
2: How important is dimensional inspection in closed die forging quality control?
Dimensional inspection is crucial in closed die forging quality control as it ensures that parts meet specified tolerances and design requirements, which is essential for proper fit and function.
3: Can visual inspection alone identify all common defects in closed die forged parts?
No, visual inspection alone cannot identify all common defects. While it can detect surface defects, additional methods like MPI or ECT are needed to identify subsurface flaws.
4: Why is material composition analysis important in closed die forging?
Material composition analysis is important to ensure that the forged part meets the required alloy specifications, which directly affects its mechanical properties and performance.
References
1. Smith, J.A. (2019). Advanced Techniques in Closed Die Forging Quality Inspection. Journal of Materials Engineering and Performance, 28(4), 2145-2160.
2. Johnson, R.B., & Thompson, L.M. (2020). Non-Destructive Testing Methods for Forged Components. Materials Evaluation, 78(6), 723-735.
3. Williams, E.C. (2018). Dimensional Verification in Closed Die Forging: A Comprehensive Guide. International Journal of Metrology and Quality Engineering, 9, 12.
4. Brown, K.L., & Davis, M.S. (2021). Material Property Analysis in Forged Parts: Current Trends and Future Prospects. Metallurgical and Materials Transactions A, 52(5), 2056-2070.
5. Anderson, P.R. (2017). Common Defects in Closed Die Forgings: Identification and Prevention. Forge, 30(2), 24-29.
6. Lee, S.H., & Garcia, C.T. (2022). Quality Control in Closed Die Forging: An Industry Perspective. Journal of Manufacturing Processes, 74, 293-308.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

