How to Improve Surface Finish on Sand Casting Parts?
Sand casting is still a practical method of making huge, complicated metal components that are cost sensitive. But if the mould, sand system and pouring circumstances are not adequately managed, the surface of a sand-cast part may be rough or display sand adhesion, burn-on, scabs, veining or other flaws. These problems might lead to higher requirements for cleaning, grinding, machining and inspection following casting. Therefore, improving the surface smoothness is not simply a matter of smoothing the mould. This involves coordination of pattern design, sand preparation, mould compaction, refractory coatings, gating, pouring and post-casting treatment. The proper procedure also depends on the alloy, the casting geometry, the dimensional accuracy required and the final use. For foundries and purchasers in the evaluation of casting quality, the objective should be to obtain a consistent as-cast surface that satisfies the drawing and application requirements without excessive processing expenses. The following methods describe how to regulate the source of the surface roughness in a repeatable manner and how to reduce it.
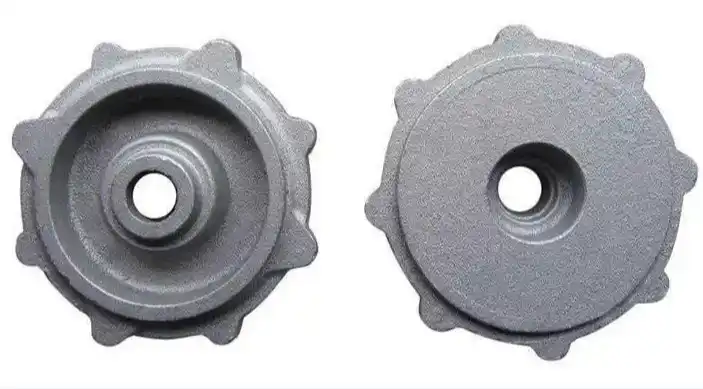
Start With Pattern and Mold Design
Use a pattern surface that supports the required finish.
The state of the pattern has a direct impact on the surface of the mold because it forms the cavity that determines the external surface of the casting. Scratches, dents, excessive roughness, or damaged portions of the pattern might be transferred to the mold and ultimately be seen in the completed component.
The surface of a well-maintained pattern should be appropriate to the casting process for which it is designed. Pattern material is important, too. Metal patterns give good durability and dimensional stability for repeated manufacturing, while suitably treated resin or other pattern materials may be suited for varying volumes of production.
Where appropriate, draft angles should also be included. Good airflow helps to remove the pattern and lowers the danger of harming the mold cavity. Even if the sand is properly prepared, if the mold wall is torn during the removal of the pattern, the final casting may contain localized roughness or other surface defects.
Design Around Metal Flow and Casting Geometry
The manner in which molten metal enters and fills the cavity also affects surface quality. Sharp transitions, sudden changes in the section thickness, badly placed gates, and needless turbulence are the cause of faults, which subsequently show up as surface imperfections.
Therefore, the pattern and mold design should be carried out along with the gating system. Simulation can help engineers understand the filling behavior of complicated components as well as identify locations where the flow may become unstable or premature solidification can take place.
The idea is not to make all the pieces of the mold the same. It aims to develop a mold that can be filled reliably while reducing situations that lead to inclusions, cold shuts, erosion, and other flaws.
Select and Control the Sand System Carefully
Balance Grain Size With Permeability
Sand particle size is one of the most important variables that impact the as-cast surface roughness. In general, finer grains can lead to a finer mold surface, which can help minimize the texture imparted to the casting. But that’s not necessarily the way forward, with finer and finer sand.
Welong's integrated experience in hot forging, forging, casting, machining, quality control, and supply-chain coordination provides a practical starting point for customized metal-part projects.
This is why foundries have to balance:
-
Grain distribution and size
-
Grain form
-
Permeability –
-
Strength of mold
-
Compactability:
-
Can be reused
-
Casting temperature
-
Alloy properties
-
Surface finish needed
The right sand specification should be based on the whole process, not only on the surface roughness.
Maintain Consistent Sand Moisture and Binder Conditions
In particular, for systems with water-based binders, it is crucial to regulate the moisture. Too much or uneven moisture can impact strength and gas production; not enough moisture can reduce the ability of the mold to keep its shape.
Control of binder and catalyst levels is also necessary in chemically bonded sand systems. The variations between batches could affect the strength of the mold, its ability to collapse, its permeability, and the quality of its surface.
A foundry should develop and monitor process ranges, rather than relying on the experience of the operators. Regular testing of the sand qualities can detect changes before they become casting faults.
Avoid Over-Compaction
Mold compaction controls the tightness of the sand particles around the pattern. Poor compaction may result in a weak or uneven surface of the mold, while too much compaction might decrease permeability and increase the risk of gas-related problems.
The compaction degree relies on the molding technology and the casting shape. Deep pockets, thin sections, cores, and complex shapes may not need the same considerations as basic open geometries.
Consistent compaction is particularly crucial in production runs, as differences between molds might result in variable surface quality from batch to batch.
Apply Mold Coatings Where They Add Value
Choose a Refractory Coating for the Alloy and Application
Select a Refractory Coating for the Alloy and Application
Mold coatings may form a refractory barrier between the molten metal and the molding sand. They are frequently employed when additional protection from metal penetration, burn-on, or certain surface flaws is required.
Different coating formulas are good for different casting situations. For example, zircon-based coatings are often utilized when strong refractory performance and resistance to metal penetration are required. Other formulations may be employed depending on the alloy, mold material, casting temperature, and production method.
The coating should not be considered a universal solution. Effectiveness relies on formulation, application method, thickness, drying, and state of mold.
Apply the Coating Uniformly
An inconsistent coating might lead to inconsistent surface conditions. If the area is too thin, it may not be protective enough; if the coating is too thick, it may cause drying or gas problems.
Application methods may include spraying, brushing, or other controlled procedures depending on the configuration of the mold and the manufacturing requirements.
Before pouring, the coating should be dry enough and adhere firmly to the mold surface. Particular attention should be paid to corners, deep cavities, cores, and other regions where coating coverage can be difficult to maintain.
Improve Gating and Pouring Control
Reduce Turbulence During Mold Filling
The way molten metal enters the mold has a direct influence on casting quality. Highly turbulent flow can increase oxidation, mold erosion, and the movement of inclusions. These problems may eventually appear as surface defects or require additional cleaning.
Gating design should therefore provide controlled filling appropriate to the casting geometry and alloy. The best configuration varies with part size, section thickness, metal fluidity, and production method.
Rather than relying on one gating arrangement for every component, engineers should evaluate the actual filling behavior of each casting design.
Maintain Stable Pouring Conditions
Welong's integrated experience in hot forging, forging, casting, machining, quality control, and supply-chain coordination provides a practical starting point for customized metal-part projects. If it is excessively high, the thermal load on the mold may increase, and some surface reactions may become more pronounced.
A stable pouring practice is therefore more valuable than simply increasing the pouring temperature.
Operators should follow defined process parameters and minimize unnecessary interruptions during pouring. Where production volume and casting geometry justify it, automated or controlled pouring systems can improve repeatability.
Use Filters When Inclusion Control Is Important
Ceramic foam filters and other filtration methods can be incorporated into suitable gating systems to reduce the movement of certain non-metallic inclusions into the mold cavity.
However, filtration should be considered as part of the complete gating design rather than as an isolated solution. Filter selection, placement, flow capacity, and compatibility with the alloy all need to be evaluated.
Identify Surface Defects by Their Root Causes
Distinguish Roughness From Metal Penetration
Not every rough surface has the same cause. General texture may simply reflect the molding sand, while deeper irregularities can result from metal penetration or a reaction between molten metal and the mold.
If metal penetrates between sand grains, the casting may require significant cleaning or grinding. In such cases, simply changing the post-casting cleaning method may not solve the underlying problem.
Potential corrective actions can include adjusting sand characteristics, improving mold compaction, using a suitable refractory coating, or modifying the gating and thermal conditions.
Investigate Sand Adhesion and Burn-On
Sand adhesion can occur when the molten metal interacts strongly with the mold surface. Thermal conditions, mold material, coating quality, and casting alloy can all contribute.
When the same defect appears repeatedly in the same location, engineers should examine the local geometry and thermal conditions rather than treating every casting as an independent problem.
This type of root-cause analysis is particularly valuable for production castings because a small change to the mold or process can sometimes prevent repeated cleaning work across an entire batch.
Use Post-Casting Treatment Strategically
Select Cleaning Methods According to the Casting
Even with a well-controlled molding and pouring process, sand castings normally require some level of cleaning. Common methods include shot blasting, abrasive blasting, grinding, and manual removal of gates and risers.
Shot blasting can efficiently remove residual sand and surface deposits from many components. However, blasting intensity and media should be selected according to casting size, wall thickness, material, and geometry.
Thin sections and delicate features require more controlled treatment than heavy industrial components.
Machine Only Where the Specification Requires It
Machining can provide a significantly smoother and more precise surface than the as-cast condition, but it also adds time and cost.
A better manufacturing strategy is to determine which surfaces actually require machining. Functional interfaces, sealing areas, bearing seats, and dimensional reference surfaces may need machining, while non-critical external surfaces may be acceptable in an as-cast condition.
This approach can reduce unnecessary machining while still meeting functional requirements.
The key in hot forging is to define surface roughness and dimensional requirements on the drawing or purchasing specification rather than assuming that every surface must receive the same treatment.
Build Surface Finish Into Quality Inspection
Measure Surface Roughness Instead of Relying Only on Appearance
Visual inspection is useful for identifying obvious problems, but appearance alone cannot provide a complete assessment of surface finish.
Where surface roughness is a critical requirement, manufacturers can use appropriate roughness measurement equipment to evaluate the surface against the specified criteria. Measurement locations should be selected according to the drawing, customer requirements, and casting geometry.
For repeat production, maintaining inspection records can also help identify process drift over time.
Track Defects Across Production Batches
A useful quality system does more than reject defective parts. It identifies recurring patterns.
For example, if roughness repeatedly increases after a particular number of molding cycles, the foundry may need to examine sand properties. If defects occur only around specific gates, the gating design may require review. If surface quality changes between operators, the pouring or mold preparation procedure may need better standardization.
Tracking defects by location, frequency, casting batch, material, and process parameters can make corrective action much more efficient.
Reduce Surface-Finish Costs Through Process Control
Improving surface finish should not mean adding more finishing operations to every casting. In many cases, the most economical solution is to prevent the defect at the mold or pouring stage.
A practical improvement program can follow this sequence:
-
Define the required surface finish for each casting surface.
-
Identify whether the problem originates from the pattern, sand, mold, pouring, or cleaning stage.
-
Measure relevant process variables instead of relying only on visual judgment.
-
Test one process change at a time where practical.
-
Compare defect rates and finishing time before and after the change.
-
Standardize the successful process and continue monitoring it.
This approach helps manufacturers avoid unnecessary modifications. For example, changing to a finer sand may appear to be an obvious solution to roughness, but if the actual issue is poor mold compaction or metal penetration, the change may create new permeability problems without solving the original defect.
The most effective surface-finish strategy is therefore usually a combination of appropriate mold materials, controlled sand properties, stable molding, suitable coatings, controlled metal flow, and targeted post-casting treatment.
Conclusion
Improving the surface finish of sand-cast components starts with controlling the process before the metal enters the mold. Pattern condition, mold design, sand grain characteristics, moisture or binder control, compaction, refractory coatings, gating, and pouring conditions can all influence the final surface.
The right solution depends on the casting rather than on one universal technique. Finer sand may improve mold texture but can affect permeability; stronger compaction can improve mold definition but may restrict gas escape; additional finishing can improve appearance but also increases manufacturing cost. For this reason, surface quality should be managed as part of the complete casting process.
For buyers and manufacturers, a capable casting supplier should be able to connect material selection, mold preparation, casting, cleaning, machining, and inspection rather than treating surface finish as an isolated post-processing issue. Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. provides casting and machining services for customized metal components and supports processes including sand casting, investment casting, centrifugal casting, and machining. The company operates under an ISO 9001:2015 quality management system and API-7-1 certification and works with materials including cast iron, steel, stainless steel, aluminum, copper, zinc, and other alloys.
For projects where surface condition, dimensional accuracy, material selection, and downstream machining all need to be considered together, discussing the casting geometry, material, required surface finish, and application requirements with the manufacturer at the quotation stage can help establish a more practical production route and avoid unnecessary finishing costs.Get in touch with Welong at metal@welongpost.com if you have any questions or would like to conversation around your person sand casting necessities.
FAQ
1: What is the most important factor in achieving a good surface finish in sand casting?
While many factors contribute, mold design and sand selection are among the most critical for achieving a good surface finish in sand casting.
2: How does sand grain size affect surface finish?
Generally, finer sand grains result in smoother surface finishes, but a balance must be struck to maintain adequate permeability for gas escape.
3: Can mold coatings improve surface finish?
Yes, mold coatings create a barrier between the molten metal and the sand mold, reducing metal penetration and improving surface finish.
4: What role does pouring technique play in surface finish quality?
Advanced pouring techniques, such as bottom pouring or tilt-pour casting, can minimize turbulence and improve metal flow, resulting in better surface finishes.
References
1. Smith, J. A. (2019). Advanced Techniques in Sand Casting Surface Finish Improvement. Journal of Foundry Technology, 45(3), 112-128.
2. Johnson, R. B., & Thompson, L. M. (2020). Mold Design Optimization for Enhanced Surface Quality in Sand Casting. International Journal of Metalcasting, 14(2), 456-470.
3. Chen, X., & Liu, Y. (2018). Effect of Sand Properties on Surface Finish of Cast Iron Parts. Materials Science and Engineering: A, 735, 243-252.
4. Brown, E. T. (2021). Innovative Approaches to Reducing Surface Defects in Sand Cast Aluminum Alloys. Light Metals Technology Conference Proceedings, 89-101.
5. Garcia, M. P., & Rodriguez, S. A. (2017). Comparison of Mold Coatings for Improved Surface Finish in Steel Sand Castings. Foundry Research Journal, 52(4), 201-215.
6. Wilson, K. L. (2022). Advancements in Post-Casting Treatments for Enhanced Surface Quality. Modern Casting, 112(7), 32-38.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

