How to Choose Between Open Die and Closed Die Forging for Your Project
Forging is widely used to manufacture metal components that require controlled material flow, reliable mechanical properties, and a strong internal structure. However, choosing a forging process is not simply a matter of deciding which method is stronger or more economical. The right process depends on the size and geometry of the component, production volume, material grade, dimensional requirements, tooling budget, and the amount of machining required after forging. The two processes most often compared for industrial components are open die forging and closed die forging. They use different approaches to control the shape of the workpiece and therefore suit different production requirements. Open die forging uses dies that do not completely enclose the workpiece, allowing the material to be moved and compressed in stages. Closed die forging uses shaped die cavities to control material flow and produce a component closer to its final geometry. For a large shaft, ring, pressure vessel component, or custom heavy forging, open die forging may provide the flexibility needed to control the deformation process. For a high-volume production program involving smaller and more geometrically defined components, closed die forging may provide better repeatability and reduced machining requirements. The following factors can help engineers, purchasing teams, and manufacturers determine which process is more appropriate for a specific project.
Start With the Size and Geometry of the Component
Why Part Dimensions Matter?
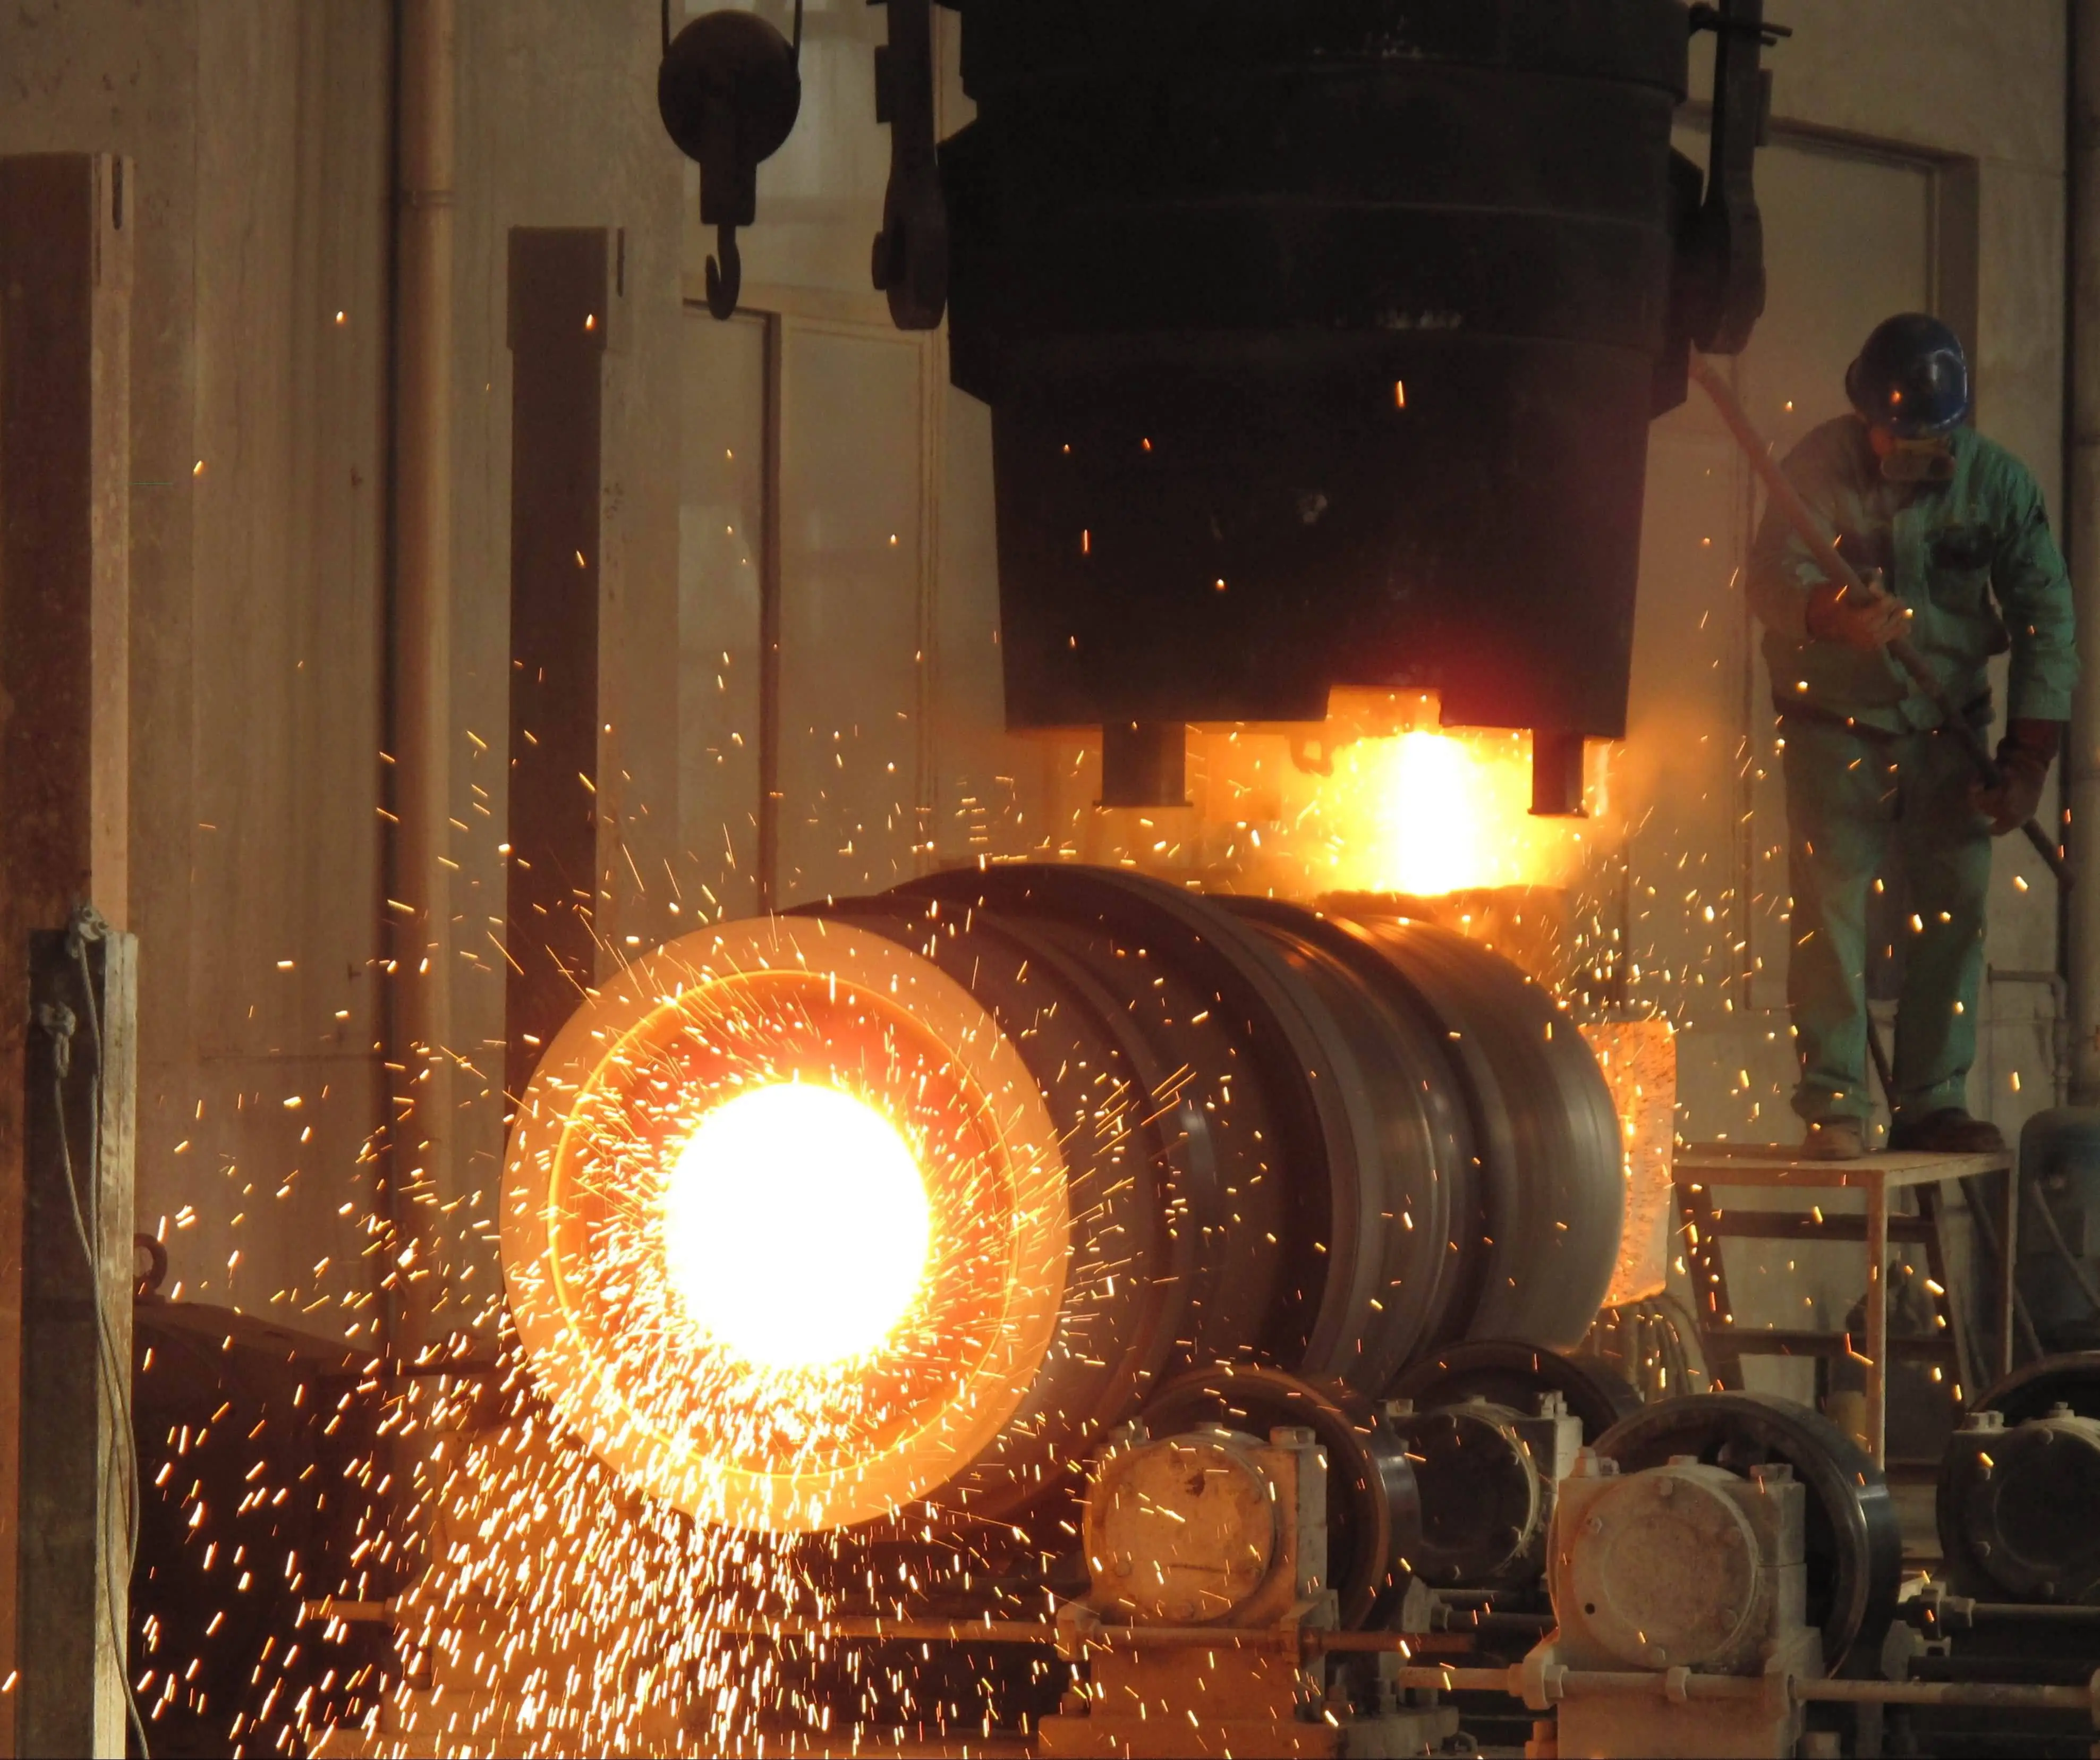
One of the first things to consider is the physical size of a part. Open die forging is especially useful for large and heavy components since the workpiece can be handled between relatively simple dies. The forging does not have to fit into a completely closed cavity; therefore, the maker has more latitude with wide cross-sections and huge forging weights.
This makes the technique suitable for usage in applications such as massive shafts, discs, rings, blocks, bars, and other heavy industrial components. Also practical when a customer wants a custom shape or the final geometry may alter during product development.
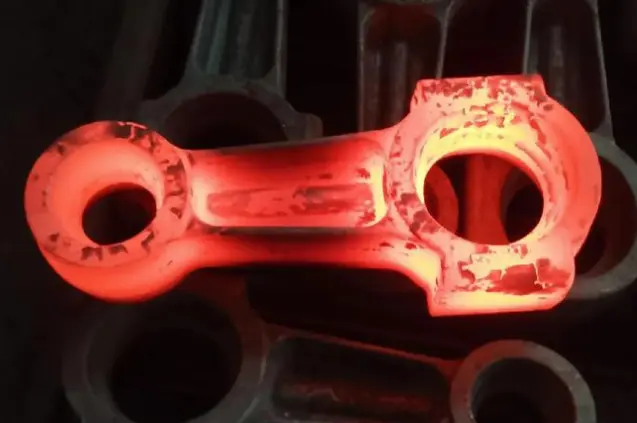
Closed die forging is often a better option when the part has a fixed three-dimensional shape that is to be consistently made. The dies contain cavities of the shape required for the piece, into which, under pressure, the heated billet is forced to flow.
This method can reduce the amount of material to be subsequently removed by machining for reasonably small components with repeatable geometries. However, the size of the component must be within the capability of the forging equipment and tooling.’
Consider Geometric Complexity
“Geometry can be just as much of an issue as overall dimensions. A big, comparatively simple part may be a good choice for open die forging, while a smaller part with several curves, bosses, recesses, or well-defined transitions may be well suited for closed die forging.
Open die forging offers tremendous freedom since the workpiece can be progressively shortened, extended, upset, or otherwise modified between forging operations. The maker can thus build a forging sequence around the material and the dimensions necessary, instead of a predetermined cavity.
In closed die forging there is another advantage. Once the dies are appropriately built, the cavity controls the flow of the material, and the same basic geometry can be repeated for the length of a manufacturing run. This repeatability can be important for components that must mate with other components or match set dimensional constraints.
The main thing is, you don’t want to look at complexity without looking at the amount of production. A complex component made only a few times may not justify expensive dedicated tooling, yet the same component made in thousands of units may make closed die tooling economically advantageous.
Compare Tooling Investment With Production Volume
When Does Open Die Forging Make Economic Sense?
Tooling cost can be a significant factor in the economics of a forging process. In open die forging, the dies are usually rather basic and do not need a chamber that reproduces the whole geometry of the completed part. This can lower the initial tooling cost and make the method suitable for prototypes, replacement parts, development programs, and limited production runs.
This flexibility is especially useful when the design of the component is not yet fixed. Engineers may have to change dimensions, change a transition, change a machining allowance, or change the forging sequence. Such a technique based on simpler tooling is more suited to such adjustments than is a dedicated closed die system.
Therefore, open die forging is frequently used when just a small number of parts are required or when the value of the individual component is high enough that the flexibility of the process is more significant than the cost of the tooling.
When Does Closed-Die Tooling Become More Attractive?
Closed die forging requires additional preparation, since the dies must be developed and fabricated to the requisite geometry. The tooling can comprise a number of cavities or stages, including provisions for flash and material flow, depending on the component.
That initial expense can make it less appealing for a very small run of production. But the calculation alters when the amount of output grows. Thousands or even tens of thousands of similar components are needed; the tooling cost can be spread over a significantly greater number of parts.
Once the method is established, closed die forging can deliver repeatable results and lower cycle times for acceptable components. Therefore, buying teams should consider the overall cost per completed component, not only the cost of the initial tooling.
When evaluating a project, tooling, raw material, forging labor, energy, heat treatment, machining, inspection, scrap, and the anticipated amount to be produced should be considered.
Evaluate Material Flow and Mechanical Requirements
How Deformation Affects the Workpiece?
Another key aspect to consider is the material behavior. Forging is the controlled plastic deformation of a heated metal workpiece to alter its shape. The technique in which deformation is applied is important for the grain flow, internal discontinuities, dimensional control, and the ensuing mechanical characteristics.
In open die forging the workpiece can be altered by a series of reductions and other operations. This permits the forging schedule to be made according to the grade of material, the initial dimensions of the billet, and the ultimate qualities required.
This flexibility can be useful for big alloy steels, stainless steels, nickel-based alloys, and other technical materials. Instead of constraining the entire workpiece to a single complex cavity, the producer can select appropriate reductions and intermediate dimensions.
Closed die forging also results in regulated material flow, yet the material must flow to fill the die cavity properly. The filling of the cavity depends on the forging temperature, the volume of the billet, the design of the die, the speed of the deformation, the lubrication, and the characteristics of the material.
The issue is not merely whether one procedure yields a 'better' material structure. Both procedures can be used to manufacture good-quality forgings, provided that the material, equipment, forging sequence, temperature, and quality standards are correctly regulated.
Match the Process to the Alloy
Forging temperature and deformation properties vary with different alloys. Carbon and many low-alloy steels are readily forged by conventional industrial practices; however, stainless steels, tool steels, nickel-base alloys, and other higher-performance materials may require more carefully controlled forging settings.
For an alloy with a restricted processing window or a specific deformation schedule, the forging provider should evaluate the material specification before choosing the technique.
The starting material size also plays a role. Depending on the component and the reduction necessary, a manufacturer may begin with a billet, bar, ingot, or other semi-finished form. The relationship between the beginning material and the final forging must be considered in the process planning.
For critical components, the supplier should not consider forging as a standalone process but should additionally consider heat treatment and inspection requirements along with the forging method.
Consider Dimensional Tolerance and Machining Requirements
Closed Die Forging for Defined Near-Final Shapes
One of the preferred manufacturing processes is closed die forging for its ability to make parts very near to their final geometry. The exterior shape is controlled by the die cavity in open die forging and can reduce the quantity of material to be removed during machining.
This does not mean that all closed die forgings can be used without machining. Critical surfaces, holes, threads, bearing seats, sealing regions, and other functional elements typically require further machining.
However, if the forging design is correct, decreasing the machining allowance can still reduce the machining time and material consumption.
Even a small reduction in machining time per part can make a big difference in manufacturing cost for high-volume production.
Open Die Forging Requires More Machining Planning
Open die forgings are usually more free around the final shape; therefore, machining allowances need to be thought of carefully. The machined component may be purposely made with excess material to obtain the appropriate final dimensions.
Not that it's necessarily a bad thing. For big shafts, blocks, rings, discs, and other heavy components, the flexibility of open die processing may be more important than attaining a near-final shape immediately from the forging procedure.
The idea is to describe the link between the forging dimensions and the machining dimensions before production starts.
A good supplier will analyze the customer’s drawing and identify essential dimensions, machining surfaces, tolerances, datum references, and inspection points. This avoids a situation where the forging is theoretically acceptable but does not have enough material for the machining operation needed.
Review Forging Temperature and Process Control
Temperature Must Match the Material
Forging temperature directly affects the material deformation and process stability. Each alloy has a temperature range that is good for hot working, and the maker must keep the temperature in the proper range throughout the forging sequence.
One of the more difficult problems is large workpieces where the surface may cool quicker than the interior. The forging schedule must then include reheating, transfer time, deformation processes, and the workpiece dimensions.
In this aspect open die forging provides flexibility, as huge components can be worked sequentially. This allows the maker to check the workpiece and decide if further heating or intermediate procedures are necessary before proceeding.
Also, closed die forging demands very tight temperature control. If the temperature is too low or the deformation conditions are not suitable, this can influence the filling and the surface quality, because the material has to fill a predetermined cavity.
The forging temperature should therefore be determined according to the alloy and the part to be forged and not presumed to favor one forging procedure in all situations.
Control the Entire Forging Sequence
Simply nailing the starting heat doesn’t make a forging process reliable. The sequence of upsetting, drawing, pressing, reheating, intermediate inspection, and final sizing can affect the completed component.
For important industrial items the supplier should have a defined process route and quality-control strategy. This may comprise dimensional inspection, hardness testing, ultrasonic testing, magnetic particle inspection, chemical composition verification, and mechanical testing, depending on the application.
The specific inspection package shall be established by the drawing, purchasing specification, applicable standard, and intended usage.
Consider Production Quantity and Delivery Requirements
Small Runs Favor Process Flexibility
The economic advantage of pricey dedicated tooling is reduced when only a few components are required. This is why open die forging is often used for small production runs.
It can also be appropriate when the customer requires multiple versions of a fundamental component. The maker may employ flexible tooling and machining to reach the desired dimensions, rather of creating a separate die for each geometry.
This can help development and make adapting as the project evolves easier.
High-Volume Programs Can Favor Closed Dies
Closed die forging is increasingly interesting to customers who require large quantities of identical components. The production may be repeated with a high degree of consistency after the tooling and process parameters are set.
The economic gain is achieved by amortization of tooling costs across greater production volumes and through the use of repeatable forging cycles and less downstream machining for suitable items.
That’s why it’s important to address the quantity to produce early in the quotation process. A cost-effective forging process for 50 bespoke parts may not be the best solution for 50,000 identical parts.
Do Not Ignore Inspection and Post-Forging Operations
Heat Treatment and Machining
Forging is only one stage in the manufacturing chain. Many industrial forgings require heat treatment to achieve specified mechanical properties, followed by machining to meet final dimensional requirements.
The supplier should therefore consider forging, heat treatment, machining, and inspection as a connected manufacturing route.
For example, a component may require rough forging followed by normalizing, quenching and tempering, rough machining, ultrasonic testing, final machining, and dimensional inspection. The most economical forging method is the one that produces the best overall manufacturing route, not necessarily the one with the lowest forging cost alone.
Documentation Matters for Industrial Procurement
For industrial buyers, technical documentation can be as important as the physical component. Depending on the project, customers may require material certificates, heat-treatment records, inspection reports, dimensional reports, non-destructive testing records, and certificates of conformity.
These requirements should be communicated before production begins. They can affect material selection, process planning, inspection stages, and delivery schedules.
A professional forging supplier should be able to review these requirements during quotation and identify any special testing or documentation that could affect project cost and lead time.
Conclusion
When deciding between open die and closed die forging, you need to think about a lot of things, such as the size and complexity of the item, the amount of production, the qualities of the material, and the cost. Open die forging is flexible and works well for making big or unique pieces, limited production runs, and materials that need precise control of their grain structure. Closed die forging is great for making a lot of parts with excellent accuracy and using the least amount of material. You should make your choice based on the needs of your project, taking into account things like the shape of the parts, the size of the production, the properties of the materials, and your budget. You can make an informed choice that improves your production process and guarantees the best possible result for your forging project by knowing the pros and cons of each approach.
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd., established in 2001, provides customized metal parts for customers across multiple industrial sectors. With ISO 9001:2015 and API-7-1 certifications, the company works across forging, casting, and machining processes and supports projects involving different materials, component sizes, and manufacturing requirements.
For forging projects, Welong can support customers from initial drawing review and process evaluation through production, quality control, and delivery. This approach is particularly useful when the choice between open die and closed die forging affects tooling investment, machining allowance, production quantity, or inspection requirements.
When requesting a quotation, customers can provide the part drawing, material specification, estimated quantity, applicable standards, required heat treatment, dimensional tolerances, and inspection requirements. With this information, the manufacturing team can evaluate the appropriate forging route and provide a more practical production proposal.
With a global customer base of more than 100 clients in over 20 countries, Welong focuses on customized metal manufacturing and international supply chain support. For projects that require large custom forgings, repeat-production components, or integrated forging and machining services, discussing the complete manufacturing route with the supplier at the quotation stage can help reduce avoidable tooling, machining, and production issues. Contact us at info@welongpost.com to discuss your project requirements.
FAQ
1: What is the primary difference between forging with open die and closed die?
Open die forging employs simpler tools and allows for greater freedom in the size and shape of parts. Closed die forging, on the other hand, uses complicated dies to make parts that are very close to the final shape with less waste.
2: When is it better to use open die forging instead of closed die forging?
Open die forging is best for making big or bespoke pieces, making short batches of parts, and working with materials that need thorough control of their grain structure and characteristics.
3: What are the benefits of closed die forging?
Closed die forging is more precise, accurate in size, efficient for making a lot of items, and it wastes less material than open die forging.
4: How does the choice of material affect the decision to use open die or closed die forging?
The option depends on how easy it is to deal with the material, how sensitive it is to temperature, and how complicated the alloy is. Closed die forging works better for materials that flow well, whereas open die forging works better for materials that are hard to deal with or have complicated alloys.
References
1. Smith, J. (2019). "Advanced Forging Techniques: Open Die vs. Closed Die." Journal of Materials Processing Technology, 45(3), 278–295.
2. Johnson, A. and Brown, T. (2020). "Comparative Analysis of Open and Closed Die Forging for Aerospace Applications." International Journal of Mechanical Engineering, 12(2), 89-104.
3. Thompson, R. (2018). "Things to Think About When Choosing a Forging Process." Metallurgical and Materials Transactions B, 49(6), 1235-1250.
4. Lee, S. et al. (2021). "Cost-Benefit Analysis of Open Die and Closed Die Forging in Contemporary Manufacturing." Journal of Manufacturing Processes, 62, 312-328.
5. Garcia, M. and Wilson, P. (2017). "Improving the structure of grains in forged parts: open die vs. closed die methods." Materials Science and Engineering: A, 703, 411–425.
6. Patel, K. (2022). "Forging Sustainability: A Comparison of Material Efficiency Between Open and Closed Die Techniques." Sustainable Materials and Technologies, 31, e00295.
Share your inquiry, get the quotation accordingly!
China WELONG- Your Reliable Partner in Metal Solutions