How to Achieve Net-Shape Forging With Minimal Machining
Net-shape forging is a manufacturing approach in which a forged component is produced very close to its required final geometry, reducing the amount of material that must be removed afterward. For manufacturers producing large quantities of steel, stainless steel, aluminum, titanium, or nickel-alloy components, this approach can reduce machining time, improve material utilization, and shorten the overall production route. However, achieving a true net-shape result is not simply a matter of using a more accurate forging die. The entire forging process has to be designed around the final part requirements. Billet volume, preform geometry, die design, material temperature, deformation sequence, lubrication, and dimensional inspection all influence whether a component can leave the press with only limited finishing work. It is also important to distinguish net-shape forging from near-net-shape forging. In practical manufacturing, some components still require machining on critical interfaces, holes, threads, sealing surfaces, or other areas where very tight tolerances are required. The objective is therefore not to eliminate machining at any cost, but to remove only the material that genuinely needs to be removed while preserving the required part quality.
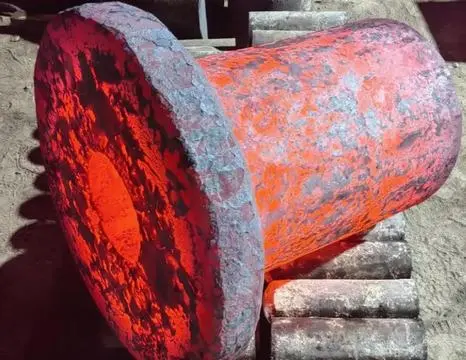
What Determines Whether a Part Is Suitable for Net-Shape Forging?
Start With the Final Part Requirements
The feasibility of net-shape forging should be considered from the final part backward. Before the die design, the engineers have to establish the functionally critical dimensions and surfaces.
For example, a bearing seat, sealing surface, threaded hole, or precise mating surface may demand tighter tolerances than other portions of the component. Even when most of the external profile can be forged near final size, some features may still require machining.
The distinction is essential, as it allows features to be left out of the forging procedure, which might add complexity to tooling without providing a real production benefit. A preferable strategy is to determine those surfaces that can be directly forged and those to be provided with a controlled machining allowance.
Thus, a careful study of the part drawing can indicate if the project is best suited for net-shape forging, near-net-shape forging, or a mix of forging and machining.
Control Billet Volume and Preform Geometry
The volume of material is one of the cornerstones of dimensional homogeneity. If the billet is too small, the die cavity may not fill up entirely. If there is too much material, too much flash may emerge, and you may need to do further trimming or machining.
The preform provides an intermediate geometry that directs the material to the locations it needs to go. Rather than pushing a basic billet directly into a very complex final cavity, producers may use one or more preforming procedures to provide a more desirable material distribution.
This is also crucial for components with different cross-sections, bosses, ribs, or other characteristics where the flow of metal needs to be controlled. A well-designed preform can limit the localized deformation and aid in minimizing flaws like laps, folds, or underfilled regions.
A little improvement in billet utilization can make a big difference in total material use in high-volume production. This makes billet weight and preform design crucial economic variables as well as quality considerations.
How Should the Die Be Designed for Minimal Machining?
Optimize Parting Lines, Draft, and Corner Radii
The geometry directly impacts the flow of the metal into the cavity and the ease with which the final forging can be removed. The location of the separating line is of special importance, since an ill-placed parting line may result in excessive flash or difficulty in precisely forming some features.
Draft angles must also satisfy two criteria: to allow the forging to release from the die and to avoid needless alterations to the final shape. The right draft will depend on the material, the part geometry, the tooling setup, and the manufacturing process.
Corner and transition radii are crucial too. Sharp edges might interfere with material flow and increase the likelihood of laps or incomplete fill. Proper radii lead to better flow channels and will help decrease localized stresses in the forging and the tooling.
Thus, it is important to discuss the die design in conjunction with the designing of the part rather than as a separate tooling effort.
Design for Controlled Flash and Trimming
In closed-die forging sometimes a flash is needed to create pressure and to achieve complete die filling. But flash that is excessive is waste and can increase the amount of trim required.
Thus the flash land, gutter, and surrounding die geometry should be constructed to deliver appropriate pressure without any undue extra material. The optimum arrangement is a function of the alloy, the part geometry, the press capacity, and the deformation sequence.
Using a net-shape method doesn’t necessarily mean eliminating flash entirely. Instead, the aim is to regulate the creation of the flash so that the forging is consistently filled with the minimal loss of material and subsequent operations.
Account for Tool Wear and Dimensional Change
Many things made in one trial with a die cannot be made in the same dimensions after thousands of production cycles. Wear, heat cycling, lubrication conditions, and repeated mechanical loads can cause subtle changes to crucial die surfaces.
Thus, engineers should evaluate which dimensions are vulnerable to die wear and how those dimensions will be monitored for production tooling. Inspection data can be applied, when applicable, to develop maintenance or die-replacement requirements prior to the generation of excess scrap due to dimensional drift.
This is especially critical for net-shape applications, since the smaller the machining allowance, the less opportunity there is to mitigate for dimensional variation after forging.
Which Process Parameters Have the Greatest Influence?
Maintain a Stable Forging Temperature
Temperature greatly influences material flow, deformation resistance, surface condition, and microstructural development. The correct temperature process range is dependent upon the material grade and forging method and should be determined from applicable material and process data rather than as a general value.
Inadequate heating increases the forging loads and makes die filling more difficult. Excessive heating, however, may cause an increase in oxidation, grain growth, or other unwanted changes in the material.
Hence, it is often more vital to have temperature consistency than simply meeting a nominal goal temperature. The temperature conditions of the forging process have to be developed, taking into account the billet, the die, the transfer time, and the manufacturing cycle.
Control Press Speed and Deformation Sequence
Press speed affects strain rate, heat transfer, material flow, and production cycle time. The best is specific to the material and the forging equipment.
In the case of complicated components, the sequence of deformation can be as significant as the ultimate forming force. A good sequence will bring material into the necessary areas gradually rather than having one action produce all the geometry.
Localized flow in the forging process can cause folds, laps, underfilling, or excessive flash if the sequence of deformation is not well-matched to part geometry. Hence, process development has to take into account the whole developing sequence and not only the last stroke.
Use Lubrication as a Process-Control Tool
The lubrication minimizes the friction between the workpiece and die. However, lubrication does more than only help remove the forged piece. The friction impacts the metal flow through the cavity and thus the dimensional uniformity.
Incorrect lubricant application can cause the flow behavior to be varied in the regions of the die. For repeat production, the kind of lubricant, application method, coverage, and die temperature should be managed as part of the whole process and not as minor operating details.
How Can Simulation Reduce Development Risk?
Use FEA to Study Material Flow Before Tool Manufacturing
Finite element analysis can assist engineers in seeing how the billet or preform will deform before they commit to production tooling. A simulation allows you to see if the part may be underfilled, have too much flash, deform in specific areas, or have a flow pattern that is not optimum.
It is especially useful when the part has an irregular cross-section or when the material has a relatively high resistance to deformation. During the development stage, engineers can compare alternate preforms, die geometries, and process conditions rather than having to depend on repeated physical trials.
FEA does NOT substitute for physical verification. Its significance lies in the potential to decrease wasteful trial-and-error and provide more information for choosing which tooling innovations are worthy of actual testing.
Combine Thermal and Mechanical Analysis
Forging is a thermo-mechanical coupled process. The temperature of the material changes during deformation, and the heat transmission is influenced by contact with the die and surrounding environment.
The thermal analysis can therefore support the mechanical simulation by highlighting where the workpiece could cool down quickly or produce high temperature differences. This knowledge can assist in explaining why similar areas of a part may react differently throughout the forming.
For materials that are highly temperature sensitive, this type of study can be essential in defining a repeatable production window.
Validate Simulation With Production Data
The findings of the simulation should be compared with real forging trials. Loading data, forging temperature records, dimensional inspection, and observed material flow can all provide important input.
If the physical outcome does not match the simulation, the material model, the assumptions of the friction, the thermal conditions, or the boundary conditions may need to be reconsidered.
You should approach the feedback loop as more valuable than a one-off design step in simulation. Simulation and production data should go hand in hand during process development for complex net shape applications.
What Manufacturing Technologies Can Improve Net-Shape Results?
Precision Closed-Die Forging
Controlled exterior geometry and reproducible manufacturing dimensions are often achieved with precision closed-die forging. With good tooling and a correctly designed preform, many external surfaces can be brought close to final proportions.
This is especially attractive where the volume of production justifies dedicated tooling. For smaller volumes the investment in tooling has to be balanced against the expected decrease in machining and material consumption.
Isothermal Forging for Difficult Materials
Isothermal forging keeps the workpiece and dies at controlled high temperatures so as to minimize temperature-associated variations in the course of deformation. It may be beneficial for materials that are difficult to forge or very sensitive to temperature change, such as some aerospace alloys.
It is not always the ideal option for every component, as the process requires specialized heat and tooling control. The value thereof shall be estimated on the basis of the material, the geometry, the volume of production, and the dimensional performance necessary.
Hybrid Forging and Machining Strategies
In practice, a net-shape approach frequently involves combining forging with some machining rather than trying to remove machining altogether.
A part may be forged to near final exterior dimensions yet leave controlled stock on a bearing interface or sealing surface. In this way, the forging does most of the material removal, and machining gives you the last precision where you really need it.
This hybrid forging process provides a superior combination of tooling cost, dimensional accuracy, manufacturing speed, and material efficiency for numerous industrial items.
How Should Net-Shape Forgings Be Inspected?
Check Critical Dimensions After Forging
Dimensional examination should be concentrated on those features that determine whether the forging can be directly processed into the next operation. It can be overall dimensions, concentricity, profile accuracy, thickness, and essential feature locations depending on the component.
Selection of inspection methods for production parts should be based on drawing requirements and manufacturing tolerances. The first item inspection can be particularly valuable during process qualification, since it can verify that the created tools and process are capable of delivering the specified geometry.
Monitor Surface and Internal Quality
“A part can have respectable outside dimensions and not be free of quality problems. Surface problems like laps, fissures, or die markings may have to be investigated before the forging goes on to further processes.
Additional inspection methods may be employed to assess internal or metallurgical quality, if required by the material, application, or client specification.
The inspection strategy should be customized to the material of the component, service needs, standards, and customer requirements rather than applying the same inspection package to all forgings.
Track Process Stability During Production
Repeatability is crucial for net-shape fabrication. If a forging is in conformance with the drawing requirements one time but then falls out of tolerance over time, it is not a reliable production process.
Therefore, manufacturers should monitor relevant process variables and dimensional data over time. Trends in forging load, temperature, die condition, and critical dimensions can be used to detect process changes before they become serious quality problems.
Here a good forging process is more important than a high-precision die.
When Does Net-Shape Forging Deliver the Greatest Value?
Net-shape forging is generally most attractive when the component has enough production volume to justify precision tooling and when a substantial portion of the final geometry can be formed reliably.
The benefits can include:
-
Lower machining time
-
Reduced machining material removal
-
Better billet utilization
-
Shorter production routes
-
Lower material waste
-
More consistent repeat production
-
Reduced dependence on extensive post-forging machining
However, tooling cost and process-development time should also be considered. A simple part produced in a small quantity may not justify a highly optimized net-shape die, while a complex component produced in large volumes may benefit substantially from the investment.
The correct decision should therefore compare the complete manufacturing route rather than looking only at the initial forging cost.
How to Develop a Net-Shape Forging Project
A successful project normally starts with the finished component rather than with the forging equipment. The manufacturer and customer should review the drawing, material grade, annual production volume, critical tolerances, surface requirements, and existing machining route.
The next step is to determine which features can be formed directly and where machining allowance should remain. Preform development and die design can then be evaluated using engineering calculations and, where appropriate, FEA simulation.
After tooling development, trial forgings should be inspected against the drawing requirements. The results can be used to adjust material volume, die geometry, process parameters, or machining allowance before production is released.
This structured approach helps avoid a common mistake: trying to achieve the smallest possible machining allowance before the basic material-flow behavior has been validated.
Conclusion
Achieving net-shape forging process performance with minimal machining requires more than precision tooling. The final part requirements, billet volume, preform geometry, die configuration, temperature, deformation sequence, lubrication, and inspection strategy all need to work together.
The most effective approach is to identify which surfaces truly need machining and then design the forging route to bring the remaining features as close to final dimensions as practical. FEA and thermal analysis can reduce development risk, while physical trials and dimensional inspection remain essential for validating the production result.
Net-shape forging is therefore best viewed as a complete manufacturing strategy rather than a single forging technique. When the part geometry, production volume, material, tooling investment, and quality requirements are aligned, it can reduce unnecessary machining and material waste while maintaining the dimensional performance required for industrial applications.
Your Trusted Partner for Custom Metal Parts & Global Manufacturing Solutions
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. provides customized metal-part manufacturing solutions covering forging, casting, and machining. Established in 2001, the company operates with ISO 9001:2015 and API-7-1 quality systems and supports customers across Europe, North America, and Asia.
For projects where minimizing machining is important, the manufacturing route should be evaluated before tooling is finalized. Our team can support the process from drawing review and material selection through forging development, machining, quality control, and supply-chain coordination.
If you are evaluating a component for net-shape or near-net-shape forging, providing the part drawing, material specification, annual quantity, critical tolerances, and current machining requirements can help determine the most practical forging process. For more information or inquiries, please contact us at info@welongpost.com.
FAQ
1: What is net-shape forging?
Net-shape forging is a manufacturing technique that produces parts close to their final shape, requiring minimal or no machining after forging.
2: How does net-shape forging reduce production costs?
Net-shape forging reduces costs by minimizing material waste, decreasing machining time, and lowering energy consumption in post-forging operations.
3: What are the key challenges in achieving net-shape forging?
Key challenges include optimizing die design, controlling material flow, maintaining precise process parameters, and managing temperature distribution during forging.
4: How do simulation tools contribute to net-shape forging?
Simulation tools like FEA help predict material behavior, optimize die designs, and refine process parameters without costly physical trials.
References
1. Smith, J. D., & Johnson, R. A. (2019). Advancements in Net-Shape Forging Technologies. Journal of Materials Processing Technology, 285, 116-128.
2. Chen, L., Wang, X., & Zhang, Y. (2020). Optimization of Die Design for Net-Shape Forging Using FEA and Machine Learning. International Journal of Advanced Manufacturing Technology, 106(5), 2145-2160.
3. Anderson, M. K., & Thompson, P. E. (2018). Thermal Management Strategies in Precision Forging for Net-Shape Production. Journal of Manufacturing Science and Engineering, 140(8), 081010.
4. Kumar, S., & Patel, V. (2021). Hybrid Forging Processes: Integrating Additive Manufacturing with Traditional Forging. Materials Today: Proceedings, 45, 5123-5130.
5. Wilson, E. G., & Brown, T. H. (2017). In-Process Monitoring and Adaptive Control Systems for Net-Shape Forging. CIRP Annals, 66(1), 267-270.
6. Nakamura, T., & Lee, S. K. (2020). Material Selection and Form Design for Net-Shape Forging of High-Performance Alloys. Materials Science and Engineering: A, 782, 139285.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

