Drop Forging vs Press Forging: Key Differences Explained
Forging is widely used to manufacture load-bearing metal components because controlled plastic deformation can produce a useful grain flow and reduce the risk of defects associated with some other manufacturing routes. Among the many forging processes available, drop forging and press forging are two important options for producing shaped components. Both are shaping procedures for heated or otherwise adequately conditioned metal . Both involve dies and compressive force . Both are extremely distinct . Drop forging is the use of rapidly moving hammer or ram strikes, normally in a sequence of strokes. A mechanical or hydraulic press is used for press forging to apply force in a regulated stroke. This variation impacts deformation rate, die contact time, material flow, equipment needs, production planning, and the way engineers look at tooling and quality control. Neither approach is naturally superior for every application. The best approach will rely on the alloy, part geometry, needed production volumes, dimensional requirements, availability of equipment and final mechanical qualities required. This knowledge helps manufacturers and buying teams choose a forging path considering the entire production process, not just one aspect like forming speed.
Understanding How Force Is Applied in Each Forging Process
How Drop Forging Uses Impact Energy?
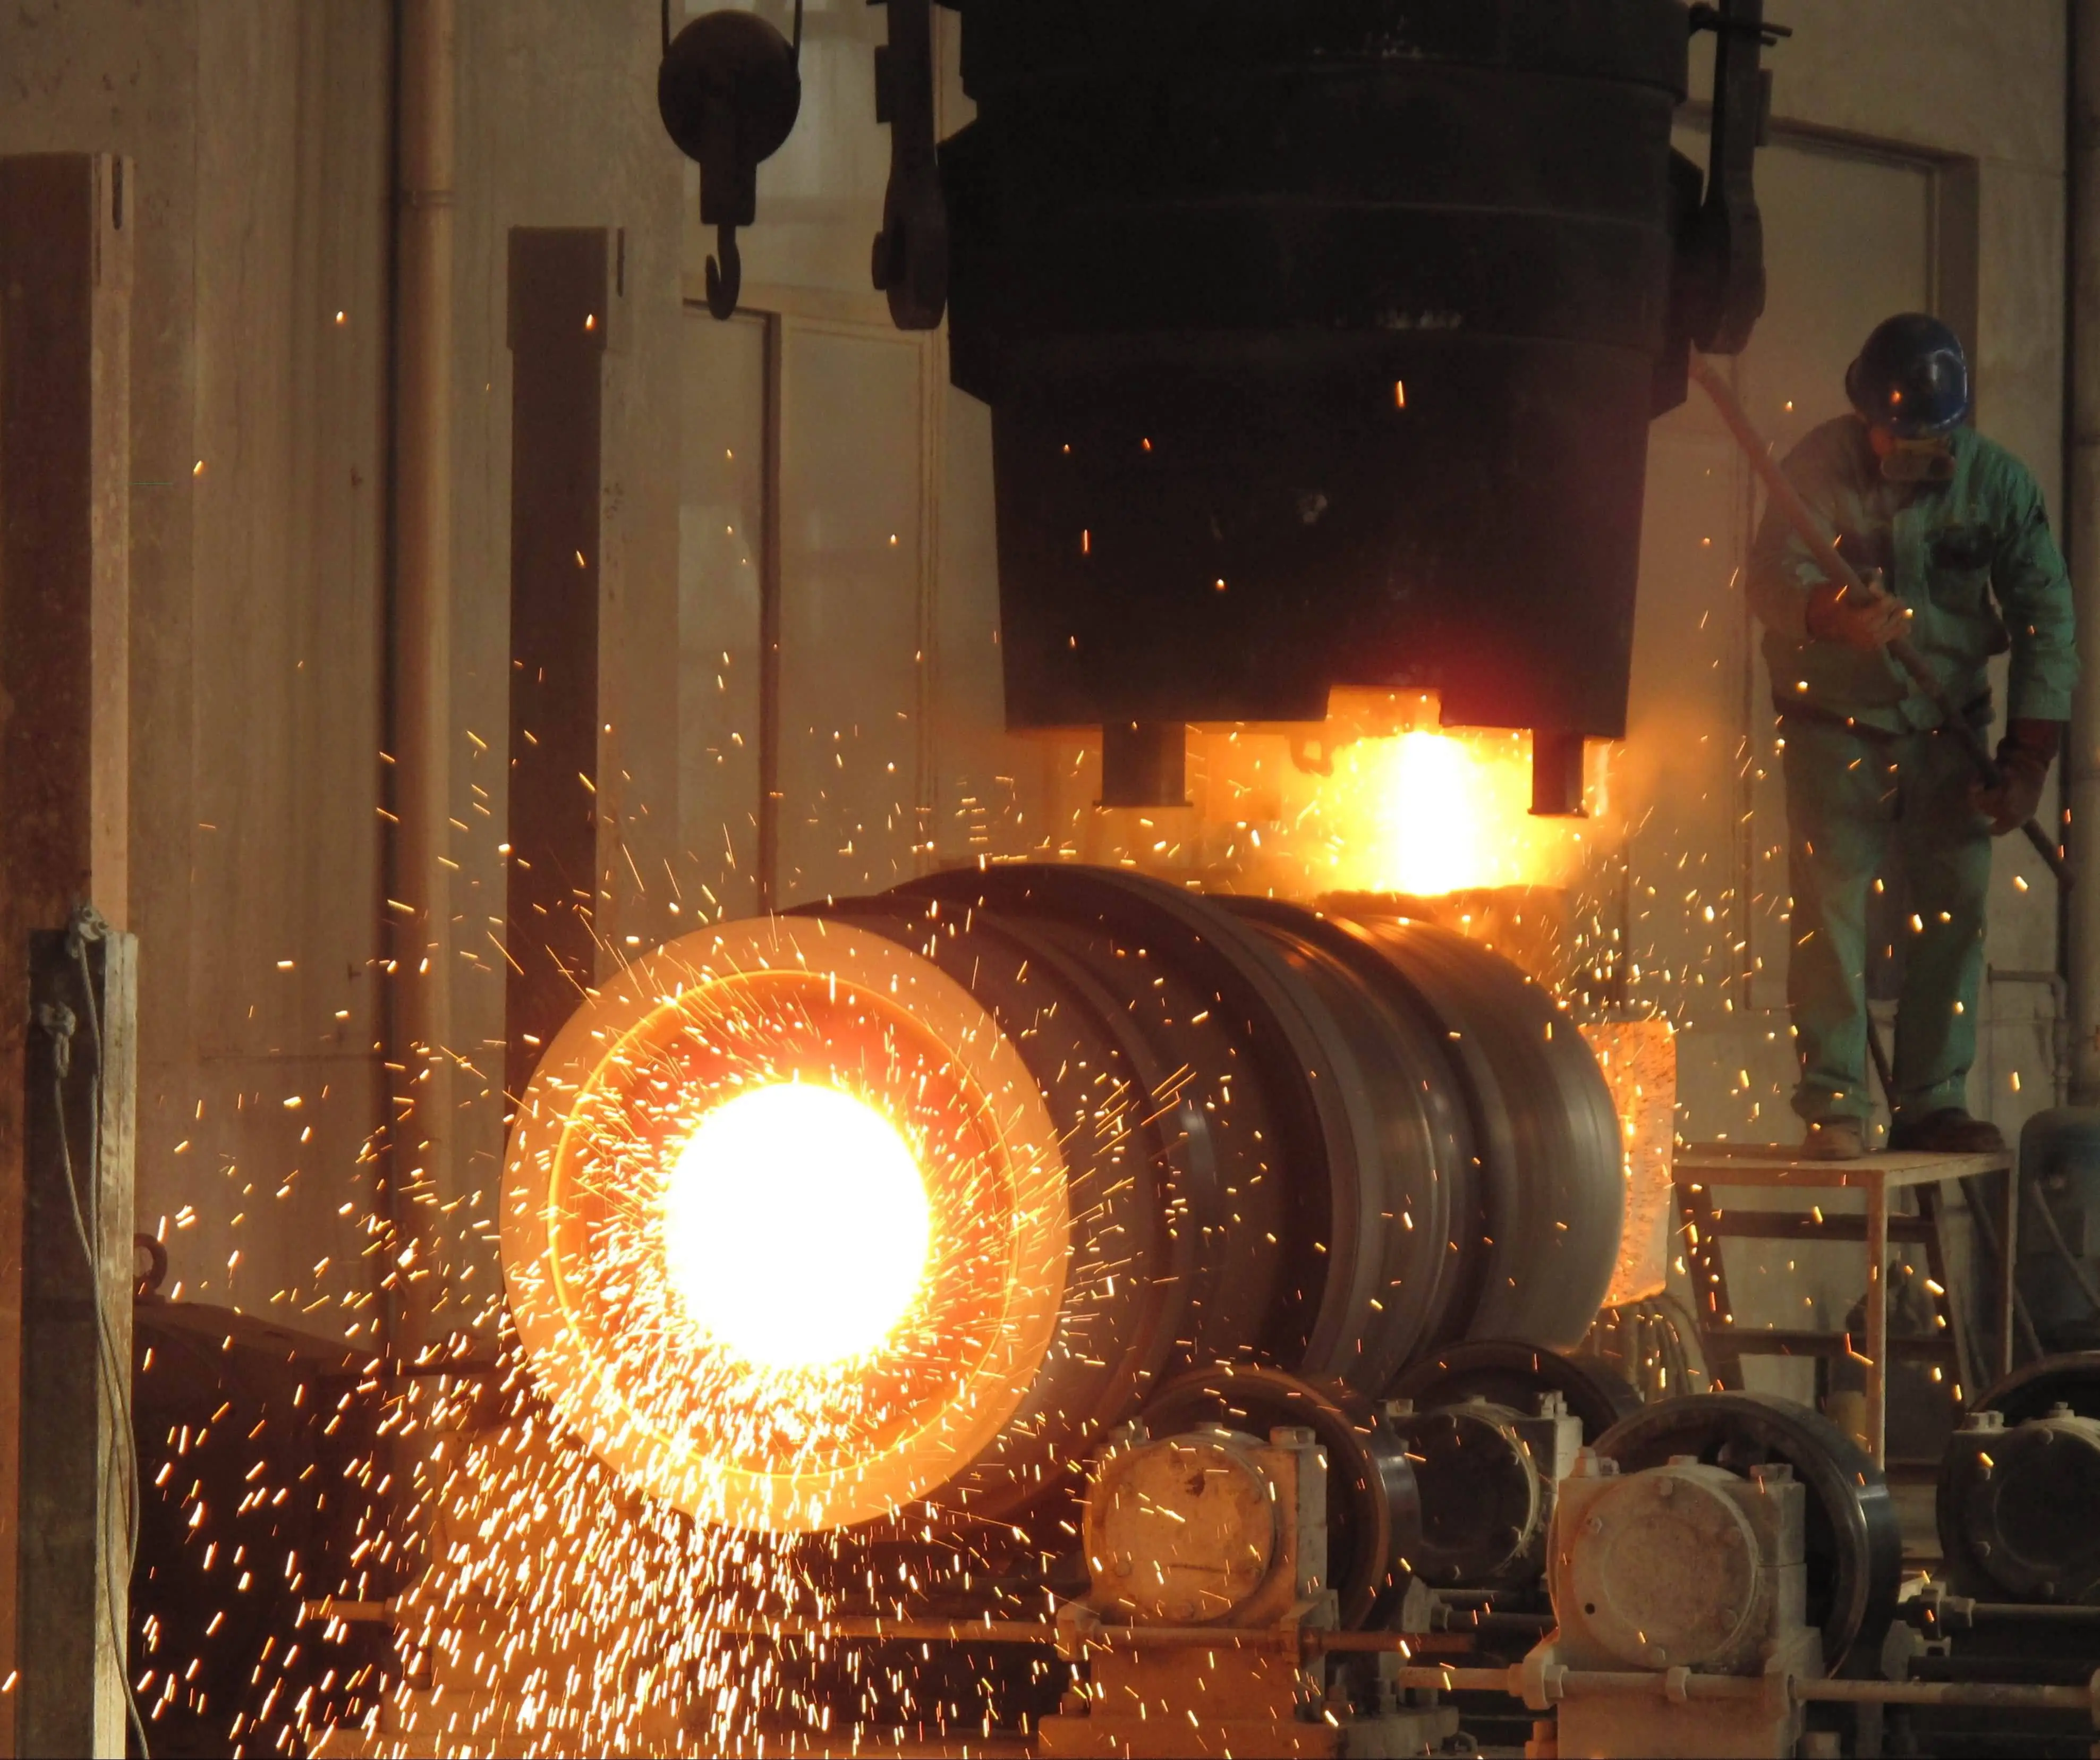
In drop forging, a heated billet or preform is positioned between dies, and an upper die is driven downward by a hammer or ram. Depending on the equipment, the energy may come from a falling mass, a powered hammer, or another impact mechanism. The workpiece is progressively shaped through one or more blows until the material fills the required regions of the die.
The most important characteristic is the relatively high deformation rate. Instead of maintaining contact and applying pressure continuously for a longer period, the hammer delivers short-duration impacts. Several blows may be required, particularly when the component has multiple forming stages.
This approach can provide efficient production for suitable component designs. It is commonly considered for forged components where repeatable die impressions and effective material flow are important. However, the impact nature of the process also places demanding loads on the dies and forging equipment. Die design therefore needs to account for impact loading, wear, flash formation, draft, and the required material flow.
The final properties should not be attributed to impact alone. Forging temperature, reduction, alloy chemistry, cooling conditions, and subsequent heat treatment all influence the resulting microstructure and mechanical performance.
How Press Forging Controls Deformation?
Press forging replaces repeated hammer blows with a controlled squeezing action. The upper and lower dies close around the workpiece while a mechanical or hydraulic system applies force through the stroke.
Because the force is applied progressively, engineers can control variables such as ram movement, stroke, and forming sequence more closely than in a conventional hammer operation. This makes press forging useful when controlled deformation and dimensional consistency are major priorities.
Press forging can be performed using different equipment configurations. Mechanical presses are generally associated with repeatable strokes and relatively high production rates, while hydraulic presses provide greater flexibility in force application and can be useful for large forgings or applications requiring substantial forming depth.
The longer die contact associated with press forging can also influence heat transfer between the workpiece and the dies. For hot forging, temperature control therefore becomes an important part of process development. Excessive cooling during forming can increase deformation resistance and affect material flow.
Why Impact and Compression Produce Different Process Conditions?
It is tempting to summarise the two processes as fast drop forging versus slow press forging, but that comparison is incomplete.
The more useful engineering distinction is how the forming load is delivered and controlled. Drop forging delivers energy through impact, while press forging applies force progressively through a controlled stroke. This changes the deformation conditions experienced by the workpiece.
As a result, engineers should consider deformation rate, depth and distribution of plastic deformation, die contact time, forging temperature, required forming stages, die wear, equipment capacity, and dimensional requirements.
The distinction is particularly important when evaluating a new component. A process that works well for a relatively small automotive component may not be appropriate for a large industrial forging, even if the basic geometry appears similar.
Selecting the Forging Method for Different Production Requirements
Production Volume and Tooling Investment
Production quantity is an important factor, but it should not be used alone to select the process.
Drop forging can be attractive for repeat production because established dies can produce the same component through a repeatable sequence of blows. Once tooling and process parameters have been validated, production can be efficient for suitable part sizes and geometries.
Press forging can also support high-volume manufacturing, particularly when mechanical presses are used. Its production economics depend on press capacity, stroke rate, tooling design, material utilisation, and the number of forming operations.
For this reason, procurement teams should compare cost per finished part rather than simply comparing the purchase price of the forging equipment. A meaningful cost evaluation should include tooling, material, heating, forging cycle time, trimming, heat treatment, machining, inspection, die maintenance, and expected tool life.
A process with a higher initial tooling investment may still provide a lower unit cost when production volume is high enough. Conversely, a more flexible process can be attractive when quantities are limited or product designs are likely to change.
Part Geometry and Material Flow
Part geometry is another important selection factor. Both drop forging and press forging can produce relatively complex components, but the most appropriate process depends on how the material must flow through the dies.
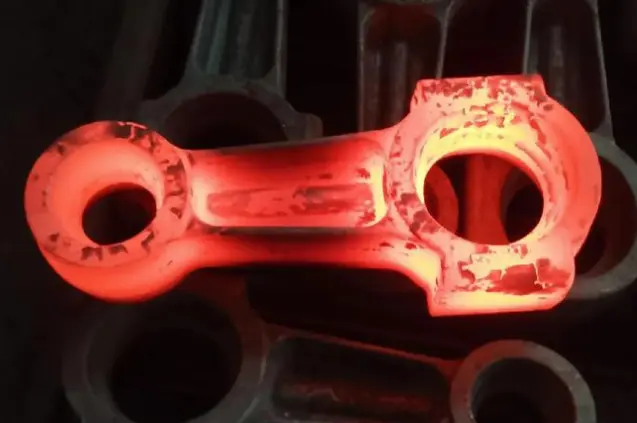
Drop forging is often effective for components that can be formed progressively through several impressions. Automotive and industrial components such as connecting rods, shafts, levers, and other shaped parts can be manufactured using hammer-based forging routes when the design and material are suitable.
Press forging offers advantages when controlled deformation through a significant portion of the workpiece is required. It can also be useful for larger components and processes where the forging sequence requires careful control of the reduction.
Instead of asking whether a part is simply "complex", engineers should evaluate its maximum cross-section, length-to-thickness ratio, draught angle, parting-line location, material flow direction, machining allowance, and number of required forming stages.
The removal of the finished forging from the die must also be considered. A geometry that appears straightforward in a CAD model may create practical difficulties if it requires excessive draft, creates difficult die corners, or restricts material flow.
Material Grade and Forging Temperature
Not every alloy responds to rapid deformation in the same way. Carbon steels, alloy steels, stainless steels, aluminium alloys, titanium alloys, and other engineering materials can have different forming windows and temperature sensitivities.
A material that is suitable for hammer forging may require different process parameters on a press. Likewise, alloys with limited ductility may benefit from carefully controlled deformation conditions.
Temperature is especially important for hot forging. If the workpiece loses too much heat during forming, its resistance to deformation can increase, and the risk of incomplete die filling or other forming problems may rise.
For this reason, the forging route should be developed together with the material specification and heat-treatment schedule rather than treating the forging machine as an isolated decision.
Evaluating Grain Flow and Mechanical Performance
How Forging Influences Grain Flow?
Forging is often selected because controlled plastic deformation can produce favourable grain flow compared with machining a component entirely from a solid block. However, grain orientation is determined by the way material moves through the die, not simply by whether a hammer or press is used.
In drop forging, repeated impacts can progressively move material into the die cavity and establish directional grain flow that follows the shape of the component. This can be beneficial when the grain-flow direction corresponds with important load paths.
Press forging can also produce controlled grain flow. Progressive deformation allows engineers to manage the forming sequence and material movement through the workpiece. This can be particularly useful when the component has large sections or requires substantial deformation.
Therefore, it is inaccurate to state that one process always produces a superior grain structure. The actual result depends on reduction, preform design, die geometry, forging temperature, deformation sequence, and subsequent heat treatment.
Strength, Toughness, and Fatigue Performance
Strength, toughness, ductility, fatigue resistance, and hardness are affected by many variables beyond the choice of forging equipment.
A properly designed forging process can produce a sound component with favourable material flow, but the final mechanical properties also depend on alloy composition, forging temperature, amount of deformation, cooling rate, heat treatment, grain size, and machining condition.
For example, a component subjected to cyclic loading may require a grain-flow direction that follows the primary stress path. Another component may require more consistent properties across multiple directions. These requirements should be considered during die and preform design.
For critical components, manufacturers should verify the result through appropriate mechanical testing and metallurgical inspection rather than relying on general assumptions about drop forging or press forging.
Depending on the application, quality verification may include tensile testing, hardness testing, impact testing, ultrasonic testing, magnetic particle inspection, dimensional inspection, or metallographic evaluation.
Surface Finish and Dimensional Control
Surface condition and dimensional accuracy are also important when comparing forging processes.
Press forging can provide controlled die closure and predictable deformation, which may help maintain dimensional consistency. Mechanical presses can provide repeatable strokes, while hydraulic presses allow greater flexibility in controlling the application of force.
Drop forging can also produce accurate components when the dies, equipment, and process parameters are properly controlled. However, repeated impact loading can contribute to die wear, and die condition can influence dimensional consistency during long production runs.
Neither process should be expected to eliminate machining in every application. Shafts, flanges, connecting components, and other precision parts may still require turning, milling, grinding, drilling, or other finishing operations after forging.
The more useful engineering question is therefore not which process has universally better accuracy, but which forging route can achieve the required near-net shape while keeping subsequent machining and finishing requirements under control.
Comparing Drop Forging and Press Forging in Practical Applications
When Drop Forging May Be the Better Option
Drop forging can be a strong candidate when a component will be produced repeatedly and the geometry is compatible with progressive die impressions and hammer-based forming.
It may be considered for applications where:
-
repeated production is required;
-
the component benefits from directional grain flow;
-
several controlled hammer blows can efficiently fill the dies;
-
the component size is compatible with available hammer capacity;
-
established tooling can be used for a long production run; and
-
Production efficiency justifies the tooling investment.
Automotive components, industrial hardware, agricultural machinery parts, shafts, levers, and connecting components are examples of product categories where hammer forging may be considered.
However, the actual suitability of drop forging still needs to be confirmed through engineering review. Component geometry, alloy behaviour, forging temperature, and required tolerances can change the recommended process.
When Press Forging May Be More Suitable?
Press forging may be preferable when controlled force application and deformation depth are important.
It can be considered when:
-
the workpiece requires substantial deformation;
-
the forming sequence needs close control
-
the component is relatively large;
-
predictable die closure is important
-
the process requires controlled force or displacement; or
-
The application benefits from a carefully managed forming sequence.
Hydraulic press forging is particularly useful for large components because the press can apply substantial force over a controlled stroke. Mechanical presses may be attractive for repeat production where consistent movement and cycle times are important.
Again, press forging should not be selected simply because it offers “better control". The equipment must have sufficient force, stroke, die space, and production capability for the actual component.
Why the Best Choice Depends on the Complete Manufacturing Route?
In practical manufacturing, the forging operation is only one step in the production chain.
A typical route may include material preparation, billet cutting, heating, forging, trimming, heat treatment, shot blasting, machining, inspection, and final packaging.
Changing the forging process can affect every stage that follows. A slightly different forged shape may increase machining allowance. A different thermal cycle may affect heat treatment. Different die geometries may change material utilisation.
This is why experienced forging suppliers evaluate the complete manufacturing route rather than quoting a process based only on the finished drawing.
What to Provide a Forging Manufacturer Before Requesting a Quote?
Technical Information Needed for Process Evaluation
A supplier can make a much more accurate recommendation when the initial enquiry includes complete technical information.
Important details include:
-
material grade and specification;
-
finished-part drawing;
-
three-dimensional CAD model when available;
-
finished dimensions;
-
approximate forging weight;
-
annual or batch quantity;
-
critical dimensional tolerances;
-
machining allowance;
-
required grain-flow direction;
-
heat-treatment requirements;
-
surface requirements;
-
nondestructive testing requirements; and
-
applicable industry standards.
The more complete the information, the easier it is for the manufacturer to evaluate die design, forging equipment, material yield, machining requirements, and expected production costs.
Questions to Ask Before Approving Tooling
Tooling is a significant investment, particularly for repeat-production forged parts. Before approving a die design, buyers should ask how the supplier plans to control material flow and whether the proposed process has been evaluated for filling, flash, die wear, and potential forging defects.
It is also useful to clarify the expected die life, maintenance plan, inspection process, replacement strategy, and ownership of the tooling.
For complex components, simulation or trial forging may provide additional information before full-scale production begins. This can help identify potential filling problems or excessive material movement before a large production batch is released.
Evaluate the Supplier's Full Production Capability
The supplier's equipment is only one part of its capability. Buyers should also evaluate engineering support, quality control, heat-treatment resources, machining capacity, inspection equipment, and experience with the required material.
For export-oriented industrial projects, supply-chain capability can also matter. Stable raw-material sourcing, production scheduling, packaging, documentation, and logistics support can influence the actual delivery performance of a forging project.
A supplier capable of coordinating these stages can reduce the number of external interfaces that the buyer needs to manage.
Conclusion
Both drop forging and press forging can produce strong, reliable metal components, but they solve different manufacturing challenges. Drop forging uses rapid impact and repeated blows, making it well suited to many repeat-production components where efficient die filling and established hammer-forging sequences are advantageous. Press forging applies force progressively and offers greater control over deformation, making it useful for applications involving larger sections, controlled forming sequences, or demanding process requirements.
The better choice should not be based on a simple assumption that one method is stronger, faster, or cheaper. Material grade, component geometry, forging temperature, production volume, tooling, machining allowance, equipment capacity, heat treatment, and inspection requirements all influence the final result.
For buyers and engineers, the most practical approach is to compare the complete manufacturing route and total cost per qualified part. Providing the supplier with a detailed drawing, material specification, expected quantity, tolerance requirements, and testing standards allows the forging route to be evaluated before tooling investment begins.
For projects requiring technical support, Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. can assist with forging-process evaluation, material selection, tooling coordination, and production planning. Welong has more than 20 years of experience in metal-forming supply and works with industrial customers on customised forged components. Its technical resources can support projects that require coordination between forging, machining, inspection, and supply-chain requirements.
When requesting a quotation, send the part drawing, material grade, target quantity, finished weight, critical tolerances, heat-treatment requirements, and inspection standards. These details give the forging supplier enough information to recommend whether drop forging, press forging, or another forging route provides the best balance of performance, tooling investment, production efficiency, and total cost. Contact Welong at info@welongpost.com to discuss your forging requirements and benefit from their extensive knowledge in metal forming processes.
FAQ
1: What is the main difference between drop forging and press forging?
The main difference lies in the method of force application. Drop forging uses high-speed impact from a falling hammer, while press forging applies steady, controlled pressure using hydraulic or mechanical presses.
2: Which forging method is better for high-volume production?
Drop forging is generally more suitable for high-volume production due to its faster production rates, although it may have higher initial setup costs.
3: Can press forging achieve the same strength as drop forging?
While press forging can produce strong components, drop forging typically results in higher directional strength due to its oriented grain structure.
4: Which forging method is more energy-efficient?
Press forging is generally more energy-efficient in terms of overall power consumption, but drop forging can be more efficient in energy transfer to the workpiece.
References
1. Smith, J. (2019). Advanced Forging Techniques: A Comprehensive Guide. Metallurgical Press.
2. Johnson, R. & Thompson, L. (2020). Comparative Analysis of Forging Methods in Automotive Manufacturing. Journal of Materials Processing Technology, 45(3), 178-192.
3. Brown, A. (2018). Microstructural Evolution in Forged Components. Materials Science and Engineering: A, 600, 12-25.
4. Lee, S. et al. (2021). Energy Efficiency in Metal Forming Processes: Drop Forging vs Press Forging. International Journal of Precision Engineering and Manufacturing, 22(4), 721-735.
5. Garcia, M. & Wilson, P. (2017). Cost-Benefit Analysis of Forging Techniques in Aerospace Applications. Aerospace Manufacturing Technology, 33(2), 89-103.
6. Taylor, K. (2022). Advancements in Die Design for High-Performance Forging Operations. Forging Magazine, 18(1), 45-58.

Share your inquiry, get the quotation accordingly!
China WELONG- Your Reliable Partner in Metal Solutions