One of the most popular ways to make metal parts with complicated shapes, internal cavities and a variety of sizes is through the casting technique. Casting: The process of forming a component by pouring molten metal into a mould and allowing it to harden. Instead of cutting away material from a solid block. The process can be modified to cast iron, steel, aluminium, copper alloys, nickel alloys and a host of other technical materials. The properties of a casting process are influenced by far more than simply pouring molten metal into a mould. The mould material, pattern design, gating and feeding, melting technique, pouring temperature, solidification behaviour, cooling circumstances, heat treatment and inspection all influence the final casting. Casting is a large range of procedures that includes sand casting, investment casting, permanent mould casting, die casting, squeeze casting, centrifugal casting and other specialised methods, according to ASM International. It helps engineers and purchasing teams know these variances and makes it easier to select the right manufacturing path before tooling and production begin. The correct option relies on the geometry of components, material, manufacturing volume, dimensional requirements, surface finish, tooling budget and the level of inspection necessary for the finished part.
How Does the Casting Process Works?
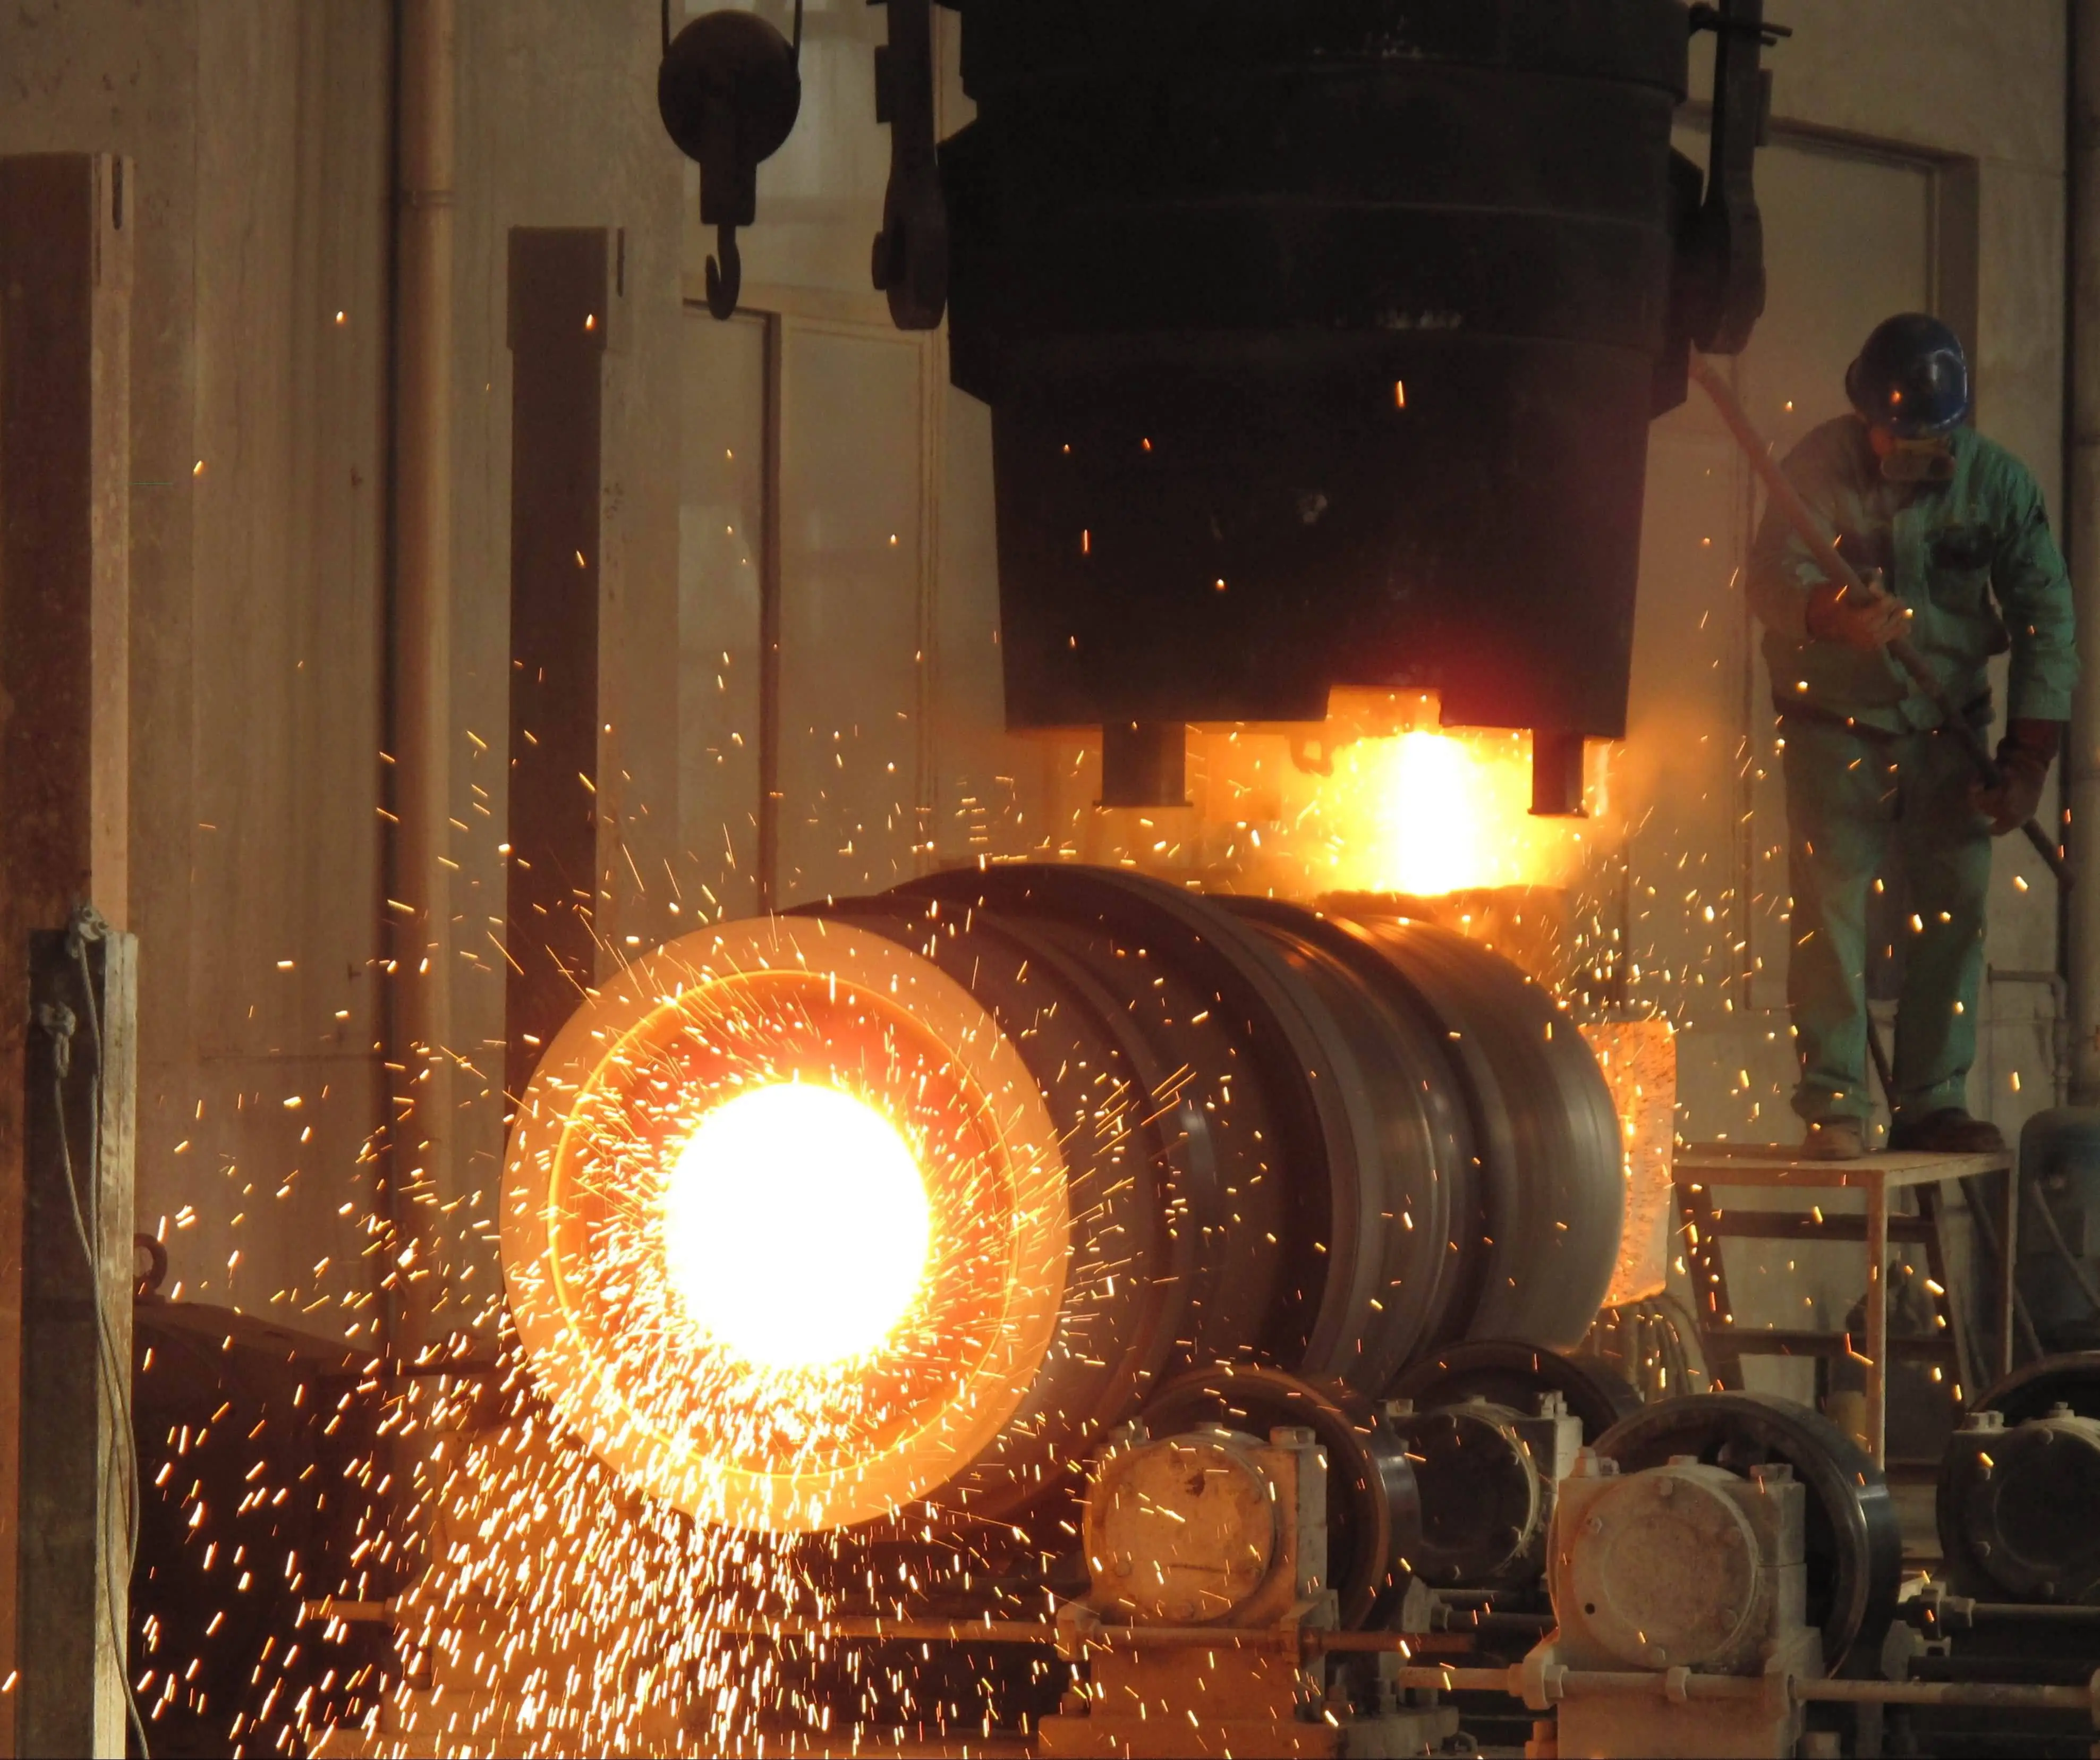
Though unique foundries employ diverse equipment and process controls, the order of most metal casting operations is alike. First the component geometry is transformed into an appropriate mould and pattern design. The alloy is next melted and conditioned and then transferred to the mould. The metal is then allowed to solidify in a controlled manner. The mould is then removed, the casting cleaned and inspected, and finishing or heat treatment applied as needed.
From Pattern Design to Finished Casting
And the quality of casting depends directly on the design of pattern and mould. Engineers need to examine the parting lines, draft angles, wall thickness, cores, gating, risers, machining allowances and locations of possible shrinkage concentration.
In filling, the molten metal must fill the cavity before excessive premature solidification occurs. The feeding mechanism should also supply enough liquid metal to make up for the contraction occurring during solidification. Poor filling or lack of feeding can help cause problems such as misruns, cold shuts or shrinkage cavities. The ASM references list the key parts of casting engineering as filling, feeding, solidification, and mould design.
When solidification is complete, the casting is removed from the mould. Depending on the technique, this can mean breaking away a sand mould, removing a ceramic shell, opening a permanent mould, or ejecting a component from a die. Further processes may include gate and riser cutting, shot blasting, grinding, machining, heat treating, painting, and dimensional inspection.
Why Temperature and Solidification Matter?
Temperature management is one of the main features of a good casting process. The metal must be fluid enough to fill the mould, but not so hot as to cause excessive oxidation, gas absorption or other metallurgical difficulties.
And solidification is really crucial. The rate of cooling influences the microstructure, the shrinkage behaviour and the characteristics of the final casting. The geometry of the part is also important, since normally thick sections will cool differently than thin sections. Imbalances in section thicknesses can create feeding problems and a greater risk of internal defects.
That’s why casting design cannot be divorced from process design. What appears simple from a machining point of view might be a lot of engineering to cast in a consistent manner.
Key Characteristics of Different Casting Methods
The diverse casting technologies have varied mould systems, pressures, tooling approaches, and production strategies. These differences define where each method is best suited.
Sand Casting
Sand casting uses moulds made of sand and a suitable binder system, which are expendable. It is one of the most versatile casting technologies since moulds may be used for relatively big components and complex geometries and do not require permanent metal tooling for each production run.
The method is applicable to numerous ferrous and nonferrous alloys. Cores are also used for forming internal channels, cavities and hollow parts. The technical references of ASM cover sand casting regarding pattern making, gating, feeding, moulding materials, and sand reclamation.
The biggest advantage is the flexibility. Sand casting is commonly used for big pieces, prototypes, replacement parts, and low to medium production volumes. Limitations - Rougher surface polish than some precision casting processes. - More variance in dimensions. Functional surfaces are consequently often subject to machining.
Investment Casting
Investment casting, or lost-wax casting, involves the use of a disposable pattern to produce a ceramic shell around the desired component geometry as part of the casting process. The design is removed, and molten metal is put into the ceramic mould.
This method is especially effective for complex forms, thin parts, difficult passageways, and parts where reduced machining will provide a production advantage. Pattern production, shell construction, dewaxing, burning, pouring, shell removal and finishing are part of the process. Investment casting is a specialised process that produces intricate components but demands careful attention to shell and pattern design. From ASM documentation.
Investment casting takes more tooling and pattern preparation and process steps than basic sand casting. It is thus chosen when the added processing is worth the geometric detail and dimensional control.
Die Casting
Die casting employs reusable metal dies and drives molten metal into the cavity under pressure. It is especially related to the production of large quantities of nonferrous parts, including numerous in aluminium, zinc and magnesium alloys.
The main advantage is repetition. Once the production tooling is qualified, die casting can create vast quantities of parts with consistent geometry and relatively quick cycle times. It is utilised for automotive, electronics, equipment and consumer goods components.
But die tooling is expensive to produce. Economics are very dependent on volume of production and design of components. A die-casting solution that makes economic sense for hundreds of thousands of parts may not be cheap for a short manufacturing run.
Permanent Mould, Centrifugal, and Squeeze Casting
Permanent-mould casting uses moulds that may be reused, and it is generally used for suitable nonferrous alloys. Reusable tooling can offer better repeatability and surface qualities than disposable sand moulds, but the tooling requirements are greater.
In centrifugal casting the rotational force causes the molten metal to be forced against the wall of the mould. It is especially connected with cylindrical or rotationally symmetrical parts such as certain pipes, sleeves and rings.
During solidification pressure can be applied by squeeze casting and is employed where enhanced density and mechanical performance are needed. These procedures are examples of why “casting” is not a single manufacturing technique. Casting references for ASM include permanent mould, centrifugal, squeezing, semisolid and a number of specialised casting methods.
Materials Commonly Used in Casting
The selection of materials and processes should be made collectively. Melting, fluidity, solidification, heat-treatment possibilities and expected attributes of the completed component are determined by the alloy.
Cast Iron and Steel
Cast iron is frequently used for housings, machine bases, automotive parts, pump bodies and other parts where castability and certain mechanical qualities are required. Varied grades have varied mixtures of strength, wear resistance, machinability and damping properties.
Steel castings are beneficial when better strength, toughness, temperature resistance or corrosion resistance are required. Suitable foundry routes can manufacture carbon steels, low-alloy steels, stainless steels and other grades. Steel casting engineering needs great attention to melting, design of mould and core, filling, feeding, solidification, heat treatment, and inspection.
Aluminium and Other Nonferrous Alloys
Aluminium alloys have a wide application range. They have strong castability, low density and a relatively low melting temperature, which makes them cast widely. Common casting methods include sand casting, permanent mould casting and die casting.
If the material and component requirements are compatible with the selected process, copper alloys, zinc alloys, magnesium alloys and nickel-based alloys can also be cast. The optimal procedure is a function of the mix of alloy, geometry, quantity, and desired qualities and not material name alone.
How to Select the Right Casting Process?
First, when selecting a casting technique, you should begin with the part, not the equipment. For example, a supplier may have state-of-the-art die-casting technology, but it does not mean die-casting is automatically ideal for a low-volume steel component.
Evaluate Geometry and Internal Features
Casting can typically make complex surface shapes effectively, but internal channels require cores or specific mould construction. Engineers should check wall thickness, section transitions, undercuts, holes, cavities, and machining areas before choosing a technique.
Filling and solidification are facilitated by uniform or suitably controlled wall sections. Sudden changes in section thickness tend to cause local temperature conditions which are detrimental to feeding and increase the probability of defects. Important design considerations in the casting process are the consistency of the ASM notes section and premature freezing.
Match Production Volume to Tooling Investment
Production volume has a substantial effect on process economics. Sand casting generally allows for more flexibility with tooling, while die casting needs a higher initial investment in equipment but can support efficient repeat production after the tooling is established and qualified.
Investment casting is more complex in process than these processes but less difficult than the other processes and is used when the detail of the component warrants the additional pattern and shell-making phases.
Purchasing teams should not ask for a universal break-even number, but rather a quotation that breaks out tooling, sample production, piece price, finishing, inspection, packing and shipping. This provides a more true representation of the entire landing cost.”
Define Quality and Inspection Requirements
1. Quality requirements must be set before production. 2. Specifications may include dimensional inspection, chemical composition, mechanical testing, hardness testing, surface inspection, radiographic testing, ultrasonic testing, magnetic particle inspection or dye penetrant testing according to application.
The classification of casting defects is sometimes done in groups such as: • Cavities • Discontinuities • Defective surfaces • Incomplete castings • Dimensional difficulties • Inclusions or structural anomalies Casting faults such as gas porosity, shrinkage, cold shuts, and others are listed by ASM International and must be watched throughout process design and inspection.
Casting Defects and Process Control
There is no casting procedure that is absolutely free of flaws. The task is to implement the process so that the known risks are handled and the resulting components conform to the approved specification.
Porosity and Shrinkage
Porosity may be caused by gas-related mechanisms or other process circumstances that create voids within the casting. Shrinkage can occur due to metal contraction during solidification and due to the feeding mechanism not being able to adjust for the contraction well enough.
Both problems demand more than a final inspection. In developing the process, gating and riser design, melt treatment, pouring practice, mould design, and solidification behaviour should be taken into account.
Cold Shuts, Misruns, and Inclusions
Cold shuts occur when two metal fronts do not properly fuse together during the filling process. • Misruns: When the molten metal fails to entirely fill the mould hole before it solidifies and can no longer flow.
Inclusions may be oxides, slag, mould materials or other foreign material entering or persisting in the molten metal. Appropriate melting practice, melt cleanliness, mould preparation and controlled filling are hence preventive measures.
Inspection Should Match Application Risk
Not every casting must be subject to the same inspection programme. For example, a decorative component may require simply dimensions and visual inspection, whereas a pressure-containing or safety-sensitive component may require rigors nondestructive examination and mechanical testing.
This is vital to know while evaluating quotes from suppliers. The unit price may be lower, but the whole production cost may not be if it does not include the inspection, testing, machining or documentation required by the final application.
Casting vs. Forging: When the Processes Differ
Casting and forging are both established metal manufacturing methods, but they solve different engineering problems.
Casting is particularly useful when a component requires complex geometry, internal cavities, integrated features, or shapes that would require substantial material removal if machined from solid stock. Forging mechanically deforms heated or otherwise workable metal and is often selected when the required geometry and performance characteristics favour a wrought manufacturing route.
The appropriate choice should be based on component geometry, required mechanical properties, production volume, material, tolerances, and downstream machining requirements rather than assuming that one process is universally superior.
Conclusion
Understanding casting process characteristics and types provides a practical foundation for selecting the right manufacturing route for metal components. Sand casting offers flexibility for large, complex, and lower-volume parts; investment casting is suitable for detailed geometries where precision and reduced machining are important; and die casting can provide efficient repeat production when volume and tooling economics justify the investment. Permanent mould, centrifugal, squeeze, and other specialised processes expand the available options for particular materials and component requirements. The most effective selection process starts with the component itself. Geometry, material, annual volume, dimensional tolerance, surface finish, mechanical requirements, tooling budget, post-processing, and inspection standards should all be evaluated together. Casting quality also depends on process engineering, especially mould design, gating and feeding, melting practice, temperature control, and solidification. For procurement teams, supplier evaluation should therefore extend beyond unit price. A reliable casting partner should be able to understand technical drawings, recommend a suitable process, control tooling and production, provide appropriate inspection documentation, and communicate clearly throughout development and mass production. When these factors are considered together, the casting process can provide an efficient manufacturing route for components ranging from large industrial castings to highly detailed precision parts.
FAQ
1. What factors determine the most suitable casting process?
The main factors include component geometry, material, production volume, dimensional requirements, surface finish, tooling budget, mechanical properties, post-processing, and inspection requirements. These factors should be evaluated together because changing one requirement can affect the most economical casting route.
2. Is sand casting suitable for large components?
Yes. Sand casting is widely used for components ranging from relatively small parts to large industrial castings. Its expendable mould system provides substantial flexibility in component size and geometry, although the achievable dimensional accuracy and surface finish depend on the moulding system, pattern, alloy, and foundry process controls.
3. When should investment casting be considered?
Investment casting is worth considering when a component has complex geometry, detailed features, thin sections, or other characteristics that make conventional machining or simpler casting methods less attractive. It can reduce machining requirements, although its multi-stage pattern and ceramic-shell process can increase production complexity.
4. What causes common casting defects?
Common defects can be associated with gas, shrinkage, incomplete filling, poor fusion, inclusions, dimensional problems, and surface conditions. The specific cause depends on the alloy, mould, filling conditions, feeding design, solidification behaviour, and production controls. ASM International classifies casting imperfections into several broad categories and discusses defects including gas porosity, shrinkage, and cold shuts.
Partner with Welong for Your Casting Process Requirements
Welong supports customers requiring customised cast components and related manufacturing coordination. For a new project, buyers can provide a drawing, sample, or 3D model together with the required material, quantity, tolerances, inspection specifications, and delivery requirements. The engineering and production teams can then evaluate the appropriate casting process, tooling approach, finishing requirements, and quality-control plan before production. This approach helps align the manufacturing method with the actual requirements of the component instead of selecting a process based only on the initial unit price. For procurement teams sourcing cast components for international projects, a clear technical review at the beginning can help reduce unnecessary tooling changes, quality issues, and communication gaps during production. Contact us at metal@welongpost.com to discuss your project requirements and discover how our expertise can enhance your supply chain success.
References
1. Campbell, John. "Complete Casting Handbook: Metal Casting Processes, Techniques and Design." 2nd Edition, Butterworth-Heinemann, 2015.
2. Beeley, Peter R. "Foundry Technology." 2nd Edition, Butterworth-Heinemann, 2001.
3. American Foundry Society. "Casting Design and Performance Standards for Industrial Applications." AFS Technical Publication, 2020.
4. Brown, John R. "Foseco Non-Ferrous Foundryman's Handbook." 11th Edition, Butterworth-Heinemann, 1999.
5. Stefanescu, Doru Michael. "Science and Engineering of Casting Solidification." 3rd Edition, Springer, 2015.
6. Investment Casting Institute. "Investment Casting Design Guidelines and Quality Standards." ICI Technical Manual, 2019.