Cold chamber die casting is a commonly used manufacturing process for metal parts requiring a combination of complicated shapes, dimensional stability, mechanical strength and efficient, high-volume production. Unlike hot chamber die casting, the procedure employs a separate melting furnace and injects a measured amount of molten metal into the shot sleeve before injection. This makes the procedure particularly well suited to aluminium and other metals not generally handled on a continuously submerged hot chamber injection system. Today, cold chamber die casting is used for components in automotive systems, industrial equipment, electronics, electrical items, transportation equipment and other engineered applications. Its value is not merely to quickly produce a metal shape. When correctly managed with regard to the alloy, die design, injection settings, cooling system, and inspection procedures, the process can result in reproducible dimensions and a favourable ratio of component weight, strength, and production efficiency. For purchasers assessing this manufacturing method, understanding how the equipment works is as crucial as understanding where cold chamber die casting fits into a production strategy.
How Does the Cold Chamber Die Casting Process Work?
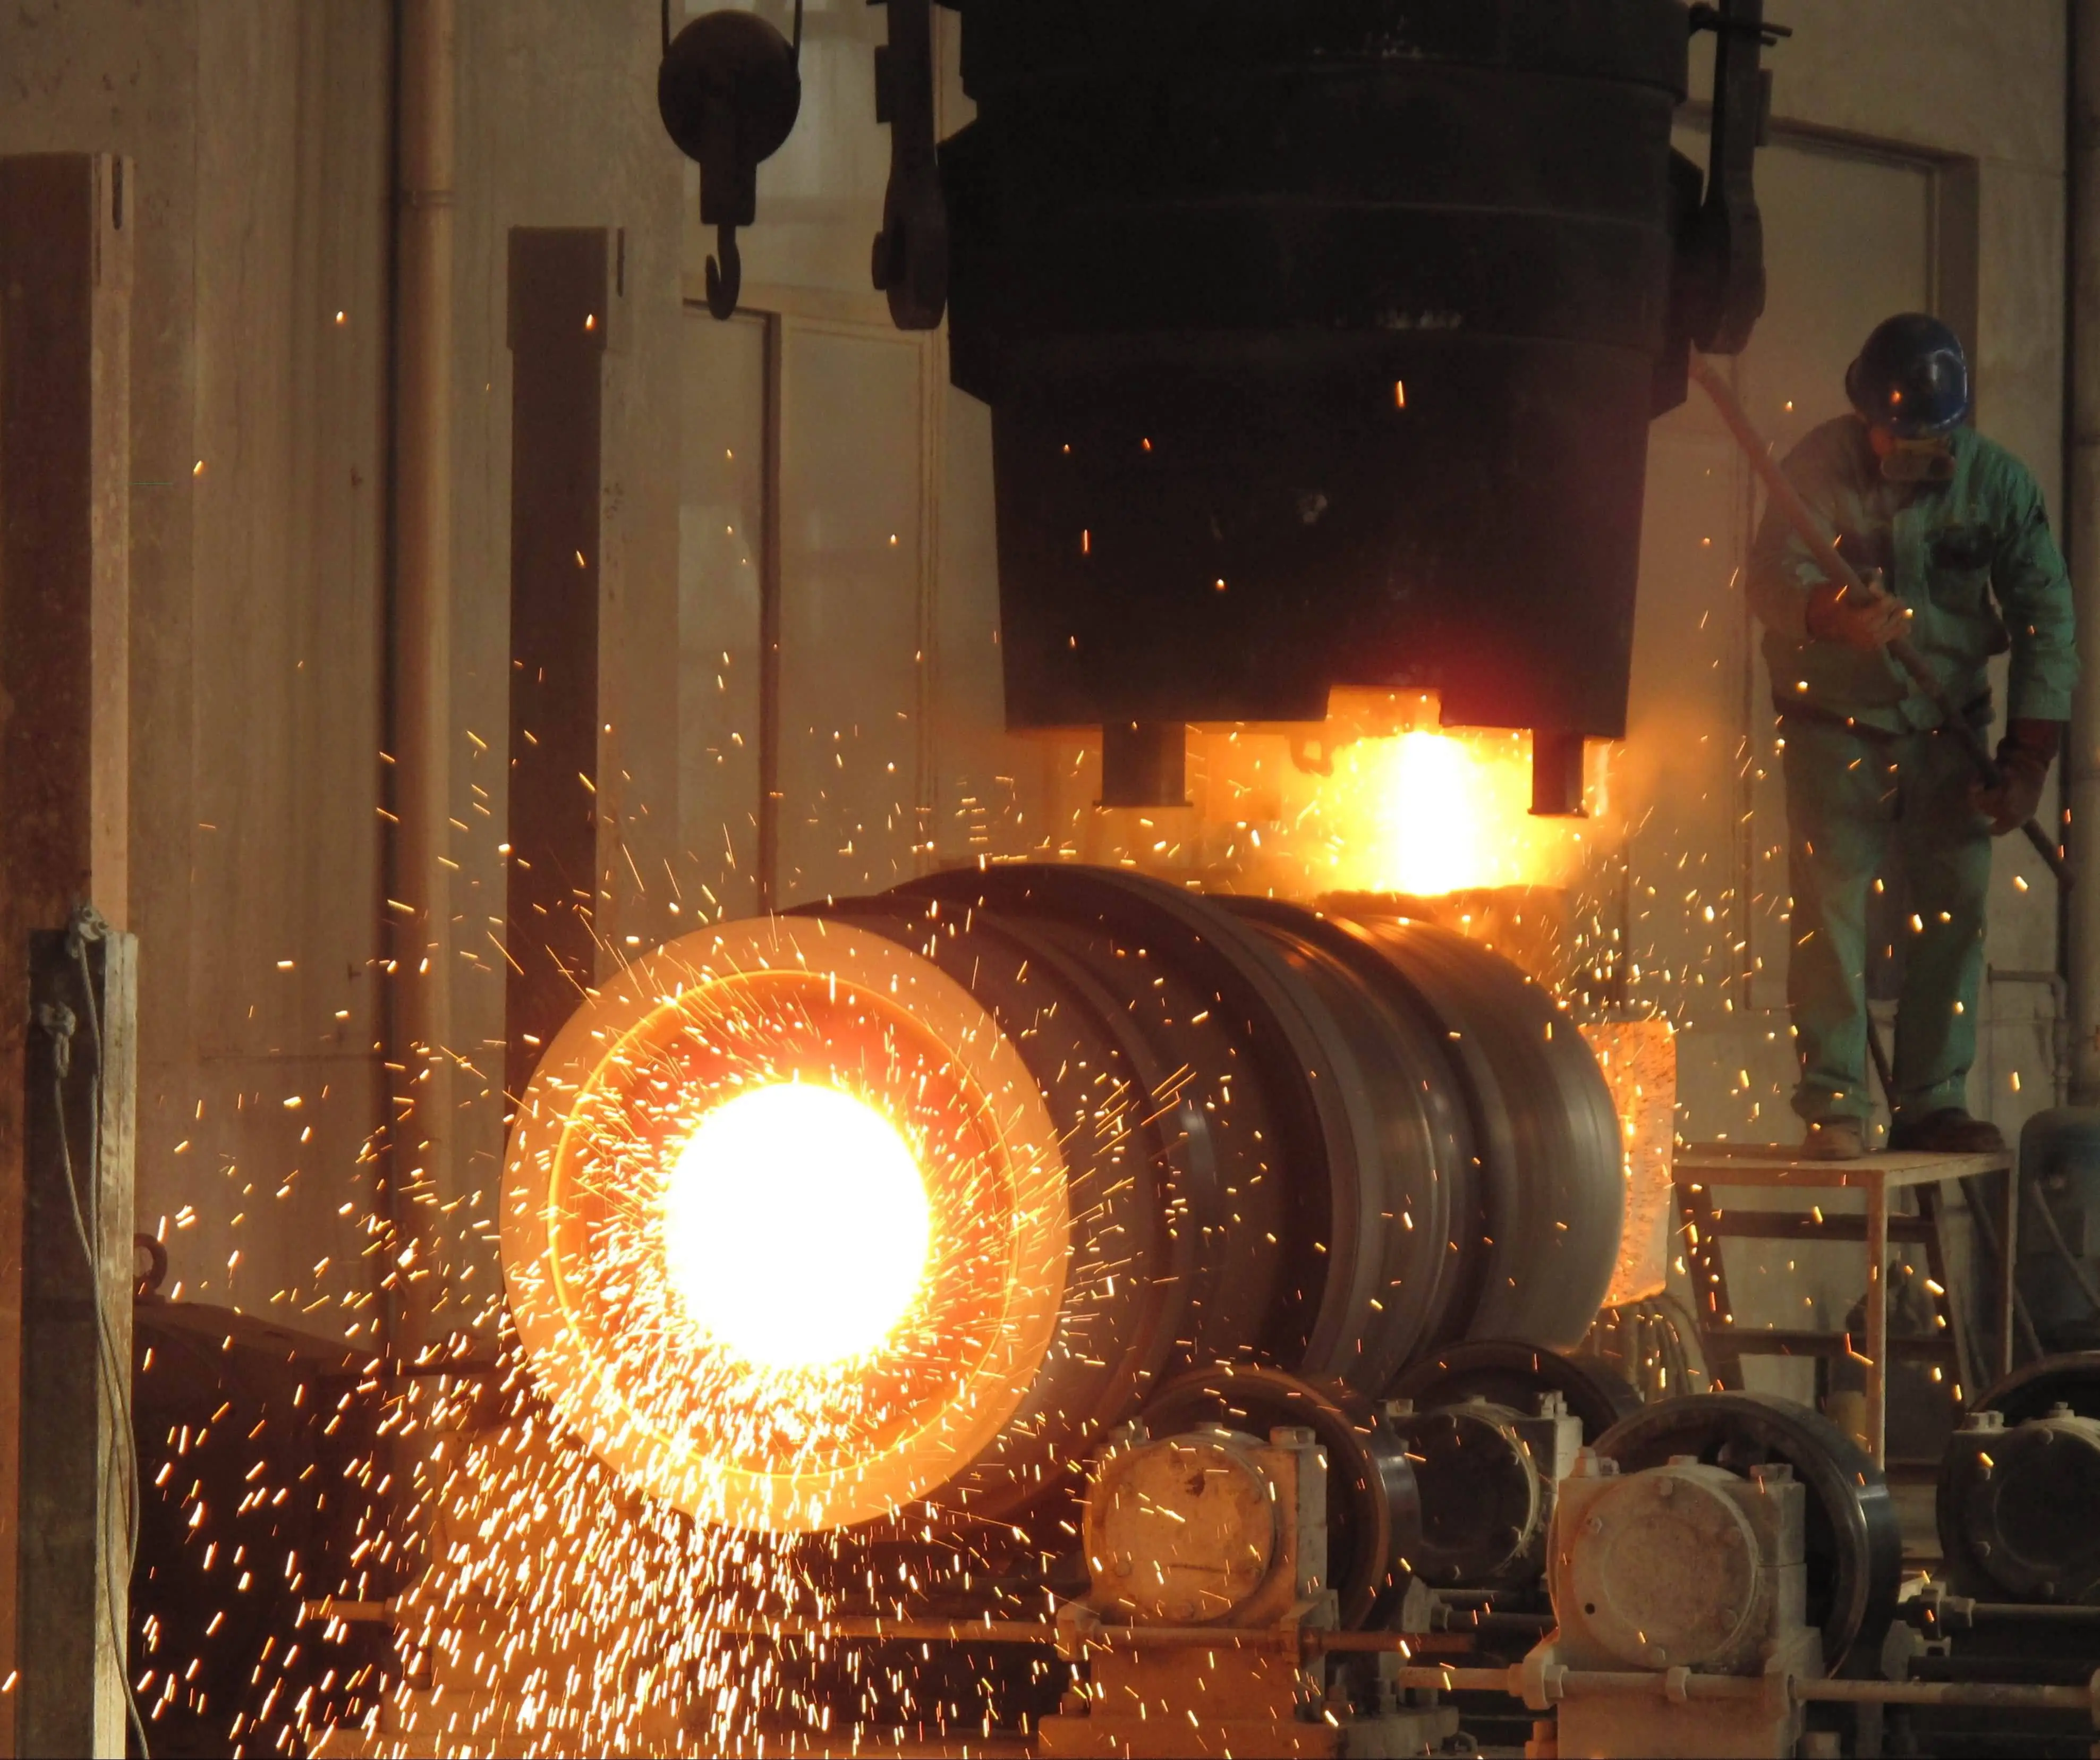
The basic premise is rather simple, yet each stage has a direct impact on the final product quality. The molten metal is produced in a separate furnace and then poured into the shot sleeve. Then the plunger forces the metal into the die cavity with a high pressure. The metal fills the desired geometry and solidifies fast.
From Alloy Melting to Die Filling
The specified alloy is melted in a furnace. This is separate from the die casting process. The temperature is controlled as per the alloy standard and production needs. Operators or automated devices then drop a pre-measured shot of molten metal into the shot sleeve.
Normally the injection system works in controlled stages. In the first movement, the plunger advances at a relatively slow speed to facilitate control of the metal flow and decrease the entrainment of air. The injection speed then increases as the molten metal enters the runner system and die cavity.
After the cavity has been filled, intensification pressure can be applied to compensate for solidification shrinkage and to maintain contact of the molten metal with the die surfaces. The component remains in the die until sufficient solidification has taken place to allow ejection.
This is done for each cycle of production. All of these, furnace temperature, metal transfer, injection parameters, die temperature, lubrication and ejection may be monitored and managed to provide better repeatability in automated manufacturing.
Why the Separate Chamber Matters?
The distinguishing characteristic of the process is the separation of the melting furnace and the injection chamber. This configuration is significant for the processing of alloys which have properties that prevent continued contact with hot chamber injection components.
Aluminium alloys belong to the most frequently used material groups for cold chamber die casting. Copper-based alloys can also be worked with the proper equipment and die design. Their greater working temperatures can also raise the thermal demands placed on the tooling and machine.
Cold chamber equipment can also be used for magnesium alloys where the method is suitable for the material characteristics and the production needs. The alloy selection should always be considered together with casting temperature, fluidity, die temperature, mechanical requirements and production volume.
Materials Commonly Used in Cold Chamber Die Casting
The selection of material will influence the completed component, tooling needs, cycle conditions, machining requirements and overall production cost.
Aluminium Alloys for Lightweight Components
Aluminium is commonly connected with cold chamber die casting because of its comparatively low density and its useful strength, corrosion resistance, and high castability. Typical commercial die-casting alloys include grades like A380 and A3831. The specification is dependent on the application and qualities required.
When the geometry and service requirements are consistent with the technique, aluminium die casting can be used for automotive housings, brackets, covers, structural components, motor housings, pump bodies, and other complex parts.
Finally, the qualities of an aluminium casting are not only a function of the nominal alloy composition. The completed part might be influenced by filling circumstances, cooling behaviour, porosity, heat treatment if appropriate, machining and inspection.
Copper and Magnesium Alloy Considerations
Copper alloys can be selected when some qualities, like electrical conductivity, thermal conductivity, strength, or wear resistance, are needed. However, their processing requirements can be more demanding than those of the conventional aluminium die casting alloys.
Magnesium alloys are low-density materials for applications where component weight is a critical factor. They demand meticulous supervision of material handling, process parameters, die design and production circumstances.
For procurement teams the main idea is that an alloy should not be chosen only based on the material datasheet. The supplier must verify that the specific alloy can be reliably cast into the required component geometry and production environment.
Where Cold Chamber Die Casting Is Commonly Applied?
The most powerful applications are typically those with relatively high production numbers, predictable component geometry, and a requirement for effective material utilisation.
Automotive and Transportation Components
Cold chamber die casting is one of the key application areas in automotive manufacture. Aluminium castings are utilised in gearbox housings, motor housings, brackets, covers, structural supports, pump bodies and a wide range of other components.
This is a very beneficial approach when designers want to merge numerous geometric characteristics into a single component. Features like ribs, bosses, mounting points, passageways, etc. can often be integrated into the casting design and may reduce the number of components that are created separately.
But it doesn’t mean every engine or powertrain component should be immediately die-cast. For parts exposed to rigorous mechanical loads, high temperatures, pressure or fatigue, a different casting technique, forging, machining or another manufacturing path may be necessary. Tooling investment should therefore be judged on the basis of the demands of the application.
Industrial Machinery and Equipment
Industrial equipment makers employ die-cast components for housings, covers, brackets, valve bodies, pump components, gear housings and other designed parts.
This is where repeatability can be so helpful. Once the production process is stabilised, huge quantities of components with uniform geometry can be manufactured, while machining can be restricted to important functioning surfaces.
This can facilitate assembly for equipment manufacturers that buy components from an outside supplier since mounting locations and mating characteristics can be maintained within specified dimensional specifications.
Electronics, Electrical, and Thermal Management Products
Aluminium die casting is also utilised in electrical and electronic equipment, where lightweight housings, heat dissipation, electromagnetic shielding and dimensional integration are critical.
Motor housings, electronic enclosures, heat-management components and structural frames can include thin walls, ribs, bosses and mounting elements that ordinarily might require numerous discrete manufacturing operations.
The actual thermal performance of a die-cast part is a function of the selection of alloy, wall thickness, shape, surface condition and the design of the overall thermal system. Therefore, die casting must be seen as part of the total product design rather than as an independent manufacturing decision.
Design Factors That Influence Cold Chamber Die Casting
Good part design can significantly reduce tooling problems, secondary machining, and production instability.
Wall Thickness, Draft, and Fillets
Uniform wall thickness is generally preferable because large variations can create differences in solidification behaviour and increase the possibility of defects. Thin sections may be achievable, but the practical limit depends on alloy, component geometry, die design, filling conditions, and machine capability.
Draft angles should be incorporated where needed to allow the casting to release from the die. The appropriate value depends on the surface finish, geometry, depth, alloy, and whether a particular surface is textured or machined afterward.
Fillets are also important. Sharp internal corners can concentrate stress and interfere with metal flow. Proper radii generally support smoother filling and can improve die durability.
Runners, Gates, and Overflow Design
The runner and gate system determine how molten metal enters the cavity. A poorly designed gating system can produce turbulence, incomplete filling, cold shuts, excessive air entrapment, or uneven solidification.
Overflow features and vents can be used to help manage air and excess material during filling. These features should be considered during the initial tooling design rather than added as an afterthought.
For complex parts, simulation can help engineers examine filling behaviour, temperature distribution, and potential solidification issues before the die is manufactured. This can reduce the number of tooling modifications required during sampling.
Quality Control and Common Casting Defects
Quality assurance in cold chamber die casting requires more than final dimensional inspection. Process control and defect prevention should begin during material preparation and continue through production and final inspection.
Porosity, Cold Shut, and Incomplete Filling
Porosity can occur for different reasons, including entrapped gas and solidification shrinkage. The likelihood and location of porosity are influenced by filling conditions, die temperature, alloy characteristics, venting, gating, and intensification pressure.
Cold shuts can occur in cold chamber die casting when separate metal fronts fail to fuse properly. Incomplete filling may result when the metal loses sufficient fluidity before the cavity is fully filled.
The correct corrective action depends on the underlying cause. Simply increasing injection pressure is not necessarily the right solution. Engineers may need to evaluate gate location, injection speed, die temperature, venting, alloy temperature, or cavity geometry.
Inspection and Traceability
A professional supplier should establish inspection requirements according to the component's function. Typical controls may include dimensional inspection, visual inspection, material verification, hardness testing, density evaluation, and other testing methods where required.
For critical applications, buyers may also request X-ray or other non-destructive testing to evaluate internal casting quality. The inspection method should be selected according to the customer's drawings, specifications, industry requirements, and risk profile.
Material and production traceability are equally important for long-term supply. Lot information, inspection records, process documentation, and sample approval records help buyers investigate quality issues and maintain consistent production standards.
Cold Chamber Die Casting Compared with Other Processes
No manufacturing process is ideal for every component. The appropriate choice depends on part geometry, alloy, annual volume, dimensional requirements, tooling investment, and secondary processing.
Cold Chamber vs. Hot Chamber Die Casting
The main distinction is the relationship between the melting furnace and injection system. Hot chamber machines keep the injection mechanism in contact with molten metal, while cold chamber machines receive a separate charge of molten metal for each shot.
This makes cold chamber equipment suitable for many aluminium alloys and other materials that are less suitable for conventional hot chamber processing.
Hot chamber die casting can offer very fast cycle times for compatible lower-temperature alloys. Cold chamber systems, however, provide access to material groups that expand the range of potential applications.
Cold Chamber Die Casting vs. Sand Casting
Sand casting can accommodate a broad range of alloys and larger component geometries and can be economical for lower-volume production. However, it generally requires more extensive finishing and machining when compared with a properly designed high-pressure die casting process.
Cold chamber die casting becomes increasingly attractive when production volume is high enough to justify dedicated tooling and when repeatable geometry is important.
The decision should therefore be based on total manufacturing cost rather than casting price alone. Tooling, machining, finishing, scrap, inspection, and production volume all need to be considered.
How to Select a Cold Chamber Die Casting Supplier?
Choosing the right supplier can have as much influence on project success as the initial process selection.
Engineering and Tooling Capability
A capable supplier should be able to review the customer's drawings before tooling begins. A Design for Manufacturability (DFM) review can identify areas such as difficult wall transitions, insufficient draft, problematic gate locations, unnecessary machining allowances, or features that could increase tooling complexity.
The supplier should also be able to explain the proposed alloy, die construction, injection strategy, cooling arrangement, trimming process, and machining requirements.
This engineering discussion is particularly important for new products because design changes are generally easier and less expensive before the die has been manufactured.
Quality Systems and Production Capacity
Buyers should evaluate the supplier's quality management system, inspection equipment, production capacity, and ability to maintain traceability throughout the order.
ISO 9001 certification can provide evidence of an established quality management framework, but certification alone should not be treated as proof of product-specific capability. Buyers should also review sample inspection reports, process controls, equipment capability, and relevant experience with similar components.
Production capacity should match expected demand. A supplier that can produce prototypes but cannot support the required annual volume may create supply problems later. Conversely, a supplier with extensive capacity may not be the right choice if the project requires frequent engineering changes and low-volume flexibility.
Cost Factors Buyers Should Consider
The price of a die-cast component is influenced by more than the alloy price.
Tooling is often a significant initial expense, especially for components requiring multiple slides, complex cores, special cooling channels, or tight dimensional control. Part geometry also affects cycle time, trimming, machining, and inspection requirements.
Production volume has a major effect on the economics of the process. A high-volume programme can spread tooling costs across a large number of components, making cold chamber die casting more competitive.
Secondary operations should also be included in the quotation. CNC machining, deburring, surface treatment, heat treatment where applicable, leak testing, assembly, and special inspection can substantially change the final unit cost.
For an accurate comparison, buyers should request a quotation that clearly separates tooling, casting, machining, finishing, inspection, packaging, and transportation where relevant.
Conclusion
Cold chamber die casting is a versatile manufacturing process for producing high-volume metal components from materials such as aluminium and selected copper and magnesium alloys. Its separate melting and injection arrangement makes it particularly suitable for alloy groups that are not well suited to conventional hot chamber systems. The process can provide repeatable dimensions, complex geometries, efficient production, and opportunities to integrate multiple features into a single component. However, the final result depends heavily on alloy selection, die design, gating, injection parameters, cooling, inspection, and secondary machining. For buyers, the most important step is to evaluate the entire manufacturing solution rather than focusing only on the quoted casting price. A supplier with appropriate engineering experience, tooling capability, quality controls, production capacity, and communication processes can help reduce avoidable tooling changes and improve consistency during mass production.
FAQ
1. What materials can be used for cold chamber die casting?
Aluminium alloys are among the most common materials used in cold chamber die casting. Selected magnesium and copper alloys can also be processed when the equipment, tooling, and process parameters are appropriate. The final material choice should be based on the required mechanical, thermal, electrical, corrosion, and dimensional characteristics of the component.
2. What types of parts are suitable for cold chamber die casting?
Typical applications include automotive housings, motor components, brackets, covers, pump bodies, industrial equipment components, electronic enclosures, and other relatively high-volume components with repeatable geometry. Parts with extremely demanding service conditions may require another manufacturing process or a combination of casting and machining.
3. Is CNC machining required after cold chamber die casting?
Not always. Many features can be incorporated directly into the casting, but critical mating surfaces, holes, threads, sealing areas, and tight-tolerance features may require CNC machining. The amount of secondary machining should be considered during the initial part design and quotation stage.
4. How can buyers evaluate a die casting supplier?
Buyers should review the supplier's relevant manufacturing experience, engineering capability, tooling resources, quality management system, inspection equipment, production capacity, material traceability, and ability to support sampling and mass production. It is also useful to request DFM feedback, sample inspection reports, and a clear breakdown of tooling and production costs before placing an order.
What information should be provided when requesting a quotation?
A useful RFQ for cold chamber die casting should include the 2D drawing, 3D model when available, material specification, estimated annual volume, initial order quantity, required tolerances, surface treatment, machining requirements, inspection requirements, packaging expectations, and target delivery schedule. Providing complete information allows the supplier to evaluate tooling and production requirements more accurately. Contact us at metal@welongpost.com to discuss your specific requirements and receive detailed quotations.
References
1. American Foundry Society. "Die Casting Process Fundamentals and Applications." AFS Technical Publication, 2022.
2. Metals Handbook Committee. "Casting Processes and Equipment." ASM International Handbook Series, Volume 15, 2021.
3. North American Die Casting Association. "Product Design Guidelines for Die Casting Manufacturing." NADCA Technical Standards, 2023.
4. Society of Manufacturing Engineers. "Advanced Manufacturing Processes for Automotive Applications." SME Technical Paper Series, 2022.
5. International Journal of Manufacturing Technology. "Quality Control Methods in High-Pressure Die Casting Operations." Academic Press Publishing, 2023.
6. Industrial Manufacturing Research Institute. "Comparative Analysis of Metal Casting Technologies." Technical Research Report, 2022.