About the Characteristics of Sand Casting Process
When manufacturers need to produce metal components with complex geometries, large dimensions, or relatively low-to-medium production volumes, sand casting remains one of the most practical casting methods available. Sand casting differs from procedures that use permanent metal dies in that it makes a mould around a pattern and destroys the mould after the metal has set. This allows great flexibility in the process for various component designs, materials and production needs. The underlying premise is simple enough, but to get a reliable casting takes a lot more than just pouring molten metal into sand. The final part is affected by pattern design, qualities of moulding sand, cores, gating and risering, alloy chemistry, pouring temperature, solidification behaviour, and inspection. The foundry must control collectively these variables to obtain the requisite dimensional precision, mechanical qualities, surface condition and internal quality. “Another key feature is the wide range of materials and sizes. The procedure can be applied to cast iron, carbon and alloy steels, stainless steels, aluminium alloys, copper alloys and other casting materials, depending on the equipment and process competence of the foundry. Components can be anything from very big industrial castings to relatively little pieces. That is why engineers, purchasing teams, product designers and manufacturers considering multiple manufacturing methods need to grasp the features of sand casting.
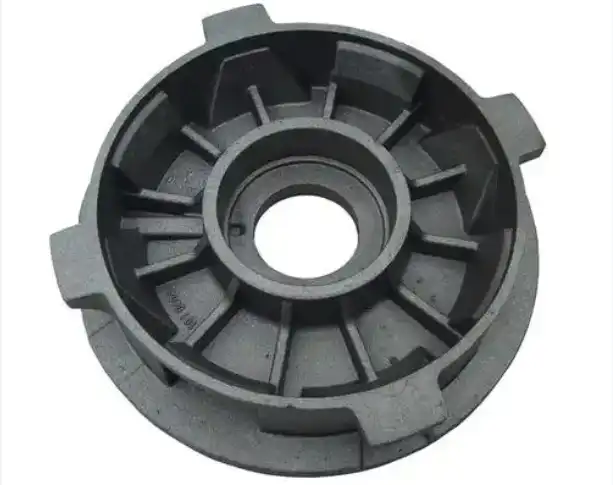
Why Does Sand Casting Remain a Flexible Manufacturing Process?
Lower tooling requirements for many production applications
One of the major reasons manufacturers still utilise sand casting is that the tooling approach is relatively adaptable. A lot of sand-casting applications do not need a substantial investment in a permanent metal mould as compared to permanent mould operations like die casting. A pattern forms the hollow, and the mould can be broken away after casting.
This quality can be especially beneficial for prototypes, replacement components, customised industrial parts, and production runs where the quantity needed does not warrant expensive permanent tooling. Sand casting is not automatically regarded as the lowest cost choice in every case, as pattern costs can still vary greatly depending on the component geometry, pattern material, dimensional requirements and degree of automation.
The economic benefit is even larger when the design might vary during the product development. Instead of redesigning an expensive permanent die, the producer can change the pattern. But the entire manufacturing cost should also include pattern development, mould preparation, cores, melting, polishing, inspection, machining and transportation.
Broad material and component size capability
Another important feature of sand casting is its capacity to accommodate a wide range of alloys and part sizes. While cast iron is most frequently cast in sand moulds, the method can be used to cast steel, stainless steel, aluminium, copper alloys and other metals if proper moulding, pouring and metallurgical controls are employed.
The procedure can also be applied to components with large differences in weight and geometry. Big pump casings, machine bases, valve bodies, engine parts, components of industrial equipment and other heavy castings can be manufactured by means of well-designed sand moulds and cores.
There is no single restriction for the process; the real size limit is decided by the foundry. The largest feasible casting size is limited by melting capacity, mould equipment, flask size, hoisting system, pouring facilities, heat-treatment equipment, and inspection facilities.
For the customer this means that the real production capacity of a foundry should be tested, rather than assuming that any sand-casting supplier can make a large or heavy component.
Adaptability to complex geometries
Sand moulds can yield shapes that would be impossible to produce by conventional machining alone. Cores and good pattern design can be used to include internal channels, cavities, bosses, recesses and other features in a casting.
Cores are particularly crucial if a component has internal voids that cannot be created directly by the external mould cavity. The core is placed into the mould before pouring so that the molten metal freezes around it and gives the proper interior geometry.
At the same time, design flexibility does not mean that any shape is equally suited for casting. Sudden changes in wall thickness, abrupt corners, isolated heavy portions, and poorly designed transitions might increase the tendency for shrinkage, distortion, or other casting difficulties. A good sand casting design thus addresses how the liquid metal will fill the mould and how the part will solidify.
How Does Process Control Influence Sand Casting Quality?
Pattern, mould, and core preparation
The quality of a casting begins before the molten metal enters the mould. Pattern dimensions shall include allowances for such elements as shrinkage of metal and, where appropriate, allowances for machining. The design must also be capable of being made and withdrawn from the mould without injury to the cavity.
The properties of the moulding sand, such as grain size, permeability, moisture content, strength and compactability, have to be properly controlled. The optimum values depend on the metal cast and the moulding system. Pouring too weak of a mould may cause it to shatter or degrade. Poor permeability might result in the gases created during moulding and pouring being trapped and causing problems.
Core production also needs attention. Cores must have sufficient strength and dimensional stability but also enable gases to escape during casting. Core positioning is also an important consideration since even a minor displacement might modify wall thickness or affect the final dimensions of an internal route.
These facts show why sand casting is not merely a process of making a cavity in sand. To be consistently good, you need to control the entire mould system.
Gating and riser design
The gating system regulates the flow of molten metal into and through the mould. Its design impacts the filling rate, turbulence, temperature distribution and potential of entrainment of air or pollutants.
Risers have another purpose. Many alloys contract in bulk as the molten metal solidifies. A properly built riser supplies additional liquid metal to make up for shrinkage in locations that would be otherwise internally deficient.
Therefore, the interdependence of gating, risering, casting geometry and solidification behaviour is important for the quality of castings. Foundries can employ casting simulation software to check the filling and solidification of parts before going into production, especially for complex or high-value components.
Industrial buyers are better off asking a supplier if they do process simulation or documented casting process development than comparing pricing offered.
Control of alloy chemistry and pouring conditions
The state of the molten metal directly influences the performance of the casting. Foundries may check chemical composition and modify alloy chemistry to achieve the needed standard before pouring. Additional processing may be required to control inclusions, dissolved gases or other metallurgical properties depending on the material.
Another crucial variable is the temperature of the pour. If the temperature of the metal is too low, premature solidification may interfere with the filling of the mould. If it is too high, it may enhance oxidation, mould-metal reactions, or other undesirable reactions.
Thus, the pouring procedure should be developed on the basis of the alloy, casting geometry, mould properties and production equipment. For parts that must meet defined mechanical or dimensional standards, consistency from batch to batch is critical.
What Surface Finish and Accuracy Can Be Expected?
Surface condition of as-cast components
One notable restriction of sand casting is that the as-cast surface is usually less smooth than that produced by methods like as-investment casting or high-pressure die casting. The exact result depends on the moulding sand, binder system, pattern quality, mould preparation, alloy and foundry procedure.
However, the somewhat rough as-cast surface does not mean that the method is not suited for industrial components. Many castings are designed with machining allowances on key areas. The appropriate final state can then be obtained by shot blasting, grinding, machining or other finishing operations after casting.
Thus, the comparison should be made on the basis of the full manufacturing path and not only on the as-cast surface. In case of a part with several precision interfaces, for example, the vendor must guarantee which surfaces will be machined and what dimensional tolerances can be achieved after machining.
Dimensional accuracy and machining allowances
There are several factors affecting the accuracy of sand casting, such as pattern precision, mould stability, alloy shrinkage, temperature conditions, core placement and the shape of the casting. Distortion and non-uniform solidification can affect final dimensions and may need to be considered more carefully for larger or more complicated components.
For areas requiring stricter tolerances, machining allowances are usually integrated into the casting design. This gives sufficient material for later machining without having to deal with unwanted surplus metal.
It is useful for procurement purposes to establish the crucial dimensions separately from the general casting dimensions. The supplier should be able to determine which dimensions are regulated in the as-cast condition and which ones are obtained after machining.
This way, the casting process is more directly connected to the specification of the final component.
Which Casting Defects Need to Be Controlled?
Porosity, shrinkage, inclusions, and misruns
Like other metal-forming processes, sand casting can produce defects if process variables are not properly controlled. Gas-related porosity can occur when gases become trapped in the metal or cannot escape through the mould system. Shrinkage defects may develop when insufficient liquid metal is available to compensate for contraction during solidification.
Inclusions can result from oxides, slag, refractory material, or other foreign matter entering the casting. Misruns and cold shuts may occur when molten metal loses too much heat or when mould filling is not properly controlled.
These defects do not have a single cause. The solution may involve changes to the mould, gating system, riser design, pouring practice, alloy treatment, or process parameters.
This is why experienced foundries generally approach defect control as a process-engineering issue rather than relying only on final inspection.
Inspection and verification after casting
Inspection requirements should be established according to the function and specification of the component. Visual inspection can identify obvious surface problems, while dimensional inspection verifies critical measurements against drawings or agreed specifications.
For components where internal quality is important, non-destructive testing can provide additional information. Depending on the material and component geometry, common methods include radiographic testing, ultrasonic testing, magnetic particle testing, and liquid penetrant testing.
Mechanical testing and chemical analysis may also be required when material certification is part of the purchasing specification. Heat-treatment records, dimensional inspection reports, and other quality documentation can provide additional traceability for industrial applications.
The appropriate inspection plan should be agreed before production rather than added only after a defect has been discovered. This is especially important for components used in demanding machinery, pressure-related equipment, transportation systems, or other applications with defined material and quality requirements.
What Environmental Factors Should Foundries Consider?
Reclamation and reuse of moulding sand
Sand consumption is an important environmental and operating consideration for sand casting foundries because used moulding material is generated after moulds are broken down. Many foundries use sand-reclamation systems to recover suitable material for reuse, reducing the need for continuously adding new sand.
The effectiveness of reclamation depends on the moulding process, binder system, sand type, and equipment. Recovered sand must be monitored because its characteristics can change after repeated use.
Not all spent moulding material can necessarily be returned directly to the process. Foundries must manage waste sand, used binders, dust, and other process residues according to applicable environmental and waste-management requirements.
For customers evaluating suppliers, environmental management should therefore be considered alongside production capability. A well-organised foundry should have defined procedures for handling used moulding materials and other production waste.
Energy use during melting and finishing
Melting metal is one of the most energy-intensive stages of foundry production. Electricity or fuel is required to bring the alloy to the necessary temperature, while additional energy may be consumed during mould preparation, heat treatment, shot blasting, machining, and material handling.
Energy efficiency can be improved through furnace optimisation, appropriate charge materials, improved process control, heat recovery, equipment maintenance, and reduced rework. Since casting defects can result in scrapped components, improving first-pass yield can also reduce the energy and materials consumed per accepted part.
The environmental performance of a casting should therefore be considered across the whole manufacturing route rather than focusing only on the moulding stage.
More efficient process development
Digital tools are also changing the way foundries develop castings. Three-dimensional pattern design, casting simulation, automated moulding systems, and improved inspection technologies can help manufacturers identify potential process problems earlier.
For complex components, simulation can be used to study mould filling and solidification before physical production begins. This may reduce trial-and-error work and help engineers optimise gating, risering, and component geometry.
These technologies do not replace practical foundry experience. Instead, they combine process knowledge with digital analysis to make production more predictable and reduce unnecessary material and energy consumption.
Conclusion
The sand casting process remains an important manufacturing option because it combines design flexibility, broad material compatibility, and the ability to produce components across a wide range of sizes. Its relatively adaptable tooling approach makes it particularly useful for customised parts, prototypes, replacement components, and low-to-medium production volumes, while appropriate foundry equipment can also support larger production requirements.
At the same time, successful casting depends on much more than the basic mould-and-pour concept. Pattern and core design, moulding sand properties, gating and risering, alloy chemistry, pouring conditions, solidification behaviour, finishing, and inspection all contribute to the final result. Surface finish and dimensional accuracy may require additional machining, while defects such as porosity, inclusions, and shrinkage must be addressed through effective process engineering and quality control.
Environmental considerations are also becoming increasingly important. Sand reclamation, efficient melting, waste management, process simulation, and improved production control can help foundries reduce material waste and energy consumption while maintaining consistent output.
For manufacturers evaluating a casting supplier, the most useful approach is to look beyond the basic advantages of the process. The supplier's equipment, engineering capability, material expertise, inspection system, production capacity, documentation, and ability to support downstream machining should all be considered. When these factors are properly aligned with the component requirements, sand casting can provide a practical and scalable route for producing reliable metal parts.
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd., established in 2001, provides customised metal components for customers in multiple industrial sectors. The company works with forging, sand casting, investment casting, centrifugal casting, and machining, covering materials such as cast iron, steel, stainless steel, aluminium, copper, zinc, and various alloys. With ISO 9001:2015 and API-7-1 certifications and experience serving customers across Europe, North America, Asia, and Oceania, Welong supports projects from product improvement and manufacturing coordination through quality control and international delivery. For customers sourcing cast or machined components, this integrated supply-chain approach can help connect technical requirements with production and delivery needs. For more information or inquiries, please contact us at metal@welongpost.com.
FAQ
1: What is sand casting?
Sand casting is a manufacturing process where molten metal is poured into a sand mold, allowed to solidify, and then the mold is broken away to reveal the finished part.
2: What are the main advantages of sand casting?
The main advantages include cost-effectiveness for low to medium production volumes, flexibility in design and material options, and the ability to produce large and complex parts.
3: What materials can be used in sand casting?
Sand casting can be used with a wide range of metals and alloys, including iron, steel, aluminum, copper, and brass.
4: How does sand casting affect product quality?
Sand casting can impact surface finish, dimensional accuracy, mechanical properties, and metallurgical structure. Quality control measures are implemented to manage potential defects.
References
1.Campbell, J. (2015). Complete Casting Handbook: Metal Casting Processes, Metallurgy, Techniques and Design. Butterworth-Heinemann.
2. Beeley, P. (2001). Foundry Technology. Butterworth-Heinemann.
3. Brown, J. R. (2000). Foseco Ferrous Foundryman's Handbook. Butterworth-Heinemann.
4. Groover, M. P. (2010). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems. John Wiley & Sons.
5. American Foundry Society. (2015). Casting Source Directory. AFS Publications.
6. Murthy, V. S., & Rao, R. (2016). Advanced Casting Technologies. IntechOpen.

Share your inquiry, get the quotation accordingly!

China WELONG- Your Reliable Partner in Metal Solutions

